


Why Choose an Air Breathing Compressor?

Why Choose an air breathing compressor?

An air breathing compressor supplies breathable air for diving, emergency response, and industrial respiratory systems. Unlike a standard workshop compressor, it must control contamination, moisture, temperature, and pressure. A small oil carryover can become a serious respiratory hazard.

The U.S. Occupational Safety and Health Administration requires supplied breathing air to meet at least Grade D quality under 29 CFR 1910.134. The Compressed Gas Association’s CGA G-7.1 standard adds limits for oxygen, carbon monoxide, carbon dioxide, oil, and odor. These requirements make filtration and monitoring essential, not optional. The U.S. Department of Energy also reports that compressed-air systems can lose 20–30% of generated air through leakage. That figure concerns industrial systems, but it highlights an important lesson: efficiency affects reliability.

Hank van Ormer, a respected compressed-air systems specialist, has often stressed this principle: “Breathing air is a life-support utility, not simply compressed air.” The wording is simple. The responsibility is not. A suitable air breathing compressor should provide stable pressure, certified filtration, dependable cooling, and clear maintenance records. ISO 8573-1 can help assess compressed-air purity, although it does not replace breathing-air regulations. Users still need to verify the complete system, including intake location, filters, cylinders, hoses, and testing intervals. Choosing by price alone may look sensible at first. It may not remain sensible beside a compressor room, a dive boat, or a worker wearing a mask for hours. The technology is dependable, but only when inspection remains disciplined.
Why Choose an Air Breathing Compressor?

What Defines a Breathing-Air Compressor? OSHA Requires 19.5–23.5% Oxygen

Why Choose an Air Breathing Compressor?

A breathing-air compressor supplies clean air for supplied-air respirators, not ordinary workshop tools. Its purpose is protecting the wearer’s lungs during spraying, blasting, coating, or confined-space work.

OSHA requires breathing air to contain 19.5–23.5% oxygen. This range matters. Too little oxygen can cause confusion, weakness, or unconsciousness. Excess oxygen can increase fire risks.

A reliable system also needs controlled carbon monoxide, carbon dioxide, oil mist, and unpleasant odors. Compressor intake placement is critical. An intake near vehicle exhaust can contaminate air before filtration begins.

Technicians should check filters, drains, pressure gauges, and alarms on a documented schedule. A clean gauge can create false confidence. Testing is still necessary, especially after maintenance or unusual compressor noise. The wrong assumption here can be costly.

Tips:

Keep the intake away from engines, solvents, and exhaust outlets. Drain moisture from low points before use. Replace filters according to actual operating conditions, not only calendar dates. Verify oxygen and contaminant levels through qualified air testing. Never ignore an oily smell, warm hose, or sudden pressure change. Small warning signs deserve attention.


How Grade-D Air Limits CO to 10 ppm and CO₂ to 1,000 ppm

Why Choose an Air Breathing Compressor?

How Grade-D Air Limits CO to 10 ppm and CO₂ to 1,000 ppm

Breathing air compressors need more than pressure and flow. They need verified air quality at the user’s face. Under ANSI/CGA G-7.1, Grade-D breathing air limits carbon monoxide to 10 ppm and carbon dioxide to 1,000 ppm. These limits are also referenced by OSHA’s respiratory protection requirements, 29 CFR 1910.134.

CO is especially dangerous because it is colorless and odorless. A poorly maintained compressor can draw exhaust from a nearby vehicle, generator, or boiler. CO₂ creates a different concern. Rising levels may indicate poor ventilation or contaminated intake air. In a workshop, that could mean a blocked intake, hot machinery, or an overlooked exhaust path. Small details matter.

Tips: Test air quality at installation and at scheduled intervals. Check the intake location after layout changes. Replace filters according to measured conditions, not guesswork. Record CO, CO₂, oxygen, and oil mist results. The National Institute for Occupational Safety and Health emphasizes routine evaluation of supplied-air systems, while OSHA requires breathing-air quality testing at least quarterly for certain systems. However, quarterly testing may still be insufficient after repairs or contamination events. Grade D is a baseline, not a guarantee.

Why 2,216–4,500 psi Storage Supports Modern SCBA Systems

Why Choose an Air Breathing Compressor?

Why 2,216–4,500 psi Storage Supports Modern SCBA Systems

Modern SCBA systems rely on compressed air storage at 2,216 or 4,500 psi. These pressures provide practical cylinder capacity without making the equipment unmanageably large. A 4,500 psi cylinder can store more usable air within a similar footprint. That matters when firefighters move through narrow corridors, climb stairs, or carry tools. Every breath counts.

OSHA 29 CFR 1910.134 requires breathing air to meet Grade D specifications under CGA G-7.1. That specification limits carbon monoxide to 20 ppm and carbon dioxide to 1,000 ppm. Oxygen must remain between 19.5% and 23.5%. An air breathing compressor must therefore control filtration, moisture, oil, and temperature carefully. Pressure is only one part of the system. Clean air is the real priority.

NIOSH respiratory protection guidance reminds users that rated service time does not equal guaranteed working time. Heavy exertion increases breathing demand. Cold conditions, poor maintenance, and repeated filling can also affect performance. A cylinder marked for 30 minutes may feel much shorter during intense work. This is where planning can fail. Regular air-quality testing, calibrated gauges, and documented compressor maintenance support safer SCBA readiness. The uncomfortable truth is simple: higher pressure improves capacity, but it cannot correct careless inspection or contaminated breathing air.

How Multi-Stage Filtration Meets CGA G-7.1 Breathing-Air Standards

Why Choose an Air Breathing Compressor?

How Multi-Stage Filtration Meets CGA G-7.1 Breathing-Air Standards

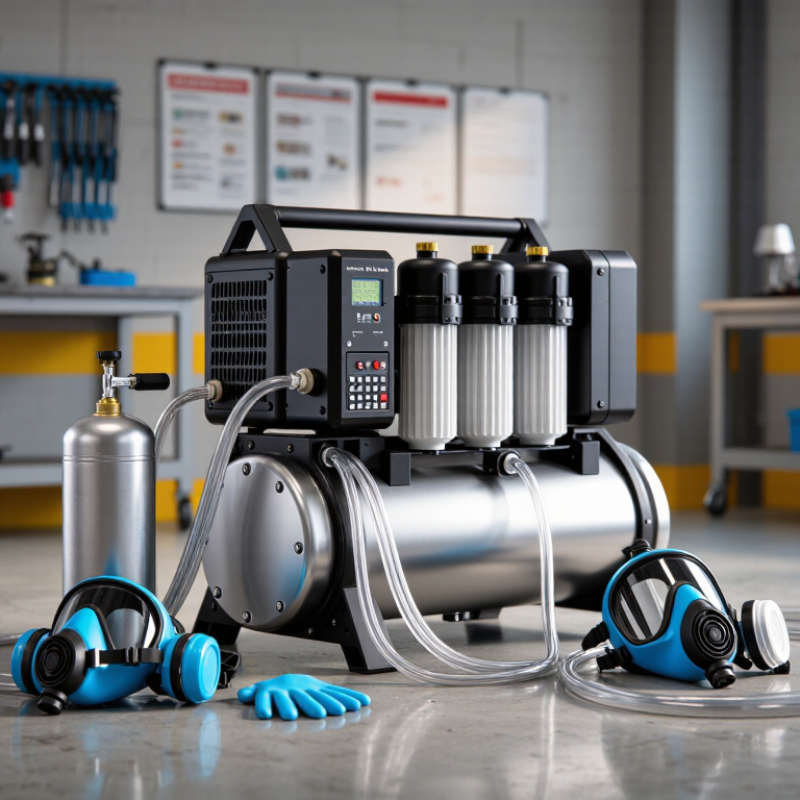
A breathing-air compressor is chosen for controlled, clean air, not simply high pressure. CGA G-7.1 Grade D guidance sets measurable limits for oxygen, carbon monoxide, carbon dioxide, oil mist, and odor. Multi-stage filtration supports these limits by removing different contaminants at different points. An intake filter catches dust. A coalescing stage reduces liquid water and oil aerosols. Activated carbon helps control odors and hydrocarbons. A desiccant stage lowers moisture before air reaches the storage cylinder or respirator.

Filtration alone is not proof of compliance. Compressor temperature, intake location, cartridge age, condensate drainage, and maintenance records matter. Carbon monoxide can enter through a poorly positioned intake or exhaust leak. A carbon monoxide monitor and scheduled laboratory testing provide stronger evidence than appearance. Testing should follow applicable CGA G-7.1 requirements and involve qualified personnel. A filter can look clean and still be exhausted. That detail is easy to miss.

Tips: Check pressure-drop readings, replace elements according to actual service conditions, and sample air after maintenance. Keep intake openings away from engines, solvents, and vehicle traffic. Record test results, alarm checks, and cartridge changes. Do not rely on smell; some harmful contaminants have no warning odor. A simple checklist helps, but review it when equipment or working conditions change.

Why Choose an Air Breathing Compressor? - How Multi-Stage Filtration Meets CGA G-7.1 Breathing-Air Standards

System Element Primary Function Typical Performance or Design Value Contaminant or Risk Addressed Relation to CGA G-7.1
Compressor intake location Draws ambient air from a clean, well-ventilated area. The intake should be positioned away from vehicle exhaust, combustion vents, solvent vapors, storage tanks, and other pollution sources. Carbon monoxide, carbon dioxide, hydrocarbons, and airborne particles. Source-air control is essential because filtration cannot reliably correct every sudden or high-level contaminant event.
Stage 1: Intake particle pre-filter Removes coarse dust and debris before compression and downstream treatment. A commonly used design range is approximately 5–10 micrometres nominal particle filtration, depending on the selected element. Dust, rust, pollen, and larger solid particles. Supports clean-air production but does not by itself establish breathing-air compliance.
Stage 2: Coalescing filter Separates liquid water and oil aerosols from compressed air. Fine coalescing elements are commonly specified around 0.01 micrometre particle ratings, with efficiency and pressure drop dependent on the product and flow rate. Liquid water, compressor oil mist, and fine aerosols. Helps control oil and moisture but cannot remove carbon monoxide or carbon dioxide.
Stage 3: Desiccant or membrane dryer Reduces water vapor and helps prevent condensation in storage vessels and breathing-air lines. The required pressure dew point is selected according to ambient temperature, system pressure, and application conditions. Condensation, corrosion, freezing, and excessive humidity. Moisture control supports hygienic and reliable delivery; the applicable breathing-air specification and operating procedure determine acceptance criteria.
Stage 4: Activated-carbon adsorber Adsorbs oil vapors and many organic vapors that remain after aerosol separation. Performance depends on carbon quantity, contact time, temperature, humidity, contaminant concentration, and timely replacement. Oil vapor, hydrocarbon vapor, and objectionable odors. Supports the CGA G-7.1 requirement for no pronounced odor and the applicable hydrocarbon limit, but requires verification by testing.
Stage 5: Final particulate filter Captures residual particles released by the treatment system or piping. A final filter is commonly selected with a fine rating such as 0.01 micrometre, subject to the manufacturer’s tested efficiency and flow limits. Fine particles, carbon dust, and downstream line debris. Provides the final physical barrier; it does not remove gaseous carbon monoxide or carbon dioxide.
Carbon monoxide monitoring Measures a toxic gas that may enter through intake contamination or compressor-related conditions. CGA G-7.1 Grade D commonly specifies a maximum of 20 ppm carbon monoxide. Carbon monoxide poisoning risk. Continuous or scheduled monitoring is needed because standard particulate and coalescing filters do not remove carbon monoxide.
Carbon dioxide monitoring Confirms that carbon dioxide remains within the breathing-air specification. CGA G-7.1 Grade D commonly specifies a maximum of 1,000 ppm carbon dioxide. Excessive carbon dioxide from contaminated intake air or ventilation problems. Requires source-air management and analytical verification; filtration alone is not a substitute for monitoring.
Oxygen monitoring Verifies that the delivered breathing air contains an appropriate oxygen concentration. CGA G-7.1 Grade D commonly specifies 19.5–23.5% oxygen by volume. Oxygen deficiency or enrichment. Oxygen concentration must be confirmed by an appropriate analyzer; filters do not regulate oxygen content.
Hydrocarbon and odor control Controls compressor oil carryover, hydrocarbon contamination, and noticeable odors. CGA G-7.1 Grade D commonly specifies no pronounced odor and a condensed hydrocarbon limit of 5 mg/m³. Oil contamination, solvent vapors, and unpleasant or potentially harmful odors. Requires suitable filtration, clean intake air, maintenance, and periodic laboratory or field testing.
Maintenance and validation Preserves filtration capacity and confirms that air quality remains within specification. Replace elements according to differential pressure, service life, operating hours, contamination load, and test results rather than time alone. Filter breakthrough, saturated carbon, pressure drop, leaks, and contaminated storage vessels. Compliance is demonstrated through documented inspection, maintenance, monitoring, and breathing-air analysis.
Important: The performance values shown are commonly referenced design or specification values, not a guarantee for every compressor or filter configuration. Actual compliance with CGA G-7.1 depends on intake-air quality, compressor design, filtration equipment, flow rate, maintenance, monitoring, and documented breathing-air testing.

Why Certified Air Testing Reduces Contamination and Respiratory Risk

Why Choose an Air Breathing Compressor?

A breathing-air compressor must deliver more than pressure. It must deliver air that workers can safely inhale. Contamination may enter through intake fumes, compressor oil, moisture, worn seals, or poorly maintained filters. A clear hose proves nothing.

OSHA’s respiratory protection standard, 29 CFR 1910.134, requires breathing air to meet Grade D specifications. These include oxygen between 19.5% and 23.5%, carbon monoxide below 20 ppm, and carbon dioxide below 1,000 ppm. Hydrocarbon levels must remain below 5 mg/m³. Certified air testing checks these invisible hazards instead of trusting appearance or smell.

Technicians should sample air at the breathing connection, not only near the compressor. They should record pressure, temperature, filter changes, and unusual odors. ISO 8573-1:2010 separates compressed-air contamination into particles, water, and oil, helping laboratories select suitable tests. NIOSH also identifies carbon monoxide as a serious workplace hazard because it can impair oxygen delivery without obvious warning signs.

Testing intervals deserve honest review. A schedule that worked last year may fail after a new intake location, hot operating conditions, or delayed maintenance. Small oversights matter. Results should come from an accredited laboratory, with traceable methods and documented corrective actions. An air breathing compressor is only as reliable as its last verified sample.

Article Source:

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
