


Why Choose a Surface Drilling Rig for Mining?

Why choose a Surface Drilling Rig for mining? The answer begins with changing production demands. The International Energy Agency’s Global Critical Minerals Outlook 2024 reported that lithium demand increased by about 30% in 2023. Demand for nickel, cobalt, and graphite also grew strongly. These trends require reliable drilling across expanding open-pit operations.

A Surface Drilling Rig offers direct access to benches, waste zones, and ore boundaries. It can drill blast holes efficiently, maintain repeatable patterns, and support accurate grade-control programs. Modern rigs may use down-the-hole hammers, rotary systems, automated rod handling, and digital monitoring. These features can reduce manual exposure near active drilling areas. They can also improve hole depth records and maintenance planning.

The U.S. Geological Survey’s Mineral Commodity Summaries 2025 continues to document large global output of copper, iron ore, gold, and other mined materials. Such volumes place pressure on drilling teams to improve availability without sacrificing safety or hole quality. A well-matched Surface Drilling Rig can help, especially where benches are stable and access roads are properly maintained.

But the choice is not automatic. Ground hardness, water conditions, altitude, dust, fuel access, and spare-parts support can change operating results. Data can mislead. A rig that performs well in one quarry may struggle in fractured rock or steep terrain. Mine managers should compare penetration rate, fuel consumption, bit life, utilization, and total cost per drilled meter. Operator experience still matters. Technology helps, but it does not replace disciplined planning, inspection, and continuous review.
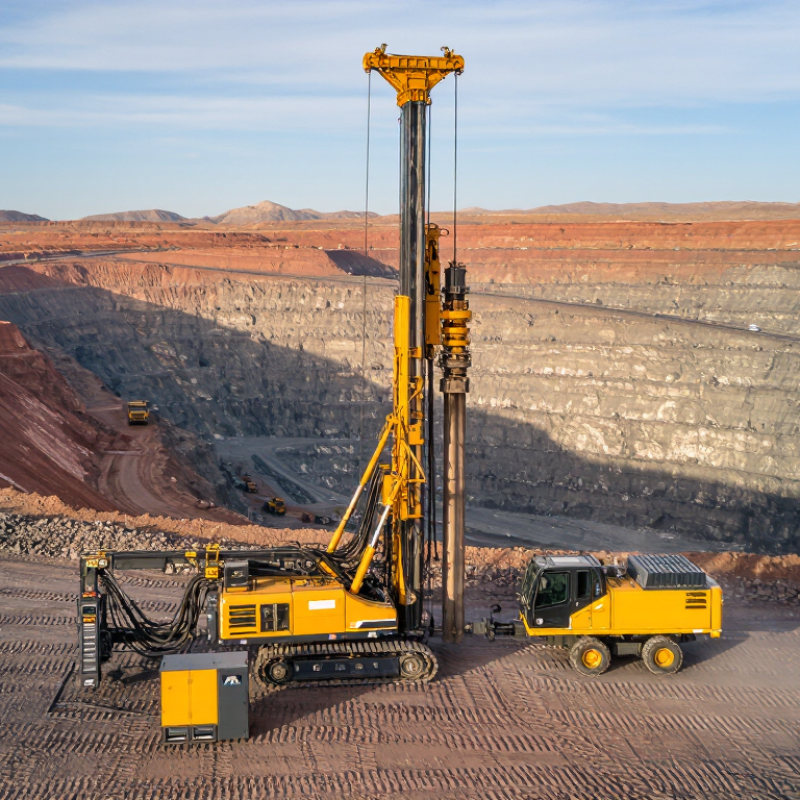
Why Choose a Surface Drilling Rig for Mining?

Define Surface Rigs: DTH, Rotary, and Top-Hammer Configurations

Surface drilling rigs are built for open-pit mines, quarries, and construction sites where the drill operates above ground. They offer direct access to rock faces, simpler movement between benches, and practical maintenance access. On a working bench, operators can inspect hoses, rods, and dust controls without entering a confined space. That visibility supports safer decisions and more consistent drilling.

Down-the-hole, or DTH, rigs place the hammer near the bit. Compressed air drives the hammer inside the borehole, helping maintain impact energy in deeper holes. DTH drilling suits hard rock, long patterns, and applications requiring reliable hole straightness. It can create significant noise and dust, so enclosure systems and water suppression matter.

Rotary rigs apply continuous rotation and feed force to the bit. They are effective in softer formations and large-diameter production holes. Their performance depends heavily on bit selection, rock abrasiveness, and feed control.

Top-hammer rigs keep the percussion mechanism outside the hole, transferring impact through the drill string. They often deliver fast drilling in fractured rock and shorter holes, though energy loss can increase with depth.

The choice is rarely obvious. Ground conditions change across one bench, and a rig selected from ideal test data may perform differently in wet or broken rock. Field trials, penetration records, fuel use, and operator feedback should guide the final decision. A lower purchase price may become expensive when deviation, blocked holes, or frequent rod changes slow the entire mining cycle.


Match Hole Size: 89–311 mm and 15–60 m (Sandvik/Epiroc Specs)

A surface drilling rig earns its place when mine planning demands consistent, accessible production. In open-pit work, hole diameter directly affects fragmentation, powder distribution, and downstream loading. A practical range of 89 to 311 mm supports many blast designs, from controlled benches to high-volume production holes. Smaller holes can improve precision. Larger holes can reduce drilling time. The trade-off deserves attention.

Depth matters just as much. For holes between 15 and 60 m, the rig needs stable feed pressure, sufficient rod capacity, and dependable air delivery. At 15 m, speed may dominate the decision. Near 60 m, alignment, flushing, and rod handling become more important. A machine can meet the published depth range yet perform poorly in fractured ground. That detail is easy to miss.

Field crews should check the rock profile before choosing equipment. Hard, abrasive formations may require stronger tooling and more frequent maintenance. Loose overburden may demand careful casing or slower collaring. I have seen suitable rigs lose productivity because compressors were undersized. Sometimes, the specification looks perfect. The job still struggles. Test drilling, operator feedback, and measured penetration rates provide more reliable evidence than a brochure alone. Track stability, dust control, service access, and fuel use also influence the real cost per metre.

Why Choose a Surface Drilling Rig for Mining?

Surface drilling rigs can cover a broad operating envelope, from smaller production holes to larger-diameter blast holes. The chart compares the stated minimum and maximum hole sizes with their corresponding depth range.

Typical applications include bench drilling, production blasting, quarrying, and infrastructure excavation. Actual performance depends on rock conditions, drill tooling, operating method, and site requirements.

Estimate Production: 70–85% Availability and Metres per Hour (OEM Benchmarks)

Why Choose a Surface Drilling Rig for Mining?

Surface drilling rigs offer measurable production, but availability matters more than headline speed. OEM benchmark tables commonly estimate 70–85% mechanical availability for well-maintained surface rigs. The SME Mining Engineering Handbook, 3rd Edition, also stresses rock strength, bit wear, hole depth, and maintenance planning as major productivity factors. A practical estimate may use 18–30 drilled metres per operating hour in hard-rock conditions. The figure is not guaranteed. Wet ground, fractured benches, and frequent rod changes can reduce output quickly.

A simple calculation helps: 24 metres per hour, 10 scheduled hours, and 75% availability produce about 180 metres daily.

That assumes efficient shift changes and limited repositioning. In real operations, delays often hide inside “available” hours. I would challenge any estimate that ignores dust suppression, compressor performance, and operator experience. Field records should replace optimistic assumptions after the first month.

Tips:

Track drilled metres, engine hours, delay minutes, and bit changes separately. Compare weekly results with the 70–85% availability range. Keep a photo log of bench conditions. Small details matter. A short trial on representative rock can reveal more than a polished sales sheet. Recheck the model after rainfall, maintenance events, and changes in hole depth.

Compare Costs: Fuel, Consumables, Maintenance, and Cost per Metre

Choosing a surface drilling rig is often a cost decision, not simply an equipment decision. Fuel is only one part of the calculation. On a limestone bench, daily fuel records can reveal large differences between idle time, drilling time, and relocation time. A rig that drills steadily may consume more fuel per hour but less fuel per metre.

Consumables can change the result quickly. Drill rods, bits, shank adapters, lubricants, and compressor filters need regular tracking. Hard, fractured ground may shorten bit life and increase replacement costs. Wet holes can also raise air consumption and create more maintenance work. These details are easy to miss. They should not be.

Maintenance costs include planned servicing, spare parts, technician hours, and lost production. A simple service schedule reduces surprises, but it cannot remove them. Dust, vibration, and poor bench access still damage components. Keeping service records helps identify repeated failures and realistic operating costs. Some estimates look precise but remain incomplete.

Cost per metre should combine fuel, consumables, maintenance, labor, and downtime, then divide them by drilled metres. This measure compares rigs more fairly than hourly fuel use. For example, a higher hourly cost may be acceptable when penetration is faster and breakdowns are fewer. However, ground conditions can change the answer next month. Review the figures by rock type, shift, and hole depth before making a purchase decision.

Verify Safety: Dust, Noise, and MSHA/ISO Controls for Open-Pit Sites

A surface drilling rig can improve safety when its controls match open-pit conditions. Dust is the immediate concern. Drilling breaks rock into fine particles, including respirable crystalline silica. MSHA’s metal and nonmetal standard sets a permissible exposure limit of 50 micrograms per cubic meter over eight hours, with an action level of 25 micrograms. Wet drilling, sealed cabins, and maintained dust collectors help keep operators away from the plume.

Noise needs equal attention. NIOSH recommends an 85 dBA exposure limit for eight hours, using a 3 dB exchange rate. MSHA generally applies a 90 dBA limit with a 5 dB exchange rate. These are not interchangeable. A rig can appear quiet outside while cabin vibration remains uncomfortable. ISO 9612 provides a structured method for workplace noise measurement, but measurements should represent real drilling cycles, not only idle conditions.

Controls must also be verified. ISO 45001 supports documented hazard identification, worker consultation, and corrective action. In practice, inspect filters, water lines, cabin seals, and alarms before each shift. Check the operator’s breathing zone, not only the exhaust area. Small leaks matter. One weak seal can defeat an otherwise strong system. Safety assumptions should be tested against dust sampling, noise dosimetry, maintenance records, and operator feedback. Field conditions are rarely perfect, and that is exactly why surface rig selection requires evidence rather than attractive specifications.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
