Why Choose Galvanized Welded Pipe for Global Projects?
Why Choose Galvanized Welded Pipe for Global Projects?
Global infrastructure projects require materials that balance cost, strength, availability, and service life. Galvanized Welded Pipe addresses these demands with a steel core and a protective zinc coating. This combination supports water systems, agricultural structures, fencing, scaffolding, and industrial frameworks across diverse climates.
The World Steel Association reported global crude steel production of approximately 1.89 billion tonnes in 2023. This scale reflects steel’s continuing importance in construction and manufacturing. Its widespread production also supports international sourcing and replacement planning. In addition, the World Steel Association’s October 2024 Short Range Outlook projected global steel demand growth in 2025. That trend reinforces the need for practical, standardized pipe solutions.
Zinc protection is especially valuable where moisture, salt, or outdoor exposure can accelerate corrosion. The American Galvanizers Association notes that hot-dip galvanized steel can achieve long service lives, often exceeding several decades, depending on the environment. However, performance is never automatic. Coating thickness, weld quality, transportation damage, drainage, and local soil conditions all matter. This point is easy to overlook.
International buyers commonly reference standards such as ASTM A123/A123M, ISO 1461, and relevant pipe specifications. These standards help define coating quality, inspection methods, dimensions, and acceptance criteria. Yet documentation must match the actual project conditions. A pipe suitable for a dry rural installation may require additional protection near coastal facilities. Galvanized Welded Pipe is not a universal shortcut. It is a dependable engineering choice when specifications, coating inspection, and installation practices are carefully aligned.
What Is Galvanized Welded Pipe?
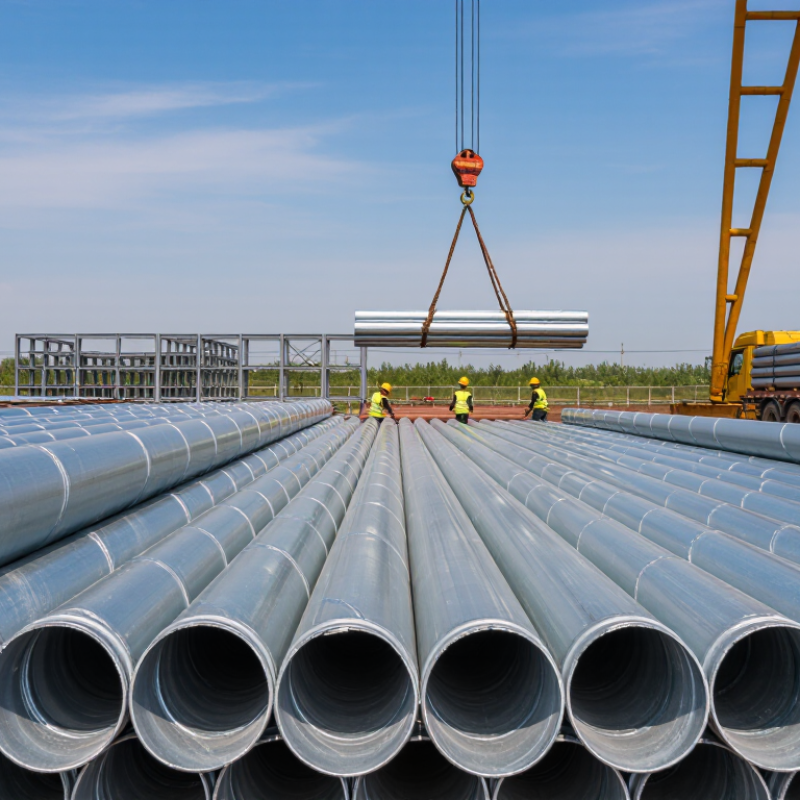
Galvanized welded pipe is steel pipe formed from a flat steel sheet and joined along a longitudinal seam. After welding, the pipe receives a protective zinc coating. This coating creates a barrier against moisture, oxygen, and surface corrosion. In practical projects, it may look like a simple silver tube, but its performance depends on both the steel and the galvanizing process.
The welded structure supports consistent dimensions and efficient production for water lines, fencing, structural frames, and utility systems. Galvanized pipe is often selected for global projects because it can reduce maintenance in humid or outdoor environments. However, it is not corrosion-proof. Cut ends, damaged coatings, trapped water, and aggressive chemicals can shorten its service life. That point is sometimes overlooked. Project engineers should verify wall thickness, zinc coating weight, weld quality, pressure requirements, and applicable regional standards before ordering. Inspection records also improve traceability across international shipments.
Tips: Check the pipe’s intended environment first. Ask for coating test results and dimensional reports. Protect exposed cut ends during installation. Avoid assuming every galvanized pipe has the same service life. Local climate, water chemistry, and installation quality can change the result. Testing is worth the effort.
How Is Galvanized Welded Pipe Manufactured?
Galvanized welded pipe begins with carefully selected steel strip or coil. Its thickness, width, and chemical composition must match the project specification. Operators uncoil and level the steel before passing it through forming rollers. The rollers gradually shape the flat strip into a round tube. This controlled forming reduces stress and keeps the diameter consistent.
The edges meet along the length, where high-frequency electrical resistance welding creates a continuous seam. No filler metal is normally required. After welding, sizing rolls correct the pipe’s roundness and dimensions. The seam matters. Technicians may use visual checks, ultrasonic testing, or hydrostatic testing to identify weak areas. Cut ends are then inspected for burrs, dents, and uneven geometry.
For hot-dip galvanizing, workers clean the welded pipe through degreasing, pickling, and rinsing. A flux treatment helps molten zinc bond with the steel surface. The pipe enters a zinc bath near 450°C, then drains and cools under controlled conditions. Excess zinc is removed to limit coating variation. Inspectors measure coating thickness, appearance, adhesion, and dimensional accuracy against the required standard. Small surface marks can remain after processing, and they should not be ignored. In practice, handling damage, trapped moisture, or incomplete cleaning may weaken local protection. Careful records and traceable inspections make the finished pipe more dependable across transport, storage, and installation.
Why Does Zinc Coating Improve Pipe Durability?
Why Choose Galvanized Welded Pipe for Global Projects?
Zinc coating improves pipe durability through two protective mechanisms. It forms a physical barrier against moisture, oxygen, and many contaminants. It also provides sacrificial protection when minor scratches expose the steel beneath. Zinc corrodes first.
The NACE IMPACT study estimated global corrosion costs at 2.5 trillion dollars annually, equal to about 3.4% of global GDP. This figure shows why corrosion control deserves early design attention. Technical data from the International Zinc Association indicates that zinc can corrode 10 to 100 times more slowly than steel, depending on atmospheric conditions. In field work, that difference can mean fewer repairs around exposed pipe supports, joints, and service corridors.
For welded pipe, coating quality still depends on preparation and application. ISO 1461 defines hot-dip galvanized coating requirements, including thickness criteria linked to steel thickness. Proper venting and drainage also matter for hollow sections. Real sites are less predictable. Salt spray, acidic soil, trapped water, and high temperatures can shorten service life. A coating is not a substitute for sound design.
That assumption is too neat. Surface damage, poor storage, or unsealed crevices may defeat otherwise strong protection. Project teams should review soil chemistry, humidity, transport conditions, and inspection access before selecting the coating system. Data supports galvanizing, but site evidence should guide the final decision.
Where Are Galvanized Welded Pipes Used Globally?
Why Choose Galvanized Welded Pipe for Global Projects?
Where Are Galvanized Welded Pipes Used Globally?
Galvanized welded pipes are used across construction, agriculture, water management, and industrial infrastructure. Their zinc coating helps resist moisture, salt air, and outdoor exposure. This makes them useful for fencing, handrails, scaffolding, greenhouse frames, and structural supports. In coastal cities, engineers often select them for external drainage and utility protection. However, location still matters. A thick coating cannot solve every corrosion problem.
In farming regions, these pipes support irrigation lines, livestock enclosures, and equipment frames. Municipal projects use them for water conveyance, street barriers, and cable protection. Warehouses and factories commonly install them in compressed-air systems, fire-safety structures, and material-handling areas. Welded construction allows consistent dimensions and efficient fabrication. It can also reduce project costs when standard sizes are available locally. Yet, welded seams need careful inspection, especially after cutting or threading. That detail is sometimes missed.
Tips: Check the required pipe standard, zinc coating, wall thickness, and operating environment before ordering. Protect exposed cut ends with a suitable repair coating. Confirm local water regulations and installation practices. A small inspection mistake can become a costly maintenance issue. Reducing cost too aggressively may also weaken long-term reliability.
How Should Galvanized Welded Pipes Be Selected and Maintained?
Galvanized welded pipes suit many global projects because their zinc coating helps resist atmospheric corrosion. Selection should begin with the service conditions, not the lowest quotation. Identify the fluid, operating pressure, temperature, pipe diameter, and installation environment. Fit matters. Outdoor coastal sites need stronger corrosion protection than dry indoor facilities. Confirm the required wall thickness, welding quality, dimensional tolerance, and coating mass against recognized project standards. Request mill certificates and inspection records. A shiny surface alone proves very little.
The pipe should also match its connection method. Threaded ends, grooved couplings, and welded joints require different preparation and tolerances. Check whether the zinc coating may affect welding fumes, joint strength, or later repairs. In some systems, galvanized steel may react with specific chemicals or dissimilar metals. That risk deserves technical review before purchase. Water is the enemy. Avoid designs that trap moisture inside sleeves, supports, or poorly drained channels.
Maintenance starts with a practical inspection schedule. Look for white rust, exposed steel, blistering, damaged threads, and coating loss near welds or cut ends. Clean deposits gently and keep drainage paths open. Do not grind away sound zinc without reason. Damaged areas can require cleaning and an approved zinc-rich repair coating, applied according to the project specification. Record locations, dates, and corrective work. Field inspections often reveal a difficult truth: small scratches are ignored until corrosion spreads beneath the coating. Protection is never permanent, and even a careful selection can fail when storage is careless or site handling becomes rushed.





