


Carbon Steel Pipe remains a practical choice for projects that need strength, availability, and predictable performance. It carries water, steam, oil, and gas in many industrial settings. Its value is not simply its strength. Standard sizes and familiar fabrication methods can also make sourcing, cutting, welding, and installation more straightforward.
As a fictional industry specialist, materials engineer Alex Morgan, puts it: “A good pipe choice balances pressure, corrosion risk, installation needs, and long-term maintenance.” This is an illustrative quote, not a verified statement from a real expert. The principle matters on site. A pipe exposed to damp air, soil, or aggressive process fluids may need coatings, linings, or a different material. Carbon steel can corrode. Ignoring that risk is an easy mistake.
The right specification depends on operating pressure, temperature, fluid, and service environment. Engineers should check the applicable project standards, material grade, wall thickness, and joining requirements before selection. A thick pipe is not automatically the safest or most cost-effective option. Neither is the cheapest one. Actual conditions can complicate a clean calculation, and maintenance plans are sometimes less certain than expected.
This guide examines where Carbon Steel Pipe performs well, what trade-offs deserve attention, and which questions help teams compare options. The aim is practical: a better-informed choice, supported by project requirements rather than habit.
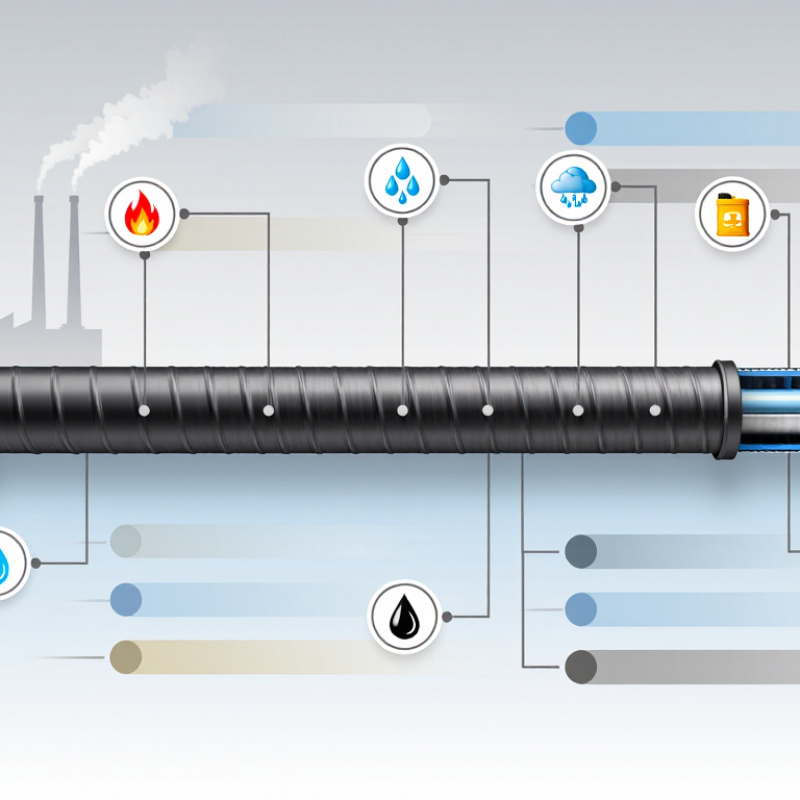
Carbon steel pipe is valued for its strength, availability, and ability to handle demanding service conditions. ASTM A106/A106M covers seamless carbon steel pipe for high-temperature applications. Its Grade B chemistry allows up to 0.30% carbon by weight. The specification also sets minimum tensile strength at 60,000 psi and minimum yield strength at 35,000 psi. These figures help engineers compare material requirements with design loads.
Carbon content matters. It can influence strength, hardness, and weldability, so the maximum is not a target that every pipe must reach. A mill test report should confirm the actual heat chemistry and mechanical results; check these against the project specification before fabrication. In the shop, that means reviewing the paperwork before cutting pipe or preparing a weld. Small details matter. Grade B is not automatically the right choice for every temperature, pressure, or corrosive environment. ASTM A106/A106M provides the material requirements, but it does not replace design review, welding procedures, or service-specific corrosion assessment. It is easy to overlook that distinction.
| Dimension | ASTM A106 Grade B / Carbon Steel Pipe Facts | Project Relevance |
|---|---|---|
| What it is | Carbon steel pipe is made primarily from iron and carbon, with other elements present in controlled amounts. ASTM A106 Grade B is a seamless carbon steel pipe grade. | The material and manufacturing route help determine suitability for a particular pressure, temperature, and service environment. |
| Standard scope | ASTM A106/A106M covers seamless carbon steel pipe for high-temperature service. | Check the applicable code, design conditions, and purchase specification before selecting a grade. |
| Carbon content | Grade B has a maximum carbon content of 0.30% by weight under the standard’s chemical requirements. | Carbon content is one factor affecting strength, hardness, and weldability; welding procedures should be selected for the actual material and application. |
| Other specified chemistry | For Grade B, the standard lists manganese at 0.29–1.06%, phosphorus at 0.035% maximum, sulfur at 0.035% maximum, and silicon at 0.10% minimum. | Verify the edition of the standard and the mill test report for the supplied product. |
| Minimum tensile strength | 60,000 psi (415 MPa). | Use specified minimum properties in design calculations, subject to the governing design code. |
| Minimum yield strength | 35,000 psi (240 MPa). | Allowable design stress is not the same as minimum yield strength and must be determined using the applicable code. |
| Typical considerations | Carbon steel pipe is commonly considered for industrial fluid and process piping; ASTM A106 specifically addresses high-temperature service. | Assess temperature, pressure, corrosion, fluid compatibility, wall thickness, and inspection requirements for each project. |
| Corrosion protection | Carbon steel can corrode depending on the environment and service conditions. | Evaluate corrosion allowance, coatings, linings, inhibitors, or other protection measures as required by the design. |
| Selection checklist | Confirm the required standard and grade, seamless construction, pipe size and schedule, design pressure and temperature, end finish, testing, documentation, and applicable code. | |
Note: Values shown are standard minimums or maximums for ASTM A106 Grade B; confirm the applicable standard edition and certified product documentation for project use.

ASTM A106 Grade B carbon steel pipe has a specified minimum tensile strength of 415 MPa. In practical terms, tensile strength describes the stress a test specimen can withstand before it breaks. It is not the same as the pressure a finished pipe can safely carry. That distinction matters. Pressure capacity also depends on outside diameter, wall thickness, operating temperature, and applicable design rules.
On a project, this strength level can suit high-temperature service when the pipe dimensions and conditions are properly checked. A mill test certificate can help confirm the supplied material’s grade and test results; verify that its heat number matches the pipe markings. Still, a number on a certificate is only one part of the picture. Inspect weld quality, fittings, and any signs of corrosion, especially where moisture collects around supports. Small details matter. I have seen calculations look tidy while field measurements told a less comfortable story. For critical service, have a qualified engineer assess the actual operating pressure and temperature rather than relying on tensile strength alone.
Carbon steel pipe offers strength, practical availability, and a range of wall thicknesses for demanding systems. But the right choice depends on service conditions and the governing specification.
ASTM A106 covers seamless pipe intended for high-temperature service.
ASTM A53 includes seamless and welded pipe for general use, with several grades and manufacturing types.
API 5L addresses line pipe for transporting oil, gas, and water, and defines requirements such as grade, testing, and traceability.
These standards are not interchangeable labels. A steam line operating at elevated temperature may call for ASTM A106, while a water line could be specified to ASTM A53 or API 5L, depending on design requirements. Verify the exact grade, dimensions, end finish, and inspection criteria on the project documents. Small details matter. A pipe can meet a material standard yet still fail to match the required pressure class or joining method.
Tips: Check the latest project specification and applicable standard edition before ordering. Confirm mill test reports, heat numbers, and required tests against the purchase documents. In practice, paperwork is sometimes overlooked until delivery day. That is a costly moment to discover a mismatch.
Why Choose Carbon Steel Pipe for Your Project?
Carbon steel pipe is often selected for its strength, availability, and practical fabrication options. But choosing a pipe by material alone is not enough. Dimensions affect flow, weight, connection fit, and pressure design. A pipe that looks right on a drawing may still create problems at a flange or support.
ASME B36.10M standardizes dimensions for welded and seamless wrought steel pipe. It uses nominal pipe size (NPS) and schedule to identify common sizes and wall thicknesses. NPS is a designation, not a direct measurement of the pipe’s inside diameter. For many sizes, the outside diameter stays fixed while the schedule changes the wall thickness. That means the bore changes too. Check the standard’s applicable tables, then confirm the specified material, manufacturing method, and tolerances against the project documents. Standards help align suppliers and designers, but they do not replace engineering checks. Small details matter.
Tips: Verify NPS, schedule, and end preparation before ordering. Compare the listed dimensions with mating fittings and flange requirements. For example, a thicker wall can reduce internal clearance in a line carrying water or process fluid. I’ve seen a simple schedule mismatch delay installation; it is easy to overlook. Check it twice.
ASME B36.10M covers dimensions for welded and seamless steel pipe. This chart compares nominal wall thicknesses for selected pipe sizes and schedules.
How to read it: NPS is a nominal size, not the pipe’s measured outside diameter. Schedule indicates wall thickness; a higher schedule means a thicker wall for the same NPS. Values shown are in inches.
Carbon steel pipe suits projects where pressure, temperature, and budget must be balanced. ASTM A106 Grade B, a common seamless-pipe specification, sets minimum tensile strength at 60,000 psi and yield strength at 35,000 psi. These figures do not determine a safe working pressure by themselves. Engineers must also check pipe diameter, wall thickness, welds, design code, and operating conditions. Under ASME B31.3, those factors shape the piping design.
Temperature matters, too. Carbon steel performs well across many industrial service conditions, but high heat can reduce strength, while low temperatures can increase brittleness. Corrosion is another deciding factor. The NACE International IMPACT study estimated corrosion costs at US$2.5 trillion globally, or 3.4% of GDP, underscoring why fluid chemistry and maintenance matter. In dry, controlled service, carbon steel can be economical; in wet or chemically aggressive service, coatings, corrosion allowance, or another alloy may be needed. That extra protection can narrow the upfront savings.
Tips: Confirm the design pressure and minimum operating temperature with a qualified piping engineer. Compare total installed and maintenance costs, not just the pipe price. A small assumption can change the choice.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

