Why Choose a Belt Cleaner for Conveyor Systems?
Why Choose a Belt Cleaner for Conveyor Systems?
A conveyor system can appear simple, yet small carryback problems create expensive operational risks. Material clings to the belt after discharge. It then falls along return paths, transfer points, and walkways. Over time, this buildup can damage idlers, contaminate products, and increase cleaning labor. A properly selected Belt Cleaner helps remove that residual material before it spreads. It also supports safer housekeeping and more stable conveyor performance.
Martin Engineering founder Edwin F. Peterson is often credited with the practical reminder, “There is no such thing as a maintenance-free conveyor.” That statement remains relevant today. A Belt Cleaner does not replace inspections, correct tensioning, or regular maintenance. It works as one part of a complete belt-cleaning strategy. The right design depends on belt speed, material moisture, temperature, splice type, and application conditions. A cleaner that works well with dry limestone may perform poorly with sticky clay. Details matter.
The benefits are visible. Fewer piles collect beneath the conveyor. Return rollers stay cleaner. Maintenance teams spend less time shoveling and more time checking critical components. Production areas may also become easier to inspect. Still, choosing the cheapest unit can be a weak decision. Poor blade contact may cause belt wear, while excessive pressure can shorten component life. That mistake is easy to make.
A reliable selection process combines manufacturer guidance, site measurements, and maintenance experience. Operators should review performance after installation, not assume success immediately. Some systems need adjustment. Others need a different cleaning stage. The goal is not perfection. It is controlled carryback, dependable operation, and a cleaner conveyor environment.
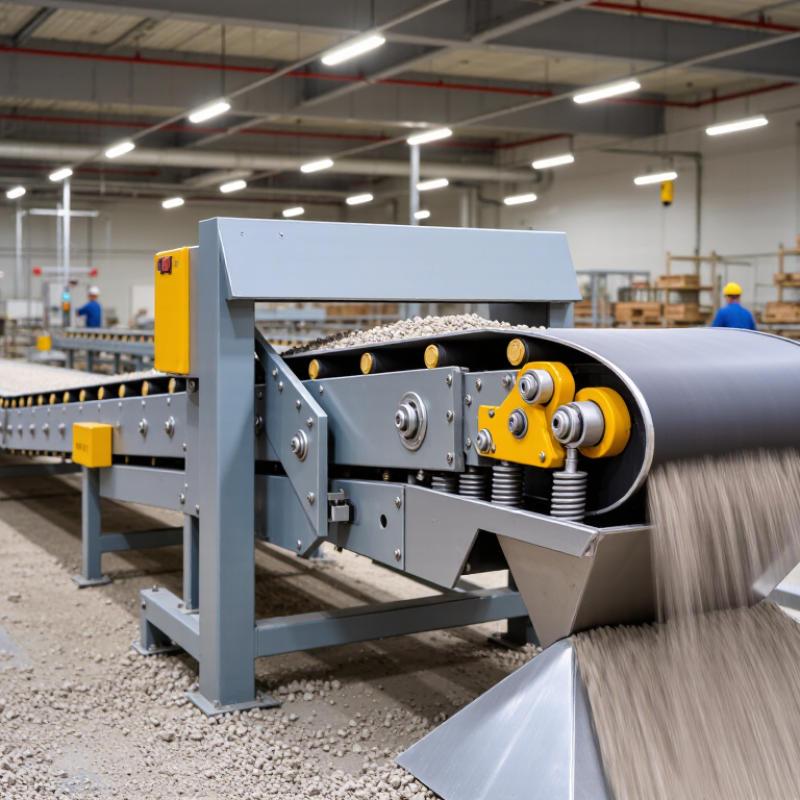
What Conveyor Belt Cleaners Remove: CEMA Definitions of Carryback and Spillage
Why Choose a Belt Cleaner for Conveyor Systems?
In CEMA terminology, carryback is material that remains on the belt after the intended discharge point. It travels along the return side and may fall onto floors, idlers, or structures. Fine coal, damp aggregate, and sticky mineral residue commonly create this problem. A properly selected belt cleaner removes much of this material near the head pulley, before it becomes a housekeeping burden.
Spillage is different. It refers to material that falls from the conveyor system during loading, transfer, or transport. Misaligned belts, overloaded chutes, poor sealing, and damaged components can cause it. A belt cleaner cannot correct every source of spillage. That distinction matters. Installing a cleaner may reduce carryback while leaving transfer-point leakage untouched.
Good selection depends on belt speed, material moisture, temperature, belt condition, and available space. In field inspections, I look for residue patterns beneath the return run and around pulley zones. Those marks often reveal whether carryback or spillage is the real issue. A primary cleaner removes the heavier layer, while a secondary cleaner can improve final removal. It is not magic. Blades can wear, belts can be damaged, and excessive pressure can create new problems. Regular inspection, correct tension, and measured performance checks remain essential. No design should be accepted without reviewing actual operating conditions.
How Primary and Secondary Cleaners Achieve 60–90% Carryback Reduction
Why Choose a Belt Cleaner for Conveyor Systems?
How Primary and Secondary Cleaners Achieve 60–90% Carryback Reduction
Belt carryback leaves a trail beneath the conveyor. It can build around return idlers, walkways, and transfer points. A primary cleaner removes the thick layer immediately after discharge. A secondary cleaner follows behind and removes the remaining film. Used together, they can reduce carryback by 60–90% when belt speed, material moisture, and cleaner pressure are properly matched.
The figure is not a promise. Material changes can alter results quickly. Wet fines may smear across the belt, while dry, coarse material can cause uneven contact. In practical inspections, small gaps often explain poor cleaning. Correct blade alignment, stable tension, and regular wear checks matter as much as cleaner design. A cleaner that works well today may need adjustment after belt splices, seasonal moisture changes, or blade wear.
Tips: Check the belt surface after each cleaner. Look for clean rubber, not polished strips. Measure carryback before and after installation. Record material conditions, belt speed, and cleaner settings. Replace worn blades before they lose contact. Do not overtighten them; excessive pressure can increase wear and energy use. Ask operators for observations, too. Their feedback may reveal problems missed during a short inspection.
Selecting Cleaner Materials for Belt Speeds Above 3.5 m/s (CEMA Guidance)
Why Choose a Belt Cleaner for Conveyor Systems?
At belt speeds above 3.5 m/s, cleaner material becomes a control decision, not a minor accessory. CEMA’s Belt Conveyors for Bulk Materials, 7th Edition, places high-speed cleaning near 700 ft/min, approximately 3.56 m/s. At this speed, impact energy increases, and poor blade contact can create carryback, dust, and rapid wear. Polyurethane blades usually suit moderate abrasion and flexible belt surfaces. Carbide-tipped blades can perform better with sharp, abrasive material, but they demand accurate alignment and splice clearance.
A common field mistake is treating 3.5 m/s as a magic boundary. It is only a screening point. Material moisture, particle size, belt cover, temperature, and cleaner pressure still control performance. ISO 14890 guidance on conveyor belt construction also reinforces the need to protect belt covers and splice areas during operation. In practical inspections, a small buildup near the head pulley often reveals a larger problem: the cleaner is too aggressive, too soft, or poorly positioned. The first specification is rarely perfect.
Tips: Confirm speed in both m/s and ft/min. Check the belt splice before selecting a carbide edge. Use abrasion testing where possible. Record blade wear weekly during commissioning. A cleaner that lasts longer is not automatically safer; excessive pressure can shorten belt life.
How Belt Cleaners Reduce Maintenance, Dust, and Material Loss in Practice
Why Choose a Belt Cleaner for Conveyor Systems?
In conveyor inspections, belt cleaners often reveal their value through ordinary details. A correctly positioned primary cleaner removes carryback before it reaches return rollers, walkways, and loading areas. Less carryback means fewer shoveling tasks and fewer unplanned stops. It also limits dust created when dried material falls from the return strand. The improvement is practical, not dramatic. That matters.
A cleaner also protects material yield. When sticky ore, aggregate, grain, or recycled material stays on the belt, it becomes waste or returns to the wrong location. Scrapers with resilient blades maintain contact while allowing belt splices to pass safely. Tension must be checked during commissioning and routine inspections. Too little pressure leaves residue. Too much can accelerate belt wear. Small adjustments matter. Operators should examine blade wear, pulley alignment, and buildup patterns, rather than treating the cleaner as a fit-and-forget device.
Maintenance teams can record cleanup time, dust observations, and recovered material before and after installation. These simple records support reliable decisions and expose weak assumptions. A cleaner may not solve dust caused by transfer points, poor sealing, or excessive belt speed. It can even create problems when installed without considering belt condition. Experienced technicians inspect the entire conveyor, verify guarding, and follow equipment instructions. Real results require steady inspection and realistic expectations.
Why Choose a Belt Cleaner for Conveyor Systems?
Belt cleaners help reduce carryback, unscheduled maintenance, airborne dust, and material loss at the discharge point.
The chart uses a normalized operating index, where 100 represents a conveyor operating without a belt cleaner. Lower values indicate reduced maintenance demand, dust exposure, and material loss. Actual results vary with belt speed, material type, moisture, loading rate, and cleaner condition.





