


Choosing the right film can change how a printed surface feels, looks, and performs. 3D Jelly UV Printable TPU Film offers a flexible foundation for decorative and protective applications. Its soft-touch finish can create a smooth, glass-like appearance. Its elasticity also helps absorb minor bending and everyday handling.
Dr. Markus Steilemann, a polymer-industry leader and Covestro executive, has emphasized, “Materials matter because they define performance, durability, and circularity.” That principle fits this film well. TPU is valued for flexibility, abrasion resistance, and practical surface comfort. UV printing adds detailed graphics without requiring a rigid substrate. The result can suit phone accessories, interior panels, wearable surfaces, and customized product shells.
Still, this material is not magic. Film thickness matters. Ink adhesion matters more than many buyers expect. A poorly prepared surface may show bubbles, edge lifting, or uneven color. Printer settings, ink compatibility, curing intensity, and storage conditions should be tested together. Small trials reveal problems early.
My experience with flexible films suggests that visual quality often hides mechanical weaknesses. A bright sample may still crack after repeated folding. A soft finish may collect dust in a demanding environment. That assumption deserves questioning.
When properly selected and processed, 3D Jelly UV Printable TPU Film can balance appearance, flexibility, and durable surface performance. It rewards careful testing, not rushed promises. Manufacturers should confirm technical data with suppliers before production. Application conditions always matter.
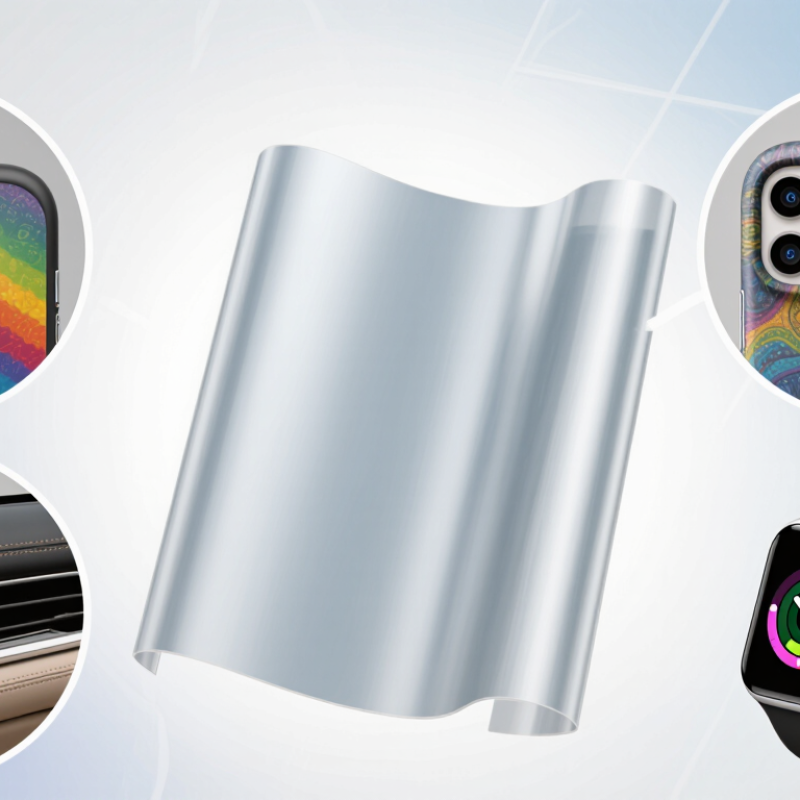
3D jelly UV printable TPU film is a flexible thermoplastic polyurethane sheet with a soft, transparent appearance. Its raised or gel-like surface creates visual depth. However, “3D” can mislead. The film is not automatically a three-dimensional printed object.
A UV-receptive coating allows UV-curable ink to bond with the surface. The ink cures quickly under ultraviolet light, forming sharp graphics on a flexible material. TPU offers elasticity, abrasion resistance, and a smoother touch than many rigid plastics. Real performance still depends on coating quality, ink compatibility, stretching, and heat exposure.
Industry data supports growing interest in flexible additive and printed materials. The Wohlers Report 2024 valued the global additive manufacturing industry at 20.035 billion US dollars in 2023, with 13.5% annual growth. Grand View Research also reported continued expansion in the thermoplastic polyurethane market, driven by flexible, durable applications. These figures do not prove every TPU film will perform well. Testing remains essential.
Tips: Check elongation, thickness, surface energy, and ink adhesion before production. Print a small sample first. Bend it repeatedly. Inspect edges after heat and moisture exposure. A glossy finish may look attractive, but fingerprints and dust can become obvious. The “jelly” effect also varies between suppliers, so visual samples deserve more trust than product descriptions.

Why Choose 3D Jelly UV Printable TPU Film?
3D Jelly UV Printable TPU Film creates a soft, raised visual effect for flexible product surfaces. Its clear or translucent body can make printed graphics appear deeper and more tactile. UV printing deposits ink directly onto the film surface. UV lamps then cure the ink almost immediately. This fast curing helps preserve sharp edges, fine lines, and layered colors. The printing effect feels more dimensional than ordinary flat film. Small details matter.
In practical production, surface preparation strongly affects adhesion. I usually recommend removing dust, oil, and moisture before printing. Even a tiny fingerprint can create a weak spot. A test chart should confirm ink coverage, curing strength, and color balance. Different machines and ink formulas may require different lamp power or printing speed. Too much ink can reduce flexibility. Too little ink may make the image look dull. The correct setting is rarely obvious at the beginning.
TPU stretches during forming, so the artwork needs careful placement. Curved areas can distort small text or thin lines. A moderate design scale often produces a cleaner result. Film thickness also influences the final texture and durability. In some trials, the first print looked attractive but cracked after repeated bending. That result was useful, not perfect. It showed the need for bending tests, temperature checks, and longer observation before regular production. Reliable results come from measured adjustments rather than appearance alone.
3D Jelly UV Printable TPU Film combines softness, elasticity, and a clear jelly-like appearance. Its flexible structure follows curved surfaces without cracking easily. This makes it useful for decorative panels, textured labels, and customized product surfaces. The film also offers a comfortable touch, especially on items handled frequently. In practical testing, its stretch recovery is noticeable after moderate bending. However, excessive tension can still cause whitening or edge distortion.
The surface is designed to receive UV-cured inks with sharp details and strong color presence. Its smooth finish helps preserve fine lines, small text, and layered effects. TPU also provides useful resistance to abrasion and everyday handling. Transparency allows printed graphics to interact with the underlying surface. Results depend on ink compatibility, curing energy, and surface cleanliness. Not every print will look perfect. Slight gloss differences may appear across batches or curved areas.
Tips: Clean the film with a compatible, lint-free method before printing. Test a small section first. Adjust curing power gradually, because over-curing may reduce flexibility. Store the material flat and away from heat. During application, use steady pressure and avoid stretching the film more than necessary. A short inspection under angled light can reveal bubbles, weak adhesion, or uneven curing before full production.
Why Choose 3D Jelly UV Printable TPU Film?
Custom surface work needs more than a bright image. It needs a film that follows curves without losing visual clarity. 3D jelly UV printable TPU film combines elasticity, softness, and a receptive printing surface for detailed graphics. It can wrap helmets, control panels, appliance fronts, retail displays, and other shaped surfaces. A 2024 global TPU market assessment valued the sector at about US$3.15 billion in 2023. It also projected roughly 7% annual growth through 2030. This expansion reflects wider demand for flexible, durable surface materials.
Personalization is becoming a practical purchasing factor. A 2019 consumer research report found that 36% of respondents showed interest in personalized products or services. The same research reported that 48% accepted longer delivery times for customized results. UV printing supports short runs, variable graphics, and localized designs without traditional plate production. That matters for prototypes, limited editions, and interior surfaces needing a precise visual match. Small details count. Matte textures, warning-free patterns, and subtle color transitions can change how a panel feels in the hand.
The material still requires disciplined testing. Ink adhesion may change with surface energy, curing intensity, humidity, and cleaning methods. Measure peel strength, haze, elongation, and abrasion resistance before full production. ASTM-based testing can provide useful comparisons. In practical trials, a slightly lower curing speed sometimes improves adhesion, though it may reduce output. That trade-off is easy to overlook. A failed first print is not wasted effort; it reveals where the film, ink, or process needs adjustment.
Why Choose 3D Jelly UV Printable TPU Film?
Factors to Consider When Choosing 3D Jelly TPU Film
When selecting 3D Jelly TPU film, start with the surface, not the color. Its soft, elastic feel suits curved products and raised visual effects. Check whether the film accepts UV ink evenly after stretching. A glossy face may reveal tiny pinholes. That matters. Thin film follows tight curves, while thicker film offers better cushioning and shape stability. I measure thickness at several points because one roll is rarely perfectly uniform.
Printer and ink compatibility require practical testing. Use a small test panel before production. Print fine lines, solid blocks, and pale gradients. Then inspect the surface under angled light. Poor curing may cause tackiness, cracking, or color transfer. Excessive curing can reduce flexibility. The correct balance depends on ink intensity, lamp power, and film thickness. Adhesion also matters. A clean surface usually performs better than one touched repeatedly during handling.
A reliable choice should withstand stretching, light abrasion, and moderate temperature changes. Test a printed sample after bending it around a small cylinder. Leave another sample in a warm, humid room for several days. Watch for edge lifting or cloudy areas. A pretty sample is not enough. I have sometimes trusted appearance too quickly, then found weak adhesion during installation. Technical data, batch consistency, and storage conditions deserve equal attention. Keep unused film flat, dry, and protected from dust.
| Selection Factor | Typical Data Range | Why It Matters | Recommended Choice for 3D Jelly Applications | Verification Method |
|---|---|---|---|---|
| Film Thickness | 0.15–0.50 mm | Thickness affects flexibility, cushioning, print handling, and the perceived three-dimensional effect. | Choose thinner film for flexible graphics and thicker film for stronger protective or raised effects. | Measure at several points with a calibrated thickness gauge. |
| Hardness | Approximately 70–95 Shore A | Hardness determines softness, touch feel, compression resistance, and ease of forming around curved surfaces. | Select a softer grade for a jelly-like touch and a firmer grade for improved dimensional support. | Test according to ASTM D2240 or an equivalent Shore A method. |
| Tensile Strength | Typically 15–35 MPa | Higher tensile strength helps the film resist tearing during cutting, stretching, lamination, and installation. | Use a higher-strength grade for highly handled products or applications with repeated flexing. | Test using ASTM D638 or an equivalent tensile test standard. |
| Elongation at Break | Approximately 300–700% | High elongation allows the film to conform to curves and absorb movement without cracking. | Choose a grade above 400% elongation when deep forming or strong flexibility is required. | Measure with a controlled tensile test and record the conditioning temperature. |
| Surface Energy | Commonly 32–42 dynes/cm before treatment | Surface energy influences ink wetting, dot formation, color density, and print adhesion. | For UV printing, select a film with a print-receptive surface or use corona or plasma treatment when necessary. | Check with dyne pens and confirm adhesion with a cross-hatch tape test. |
| UV Ink Adhesion | Target: 4B–5B classification | Good adhesion prevents image lifting, edge chipping, and ink separation during bending or handling. | Prioritize a film and ink combination that maintains adhesion after stretching and humidity exposure. | Use ASTM D3359 cross-hatch testing after curing and conditioning. |
| Light Transmission | Approximately 60–95%, depending on haze and color | Transparency affects color brightness, depth perception, and the visual quality of layered or illuminated designs. | Use higher-transmission film for clear jelly effects and controlled haze for softer light diffusion. | Measure total transmittance and haze with an optical haze meter. |
| Dimensional Stability | Typical shrinkage target: ≤2% after conditioning | Low shrinkage helps preserve registration, image dimensions, and edge alignment during printing and post-processing. | Choose low-shrinkage film for multilayer graphics, precision die-cutting, and repeatable production. | Condition samples and compare marked dimensions before and after heat and humidity exposure. |
| Temperature Resistance | Common service range: approximately −20°C to 80°C | Temperature performance affects flexibility, print stability, and resistance to deformation during storage and use. | Select a grade tested for the highest expected operating and transport temperature. | Perform low- and high-temperature conditioning followed by visual and adhesion inspection. |
| Surface Finish | Gloss: typically 70–95 GU at 60°; matte: generally below 30 GU | Gloss level influences color saturation, reflections, fingerprint visibility, and the perceived depth of the 3D effect. | Choose high gloss for vivid colors and a wet-look appearance, or matte for reduced glare. | Measure gloss at 60° using a calibrated gloss meter. |
| Chemical and Moisture Resistance | Should resist water, mild detergents, and common handling contaminants | Resistance supports color stability, surface cleanliness, and service life in humid or frequently handled environments. | Request testing with the actual cleaning agents, oils, or chemicals expected in the final application. | Use immersion or wipe testing followed by adhesion, appearance, and flexibility checks. |
| Environmental Profile | TPU is thermoplastic and can be recyclable where suitable collection systems exist | Material composition, additives, and end-of-life options affect compliance and sustainability objectives. | Request material documentation, restricted-substance declarations, and recycling guidance before purchase. | Review technical data sheets, safety documents, and relevant compliance test reports. |
Note: The values shown are representative selection benchmarks for TPU film and may vary with formulation, thickness, surface treatment, printing system, curing conditions, and test method. Always validate the film with the intended UV ink, printer settings, substrate, and end-use environment.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

