What Is an RFID Wristband and How Does It Work?
An Rfid Wristband is a wearable identification device that uses radio waves to exchange data with a compatible reader. It usually contains an RFID chip and antenna inside silicone, fabric, or laminated plastic. Passive models draw energy from the reader’s signal. They do not need a battery. Active models include a battery and can support longer communication ranges. The difference matters.
When a guest approaches a reader, the reader sends a radio signal. The wristband responds with its stored identifier. Software then matches that identifier with an approved record, such as an event entry, hotel service, or equipment check-out. The process can take less than a second. However, an RFID wristband is not a GPS tracker, and it cannot identify people without suitable readers and connected systems. Metal surfaces, liquids, crowd density, and poor antenna placement can reduce performance. A band may look simple. The infrastructure is not.
Industry data shows why this technology continues to attract investment. Grand View Research estimated the global RFID market at USD 14.26 billion in 2022, with projected growth through 2030. MarketsandMarkets also forecasts strong expansion, driven by retail, logistics, healthcare, and event operations. These figures describe the wider RFID industry, not wristbands alone. That distinction is important. Reliable deployment requires more than purchasing bands. Organizations should test read distance, privacy controls, durability, and system accuracy in real operating conditions. In practice, a small pilot often reveals problems that a product brochure misses. A successful design balances convenience, data protection, and dependable reader coverage.
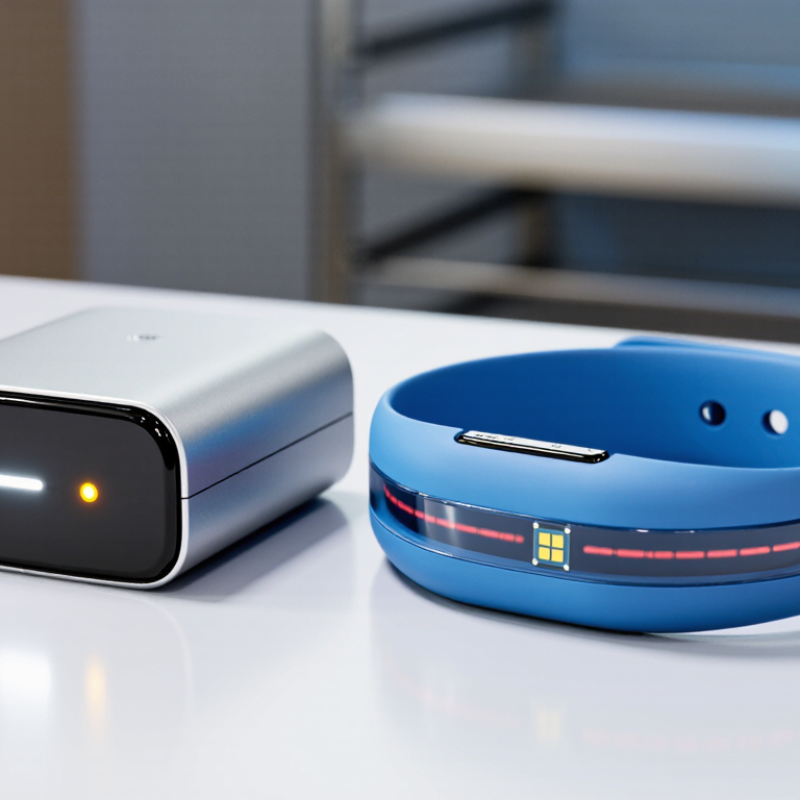
RFID Wristband Anatomy: Chip, Antenna, and Passive Power Design
An RFID wristband contains three essential parts: a small integrated circuit, a conductive antenna, and a protective wristband shell. The chip stores an identification number and manages communication with a nearby reader. It does not normally contain a battery. That detail matters.
The antenna receives radio energy from the reader’s electromagnetic field. The chip converts a small portion of that energy into usable power. It then changes the reflected signal, allowing the reader to interpret stored data. This passive power design keeps the wristband light, thin, and inexpensive to maintain. However, passive tags work only within a suitable reading range. Distance, antenna alignment, and reader strength can affect performance.
The antenna may be a thin metal coil, etched pattern, or flexible conductive layer. Its shape must match the operating frequency and the wristband’s available space. Materials near the antenna can reduce signal quality. Water, metal objects, and tightly wrapped surfaces may create practical problems. A poorly tuned antenna can make a working chip appear defective. The chip also needs protection from sweat, bending, and repeated impacts. Sealing helps, but it can increase thickness and stiffness.
In real deployment, testing the complete wristband is more reliable than testing the chip alone. Small changes matter. A comfortable strap may position the antenna poorly. A stronger reader may improve range but increase unwanted reads. Designers must balance comfort, durability, privacy, and consistent identification. The design is not perfect. That trade-off deserves review before production.
How 13.56 MHz RFID Wristbands Exchange Data Through Magnetic Coupling
An RFID wristband uses a small antenna and integrated chip to exchange data at 13.56 MHz. This frequency supports short-range, high-frequency identification through near-field magnetic coupling. The reader creates an alternating magnetic field through its coil. When the wristband enters that field, its antenna coil captures energy and produces a small electrical current.
No battery is required. The chip briefly changes the antenna’s electrical load, creating tiny variations in the magnetic field. The reader detects these variations as binary data, then validates the wristband’s identifier. This process happens within a short distance, often a few centimeters, although antenna size, reader power, and wristband position affect performance. Orientation matters. A sideways wristband may respond less reliably than a flat one.
ISO/IEC 14443 defines widely used communication principles for 13.56 MHz contactless devices. A 2024 RFID market report by Fortune Business Insights estimates the global RFID market could grow from about 16.23 billion dollars in 2023 to 40.50 billion dollars by 2032. That growth reflects broader adoption, not a guarantee of perfect wristband performance. Metal fixtures, dense water-based materials, and crowded reader environments can weaken coupling. The neat textbook model is incomplete. Real testing should measure read distance, response time, and failed reads on the actual wearer’s wrist.
From Reader Field to Identification: The Step-by-Step RFID Transaction
What Is an RFID Wristband and How Does It Work?
From Reader Field to Identification: The Step-by-Step RFID Transaction
An RFID wristband contains a small chip and antenna sealed inside flexible material. The chip stores an identifier, not a complete personal profile. In many systems, it operates without a battery. That detail matters.
When the wristband enters a reader’s radio field, the antenna receives energy from the signal. The chip briefly powers up. It then prepares its stored identification number for transmission. The reader does not “see” the wristband visually. It detects a controlled radio response.
The transaction continues through several checks. The reader captures the wristband’s response and sends it to a connected control system. That system compares the identifier with approved access rules. If the record matches, the system may unlock a gate, register attendance, or update a service account. The event usually includes a time stamp and reader location. Staff can review these records when investigating errors.
The process sounds cleaner than reality. Metal surfaces, crowded spaces, and poor wristband positioning can weaken communication. A reader may also detect more than one tag. Professional installations therefore require field testing, documented settings, and clear fallback procedures. I have found that a simple visual check still helps during busy operations. RFID improves speed, but it does not remove the need for careful system design, data protection, and human judgment.
HF Versus UHF Wristbands: 13.56 MHz, 860–960 MHz, and Read Range
What Is an RFID Wristband and How Does It Work?
An RFID wristband stores an electronic identifier in a small chip. A reader sends radio energy to the chip, which returns its stored data. Most wristbands are passive, so they need no battery. The process feels instant at a venue entrance, although the reader may check several tags within one second.
HF wristbands operate at 13.56 MHz. They usually provide a short read range, often a few centimeters to about one meter. This controlled range suits tap-based access, cashless points, and close-range identification. HF also performs consistently around people, but nearby metal can still affect results. The simple split is useful, but imperfect.
UHF wristbands generally use 860–960 MHz, depending on regional radio rules. Their read range can reach several meters, especially with suitable antennas and tag placement. This supports hands-free detection at wider entrances or checkpoints. However, the human body contains water and can weaken UHF signals. Wrist angle, crowd density, clothing, and antenna position matter. Longer range is not automatically better. It can create unwanted reads near adjacent lanes.
In real installations, testing the complete setup is essential. A wristband that works on a dry test table may behave differently on an active gate. Measure missed reads, accidental reads, and performance during movement. Read-range figures are estimates, not promises. Some designs also need stronger data protection, because a readable identifier should not expose unnecessary personal information.
HF Versus UHF RFID Wristbands
Typical passive RFID read ranges by wristband type. HF operates at 13.56 MHz, while UHF generally operates across the 860–960 MHz band.
HF wristbands typically work within about 0.1–1 metre and are less affected by nearby items such as people or liquids. UHF wristbands can commonly reach about 1–10 metres with suitable reader antennas, but performance depends on reader power, antenna design, tag orientation, surrounding materials, and regional radio regulations.
Industry Standards: ISO/IEC 14443, ISO/IEC 15693, and EPC Gen2 RFID
What Is an RFID Wristband and How Does It Work?
An RFID wristband combines an antenna, microchip, and flexible substrate. A reader sends radio energy, and the chip returns stored data. Passive wristbands usually need no battery. Their performance changes near metal, water, and tightly packed people.
ISO/IEC 14443 supports high-frequency communication at 13.56 MHz. It is common for close-range identification, often within a few centimeters.
ISO/IEC 15693 also operates at 13.56 MHz, but supports vicinity communication and may provide longer reading distances.
EPC Gen2 RFID targets UHF systems across roughly 860–960 MHz. It supports anti-collision features, allowing readers to identify many tags quickly. The standard is also referenced through ISO/IEC 18000-63.
These standards describe communication rules, not complete wristband security. A practical design should control reader power, data permissions, and backend access. A 2024 RAIN Alliance market report estimated 44.8 billion RAIN RFID ICs were sold in 2023. That figure shows strong industrial adoption, but it does not guarantee reliable wristband performance.
Real testing remains essential. Sweat, folding, and body absorption can reduce read consistency. I have seen designs fail because engineers tested empty wristbands only. That shortcut deserves reconsideration.
GS1 guidance also emphasizes consistent identifier management, especially when EPC data connects physical items with digital records.





