


Choosing the best Industrial Water Meters requires more than comparing catalog prices. Industrial facilities measure cooling water, process water, wastewater, and reclaimed supplies under very different conditions. A meter that performs accurately in clean water may struggle with suspended solids, bubbles, or chemical residue. The right choice depends on flow range, pipe diameter, pressure, temperature, conductivity, and installation space.
No meter wins every site. Electromagnetic meters suit conductive liquids and have no moving parts, which can reduce mechanical wear. Ultrasonic meters support non-invasive installation and can work well where shutdowns are difficult. Turbine meters often provide dependable readings in clean, stable flows, while positive displacement meters can perform effectively at lower flow rates. Each design has limits. That detail is easy to overlook.
This guide compares leading meter types through practical engineering criteria, including measurement accuracy, calibration needs, signal stability, maintenance access, and lifecycle cost. It also considers field realities, such as a narrow pipe gallery, a vibrating pump line, or water containing fine sediment. Manufacturer specifications matter, but verified testing matters more. Look for recognized performance standards, documented calibration procedures, traceable data, and responsive technical support. These factors help operators make defensible decisions rather than selecting equipment from a short marketing list. Even experienced teams can misjudge conditions when sampling is limited. Careful site assessment remains essential.
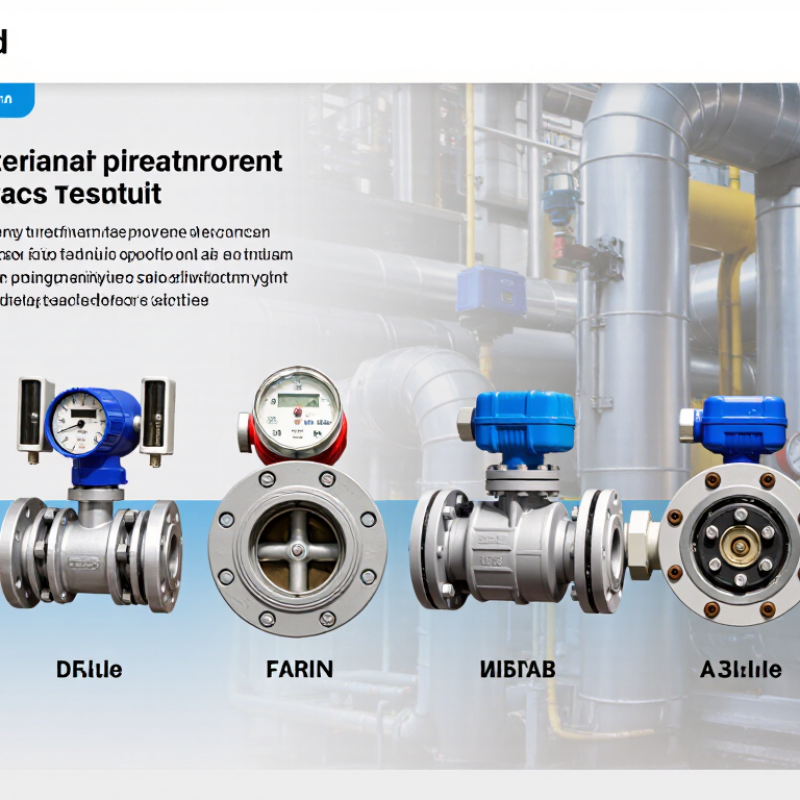
Industrial water meters are instruments that measure water moving through pipes, treatment systems, and production lines. They convert flow into readable data, usually in liters, cubic meters, or gallons. In industrial settings, measurement must remain stable under pressure, vibration, temperature changes, and suspended particles.
Their main purpose is control. Operators use flow data to track consumption, detect leaks, balance process water, and verify treatment performance. A sudden reading at 3:00 a.m. may reveal a valve problem or a hidden pipe break. Accurate metering also supports maintenance planning and more defensible operating records. The meter does not reduce waste by itself. People must act on its readings.
Core functions include measuring flow rate, recording total volume, and sending data to monitoring systems. Some meters provide alarms for reverse flow, empty pipes, or unusual consumption. Electromagnetic meters suit conductive liquids and have no internal moving parts. Ultrasonic meters can measure flow without cutting into the pipe. Turbine meters often perform well with cleaner water, but debris can affect their moving components. Selection depends on pipe size, water quality, pressure, temperature, and required accuracy.
Calibration matters. Even a well-installed meter can drift over time. In field work, installation errors are often underestimated, especially poor grounding, air pockets, and incorrect straight-pipe distances. No meter is perfect. A reliable system combines suitable equipment, regular verification, clear records, and trained operators who question readings that look unusually convenient.

Industrial water meters do more than display a number. They convert moving water into measurable flow and support better process control. Electromagnetic meters measure velocity through an induced electrical signal. Ultrasonic meters use sound waves to compare travel times. Mechanical turbine meters rely on rotating parts inside the pipeline.
Each method suits different conditions. No meter is perfect. Water quality, pipe size, pressure, and temperature can affect accuracy. Clean water may work well with mechanical or ultrasonic measurement. Conductive water, including treated wastewater, often suits electromagnetic measurement. The correct choice depends on the application, not popularity.
During operation, a meter calculates instantaneous flow and total water volume. Operators can compare these readings with production schedules, tank levels, or discharge limits. Many industrial systems send pulse, analogue, or digital signals to a monitoring platform. This helps identify leaks, blocked lines, and unusual consumption.
Small errors matter.
Installation quality remains critical. Poor grounding, air pockets, vibration, or insufficient straight pipe can distort readings. Regular verification and calibration provide stronger evidence than a screen value alone. Field inspections should check wiring, valve positions, sensor condition, and the displayed units. A meter may appear reliable while reporting the wrong scale. That possibility deserves attention. Reliable monitoring combines suitable equipment, careful installation, documented testing, and practical human review.
Choosing a top industrial water meter depends on the water, pipe, and operating conditions. Magnetic flow meters work well for conductive water, including treated water and wastewater. They have no moving parts, which reduces mechanical wear. Ultrasonic meters measure flow through sound waves and suit large pipes or temporary monitoring. However, air bubbles and poor installation can reduce their accuracy. Conductivity matters.
Turbine meters perform well with clean water and steady flow. Their rotating parts can provide reliable readings, but suspended solids may increase maintenance. Positive displacement meters handle lower flow rates and support accurate batch measurement. They are useful in chemical dosing and process control systems. Vortex meters fit some industrial applications, although pressure loss requires careful review. Small details matter.
Installation conditions often decide the final result. Operators should verify straight pipe length, pressure, temperature, and expected flow range. A common error is selecting a meter by pipe diameter alone. That assumption can create unstable readings. Regular calibration also matters, especially where water quality changes throughout the year. Reviewing logged data against tank levels or pump output can reveal hidden errors. In practice, even a well-selected meter may need adjustment after installation.
| Meter Type | Operating Principle | Best-Suited Water Conditions | Typical Industrial Applications | Main Advantages | Key Limitations | Common Installation Requirements |
|---|---|---|---|---|---|---|
| Electromagnetic Flow Meter | Measures the voltage generated when conductive water moves through a magnetic field. | Conductive liquids, including process water, wastewater, sludge, and chemically treated water. | Wastewater treatment, water distribution, chemical processing, mining, pulp and paper, and cooling-water systems. | No moving parts, low pressure loss, good accuracy, and suitable for dirty or abrasive liquids. | Cannot measure non-conductive liquids; electrodes may require material compatibility checks. | Full pipe, proper grounding, and sufficient upstream and downstream straight pipe according to the manufacturer’s instructions. |
| Ultrasonic Flow Meter | Uses the difference in ultrasonic transit time, or Doppler frequency shift, to determine flow velocity. | Clean water for transit-time meters; liquids containing suspended particles or bubbles may suit Doppler meters. | Large pipelines, raw-water intake, cooling-water monitoring, temporary surveys, and energy-management systems. | Clamp-on models can be installed without pipe cutting; low maintenance and very low pressure loss. | Performance depends on pipe condition, sensor alignment, flow profile, and liquid characteristics. | Good acoustic coupling, accurate pipe dimensions, and suitable straight-run conditions are normally required. |
| Vortex Flow Meter | Detects vortices formed downstream of a bluff body; vortex frequency is proportional to flow velocity. | Clean water and process fluids with stable flow conditions and limited solids. | Utility-water monitoring, boiler-feed systems, cooling-water circuits, and general process measurement. | No moving parts, broad measurement capability, and possible measurement of liquids, gases, and steam. | Requires adequate flow velocity; sensitive to vibration, pulsation, and flow disturbances. | Correct pipe sizing, strong mechanical support, and appropriate straight pipe are important. |
| Turbine Flow Meter | An internal rotor turns as water passes through it; rotor speed is converted into flow rate. | Clean, filtered water with relatively low concentrations of suspended solids. | High-purity water, water-treatment skids, batching, irrigation process lines, and utility monitoring. | Good repeatability, compact design, and useful performance over a defined flow range. | Moving parts can wear; debris may damage or obstruct the rotor and create pressure loss. | Filtration, correct flow direction, and straight-pipe requirements are commonly needed. |
| Positive Displacement Meter | Captures and counts fixed volumes of liquid using chambers, pistons, discs, or oval gears. | Clean water and other relatively clean, low-viscosity liquids. | Precise batch dosing, small industrial lines, chemical dilution, and point-of-use consumption monitoring. | Strong low-flow performance and direct volumetric measurement. | Moving components are subject to wear; solids can cause blockage and increased pressure loss. | A strainer is often recommended, along with proper orientation and protection from excessive flow. |
| Mechanical Multi-Jet Meter | Multiple water jets rotate an impeller, and the rotational speed represents the volume passing through the meter. | Clean or moderately clean water in small and medium-sized pipelines. | Facility water submetering, utility areas, process departments, and internal water-allocation systems. | Cost-effective, relatively simple, and commonly available in compact sizes. | Mechanical wear, sensitivity to debris, and reduced suitability for high-solid or highly pulsating flows. | Upstream filtration and installation away from severe turbulence help maintain measurement performance. |
| Open-Channel Flow Meter | Calculates flow from measured liquid depth, channel geometry, and an established hydraulic relationship. | Partially filled channels, flumes, weirs, and gravity-flow systems. | Wastewater discharge, drainage channels, irrigation canals, stormwater monitoring, and effluent compliance. | Works without a full pipe and can monitor flows containing suspended solids. | Accuracy depends on channel geometry, level measurement, installation conditions, and hydraulic stability. | A stable channel or calibrated primary device, unobstructed flow, and reliable level sensing are required. |
| Coriolis Mass Flow Meter | Measures the deformation and phase shift of vibrating flow tubes to determine mass flow. | Clean water and process liquids where high-value mass-flow, density, or concentration data is needed. | Specialty chemical processing, accurate blending, laboratory-scale production, and critical process control. | Direct mass-flow measurement with the ability to provide density information in many configurations. | Higher purchase cost, greater weight, and potential sensitivity to installation-induced vibration. | Rigid support, suitable process connections, and careful consideration of pressure drop and vibration are necessary. |
Selection should consider water conductivity, suspended solids, required accuracy, pipe size, flow range, pressure loss, installation conditions, maintenance requirements, and communication needs.
Comparing industrial water meters requires more than checking flow-range labels. A reliable meter should match the pipe size, fluid quality, pressure, temperature, and expected flow pattern. The United Nations World Water Development Report 2024 estimates that industry accounts for about 20% of global freshwater withdrawals. Small measurement errors can therefore become expensive across continuous operations.
Accuracy matters most at low flow. Many facilities measure correctly during production but miss leaks during night shifts. ISO 4064 provides metrological requirements for water meters, including accuracy testing and operating conditions. Buyers should review accuracy across the complete working range, not only the headline maximum flow. Repeatability, pressure loss, response time, and bidirectional measurement also deserve attention. Field testing is essential.
Installation can decide real performance.
Straight-pipe requirements, air bubbles, vibration, and sediment may distort readings. Ultrasonic meters usually avoid moving parts, while mechanical designs can be easier to verify and maintain. Neither option is automatically better. AWWA Manual M6 emphasizes proper selection, installation, testing, and maintenance as connected tasks. That point is easy to underestimate. The U.S. Geological Survey’s 2015 water-use report also shows how large industrial withdrawals can be, making weak data quality a management problem rather than a minor technical flaw. I would compare five-year maintenance records, calibration procedures, communication compatibility, and actual site trials before choosing a meter. A spreadsheet alone cannot reveal every failure.
Industrial water meters deliver value only when installation, calibration, maintenance, and data management work together. The UN World Water Development Report 2024 estimates that industry uses about 20% of global freshwater withdrawals. Small measurement errors can therefore become expensive operational blind spots.
Install meters on clearly defined process lines, not only at the facility entrance. Check pipe diameter, flow direction, straight-run requirements, vibration, and air pockets before commissioning. Ultrasonic meters need clean signal paths. Mechanical meters need protection from debris. Record the serial number, location, range, and initial reading. Calibration should follow the manufacturer’s procedure and a risk-based schedule. ISO 4064 provides useful principles for flow measurement accuracy, but site conditions still matter.
Maintenance should include leak checks, sensor cleaning, wiring inspections, and comparison with a trusted reference meter. Data management needs hourly or daily readings, automatic alerts, and secure backups. The World Bank’s High and Dry report warns that global water demand could exceed available supply by 40% by 2030. Reliable data supports earlier action, although dashboards cannot repair a poorly installed meter.
Tips: Create a simple meter map. Photograph each installation. Compare night flow with production schedules. Investigate sudden zero readings quickly. Do not trust perfect data blindly; a stable number may indicate a blocked sensor. Review calibration results with operators, because field experience often exposes errors that software misses.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

