


A Valve Actuator converts control signals into mechanical movement, allowing a valve to open, close, or regulate flow. It may use electric power, compressed air, or hydraulic pressure. In a plant, that movement can control water, steam, oil, gas, or corrosive chemicals. The mechanism sounds simple. The responsibility is not. A few degrees of incorrect travel can affect pressure, temperature, safety, and production quality.
Industry data shows why this technology remains important. MarketsandMarkets’ Industrial Valves Market report identifies automation, energy infrastructure, and process industries as major growth drivers. Grand View Research also reports continued expansion in industrial automation and control equipment, supported by smarter manufacturing systems. However, market estimates differ because companies classify actuators, control valves, and accessories differently. That inconsistency deserves attention.
This guide explains how a Valve Actuator works, from the command signal to the final stem or shaft movement. It examines electric motors, pneumatic cylinders, hydraulic systems, torque, fail-safe operation, and position feedback. Standards such as ISO 5211 and IEC 60534 help engineers match actuators with valve interfaces and control requirements. A practical example is a pneumatic actuator mounted above a butterfly valve. Air enters the cylinder, the piston moves, and the valve disc rotates inside the pipeline. Sensors then confirm its position. Small movement. Large consequence. No actuator is perfect, especially when sizing ignores temperature, friction, cycling frequency, or emergency requirements. Reliable selection depends on verified data, field experience, and careful maintenance records.
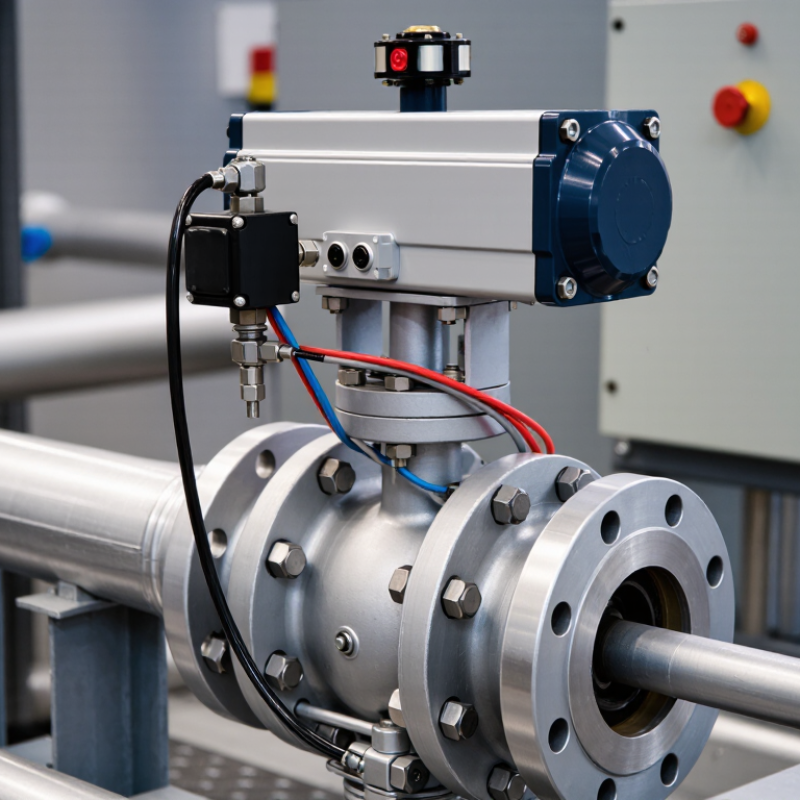
A valve actuator is the mechanism that opens, closes, or positions a valve. Its main purpose is to control fluid or gas flow without constant manual effort. In a processing line, it can respond to a control signal within seconds. The actuator may use electric power, compressed air, or hydraulic pressure. Each option suits different operating conditions. Electric models support precise positioning and easy system integration. Pneumatic models often provide fast movement in demanding industrial areas. Hydraulic units deliver high force for large, tightly sealed valves. The choice depends on valve size, torque, speed, and available energy.
Inside the actuator, a motor, piston, or drive mechanism produces movement. A gearbox may increase torque and reduce operating speed. The actuator then transfers this force to the valve stem or shaft. Sensors can confirm whether the valve is open, closed, or partly positioned. This feedback helps prevent unsafe flow changes and reduces manual inspection. However, an actuator is not automatically reliable after installation. Incorrect sizing can cause weak movement, overheating, or premature wear. Moisture, dirt, and unstable pressure can also affect performance. I have found that simple commissioning checks often reveal overlooked alignment problems. Maintenance teams should inspect connections, travel limits, seals, and response time regularly. A small adjustment can prevent a costly process interruption.
| Actuator Type | Energy Source | Output Motion | Commonly Used With | How It Works | Main Advantages | Typical Limitations | Common Fail-Safe Arrangement |
|---|---|---|---|---|---|---|---|
| Manual Actuator | Human effort | Rotary or linear |
| A handwheel, lever, or gearbox transfers operator input to the valve stem or shaft. |
|
| Normally remains in its last manually selected position. |
| Pneumatic Actuator | Compressed air or gas | Rotary or linear |
| Air pressure acts on a piston or diaphragm to produce force and move the valve. Springs may return the valve when air pressure is removed. |
|
| Spring-return designs can be configured to fail open or fail closed when air pressure is lost. |
| Electric Actuator | Electrical power | Rotary or linear |
| An electric motor drives a gearbox, screw, or stem mechanism. Limit switches, torque protection, and position sensors control movement. |
|
| May remain in position, move to a defined position, or use a backup spring or battery system, depending on the design. |
| Hydraulic Actuator | Pressurized hydraulic fluid | Rotary or linear |
| Hydraulic pressure acts on a piston or vane to create high force or torque for moving the valve. |
|
| Spring-return or stored-energy systems can provide fail-open or fail-closed action when hydraulic pressure is lost. |
| Quarter-Turn Actuator | Manual, pneumatic, electric, or hydraulic power | Approximately 90-degree rotation |
| The actuator rotates the valve shaft through a limited angle to move the closure element between open and closed positions. |
| Not suitable for valves that require multiple turns or long linear stem travel. | Can use a spring-return mechanism or other stored energy to reach a safe position. |
| Multi-Turn Actuator | Manual, electric, or hydraulic power | Multiple rotations |
| The actuator rotates the stem or stem nut through several turns, producing linear movement and seating force. |
| Usually requires more space and takes longer to operate than quarter-turn equipment. | Fail position depends on the actuator design, valve load, and any installed backup or spring mechanism. |
| Modulating Actuator | Electrical, pneumatic, or hydraulic power with a control signal | Continuous rotary or linear adjustment |
| A controller compares the desired process value with feedback and adjusts the valve position to regulate flow, pressure, temperature, or level. |
|
| Often configured to fail open, fail closed, or fail in place according to process safety requirements. |
| On/Off Actuator | Manual, pneumatic, electric, or hydraulic power | Movement between defined end positions |
| The actuator drives the valve fully open or fully closed in response to a local or remote command. |
| Does not normally provide precise flow regulation and may cause process shock if operated too quickly. | The selected safe position depends on whether continued flow or stopped flow is safer for the process. |
| Key Selection Factors | Process requirements and available utilities | Quarter-turn or multi-turn; rotary or linear | Valve type, size, pressure rating, and service conditions | Selection involves matching required torque or thrust, operating speed, control method, duty cycle, environmental conditions, and valve travel. |
| Incorrect sizing or unsuitable materials can cause slow operation, incomplete travel, leakage, or premature failure. | Choose the fail position based on the hazards and consequences of loss of power, air, hydraulic pressure, or control signal. |

A valve actuator converts external energy into controlled mechanical movement. It may use compressed air, electricity, or hydraulic pressure. The actuator transfers this force through a shaft, gear train, or linkage. That movement turns a rotary valve or pushes a linear valve stem.
With a pneumatic actuator, compressed air enters a chamber and moves a diaphragm or piston. The piston creates torque that rotates the valve disc.
An electric actuator uses a motor, reduction gears, and position sensors. The gears reduce speed but increase turning force.
Hydraulic designs use pressurized fluid when high operating torque is necessary.
The process must match the valve’s size, pressure, and operating conditions. A technician checks required torque, stroke length, cycle speed, and temperature range. A small mismatch can leave the valve partly open. That can cause leakage, unstable flow, or unnecessary wear.
Feedback systems improve control. A sensor reports the valve position to the controller, which adjusts the actuator’s movement. Many systems also include a spring-return function. If power or air pressure fails, the spring moves the valve toward a safer position.
Field experience shows that alignment matters. Even a strong actuator can perform poorly against a bent stem or excessive packing friction. I have also seen specifications treated as exact answers, although real installations vary. Dirt, cold temperatures, and frequent cycling can change performance over time. Regular inspection remains essential.
What Is a Valve Actuator and How Does It Work?
A valve actuator converts energy into controlled valve movement. It may rotate a ball valve or move a gate valve in a straight line. The actuator receives a signal from a control system, then applies torque or thrust. Limit switches and position sensors help confirm the valve’s actual position. In real installations, correct sizing matters more than appearance. A small error can leave a valve partly closed.
What Are the Main Types of Valve Actuators?
Pneumatic actuators use compressed air to produce quick, reliable movement. They suit process lines where fast cycling and simple maintenance are important. Electric actuators use a motor and gears, offering accurate positioning without an air supply. They work well when electrical control and slower adjustment are acceptable. Hydraulic actuators deliver high force from pressurized fluid. They are useful for large valves, but leaks and fluid cleanliness require attention.
Electro-hydraulic actuators combine electrical signals with hydraulic power. This arrangement can provide strong movement and precise control in demanding systems. Manual actuators, such as handwheels and gear operators, remain practical for infrequent operation. They depend on human access and physical effort.
The best choice is not always obvious. Temperature, valve size, operating speed, available utilities, and required fail-safe action must be checked together. A pneumatic unit may fail safely with a spring return, while an electric unit may need backup power. Field conditions can expose assumptions. Dust, moisture, corrosion, or limited space may change the decision. Verification during commissioning is essential.
A valve actuator converts a control signal into movement, but several supporting components determine whether that movement is accurate and safe. The power source may be compressed air, electricity, or hydraulic pressure. A gearbox adjusts speed and torque, while the stem coupling transfers force to the valve. In pneumatic systems, a solenoid valve directs air into the actuator chamber. In electric systems, a motor controller manages rotation and braking.
Positioners deserve close attention. They compare the commanded position with feedback from a sensor, then correct small errors. Limit switches confirm fully open or closed travel. Torque switches stop movement when resistance becomes excessive. A spring-return mechanism can move the valve toward a safer position after power or air loss. Enclosures also matter, especially where dust, moisture, or temperature changes threaten wiring and sensors.
The 2024 Fortune Business Insights valve actuator analysis valued the global market at approximately USD 8.6 billion in 2023 and projected continued growth through 2032. That expansion reflects rising demand for automated flow control, not merely larger motors. ISO 5211 dimensional guidance also helps match actuators with valve mounting interfaces, reducing alignment problems. Still, a compliant connection does not guarantee reliable operation. Field inspections often reveal loose terminals, poorly adjusted switches, or feedback signals that drift over time. Small faults become expensive quickly. Test the complete control chain, not only the actuator.
Standard linear mapping between a 4–20 mA control signal and valve position. The same signal range is commonly used for position feedback.
A controller or PLC sends the command signal to the actuator’s drive or positioner. The actuator converts electrical, pneumatic, or hydraulic energy into mechanical motion. A position sensor provides feedback, while limit switches, torque protection, the power supply, and the valve mounting hardware support safe and reliable operation.
A valve actuator converts control signals into mechanical movement, opening, closing, or positioning a valve. Selection should begin with the valve’s torque or thrust requirement, not the actuator’s advertised size. Calculate breakaway torque, running torque, shutoff load, cycle frequency, temperature, and corrosion exposure. Add a documented safety margin, but avoid excessive oversizing. A larger actuator can increase cost, energy use, and mechanical stress.
Pneumatic actuators suit fast, repetitive operation when clean instrument air is available. Electric units often simplify installation where air systems are impractical. Hydraulic actuators provide high force, but fluid leakage and temperature control require attention.
The U.S. Department of Energy reports that compressed-air leaks can waste 20–30% of compressor output, making air-quality checks financially important. IEC 60534 and ISO 5211 provide useful guidance for control valves and actuator interfaces. Still, standards do not replace site testing. Real friction may differ from design assumptions.
Tips: Record operating torque during commissioning, then compare it during scheduled inspections. Inspect couplings, stem alignment, seals, limit switches, and position feedback. Check pneumatic filters and regulators; moisture can quietly damage components. For electric actuators, verify wiring, enclosure integrity, and travel calibration. Review cycle counts and alarm history before failure occurs. Maintenance teams often focus on the actuator and overlook the valve seat. That is a mistake. Also, a “perfect” maintenance interval rarely exists; process duty, contamination, and seasonal temperature changes should refine it. Use documented evidence, not habit.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

