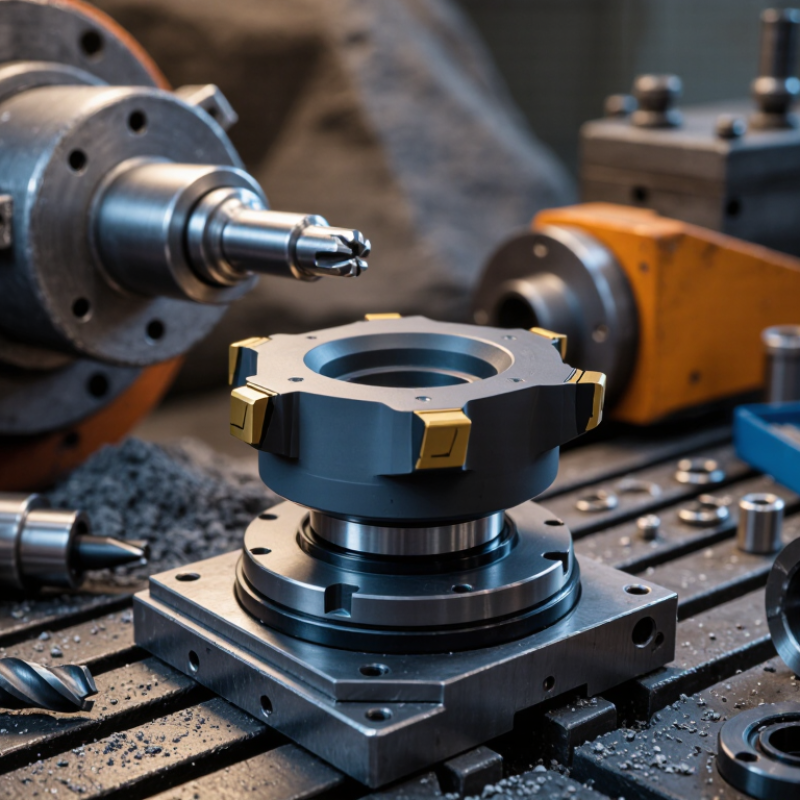
Tungsten Carbide Ceramic is often chosen when ordinary steel wears too quickly. Its extreme hardness helps components resist abrasion, cutting, and repeated contact. In workshops, it may appear as a compact cutting insert, a drill tip, or a wear-resistant nozzle. Mining equipment uses it against rock and mineral dust. Manufacturers also install it in dies, seals, guide parts, and other surfaces exposed to friction. The material can keep a sharp edge or stable shape under demanding conditions. That practical performance explains its value in manufacturing, energy, construction, and precision engineering.
The name deserves a closer look. Many commercial grades combine tungsten carbide particles with a metallic binder, commonly cobalt, rather than forming a pure ceramic body. This structure creates an important balance between hardness and toughness, although the balance changes with grade, grain size, and binder content. It resists wear strongly, but it is not indestructible. A sudden impact, poor support, or excessive heat can cause chipping or cracking. Small details matter. Selecting a grade without considering load, temperature, corrosion, and surface contact may shorten service life. Reliable recommendations should therefore come from verified material data, application testing, and experienced engineering judgment. Even then, performance can vary in real equipment. This guide examines where Tungsten Carbide Ceramic is used, why it works, and where its limitations deserve honest attention.
Tungsten carbide ceramic is an extremely hard engineering material made from tungsten and carbon. Its main phase, tungsten carbide, has a dense crystal structure that resists scratching, abrasion, and deformation. In practical products, fine tungsten carbide grains are often combined with a metallic binder, creating a cemented carbide composite rather than a completely pure ceramic. This difference matters because the binder can improve toughness while slightly reducing hardness.
The material is used where ordinary steel wears too quickly. Manufacturers shape it into cutting inserts, drilling components, wear plates, seals, nozzles, and forming tools. In a workshop, a carbide cutting edge can keep its shape while machining abrasive alloys or mineral-filled materials.
Its surface may look smooth and dark gray, but microscopic pores, grain size, and binder distribution strongly affect performance. Small changes can influence tool life.
Hardness is not everything. Tungsten carbide ceramic can crack under sudden impact, poor mounting, or rapid temperature changes. It also requires careful grinding because excessive heat may damage the edge. The material is costly to process, and incorrect selection can waste more money than it saves. A tougher grade may perform better in interrupted cutting, while a harder grade may suit steady abrasion. The label alone does not guarantee success. Real service conditions must guide the choice.
What Is Tungsten Carbide Ceramic Used For?
How Is Tungsten Carbide Ceramic Made?
Tungsten carbide ceramic begins as a fine powder made from tungsten and carbon. Manufacturers blend it with a controlled metallic binder, such as cobalt or nickel. The mixture is milled until the particles become evenly distributed. This stage strongly affects the final strength and wear resistance.
The prepared powder is dried, pressed into a compact shape, and sintered in a vacuum or protective atmosphere. Heat bonds the particles without fully melting the carbide structure. Pressure-assisted sintering may reduce internal pores. After cooling, diamond grinding gives the component its required dimensions and surface finish. Quality checks can include density testing, hardness measurement, microscopic inspection, and dimensional control. No batch is perfectly uniform. Small changes in powder size, binder content, or heat control can influence performance.
Tips: Choose the composition for the working condition. Higher hardness can improve wear life, but it may reduce toughness. Inspect edges carefully because sharp corners can chip under impact. Tungsten carbide ceramic is used in cutting inserts, drilling components, wear plates, seals, and forming dies. Confirm the expected load, temperature, chemical exposure, and vibration before selecting a grade. A practical test is valuable. Laboratory data may not reflect every real operating condition.
| Data Dimension | Typical Data or Process Information | Why It Matters | Common Uses or Notes |
|---|---|---|---|
| Material Definition | |||
| Material composition | Tungsten carbide (WC), a compound consisting primarily of tungsten and carbon. | The WC crystal structure provides high hardness, wear resistance, and compressive strength. | Used either as a binderless ceramic or as the hard phase in cemented carbide. |
| Ceramic classification | Binderless WC is a technical ceramic; WC combined with a metallic binder is commonly called cemented carbide or hardmetal. | The binder improves toughness, while binderless WC offers higher chemical purity and ceramic-like behavior. | The selected grade depends on the balance between hardness, toughness, corrosion resistance, and thermal performance. |
| Appearance and color | Usually dark gray to metallic gray; polished surfaces can have a bright reflective appearance. | Color and surface finish vary with porosity, grain size, binder content, and processing conditions. | Suitable for industrial components where surface durability is more important than decorative appearance. |
| Typical Physical and Mechanical Properties | |||
| Density | Approximately 15.6 g/cm³ for near-stoichiometric, dense WC; cemented grades commonly range from about 14 to 15.5 g/cm³. | High density contributes to mass, inertia, and resistance to penetration and deformation. | Important in wear parts, counterweights, mining tools, and precision components. |
| Hardness | Dense WC commonly measures roughly 1,800–2,400 HV, while cemented carbide grades often measure about 1,000–2,200 HV. | High hardness limits abrasive wear, scratching, edge rounding, and surface damage. | Cutting tools, dies, wear plates, nozzles, seals, and drilling components. |
| Fracture toughness | Binderless WC is relatively brittle; cemented carbide is commonly engineered in the approximate range of 5–20 MPa·m1/2, depending on binder content and grain size. | Higher toughness improves resistance to chipping and impact, but usually reduces hardness and wear resistance. | Fine-grained grades suit precision cutting; tougher grades suit interrupted cutting and heavy-duty drilling. |
| Thermal conductivity | Typically around 60–110 W/m·K, depending on purity, grain size, porosity, and binder content. | Good heat conduction helps distribute heat away from cutting edges and contact zones. | Useful in cutting tools, electrical contacts, heat-resistant fixtures, and high-load wear components. |
| High-temperature behavior | WC remains stable at high temperatures but can oxidize in air at elevated temperatures; it decomposes or reacts near its very high melting/decomposition range. | Operating temperature, atmosphere, and contact with reactive materials affect service life. | Suitable for hot wear applications when oxidation and thermal-shock conditions are properly controlled. |
| How Tungsten Carbide Ceramic Is Made | |||
| 1. Raw material preparation | Tungsten-containing feedstock is converted into tungsten powder, then reacted with carbon at high temperature to form WC powder. | Powder purity, carbon balance, and particle size strongly influence the final microstructure. | Typical WC powder particle sizes range from submicrometre scale to several micrometres. |
| 2. Powder blending | WC powder may be blended with a metallic binder, such as cobalt or nickel, together with processing additives. | Binder content and distribution control toughness, hardness, corrosion behavior, and shrinkage. | Binderless compositions are used when maximum ceramic purity and hardness are required. |
| 3. Milling and granulation | Wet or dry milling homogenizes the powder mixture; spray drying or granulation creates flowable particles for pressing. | Uniform powder flow reduces segregation, density variation, and defects in the green compact. | Process control is especially important for thin sections and complex shapes. |
| 4. Forming | The powder is shaped by uniaxial pressing, cold isostatic pressing, injection molding, extrusion, or other ceramic-forming methods. | Forming creates a fragile “green body” that contains the desired geometry before densification. | Oversized dimensions are intentionally designed to compensate for sintering shrinkage. |
| 5. Debinding | Organic binders and lubricants are gradually removed using controlled heating and, in some processes, solvent extraction. | Slow, controlled removal prevents cracking, distortion, and internal gas defects. | The debinding schedule depends on part thickness, binder chemistry, and furnace atmosphere. |
| 6. Sintering and densification | Cemented WC parts are commonly liquid-phase sintered at approximately 1,350–1,500 °C; binderless WC generally requires higher-temperature or pressure-assisted densification. | Sintering removes porosity and bonds WC grains into a dense, strong structure. | Vacuum, inert-gas, hot-isostatic pressing, or spark-plasma sintering may be used to improve density and reduce defects. |
| 7. Finishing and inspection | Diamond grinding, lapping, polishing, coating, dimensional inspection, and defect testing may be performed after sintering. | WC is difficult to machine conventionally, so diamond-based processes are commonly used for precision finishing. | Final quality checks may include density, hardness, microstructure, dimensions, and surface integrity. |
| Main Applications | |||
| Cutting and machining tools | Indexable inserts, end mills, drills, reamers, and wear-resistant cutting edges. | High hardness and hot hardness help maintain a sharp edge during material removal. | Used for machining metals, composites, wood-based materials, and abrasive nonmetallic materials. |
| Mining and drilling | Drill buttons, rock-cutting inserts, wear tips, and high-impact ground-engaging components. | Resistance to abrasion and compression extends service life in rock and mineral contact. | Tougher grades are selected where repeated impact and vibration are expected. |
| Metal forming and wire drawing | Drawing dies, extrusion dies, punches, forming rolls, and stamping components. | Low wear helps preserve dimensional accuracy and surface quality during repeated forming cycles. | Used when long die life and consistent product dimensions are required. |
| Fluid-handling components | Sealing faces, valve seats, pump parts, flow-control nozzles, and abrasive-slurry components. | Hard surfaces resist erosion, particle abrasion, and dimensional change at contact interfaces. | Performance depends on fluid chemistry, temperature, pressure, and the selected binder system. |
| Wear protection and industrial parts | Wear plates, guide components, bushings, bearings, sandblasting nozzles, and high-wear fixtures. | The combination of hardness, compressive strength, and thermal stability reduces replacement frequency. | Best suited to sliding, impact, erosion, or abrasive environments where ordinary steels wear rapidly. |

Tungsten carbide ceramic is used where surfaces face severe abrasion, repeated impact, or high contact pressure. Common applications include cutting inserts, mining tools, wear plates, nozzles, seals, and forming dies. Its performance comes from its structure: hard tungsten carbide grains are often held by a metallic binder. Pure ceramic and cemented carbide are not identical. This distinction matters.
ASM Handbook data places typical tungsten carbide hardness near 1,200–2,000 HV, depending on grain size and binder content. Its elastic modulus can exceed 500 GPa, helping components resist deformation under heavy loads. The material also has high thermal conductivity compared with many engineering ceramics. Heat can move away from a cutting edge more quickly. That benefit weakens when the design traps heat or uses an unsuitable grade. Small details matter.
The 2024 USGS Mineral Commodity Summaries reported approximately 84,000 metric tons of global tungsten mine production in 2023. This supply supports hardmetal production, but availability does not guarantee reliability. Tungsten carbide also offers strong corrosion resistance in many industrial environments, while its density is high, often around 14.5–15.2 g/cm³. It is heavy. It can also chip under sharp impact, despite its exceptional hardness. Engineers therefore balance hardness, toughness, grain size, binder percentage, and operating temperature. I would not call it indestructible. That would be poor engineering.
Tungsten carbide ceramic is valued for extreme hardness, compressive strength, and wear resistance. Its main industrial role is cutting and forming metal. Cemented carbide inserts machine steel, cast iron, stainless alloys, and difficult aerospace materials. The International Tungsten Industry Association reports that cemented carbide consumes about 60% of global tungsten use. That figure shows its industrial importance, although consumption estimates can vary by reporting method.
Mining and construction use tungsten carbide buttons on drill bits, road-milling tools, and rock breakers. These small grey inserts face sand, stone, heat, and repeated impact. Oil and gas equipment also uses carbide components in valves, nozzles, and wear sleeves. In metalworking plants, carbide dies guide wire and shape tubes under high pressure. USGS Mineral Commodity Summaries 2025 reported approximately 81,000 metric tons of tungsten mine production worldwide in 2024. China supplied about 67,000 metric tons. This concentration creates supply risks for manufacturers.
Tips: Match the grade to the load. Harder grades resist abrasion, but they may fracture under sharp impact. A tougher binder system can perform better in interrupted cutting. Check hardness, fracture toughness, grain size, and operating temperature together. “Ceramic” can be an imperfect label here. Many industrial grades are cemented composites, not fully binder-free ceramics. Field testing still matters, because laboratory wear results may not mirror dusty, wet, or vibration-heavy production floors.
Tungsten carbide ceramic is widely used where extreme hardness, wear resistance, and dimensional stability are required. The chart shows representative Vickers hardness ranges for common industrial applications. Actual values vary with carbide grain size, binder content, density, and manufacturing method.
Its main applications include cutting tools, mining and drilling inserts, wear-resistant liners and nozzles, metal-forming dies, and components exposed to severe abrasion in oil and gas equipment.
Tungsten carbide ceramic is used where ordinary steel wears too quickly. Typical applications include cutting inserts, mining tools, pump sleeves, nozzles, seals, and forming dies. Its high hardness resists abrasion, while its stiffness supports accurate machining. However, it is not unbreakable. A sharp impact can cause chipping or sudden fracture.
Grade selection should begin with the actual failure mode. For severe abrasion, engineers often choose a harder grade with fine carbide particles. For impact loading, a tougher grade may perform better, even if it sacrifices some hardness. Binder content also matters. More binder can improve toughness but may reduce wear resistance and corrosion performance. Particle size affects the balance between strength, edge stability, and surface finish. Temperature, pressure, chemical exposure, and contact speed must be reviewed together. One overlooked detail can shorten service life. Laboratory hardness data alone cannot predict every field result. Practical trials remain valuable, and the first selection may need revision.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.