


Choosing the right tester requires more than comparing prices, photos, or impressive specifications. The UP-1001 DIN Abrasion Tester is designed for evaluating wear resistance in rubber, elastomer, and similar materials under controlled abrasion conditions. For buyers, repeatability matters as much as appearance. A polished cabinet cannot compensate for unstable loading, uneven rotation, or poor calibration records.
This guide presents ten leading DIN abrasion testers for practical purchasing decisions. Each option is considered through key details, including abrasive drum design, specimen preparation, load control, measurement accuracy, and operator safety. We also examine documentation, replacement parts, service support, and compatibility with applicable testing methods. Small details matter. A clear scale can prevent reading errors. A firm clamping system can reduce inconsistent results. Reliable records support better laboratory decisions.
The comparison reflects common quality-control and research needs, but no ranking fits every facility. A footwear laboratory may prioritize fast testing, while a materials manufacturer may need stronger data traceability. Buyers should verify the current standard, calibration process, and supplier claims before ordering. Some published specifications may appear complete, yet omit practical information about maintenance or dust control. That gap deserves attention. Our assessment aims to combine technical knowledge with real-world usability, while acknowledging an important limitation: product performance can change with configuration, operator training, and service conditions. Use this overview as a focused starting point, not a substitute for method verification or hands-on evaluation.
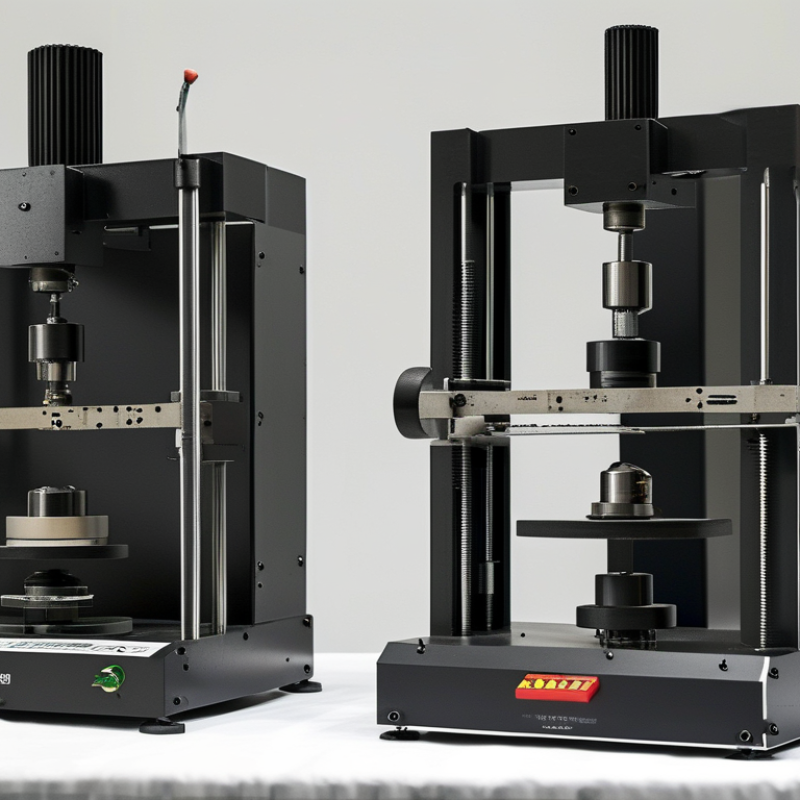
A DIN abrasion tester measures how much rubber or elastomer material is lost during controlled rubbing. The result is usually reported as relative volume loss, expressed in cubic millimetres. Lower loss generally indicates better abrasion resistance.
The test uses a cylindrical specimen, abrasive cloth, and a defined load. Under ISO 4649:2017, common conditions include a 10-newton load and a 40-metre sliding distance. The specimen rotates while contacting the abrasive surface. Technicians record its mass before and after testing, then apply material density to calculate volume loss. Small weighing errors can change the result.
The test is practical.
It helps compare outsole compounds, conveyor coverings, seals, and rubber wheels under repeatable conditions. A 2023 report from the European Tyre and Rim Technical Organisation identifies abrasion resistance as a key performance factor in tyre durability evaluations. However, DIN results do not predict every service environment. Heat, moisture, sharp stones, ozone, and repeated flexing may alter real-world wear.
That limitation matters. A compound with low DIN loss may still perform poorly on wet concrete or rough asphalt. Buyers should review specimen preparation, reference calibration, load settings, and test direction. Reports should include individual results, not only an average. Three readings may expose variation that one polished number hides.

Choosing among UP-1001 DIN abrasion testers requires more than comparing prices or exterior design. Check compliance with DIN 53516 or the applicable ISO 4649 method. Confirm the exact standard revision before testing. A reliable unit should provide controlled load, defined abrasive travel, stable rotation, and accurate specimen positioning. These details directly affect volume loss results, usually reported in cubic millimetres. Small alignment errors can produce surprisingly different readings.
Tips: Ask for calibration records, traceable reference materials, and a clear uncertainty statement. Verify the test wheel, abrasive sheet, specimen holder, and cutting tools. The machine should support repeatable conditioning and temperature control when required. Review whether its timer, counter, and measurement system are easy to inspect. Practical experience matters here. A technically impressive tester can still slow production if operators struggle with setup.
Compare the stated load range, rotation speed, stroke length, and specimen dimensions with your materials. Check whether replacement abrasives are consistently available and documented. Look for emergency protection and straightforward maintenance access. Ask how repeatability and reproducibility were validated, not only whether the tester “meets standards.” That wording can be vague. I would also run duplicate tests on a known reference compound before approving a purchase. No single specification proves long-term reliability; user training, calibration discipline, and laboratory conditions remain equally important.
Selecting a UP-1001 DIN abrasion tester requires more than checking its advertised price. In routine laboratory work, load stability often matters more than appearance. DIN 53516 uses a 10 N test force, a 40-metre abrasion path, and a standardized abrasive sheet. Confirm that the instrument controls these conditions accurately. ISO 4649 provides a related rotating-drum method, so method compatibility should be verified before purchase.
Check the specimen holder, cutter dimensions, drum speed, and abrasive-sheet alignment. A small positioning error can distort volume-loss results. The tester should offer clear calibration procedures, traceable weights, and repeatability records. Data logging is useful, but only when operators can export raw readings. According to Smithers’ 2024 rubber industry outlook, global rubber consumption exceeded 30 million tonnes annually, increasing pressure for dependable quality testing across industrial applications.
Look for overload protection, emergency stopping, dust control, and accessible replacement parts. Ask whether calibration support is available locally. It is easy to overlook servicing costs. A strong tester should also include a readable display and simple parameter settings, especially when several operators share one laboratory. However, no machine removes every source of uncertainty. Material hardness, surface texture, humidity, and operator technique can still affect results. One test may mislead. Run repeat specimens, compare reference materials, and question unusually good data.
Top 10 UP-1001 DIN Abrasion Testers Compared should be judged by repeatability, not appearance. DIN 53516 uses a defined abrasive path, load, and specimen size. A compliant tester should support the standard 10 N load and 40 m travel. It should also control drum speed near 40 rpm. Small deviations can distort volume-loss results. That matters when rubber compounds differ by only a few cubic millimetres.
For buyers, compare ten units across calibration stability, fixture alignment, dust extraction, and operator safety. A 2024 statistical release from the International Rubber Study Group placed global natural-rubber consumption near 15 million tonnes in 2023. Such scale makes comparable abrasion data valuable for footwear, seals, tires, and industrial components.
Look for traceable load verification and accessible calibration records. Digital displays help, but they do not prove accuracy.
Practical testing exposes differences quickly. Check whether the specimen holder stays rigid during a full abrasion cycle. Review replacement-drum availability and cleaning time. Cross-checking DIN 53516 results with ISO 4649 methods may reveal procedural variation, but the methods are not identical. A top-ten table still has limits. Some listings rely on brochures rather than interlaboratory evidence. Buyers should request repeatability data, raw test records, and service history before ranking any UP-1001 tester. Small details matter.
Selecting the right UP-1001 DIN abrasion tester requires more than comparing rankings. A top-ten list can guide research, but your laboratory needs a precise match. Begin by matching the tester’s load range with your material and testing method. Confirm specimen dimensions, drum speed, and abrasive sheet requirements. Check the reading system carefully. Small details matter. Ask whether the instrument provides stable pressure, repeatable rotation, and clear wear measurements. In routine testing, operators may lose time aligning samples or removing rubber dust. Choose a design with accessible controls, secure clamping, and simple cleaning access. These features support consistent daily work.
Reliability depends on verification, not attractive specifications. Request calibration records, uncertainty information, and a practical demonstration with a similar compound. Review how the tester handles different hardness levels and surface textures. A smooth rubber reference may behave differently from a textured sole. Keep temperature and humidity records near the test area. This step is often missed. Inspect the manual for specimen preparation, maintenance intervals, and troubleshooting instructions. If technical support is distant, confirm response times and spare-part availability before purchase. Do not judge the instrument by price alone. A low initial cost can become expensive when downtime interrupts release testing. One honest concern deserves attention: even a precise tester cannot correct poor specimen preparation. Uneven trimming can distort results, yet users may blame the machine. Build a short operator training check around alignment, cleaning, and result recording.
| Rank | Anonymous Tester Profile | Recommended Laboratory Use | Standard Basis to Verify | Test Load | Specimen Requirement | Drum Diameter | Drum Speed | Standard Abrasion Distance | Result Measurement | Key Buying Advantage | Critical Buyer Check |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Digital Fully Automatic Configuration | High-volume quality-control laboratories | DIN 53516 / ISO 4649, Method A or B capability | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m | Automatic distance stop with digital mass-loss or volume-loss calculation | Best repeatability and reduced operator workload | Confirm calibration functions, software traceability, and automatic stop accuracy |
| 2 | Programmable Semi-Automatic Configuration | Research and development laboratories | DIN 53516 / ISO 4649 with programmable test cycle | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m, programmable where permitted | Digital timer, revolution counter, and calculated abrasion loss | Good balance between flexibility and operating cost | Verify whether custom cycles affect formal standard compliance |
| 3 | Precision Manual Configuration | Small laboratories and routine material screening | DIN 53516 reference method | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m | Operator-controlled run with balance-based mass-loss calculation | Lower purchase and maintenance complexity | Check operator training, manual distance control, and balance readability |
| 4 | Dual-Method DIN/ISO Configuration | Contract testing and multi-standard laboratories | DIN 53516 and ISO 4649 method selection | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m for the standard reference cycle | Mass loss and volume loss using material density data | Supports broader customer and specification requirements | Confirm the supplied abrasive system and method-specific accessories |
| 5 | High-Throughput Multi-Station Configuration | Production laboratories testing many compounds daily | DIN 53516-compatible test station design | 10 ± 0.2 N per station | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal per station | 40 ± 1 rpm | 40 m | Parallel testing with individual specimen identification | Improves sample throughput and scheduling efficiency | Check station-to-station load uniformity and independent distance control |
| 6 | Compact Benchtop Configuration | University, pilot, and space-limited laboratories | DIN 53516 test geometry and operating conditions | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m | Digital or manual measurement depending on configuration | Small footprint with the essential abrasion-test functions | Measure required clearance for the drum, specimen holder, and dust extraction |
| 7 | Heavy-Duty Industrial Configuration | Rubber, tire, footwear, and conveyor-belt laboratories | DIN 53516 / ISO 4649 operating geometry | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m | Mass-loss measurement with durable specimen clamping | Suitable for frequent use and demanding production environments | Evaluate frame rigidity, motor duty cycle, guarding, and dust management |
| 8 | Traceable Metrology Configuration | Accredited and audit-focused testing laboratories | DIN 53516 / ISO 4649 with documented verification procedures | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m | Recorded load, speed, distance, mass, and density inputs | Supports audit trails and measurement-system documentation | Request calibration certificates, uncertainty data, and verification intervals |
| 9 | Safety-Enhanced Enclosed Configuration | Shared laboratories and operator-sensitive workplaces | DIN 53516-compatible enclosure and test arrangement | 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | 150 mm nominal | 40 ± 1 rpm | 40 m | Protected test chamber with interlock or guarded access | Reduces exposure to moving parts and abrasive dust | Check emergency stop, interlock behavior, visibility, and cleaning access |
| 10 | Entry-Level Teaching Configuration | Training, demonstrations, and basic comparative testing | DIN 53516 principles; formal compliance must be verified | Target: 10 ± 0.2 N | 16 ± 0.2 mm diameter; approximately 6 mm minimum thickness | Target: 150 mm nominal | Target: 40 ± 1 rpm | Target: 40 m | Manual or basic digital result recording | Accessible platform for learning abrasion-test fundamentals | Do not use for release decisions until load, speed, distance, and calibration are validated |
Buyer note: The listed values are the commonly referenced DIN 53516 / ISO 4649 test targets. Before purchase, verify the exact UP-1001 configuration, applicable method, abrasive sheet specification, calibration documentation, specimen dimensions, electrical requirements, and safety provisions with the supplier.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

