


Precision Work Rolls are small in profile but decisive in the mill. They contact the strip directly, influencing thickness, surface finish, and dimensional consistency. The World Steel Association’s World Steel in Figures 2024 reports that global crude steel production reached 1,892.2 million tonnes in 2023. That scale helps explain why roll performance matters across hot- and cold-rolling operations. It does not, by itself, identify the best roll for a particular mill.
The main types are commonly distinguished by material and service: forged-steel rolls, cast-steel rolls, high-speed-steel rolls, and carbide rolls. Each brings different trade-offs in wear resistance, toughness, surface quality, and operating cost. OECD steel-market analyses also examine capacity, trade, and decarbonization pressures—conditions that shape mill investment and maintenance priorities. Still, a report cannot replace operating data from the line. Strip grade, rolling load, coolant practice, and finishing requirements all matter. A detail worth checking.
This guide compares the leading roll types and explains where each may fit. It also considers limitations, not just advertised advantages. Material names can sound definitive. They are not. Roll life and product quality depend on design, heat treatment, grinding, and operating discipline. The right choice is usually specific to the stand and production target. There is no universal winner.
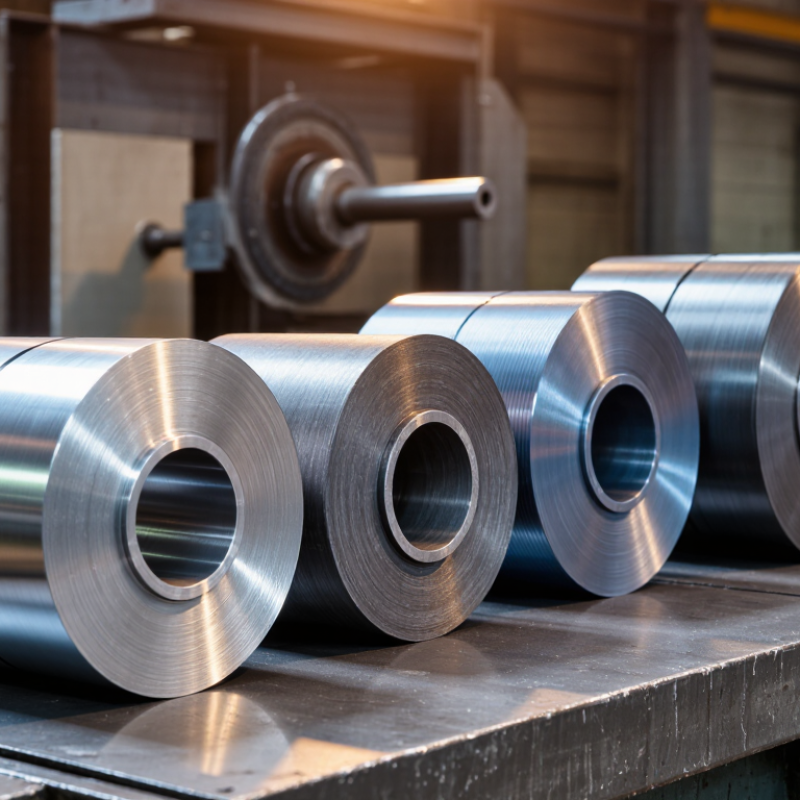
Precision work rolls are classified by mill, material, and duty—not by “precision” alone. In a four-high cold-rolling mill, smaller-diameter work rolls contact the strip directly, while backup rolls resist bending. Sendzimir mills use clustered roll arrangements and very small work rolls for thin, hard materials. The mill layout matters: a roll suitable for one stand may wear unevenly or deflect in another. World Steel Association data put 2023 global crude steel production at about 1.89 billion tonnes, underscoring the scale of rolling operations, though production volume alone does not determine roll choice.
Material selection follows contact pressure, surface finish, and wear demands. Forged steel rolls are common where toughness and resistance to fatigue are critical; high-chromium iron rolls can offer strong wear resistance in suitable applications. Carbide-based rolls may serve demanding finishing duties, but their brittleness and operating conditions need careful review. Hardness figures are meaningful only when the scale, test method, and roll layer are specified. Small detail. It changes comparisons.
Duty classification is just as practical: roughing, intermediate, and finishing work rolls face different loads, temperatures, and surface requirements. A finishing roll may need a highly controlled texture to transfer the required strip finish, while a roughing roll prioritizes durability under heavier reduction. Mill operators typically track wear, roll force, strip defects, and grinding history together. These are useful clues, not a perfect prediction; operating conditions can change faster than a specification sheet.

Cold-rolling work rolls face high contact pressure, repeated thermal changes, and abrasive strip surfaces. Their material affects wear, surface finish, and maintenance intervals. Three common choices are forged steel, high-chromium steel, and high-speed steel (HSS), each suited to different mill conditions.
Forged steel rolls offer toughness and resistance to impact. They can suit demanding stands where load changes are significant, though their wear resistance may be lower than that of harder alloys.
High-chromium rolls contain hard carbides that help resist abrasion and support a consistent strip finish. They are often considered for work that needs a balance of wear life and surface quality. A close look matters.
HSS rolls are designed to retain hardness under heat and resist wear, making them useful in demanding finishing applications. Their performance still depends on roll design, cooling, grinding, and the steel being rolled.
For example, a mill handling hard strip may value HSS wear resistance, while a stand exposed to impact may favor forged steel’s toughness.
No material wins everywhere.
Selection should follow operating data, including rolling force, temperature, surface requirements, and actual campaign life. Shop records can reveal patterns, but they are not perfect: changes in lubrication or grinding practice can blur comparisons.
Hot-strip work rolls face heat, pressure, scale, and repeated contact with moving steel. The main choices are ICDP, high-chromium iron, and high-speed steel (HSS). World Steel Association’s World Steel in Figures 2024 reports roughly 1.89 billion tonnes of crude steel production in 2023. That scale highlights why dependable roll life matters, though production volume alone cannot identify the best roll material.
ICDP rolls combine a hard working layer with a tougher core, making them a common option for finishing stands. High-chromium iron offers strong wear and oxidation resistance, useful where surface condition must remain stable over a campaign. HSS rolls contain hard carbides that help retain wear resistance under demanding hot-rolling conditions. They may extend campaigns, but grinding, cooling, and operating practice still matter. There is no universal winner. A tidy ranking can mislead: stand position, steel grade, and mill settings change the result.
Tips: Match roll material to the stand’s actual wear pattern, not just its nameplate role. Track roughness, wear, and grinding stock between campaigns. Small details matter. And mill data may be imperfect, so check trends across several campaigns before changing specifications.
Special-purpose work rolls refine strip after heavier reduction stages. Their job is not simply to make metal thinner. They influence surface texture, flatness, and the consistency of each pass. Small changes matter. A roll’s diameter, crown, finish, and material must suit the mill and product.
Temper rolls support a light reduction that improves shape and mechanical properties. Operators may use a controlled surface texture to transfer a chosen finish onto the strip. Skin-pass rolls perform a similar light treatment, often helping reduce yield-point markings and improve handling. The distinction can blur in practice, depending on the process and mill terminology. That deserves checking before specifying a roll.
Foil rolls need very smooth, carefully maintained surfaces because tiny marks can show on thin material. Clean handling matters; a trapped particle may leave a visible line. Leveling rolls address flatness rather than appearance alone. Their geometry and alignment help correct edge waves or center buckles as strip passes through the machine. Results depend on incoming material, tension, and setup, so roll selection cannot solve every shape problem. Measurements should guide adjustments, though mills do not always have perfect data.
Roll quality needs more than a polished surface and a hardness number. For steel, copper, and aluminum rolling, Rockwell C hardness provides a quick check of resistance to indentation. ISO 6508-1 defines the HRC method; the commonly used working range is 20–70 HRC. A reading near either end deserves careful interpretation. Surface condition, test location, and curved geometry can affect results. Measure several prepared spots, not just one convenient patch.
Small detail. It matters.
Brinell hardness, reported as HBW, uses a ball indenter and can help assess larger, potentially less uniform areas. ISO 6506-1 specifies the test method. HRC and HBW are different scales, so avoid treating a conversion chart as exact evidence of roll performance.
Surface finish is another key measure: Ra, in micrometres, describes average profile deviation from a mean line. ISO 21920-2 sets profile-texture parameters, while the measurement procedure and filter settings still matter. For example, a roll marked Ra 0.2 µm is not automatically suitable for every product or pass schedule. The target depends on material, lubrication, and the required strip finish.
Slightly imperfect, but important: a single Ra value cannot capture every scratch, waviness pattern, or isolated defect. Record the cutoff, instrument direction, and test locations alongside the result.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

