China Top Tile Leveling Spacers Suppliers?
Choosing reliable China Top Tile Leveling Spacers Suppliers requires more than comparing online prices. Product quality can affect floor alignment, installation speed, and the final appearance of a tiled surface. Experienced buyers usually examine material strength, molding accuracy, packaging, and production consistency before placing large orders.
Tile Leveling Spacers are commonly produced in different sizes, shapes, and materials. Some suppliers offer reusable wedges, screw systems, clips, or complete leveling kits. A dependable manufacturer should explain suitable applications clearly, such as large-format porcelain tiles, wall tiles, or uneven flooring. Ask for samples. Test them on real tile edges. Small details matter.
This guide reviews key factors behind China’s leading suppliers, including factory experience, quality control, customization ability, communication, and export service. It also considers whether a supplier can maintain stable dimensions across repeated batches. Certifications may support trust, but documents alone cannot prove daily production quality. That point is easy to miss.
Buyers should request product specifications, inspection records, packaging photos, and sample feedback before deciding. Clear communication about tolerances, clip thickness, delivery schedules, and replacement policies can prevent expensive misunderstandings. Supplier rankings may change as factories update equipment or enter new markets. Therefore, “top” should mean the best fit for a specific project, not merely the lowest quotation.
Some suppliers look impressive online. Reality needs checking. A careful comparison helps importers find dependable partners for consistent tile installation results.
Tile Leveling Spacers Explained: Clips, Wedges, Caps, and Reusable Bases
Tile leveling spacers help installers control lippage while adhesive cures. The system usually includes clips, wedges, caps, or reusable bases. Each part has a different job.
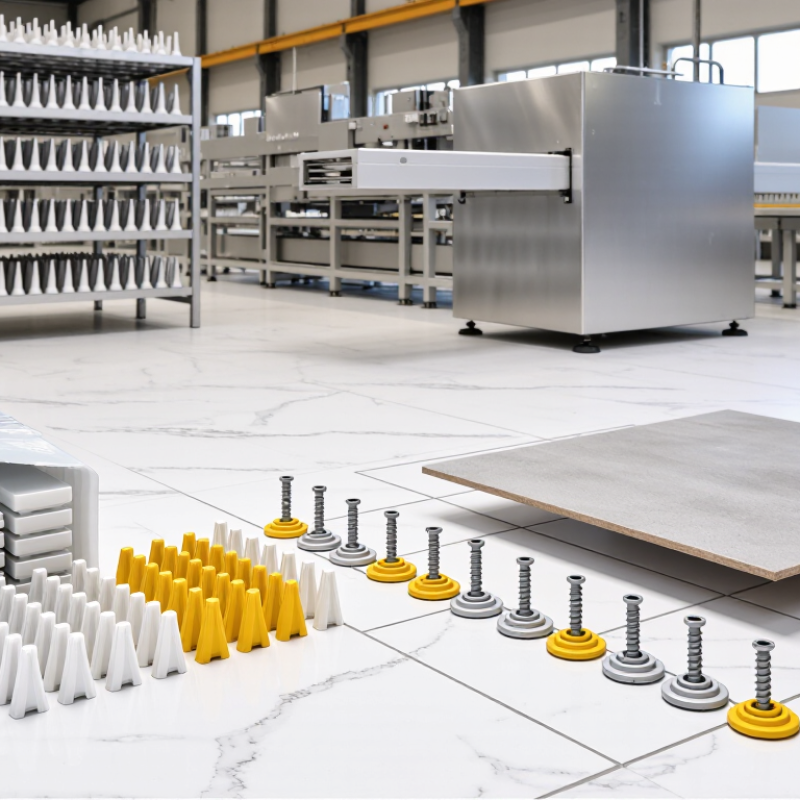
Clips sit beneath adjacent tiles and create a consistent joint. They are often made from rigid plastic with a calibrated thickness. Wedges slide through the clips and apply downward pressure. This pressure helps align tile edges across uneven floors. Caps provide a broader grip and feel easier to adjust by hand. They can be useful when wearing gloves or working with large-format porcelain.
Reusable bases use a different approach. A threaded or rotating base supports repeated installations, reducing disposable plastic waste. However, the base must remain clean. Dried adhesive can affect its movement and alignment. I have found that small debris causes more trouble than expected. A quick inspection saves time later.
When comparing China-based tile leveling spacer suppliers, ask for clip thickness tolerance, wedge strength, and material specifications. Request samples before placing a large order. Test them on the actual tile thickness and joint width. Check whether clips break cleanly without damaging tile edges. Packaging also matters, especially during long-distance shipping. A low price may hide inconsistent molding or weak wedges. That lesson is easy to overlook. Reliable suppliers should provide clear test records, stable dimensions, and responsive technical support.
Tile Leveling Spacers Explained: Clips, Wedges, Caps, and Reusable Bases
This chart maps the standard roles of the main tile leveling spacer components. Clips position adjacent tiles and define the joint, wedges apply tightening force, caps help hold the wedge in place, and reusable bases are designed for repeated installation use. The values represent whether each component normally performs the listed function, not company or brand performance.
Joint-Width Selection: 1–3 mm Spacers and ANSI A108.02 Layout Rules
Choosing tile leveling spacers starts with the finished joint, not the supplier’s product photo. For most residential installations, 1–3 mm spacers cover common layout needs. A 1 mm joint suits rectified tile with highly consistent edges. A 2 mm joint offers more tolerance for minor size variation. A 3 mm joint is safer for calibrated tile or larger format surfaces.
ANSI A108.02 states that grout joints should be at least three times the actual facial-dimension variation between tiles. It also identifies 1/16 inch, approximately 1.6 mm, as a minimum reference for rectified tile. That makes a 1 mm spacer potentially too narrow when tile variation exceeds 0.33 mm. Measure several tiles, not just one. Small differences become obvious beside a window.
The TCNA Handbook for Ceramic, Glass, and Stone Tile Installation reinforces substrate preparation, movement accommodation, and consistent joint planning. A leveling clip can reduce lippage, but it cannot correct an uneven substrate. Industry quality reports also frequently connect installation defects with poor preparation rather than spacer failure. Suppliers should provide verified spacer dimensions, compatible clip pressure, and clear material tolerances. One practical mistake is trusting nominal size alone. A “2 mm” spacer may produce a different joint after clip tension, tile warpage, and adhesive compression. Test a small area first. Then reconsider the selected width.
China Top Tile Leveling Spacers Suppliers? - Joint-Width Selection: 1–3 mm Spacers and ANSI A108.02 Layout Rules
Joint-width selection guide for tile layout planning. Spacer size indicates the intended nominal grout joint; final selection must account for tile dimensional variation, installation tolerances, substrate conditions, and the project specification.
| Nominal Spacer Size | Approx. Inch Size | Typical Tile Application | Recommended Tile Characteristics | ANSI A108.02 Layout Check | Selection Status |
| 1 mm | 0.0394 in | Very narrow interior joints; precision layout where the tile system and grout manufacturer permit a narrow joint. | Rectified or highly dimensionally consistent porcelain and ceramic tile with clean, uniform edges. | The actual facial-dimension variation should generally be no more than approximately 0.33 mm for a 1 mm nominal joint under the three-times variation check. | Precision use |
| 1.5 mm | 0.0591 in | Narrow-joint walls, backsplashes, and selected floor installations with accurately calibrated tile. | Rectified tile with consistent length, width, and edge geometry; suitable grout requirements must be confirmed. | Use only when measured tile variation is approximately 0.50 mm or less and the specified grout system supports the planned joint width. | Narrow joint |
| 2 mm | 0.0787 in | Common narrow-joint option for rectified porcelain and ceramic tile in controlled indoor layouts. | Rectified or well-calibrated tile with relatively consistent edges and a flat, properly prepared substrate. | For a 2 mm nominal joint, measured facial-dimension variation should generally be approximately 0.67 mm or less under the three-times variation check. | Balanced choice |
| 2.5 mm | 0.0984 in | Small-format or medium-format installations requiring slightly more tolerance than a 2 mm joint. | Rectified tile or calibrated tile with minor dimensional variation; useful where visual alignment remains important. | Allows approximately 0.83 mm of measured facial-dimension variation when applying the three-times variation relationship. | Tolerance focused |
| 3 mm | 0.1181 in | General-purpose narrow joint for many rectified tile layouts and selected calibrated tile installations. | Rectified or calibrated tile; often more forgiving of small manufacturing and installation variations than 1–2 mm joints. | For a 3 mm nominal joint, measured facial-dimension variation should generally be approximately 1.00 mm or less under the three-times variation check. | More forgiving |
| Core ANSI A108.02 Rule | The nominal grout joint should be at least three times the actual variation in facial dimensions of the tile being installed. Measure representative tiles from the batch before finalizing spacer size; do not select a joint solely by appearance. |
| Important Installation Note | Spacers establish alignment and nominal joint width, while leveling clips or wedges help control lippage. Neither system corrects an uneven substrate, warped tile, excessive dimensional variation, or inadequate mortar coverage. Always follow the current project specification, grout instructions, movement-joint requirements, and applicable installation standards. |
Tile Thickness Coverage: Comparing 3–20 mm Clip-and-Wedge Systems
China Top Tile Leveling Spacers Suppliers?
Tile Thickness Coverage: Comparing 3–20 mm Clip-and-Wedge Systems
When comparing tile leveling spacers from China-based suppliers, check thickness coverage before unit price. A 3–20 mm system sounds flexible, but one clip rarely performs equally well across that range. Thin porcelain tiles may need narrow clips with controlled pressure. Thick slabs require stronger clips and deeper wedge engagement. Ask for tested dimensions, not only catalog claims.
For 3–6 mm tiles, smaller clips can reduce movement around delicate edges. A 6–12 mm range suits many wall and floor tiles. From 12–20 mm, clip strength becomes more important, especially with heavy stone or large-format panels. During a practical trial, place clips on four corners and along long edges. The joint should remain consistent without forcing the wedge. Too much pressure can lift one tile or damage a fragile glaze.
Supplier reliability also depends on molding accuracy, wedge smoothness, and packaging consistency. Request samples from different production batches. Measure the clip opening with a caliper. Small variations can create visible lippage across a large floor. I have found that installation speed is not always improved by tighter wedges. Sometimes, a slower adjustment gives a flatter result. That detail is easy to overlook. Suppliers should provide material data, usage instructions, and clear replacement policies for broken clips. The best choice depends on tile thickness, joint width, substrate flatness, and installer control.
Supplier Quality Checks: ISO 9001, ISO 2859-1, and Mold Tolerance Data
When comparing China tile leveling spacer suppliers, inspect the quality system before judging price. The ISO Survey 2023 recorded more than 1.26 million ISO 9001 certificates worldwide. Certification shows process control, but it does not guarantee accurate spacers. Request recent audit records, corrective-action reports, and batch inspection results. A reliable supplier should explain how operators control resin moisture, injection pressure, cooling time, and packing.
ISO 2859-1 provides a structured sampling method for incoming and final inspection. Ask for the lot size, inspection level, AQL, sample quantity, and acceptance criteria. Do not accept “passed” without numbers. Mold tolerance data should show cavity measurements, parting-line offset, flash height, and dimensional drift across cavities.
For a 1.50 mm spacer, a stated tolerance such as ±0.05 mm is more useful than “high precision.” Also request gauge calibration records and measurement-system studies. A small Cpk table can reveal more than attractive photos. Yet one weakness remains: a single production report may hide seasonal variation or tool wear.
Tips: Ask for three consecutive lot reports. Compare cavity-to-cavity results, not only averages. Check whether inspection samples represent the full shipment. ISO 2859-1 is a sampling framework, not a substitute for technical judgment. Before approval, test assembly pressure, break resistance, and removal performance on actual tiles. I would also keep a retained sample from every accepted lot. It feels excessive, but disputes often begin with missing evidence.





