


Threaded Linear Shaft technology remains a practical choice for guided movement, positioning, and compact mechanical assemblies. Its value appears in quieter indexing systems, adjustable fixtures, packaging equipment, and laboratory instruments. Buyers now expect accurate threads, consistent straightness, corrosion resistance, and dependable delivery.
Industry reports provide useful market context. Grand View Research’s Linear Motion Market report identifies automation, robotics, and industrial equipment as major growth drivers. MarketsandMarkets also connects rising factory automation with stronger demand for precision motion components. However, these reports usually combine shafts, guides, screws, and related systems. They rarely isolate the Threaded Linear Shaft category. That limitation deserves attention.
Professor Alexander H. Slocum, a recognized authority in precision machine design, writes, “Precision machine design is a blend of art and science.” His observation applies directly here. A shaft can look flawless, yet poor thread geometry or weak surface treatment may cause binding, vibration, and early wear. Small details matter.
This guide reviews seven leading Threaded Linear Shaft suppliers worldwide. The comparison considers material grades, thread accuracy, surface finishes, customization, production capacity, documentation, and shipping reliability. Supplier claims are not treated as proof. Technical drawings, inspection records, tolerances, and application experience matter more.
Some rankings may remain debatable. Regional strengths can change quickly. A supplier with excellent machining may offer limited after-sales support. Another may provide attractive prices but inconsistent lead times. These practical differences shape purchasing risk, especially when one shaft failure stops an entire production line.
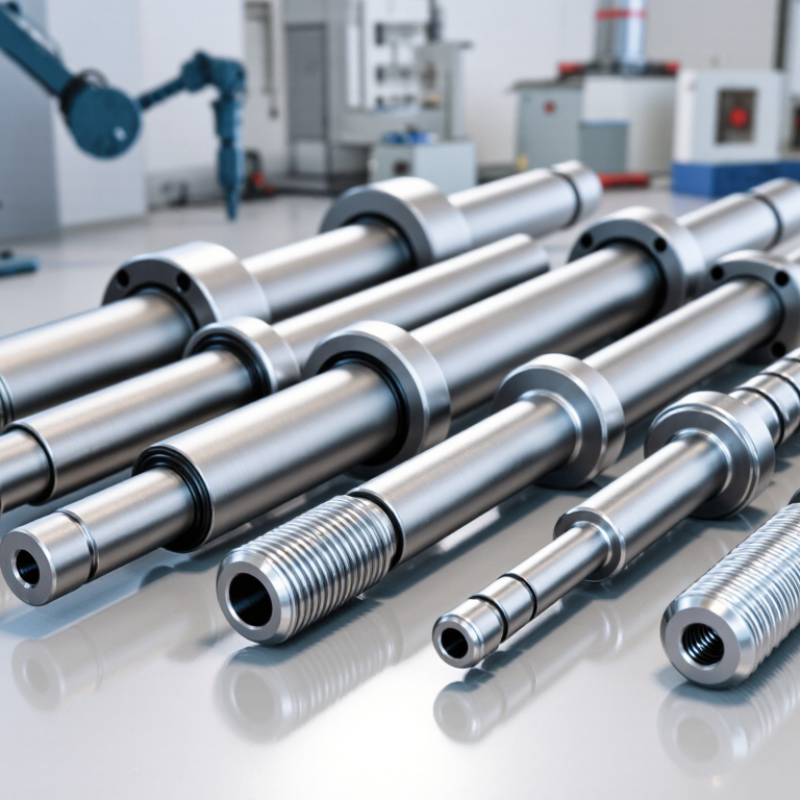
Threaded linear shafts combine a precision shaft with external threads for guided movement and secure positioning. Unlike a plain shaft, the threaded section can connect with a nut, bearing block, or adjustable support. When the shaft rotates, the matching nut moves along its length. This converts rotary motion into controlled linear travel.
These components appear in packaging equipment, laboratory instruments, automation systems, and compact lifting mechanisms. For example, a threaded shaft may move a sensor slowly across a rail or adjust a cutting head by measured increments. Engineers usually assess thread pitch, shaft diameter, material hardness, straightness, and surface finish. The correct choice depends on load, travel speed, alignment, and operating environment. A polished surface may reduce friction, but it cannot correct poor installation.
Tips: Confirm the thread standard before ordering. Measure the usable length, not only the overall length. Check the nut material and lubrication requirements together. Suppliers should provide dimensional tolerances, inspection records, and material information. These details support reliable sourcing worldwide.
In practical projects, selection is rarely perfect on the first attempt. A shaft can meet its load rating yet produce unwanted vibration. Fine threads offer careful adjustment, but they may increase movement time.
Coarse threads move faster, though positioning can become less precise. Real testing still matters. Ask for samples when tolerances are critical, and inspect runout before full production.

When comparing global threaded linear shaft suppliers, start with the shaft’s working conditions, not the catalog photograph. Diameter, thread form, pitch, hardness, straightness, and surface finish affect motion accuracy. Ask for material certificates and inspection records. A supplier should explain its testing method clearly. Vague answers deserve caution. Small details matter.
Request samples made to your actual drawing. Check thread engagement with the mating nut, runout over the full length, and burrs near the ends. In one production review, a shaft met the stated diameter but showed uneven plating, which increased friction during cycling. That defect was not obvious at first. It became expensive later. Suppliers with documented process controls, calibrated gauges, and traceable batch numbers are easier to trust. Still, paperwork alone cannot prove field performance.
Compare manufacturing capacity, minimum order quantities, lead times, packaging, and technical communication across regions. Confirm how the supplier handles design changes, nonconforming parts, and replacement claims. Clear escalation contacts reduce downtime. Ask whether heat treatment and straightening occur in-house or through subcontractors. This can reveal hidden variation. Price deserves attention, but total cost includes inspection, freight, rejects, and maintenance. A cheaper shaft may not remain cheaper after installation. I would also review references from applications with similar loads and travel speeds, while admitting that supplier promises can look stronger than real-world results.
The seven leading threaded linear shaft suppliers worldwide usually differ by engineering strength, not marketing language. Some specialize in hardened steel shafts for factory automation. Others focus on stainless steel parts for clean rooms, packaging equipment, and outdoor machinery. Several offer custom threading, tight diameter control, and ground surfaces for smoother motion. Experienced buyers should examine material certificates, thread accuracy, straightness, surface hardness, and production repeatability. A supplier with strong inspection records often delivers more reliable results than one offering the lowest quotation. Custom support also matters when shaft length, pitch, or mounting details fall outside standard drawings.
A practical comparison should include seven supplier profiles from different manufacturing regions. Review machining equipment, heat-treatment control, export experience, engineering communication, and after-sales response. Do not judge quality from polished photographs alone. Factory audits, inspection reports, and application references provide stronger evidence. Some suppliers may excel at prototypes but struggle with volume production. Others may offer excellent capacity yet provide limited design guidance. No list is flawless. Buyers should reconsider rankings after testing actual parts in their own assemblies. This step reveals noise, friction, alignment problems, and service gaps that brochures rarely mention.
When comparing seven threaded linear shaft suppliers worldwide, begin with material evidence, not polished photographs. Ask for the steel grade, hardness range, surface treatment, and corrosion test results. A reliable supplier should provide mill certificates and inspection records for each production batch. Stainless steel may suit humid equipment, while hardened alloy steel often handles repeated loads better. The correct choice depends on speed, load, lubrication, and operating temperature.
Precision requires measurable details. Request shaft diameter tolerance, straightness, thread accuracy, surface roughness, and radial runout. Ask how these values are inspected. A supplier using calibrated gauges and documented sampling procedures deserves greater confidence. During a previous sourcing project, a shaft met its diameter specification but still caused vibration. The overlooked factor was slight runout near the threaded section. Small defects matter.
Customization should begin with a clear drawing, including thread length, end chamfers, keyways, and mounting features. Confirm whether prototypes receive the same inspection as full production. Lead times also need evidence. Separate sampling, machining, treatment, inspection, and shipping time in writing. A low quoted lead time can hide outside processing delays. Request production photos or milestone updates when schedules are critical. I once accepted an attractive timeline too quickly; packaging requirements later added several days. That mistake changed how I compare suppliers.
Choosing among the seven best threaded linear shaft suppliers worldwide requires more than comparing prices. Your application should guide the decision. Check shaft diameter, thread type, travel length, load direction, and operating speed. A shaft for a packaging machine may need different surface hardness than one used in laboratory equipment.
Reliable suppliers provide material certificates, dimensional reports, and clear tolerance data. Ask whether each shaft is ground, polished, or simply machined. Surface finish affects friction and service life. Confirm thread accuracy with sample parts before ordering large quantities. In my experience, a low quotation can become expensive when poor alignment causes vibration, noise, or premature wear. Budget lies sometimes. Lead time, packaging quality, replacement support, and shipping stability also deserve attention.
Tips: Request a sample shaft and test it with your actual nut, bearing, or support block. Measure fit after cleaning the part. Ask for batch traceability and inspection records. Compare the complete cost, including tooling, freight, rejected parts, and downtime. Do not select the cheapest option automatically. It may perform well, but only under conditions different from yours. I have seen technically excellent shafts fail because the surrounding structure was too flexible. Supplier advice matters, yet your own application data should make the final decision.
| Supplier Profile | Primary Supply Region | Common Shaft Materials | Typical Thread Standards | Typical Shaft Diameter Range | Typical Length Range | Surface Finish Options | Typical Dimensional Tolerance | Typical MOQ | Indicative Lead Time | Budget Position | Best-Fit Applications |
|---|---|---|---|---|---|---|---|---|---|---|---|
| Profile A | North America | Carbon steel, stainless steel, alloy steel | UNC, UNF, metric coarse, metric fine | 8–50 mm | 100–2,000 mm | Ground, polished, black oxide, electroless nickel | Generally IT6–IT9, depending on process | 1–10 pieces for standard sizes | 2–5 weeks | High | Prototype work, automation equipment, replacement parts, low-volume precision builds |
| Profile B | Western Europe | Hardened carbon steel, stainless steel, tool steel | Metric coarse, metric fine, custom thread profiles | 10–80 mm | 150–3,000 mm | Induction-hardened, chrome-plated, ground, polished | Typically IT5–IT8 for precision-ground products | 1–5 pieces for engineered orders | 4–8 weeks | High | High-speed linear motion, machine tools, inspection systems, high-duty industrial equipment |
| Profile C | Central Europe | Stainless steel, carbon steel, case-hardened steel | Metric coarse, metric fine, left-hand threads on request | 6–60 mm | 80–2,500 mm | Rolled, ground, polished, corrosion-resistant coatings | Typically IT6–IT9 | 5–20 pieces | 3–7 weeks | Medium to high | Packaging machinery, robotic assemblies, material-handling systems, general factory automation |
| Profile D | East Asia | Stainless steel, alloy steel, chrome-molybdenum steel | Metric coarse, metric fine, JIS-compatible specifications | 8–70 mm | 100–3,000 mm | Ground, polished, hard-chrome plated, nitrided | Typically IT6–IT9; tighter grades available by quotation | 10–50 pieces | 3–6 weeks | Medium | Electronics equipment, compact automation, medical-device mechanisms, laboratory machinery |
| Profile E | China | Carbon steel, stainless steel, bearing steel, alloy steel | Metric coarse, metric fine, UNC, UNF | 6–100 mm | 50–4,000 mm | Rolled, polished, ground, black oxide, hard chrome | Typically IT7–IT10 for standard production; tighter tolerances by request | 20–100 pieces, with samples often available | 2–6 weeks | Low to medium | Cost-sensitive automation, OEM production, conveyors, fixtures, and replacement components |
| Profile F | United Kingdom and Ireland | Stainless steel, carbon steel, tool steel | Metric, BSW, UNC, UNF | 8–50 mm | 100–2,000 mm | Bright polished, ground, hard chrome, passivated stainless steel | Typically IT6–IT9 | 1–10 pieces for stocked or semi-standard items | 2–5 weeks | Medium to high | Maintenance, laboratory equipment, custom machinery, small-batch engineering projects |
| Profile G | Southeast Asia | Stainless steel, carbon steel, alloy steel | Metric coarse, metric fine, UNC, UNF | 6–75 mm | 100–3,000 mm | Polished, ground, black oxide, zinc or nickel plating | Typically IT7–IT10 | 25–100 pieces | 4–8 weeks | Low to medium | High-volume OEM parts, general industrial equipment, agricultural machinery, and cost-focused projects |
Note: The figures above are representative industry ranges for anonymized supplier profiles, not quotations from named companies. Actual capability, tolerance, minimum order quantity, pricing, material certification, and delivery time should be confirmed against the supplier’s current technical drawing and quotation.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

