


What Are the Top TCP Perforating Gun Manufacturers in China

Choosing a Tcp Perforating Gun manufacturer in China requires more than comparing catalog prices. A dependable system must match the well plan, tubing configuration, operating conditions, and required perforation performance. Small details matter: connection dimensions, pressure ratings, material specifications, and the clarity of test records can affect purchasing decisions. This guide examines manufacturers through practical criteria, including product range, engineering capability, quality control, customization, delivery support, and after-sales service.

Look closely at the evidence. Ask whether a supplier can provide current technical data, inspection records, and clear answers about compatibility and operating limits. Factory capacity and export experience may be useful indicators, but they do not prove that every product suits every project. A careful comparison should distinguish verified information from marketing language. No shortlist is perfect. Supplier capabilities can change, and public information may be incomplete. That limitation deserves attention, not glossing over. The sections ahead outline how to assess leading Chinese manufacturers and prepare more informed questions before requesting a quotation. The goal is not to declare one universal winner, but to help buyers identify a Tcp Perforating Gun supplier whose documented capabilities fit their specific requirements.
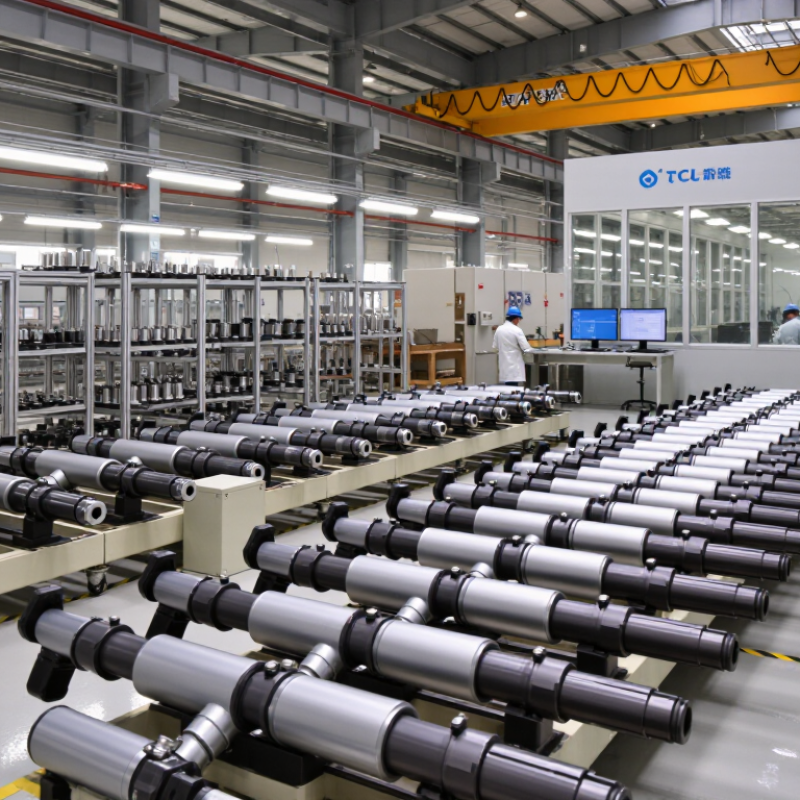
What Are the Top TCP Perforating Gun Manufacturers in China

TCP Perforating Guns: 2⅞–7-in. Diameters and 4–12 Shots per Foot

TCP perforating guns are available in diameters from 2⅞ to 7 inches, with shot densities commonly ranging from 4 to 12 shots per foot. These options let completion teams match the gun to the wellbore and perforation plan. Smaller diameters may suit restricted tubing or casing, while larger carriers can allow different charge layouts. Actual capacity depends on the specific design.

Shot density affects how closely perforations are spaced along the interval. Four shots per foot creates wider spacing; twelve creates a denser pattern. More shots do not automatically mean better results. Charge type, phasing, casing size, cement quality, and formation properties all matter. Details matter.

Before selecting a configuration, engineers typically check conveyance limits, pressure and temperature ratings, and compatibility with the completion. They also consider debris management and the planned firing sequence. A gun that fits on paper may still be difficult to convey through a deviated section. That part is easy to underestimate. Performance should be assessed against documented test conditions and the well’s actual geometry, not diameter or shot count alone.


China’s Supplier Landscape: CNPC, Sinopec, and Specialist Manufacturers

China’s TCP perforating-gun supplier landscape includes large state-owned energy groups and specialist manufacturers. Major national oil companies often support procurement, engineering coordination, and field-service networks. Their scale can help operators align equipment with established well designs. However, availability and technical support may differ between regions and projects.

Specialist manufacturers focus more narrowly on gun systems, connections, materials, and configuration options. Buyers should compare documented pressure and temperature ratings, dimensional compatibility, quality controls, and traceability records. Ask how inspection results are recorded, not only whether testing is performed. Fit comes first. A gun that looks suitable on paper may still require careful review against the well program and completion interface.

Supplier selection should include technical discussions with engineers and a review of relevant project experience. Request clear documentation, realistic delivery schedules, and a defined process for handling nonconforming parts. Field feedback can be useful, but it should be checked against verifiable records. One caution: product descriptions are not always directly comparable. I would not treat a broad catalog as proof of proven performance. The best choice depends on the application, support capacity, and evidence the supplier can provide.

Compare Manufacturers Using API RP 19B Flow-Performance Test Data

Selecting a TCP perforating gun manufacturer requires more than comparing catalog specifications. API RP 19B test records can provide a shared basis for reviewing perforator performance. Check the standard’s edition, test setup, target materials, and reported measurements. Without these details, two results may look comparable but describe different conditions.

For flow-performance comparisons, look for clearly documented flow-area or flow-test methods, where available, alongside entry-hole size and penetration data. Ask whether the tested gun used the same casing, cement, charge design, shot density, and phasing planned for the well.

Small changes matter. A larger entry hole alone does not prove better flow; debris, formation damage, and test conditions can influence results. Keep test measurements separate from predicted downhole production.

Request complete reports, not just a single performance figure. Check sample counts, repeatability, and any stated limitations. An independent test report can strengthen confidence, though it cannot guarantee field results.

One detail is easy to miss: API RP 19B data support controlled comparison, not a universal ranking of manufacturers. I would still question any claim that lacks raw measurements or a clearly described test method.

Match Gun Systems to Well Conditions: Pressure, Temperature, and Tubing Size

Selecting a TCP perforating system starts with the well’s actual pressure and temperature envelope, not a catalog headline. Compare the planned hydrostatic pressure, expected pressure differential during firing, and credible temperature extremes with the gun, seals, detonating components, and firing system ratings. API RP 19B provides a recognized framework for evaluating perforating performance; review test documentation for penetration and entrance-hole results, and check whether test conditions resemble the intended application. A rating without its test conditions is incomplete.

Tubing clearance is just as important. API 5CT dimensional tables include common tubing outside diameters of 2⅜, 2⅞, and 3½ inches, but wall thickness changes the available inside diameter. Check the full assembly, including connections, restrictions, and gun centralizers, against the completion’s tightest drift. Small clearances can complicate running and retrieval. Measure, don’t assume.

Ask manufacturers for configuration-specific pressure and temperature limits, test records, and dimensional drawings. Then compare those values with the well program’s uncertainty margins, not only its expected operating point. A system that fits on paper may still be awkward to handle offshore. I would also flag any mismatch between the qualification test and the planned well conditions; it is easy to overlook when schedules are tight.

TCP Perforating-Gun Selection: Tubing Size Reference

Bars show standard nominal tubing outside diameters in inches, a key dimension when checking gun clearance. Actual internal clearance depends on tubing weight, connections, and restrictions. Pressure and temperature limits are specific to the selected gun and its components; verify them against the well conditions and equipment specifications.

Assess Suppliers by Field Records, Quality Certifications, and Delivery Capacity

Choosing a TCP perforating gun manufacturer in China requires evidence beyond a polished catalog. Ask for field records from wells with comparable pressure, temperature, gun length, and shot density. Request anonymized job summaries, failure data, and post-job inspection notes where available. Details matter. A record from a shallow, cool well may not predict performance in a hotter interval.

Verify current quality certificates with the issuing body, and check that their scope covers design, machining, assembly, and testing. Certificates help, but they do not prove every configuration has been qualified. Review material traceability, dimensional inspection reports, pressure-test records, and procedures for handling nonconforming parts. A tidy document pack can still leave gaps. Ask who reviewed the records and when.

Delivery capacity deserves the same scrutiny as product quality. Compare quoted lead times with recent order history, available production slots, and inventory of critical components. Check how the supplier manages design changes, rejected parts, and replacement orders. One weak point in many evaluations is reliance on sales estimates alone. A factory visit or independent audit can clarify actual capacity, though neither removes field uncertainty. Define acceptance criteria and delivery milestones before placing an order.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
