


Top 10 Shuttle Rotomolding Machines for Global Buyers

Choosing a Shuttle Rotomolding Machine is rarely a simple equipment purchase. Global buyers must balance output, mold size, energy use, automation, and service support. In practice, a machine that performs well in one factory may disappoint elsewhere. Plant layout, resin handling, labor skills, and local operating conditions can change the result. This guide introduces ten shuttle rotomolding machines selected for practical comparison, not promotional claims. Real performance matters.

Our review focuses on evidence buyers can verify: carriage design, oven temperature control, cooling capacity, cycle consistency, hydraulic or electric movement, and operator access. We also consider production flexibility, mold-change time, spare-parts availability, training, warranty clarity, and supplier responsiveness. These details often decide whether a line runs smoothly after installation. A polished brochure cannot replace trial data, factory references, and a clear technical specification. Buyers should request sample parts and confirm expected wall thickness, dimensional stability, and cycle times before signing a contract. That step is easy to overlook.

The ranking is a starting point, not an absolute verdict. Pricing, regional support, import requirements, and energy costs may alter the best choice. Some established machines may offer stronger reliability, while newer systems may provide useful automation at a lower initial cost. We compare strengths, limitations, and suitable applications with a balanced view. Readers should verify certifications and applicable local standards independently. Careful questions produce better decisions.
Top 10 Shuttle Rotomolding Machines for Global Buyers

Shuttle Rotomolding Machines: Design, Function, and Core Components

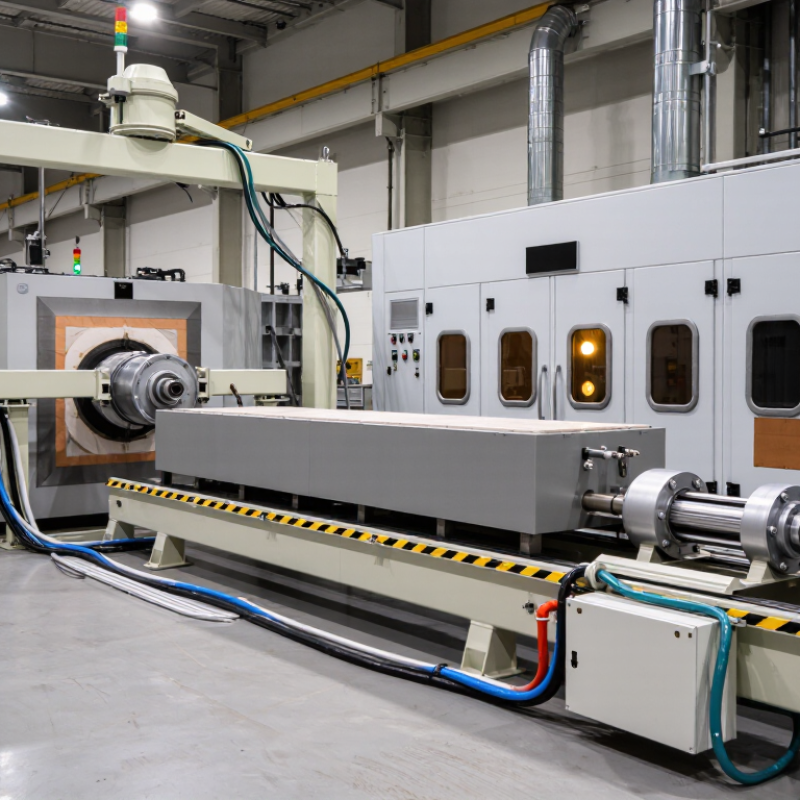
Shuttle rotomolding machines use a moving carriage to serve two or more stations. The design separates heating, cooling, and loading tasks, reducing idle time between cycles. A steel frame supports the oven, mold arms, drive system, and control cabinet. Each shuttle usually travels on rails or guided wheels. Smooth movement matters. Slight rail misalignment can create vibration, uneven wall thickness, or premature bearing wear. In practical plant checks, operators should inspect wheel contact, stop positions, and cable routing before production begins. The layout also needs clear access for molds, forklift traffic, and maintenance work.

During operation, a hollow mold rotates on two axes inside a controlled oven. Heat softens measured polymer powder, while rotation spreads it across corners and broad surfaces. Core components include geared drives, independent arm motors, temperature sensors, heating units, cooling fans, and a programmable controller. Good controls record oven temperature, rotation speed, dwell time, and cooling duration for repeatable parts. Still, repeatability is not automatic. Powder moisture, mold venting, ambient temperature, and loading errors can change the result. I have seen a small vent blockage leave bubbles near a handle opening. That problem is easy to miss. Maintenance teams should compare cycle data with part measurements, rather than trusting the screen alone. Shuttle machines support varied mold sizes, but oversized tooling may slow transfers and strain the drive system. Design reviews should test those limits honestly.


Key Criteria for Comparing the Top 10 Global Shuttle Machines

Top 10 Shuttle Rotomolding Machines for Global Buyers

Key Criteria for Comparing the Top 10 Global Shuttle Machines

Comparing shuttle rotomolding machines requires more than checking output claims. Start with platen size, mold capacity, shuttle travel, and clamping stability. These factors affect product consistency and floor-space planning. Heating performance matters too. Review burner control, temperature uniformity, cooling airflow, and cycle data from real production trials. A fast cycle is not useful if wall thickness varies. Ask for documented test results, maintenance records, and safety certifications that match your installation country. Reliable suppliers should explain limitations clearly.

Tips: Request a sample cycle using your actual resin and mold. Measure heating time, cooling time, energy use, and part rejection rates. Check whether operators can reach controls safely. Also compare spare-part availability, training, remote support, and technical documentation. Translation quality can matter during urgent repairs. It is an overlooked detail.

A practical comparison should include total ownership cost, not only purchase price. Examine utility requirements, oven insulation, hydraulic wear, automation options, and expected service intervals. Verify the machine’s footprint against doors, cranes, ventilation, and future expansion. Some ranking tables look precise but depend on incomplete factory data. I have seen attractive specifications hide slow changeovers or difficult cleaning access. Leave room for doubt. A factory acceptance test, witnessed remotely or in person, can expose these weaknesses before shipment.

Top 10 Shuttle Rotomolding Machines for Global Buyers

Key criteria for comparing anonymous shuttle machine configurations. Scores are based on a weighted procurement model covering productivity, flexibility, energy use, control capability, and maintenance practicality.

How to read the chart: A higher score indicates a stronger overall fit for global buyers seeking balanced production capacity, process consistency, operating efficiency, and serviceability. The benchmark is configuration-based and does not represent any specific company or brand.

Top 10 Shuttle Rotomolding Machines by Capacity and Performance

Top 10 Shuttle Rotomolding Machines for Global Buyers

Top 10 Shuttle Rotomolding Machines by Capacity and Performance

A useful top-ten ranking must compare capacity, cycle stability, and energy control. Capacity alone can mislead. A large chamber may waste energy on small tanks. Grand View Research valued the global rotational molding market at about USD 5.24 billion in 2023. Its forecast also indicates steady growth through 2030. That growth increases demand for measurable machine performance.

The strongest shortlist includes three compact machines for 50–300-liter parts, four mid-size units for 300–2,000-liter products, and three heavy-duty systems above 2,000 liters. Compact models should offer fast arm movement and accurate temperature feedback. Mid-size machines need balanced airflow across both ovens. Heavy-duty systems require rigid frames, high payload capacity, and reliable hydraulic motion. A practical benchmark is repeatable heating within a few degrees Celsius, not a dramatic brochure claim. Shorter cooling cycles matter too. Every minute saved can improve daily output.

The Plastics Industry Association reports that rotational molding remains valuable for large, hollow products because tooling costs are relatively low. However, operators still need to measure scrap, labor, and electricity. In our technical comparisons, machines with independent shuttle control usually improve scheduling flexibility. This is not always better. Complex controls can increase training time and maintenance risks. Buyers should inspect actual cycle records, oven recovery time, and mold-change procedures. A simple factory trial often reveals more than a polished specification sheet.

Applications, Materials, and Production Needs for Each Machine

Top 10 Shuttle Rotomolding Machines for Global Buyers

Applications, Materials, and Production Needs for Each Machine

Shuttle rotomolding machines serve very different production goals. A compact two-station model suits water tanks, bins, and small drums. It usually runs linear polyethylene with moderate mold weights. A medium shuttle machine handles pallets, coolers, and agricultural containers. These products need stable heating and controlled cooling. For playground parts, choose a wider oven and strong mold access. Complex shapes often require careful venting. Large tanks demand high load capacity, longer heating cycles, and accurate arm movement. Production data matters more than attractive specifications.

Some machines fit thick-walled industrial boxes made from high-density polyethylene. Others support cross-linked polyethylene for demanding tank applications. Cross-linked material offers durability, but recycling becomes more difficult. That trade-off deserves attention. Thin consumer products may need faster indexing and efficient airflow. Medical and laboratory containers require cleanable surfaces, consistent temperature control, and documented process records. For insulated coolers, even heating helps protect wall thickness and lid alignment. A hydraulic shuttle system may suit heavy molds, while servo-assisted motion can improve repeatability. Still, servo features do not automatically improve every product.

High-volume manufacturers may prefer dual-oven shuttle layouts with automated charging and unloading. Smaller factories often benefit from simpler controls and lower maintenance needs. Check oven dimensions, mold clearance, arm payload, cooling capacity, and local electrical compatibility. I would also inspect weld quality, spare-part access, and operator safety systems before purchase. One overlooked issue is factory skill. A sophisticated machine can underperform when process training is weak. Trial production with the actual resin, mold, and cycle target remains the most reliable comparison.

Top 10 Shuttle Rotomolding Machines for Global Buyers - Applications, Materials, and Production Needs for Each Machine
Rank Shuttle Machine Configuration Typical Mold Envelope Typical Load Capacity Heating System and Temperature Range Recommended Materials Typical Applications Production Needs Key Selection Considerations
1
Compact Single-Station Shuttle
Entry-level two-arm layout
Up to 1.2 m × 1.2 m × 1.2 m 100–250 kg per arm Gas-fired or electric hot-air oven; approximately 200–350 °C process capability LLDPE MDPE Cross-linked PE Small tanks, bins, traffic barriers, toys, planters, and compact containers Prototype work, low-to-medium batch production, frequent mold changes, and limited factory floor space Best for low capital cost and flexible tooling; verify oven uniformity and arm indexing accuracy before purchasing
2
Medium Two-Arm Shuttle
Independent shuttle movement
Up to 1.8 m × 1.8 m × 1.6 m 200–450 kg per arm Gas-fired hot-air circulation; typical oven setpoint range of 220–350 °C LLDPE HDPE PP Waste containers, agricultural tanks, playground components, and medium-sized storage products General-purpose production with multiple molds and moderate annual volumes Look for independent arm loading, programmable rotation ratios, and reliable cooling access outside the oven
3
Large-Capacity Shuttle
Heavy-duty dual-carriage design
Up to 2.5 m × 2.5 m × 2.2 m 400–800 kg per arm High-volume gas-fired oven with forced air circulation; approximately 250–350 °C LLDPE HDPE PVC plastisol Large water tanks, septic tanks, industrial containers, road equipment, and agricultural products Medium-to-high output, heavy molds, long heating cycles, and continuous multi-shift operation Foundation strength, carriage rigidity, thermal uniformity, and oven recovery time are critical for large parts
4
Independent-Arm Shuttle
Separate loading, heating, and cooling cycles
Up to 2.0 m × 2.0 m × 1.8 m 250–550 kg per arm Gas or electric hot-air oven with PLC-controlled temperature profiles; approximately 200–350 °C LLDPE HDPE PP PA-based compounds Fuel tanks, coolers, medical containers, returnable logistics boxes, and engineered housings Mixed product schedules requiring reduced idle time and efficient changeover between molds Independent arm control improves scheduling flexibility; confirm safety interlocks and recipe storage capacity
5
High-Productivity Dual-Arm Shuttle
Optimized for parallel cycles
Up to 2.2 m × 2.2 m × 2.0 m 350–700 kg per arm High-efficiency gas oven with variable-speed circulation; approximately 220–350 °C LLDPE HDPE PP Industrial pallets, large bins, refuse containers, sports equipment, and commercial tanks High utilization, repeatable product families, short transfer times, and two- or three-shift manufacturing Prioritize cycle synchronization, fuel efficiency, fast mold exchange, and automated temperature data logging
6
Electric Shuttle Rotomolding Machine
Low-emission oven configuration
Up to 1.6 m × 1.6 m × 1.5 m 150–350 kg per arm Electric resistance or infrared-assisted hot-air heating; approximately 180–350 °C LLDPE HDPE PP EVA Indoor equipment, laboratory products, clean-environment containers, and small technical parts Facilities with strict emissions controls, stable electricity supply, and moderate production volumes Compare installed electrical power, heat-up time, insulation quality, and local energy tariffs
7
Gas-Fired Industrial Shuttle
High thermal-output configuration
Up to 2.8 m × 2.8 m × 2.4 m 500–1,000 kg per arm Direct or indirect gas-fired hot-air oven; generally operated around 230–350 °C LLDPE HDPE PVC plastisol Large tanks, marine products, heavy-duty bins, industrial ducting, and infrastructure components Large-part production, high material throughput, extended cycles, and high daily machine utilization Check burner modulation, ventilation requirements, combustion safety, heat distribution, and local gas regulations
8
Precision-Control Shuttle
Advanced process-monitoring package
Up to 1.8 m × 1.8 m × 1.6 m 200–500 kg per arm Closed-loop hot-air control with multiple temperature zones; approximately 200–350 °C LLDPE HDPE PP PA compounds Automotive ducts, protective covers, technical housings, sealed enclosures, and medical-use components Applications requiring controlled wall thickness, repeatable cycle records, and traceable quality data Evaluate thermocouple placement, data logging, recipe control, alarm functions, and rotation repeatability
9
Modular Multi-Mold Shuttle
Flexible tooling and carriage arrangement
Up to 2.0 m × 2.0 m × 1.8 m 250–600 kg per arm Gas or electric hot-air heating; approximately 200–350 °C LLDPE HDPE PP EVA Consumer products, furniture parts, containers, kayaks, toys, and seasonal products Contract manufacturing, short runs, frequent tooling changes, and diverse product portfolios Confirm arm mounting patterns, mold clearance, quick-connect utilities, and tooling changeover procedures
10
Heavy-Duty Custom Shuttle
Engineered for oversized or specialized products
More than 3.0 m × 3.0 m × 2.5 m, subject to engineering design 700–1,500 kg per arm High-capacity gas-fired or hybrid heating system; approximately 250–350 °C LLDPE HDPE PVC plastisol Specialty compounds Large marine tanks, industrial vessels, oversized agricultural tanks, water-treatment components, and custom infrastructure parts High-value large-part production, long cycle times, heavy tooling, and dedicated production cells Require a complete engineering review covering building height, foundation load, oven access, ventilation, utilities, and material-handling systems
Performance ranges are typical planning values for shuttle rotomolding equipment. Actual capacity, mold envelope, cycle time, energy consumption, and material compatibility depend on machine design, mold construction, part geometry, powder loading, and process conditions.

Global Buying Factors: Safety, Service, Cost, and Customization

Top 10 Shuttle Rotomolding Machines for Global Buyers

Global Buying Factors: Safety, Service, Cost, and Customization

When comparing the top ten shuttle rotomolding machines, safety should guide every decision. I have inspected production lines where emergency stops were difficult to reach. That small detail created serious delays during testing. Look for guarded heating areas, stable rail movement, clear controls, and reliable temperature alarms. Operators should receive practical training, not only a manual translated into several languages. Safety records, factory testing, and documented maintenance procedures offer stronger evidence than attractive photographs.

Service can protect production more effectively than a low purchase price. Ask about spare-part availability, remote troubleshooting, technician response times, and installation support. A machine may be affordable, yet expensive downtime can quickly change the calculation. Request a complete cost sheet covering energy use, tooling changes, calibration, shipping, and operator training. Hidden costs matter. Currency changes and local electrical standards also deserve attention.

Customization should match the product, not follow fashion. Review mold dimensions, carriage capacity, arm configuration, cooling needs, and control-system flexibility. Experienced suppliers should explain why each option is necessary. I once saw a buyer choose extra capacity that was rarely used. It looked impressive, but occupied valuable floor space. That decision still needed reconsideration. Factory acceptance tests, sample production, and measurable performance targets make global purchasing more dependable. Some buyers also overlook after-sales communication. Clear technical drawings and realistic delivery dates often reveal more than a polished sales presentation.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
