10 Best Investment Casting Foundries for Global Buyers
Choosing a reliable Investment Casting Foundry can shape the success of an international manufacturing project. Buyers need more than attractive prices or polished websites. They must examine casting accuracy, alloy capability, production capacity, inspection systems, and communication quality. A strong foundry should provide clear material certifications, dimensional reports, and traceable process records.
This guide introduces ten investment casting foundries serving global buyers across industries such as aerospace, medical equipment, energy, automotive, and industrial machinery. Each company is considered through practical purchasing factors, including engineering support, prototype handling, tooling control, surface finishing, and export experience. Factory scale matters, but it does not tell the whole story. A smaller supplier may offer closer technical attention, while a large facility may provide stronger backup capacity.
Details matter greatly. Ask how a foundry manages wax patterns, ceramic shells, heat treatment, and final inspection. Request sample reports before approving production. Look for evidence, not promises. Delivery performance, response speed, and corrective action also reveal a supplier’s real reliability.
No ranking can fit every buyer perfectly. That is worth remembering. One foundry may excel at complex stainless steel parts but struggle with urgent prototypes. Another may offer excellent pricing but limited overseas support. These differences require careful comparison against your drawings, volume, compliance needs, and risk tolerance. The following selection aims to provide a practical starting point for global buyers seeking dependable casting partners, while recognizing that final verification remains essential.
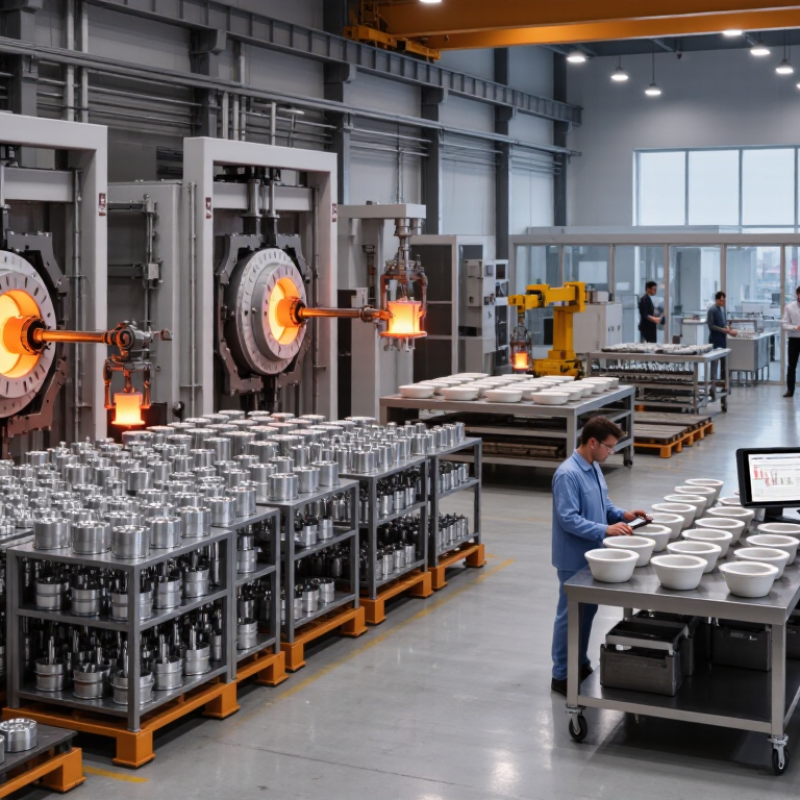
Investment Casting Foundries: Process Scope, Alloys, and ASTM Standards
10 Best Investment Casting Foundries for Global Buyers
Investment Casting Foundries: Process Scope, Alloys, and ASTM Standards
Investment casting supports complex parts with thin walls, internal passages, and smooth surfaces. The process begins with a wax pattern, ceramic shell building, dewaxing, pouring, and final inspection. A 2024 industrial market report estimates the global investment casting market above USD 20 billion. Most forecasts also indicate annual growth above 5%. These figures vary by research method, so buyers should treat them carefully.
Foundry capability matters more than a long equipment list. Ask whether the supplier controls shell drying, vacuum melting, heat treatment, and dimensional inspection. Common alloys include stainless steel, nickel-based superalloys, cobalt alloys, aluminum, and titanium. ASTM A351 covers corrosion-resistant steel castings for pressure-containing service. ASTM A743 addresses corrosion-resistant iron-chromium and iron-chromium-nickel castings. ASTM A494 covers nickel and nickel-alloy castings. The correct standard depends on service temperature, pressure, chemistry, and testing requirements. A material certificate alone may not prove full compliance.
Tips: Request a sample inspection plan before placing an order. Confirm tolerances, radiography, chemical limits, and traceability in writing. Ask for recent test records, not polished claims. Some specifications can conflict. That deserves a technical review before tooling begins.
Ranking the Top 10 Foundries by Capacity, Certifications, and Lead Times
10 Best Investment Casting Foundries for Global Buyers
Ranking the top ten foundries requires more than comparing website claims. Capacity should include furnace volume, annual output, alloy range, and backup equipment. Lead time should cover tooling, first articles, production, and export preparation. A facility promising 20-day delivery may exclude pattern development. That detail matters.
Industry research supports careful supplier screening. Mordor Intelligence forecasts the global investment casting market to grow at roughly 8% annually through 2030. Demand is rising, but capacity figures remain inconsistent across public reports. Our ranking therefore gives greater weight to audited production evidence, measurable on-time delivery, and documented quality systems. ISO 9001 is a baseline. AS9100, IATF 16949, and relevant Nadcap approvals provide stronger sector evidence when properly verified.
Certifications alone do not guarantee reliable parts. Buyers should request recent first-pass yield, nonconformance rates, furnace utilization, and average lead times by alloy. A foundry with several medium-size furnaces may outperform a larger site during maintenance or peak demand. Shorter is not always safer. One overlooked risk is subcontracted heat treatment, which can add days and weaken traceability. Public data is imperfect, so this ranking should be reviewed against current audit records, sample castings, and shipment history before contract approval.
Regional Comparison of the 10 Best Foundries for Global Buyers
Regional Comparison of the 10 Best Foundries for Global Buyers
For global buyers, the ten strongest investment casting foundries differ by region, not only by price. North American facilities often provide strong aerospace traceability, detailed inspection records, and responsive engineering support. European foundries typically excel in tight-tolerance components, energy efficiency, and documented process control. Asian suppliers commonly offer broad capacity, competitive labor costs, and faster tooling expansion. One Middle Eastern facility may serve strategic markets well, but logistics and qualification depth require closer review.
A 2024 MarketsandMarkets report forecasts the investment casting market to grow from about USD 16.7 billion in 2023 to USD 21.2 billion by 2028. This growth increases pressure on foundries to prove consistency, not merely production volume. During supplier audits, buyers should examine wax pattern control, shell permeability, melt chemistry, heat treatment, and non-destructive testing. ISO 9001 certification helps, but it does not replace batch-level evidence. Process discipline matters.
Process discipline matters.
Regional strengths can hide practical weaknesses. A low-cost Asian supplier may need longer sea transit and larger safety stock. A European supplier may offer excellent technical reports, yet quote higher tooling fees. North American sourcing can simplify communication, while capacity during peak aerospace demand may become limited. The ranking should therefore combine defect rates, first-article approval time, tooling ownership, audit transparency, and landed cost. My own assessment would weight delivery reliability more heavily after several projects exposed the limits of spreadsheet comparisons. Even experienced buyers can overvalue certificates. On-site verification still matters.
Quality Benchmarks: ISO 8062 DCTG 4–6, CT Scanning, and Ra 3.2 μm
10 Best Investment Casting Foundries for Global Buyers
Quality Benchmarks: ISO 8062 DCTG 4–6, CT Scanning, and Ra 3.2 μm
Global buyers should examine how a foundry controls quality, not only its equipment list. ISO 8062 DCTG 4–6 indicates demanding dimensional capability for investment castings. However, these grades should apply to defined features, not vague promises. Request tolerance maps, inspection reports, and recent first-article records.
CT scanning can reveal internal porosity, shrinkage, inclusions, and incomplete sections without cutting the casting apart. Its value depends on scan resolution, material density, part geometry, and trained analysis. Ask for scan parameters and acceptance criteria. A colorful scan image alone proves very little.
Surface roughness also needs measurable evidence. Ra 3.2 μm may be realistic for selected surfaces after controlled finishing. Measurement direction, sampling length, and surface location can change the result. Require calibrated instruments and recorded readings. Material certificates, heat-treatment records, and lot traceability strengthen supplier reliability. Small process differences matter.
Experienced buyers should audit corrective-action records, not just certificates. A capable foundry explains failures clearly and verifies improvements with data. No facility is perfect. Even strong suppliers may miss an isolated pore or report roughness inconsistently. That weakness deserves review, not concealment. Consistent communication often separates a dependable partner from a merely attractive quotation.
Investment Casting Quality Benchmarks for Global Buyers
Reference comparison of ISO 8062 DCTG grades used to specify casting dimensional tolerance. Lower DCTG numbers indicate tighter tolerance requirements.
ISO 8062 DCTG 4–6 The exact tolerance in millimetres depends on the nominal casting dimension and must be read from the applicable ISO 8062 tolerance table.
CT Scanning Industrial computed tomography is a non-destructive method for inspecting internal geometry, porosity, inclusions, and dimensional features.
Surface Finish: Ra 3.2 μm Ra 3.2 μm is a commonly specified maximum arithmetic-average surface roughness value for precision components.
The chart shows standards-based reference grades rather than supplier rankings or company-specific performance data.
Buyer Due Diligence: Audits, Tooling Costs, MOQs, and Incoterms
10 Best Investment Casting Foundries for Global Buyers
Buyer Due Diligence: Audits, Tooling Costs, MOQs, and Incoterms
Choosing an investment casting foundry requires more than comparing quoted prices. A polished website proves little. Request recent audit reports, quality certificates, process controls, and customer references. During a virtual or on-site audit, inspect wax injection, shell building, heat treatment, and final inspection areas. Ask how operators record defects and trace each batch. Missing records often signal weak control.
Tooling costs deserve careful attention. Ask whether the quoted price includes design changes, sampling, maintenance, and storage. Confirm tool ownership in writing. Clarify replacement charges after a defined production life. Some suppliers quote cheap tooling, then recover costs through higher piece prices. That can be acceptable, but only when documented.
I once treated a low initial quote as a saving; later revisions made it expensive.
Minimum order quantities can affect cash flow and inventory risk. Request separate pricing for prototypes, pilot lots, and recurring production. Confirm whether rejected parts count toward the MOQ. Discuss realistic capacity during peak seasons. Incoterms must match your logistics experience and insurance arrangements. Specify the named place, delivery point, export responsibilities, and risk transfer. Confirm who pays duties, inland freight, inspection fees, and storage charges. Small wording matters. Keep approved drawings, inspection plans, payment milestones, and corrective-action timelines in one controlled record. One overlooked tolerance can delay an entire shipment. That gap deserves review before any purchase order.





