


Selecting reliable China Best Hydraulic Pressure Comparator Manufacturers requires more than comparing prices or polished product pages. A Hydraulic Pressure Comparator must create stable pressure, maintain calibration, and produce traceable results under demanding laboratory conditions. In practice, a technician may connect a hand pump, read a reference gauge, and verify readings across several pressure points. Small leaks can distort the entire test.
Industry reports support this growing need for dependable calibration equipment. Grand View Research’s hydraulic equipment market analysis identifies continued demand for precision control, industrial automation, and maintenance efficiency. MarketsandMarkets’ pressure sensor market research also highlights rising requirements for accurate pressure measurement across manufacturing, energy, transportation, and process industries. These trends matter to buyers selecting Chinese suppliers. Market growth alone does not prove manufacturing quality.
Evidence matters more.
A credible manufacturer should explain its pressure range, accuracy class, medium compatibility, connection design, stabilization time, and calibration process. ISO 17025-related calibration practices are especially relevant when test results must remain traceable and auditable. Buyers should also request sample calibration certificates, factory inspection records, material information, and realistic delivery terms. Certifications deserve verification, not blind trust.
Some suppliers offer attractive specifications, yet omit long-term drift data or repeatability results. That gap should prompt careful questions. A useful comparison should examine engineering experience, production controls, after-sales support, and application knowledge. It should also recognize that no single comparator fits every laboratory. Hydraulic oil, water, temperature changes, and operator technique can affect performance. The best manufacturers combine verified technical capability with transparent communication, practical customization, and dependable service after installation. Mistakes still happen. Good suppliers show how they prevent them.
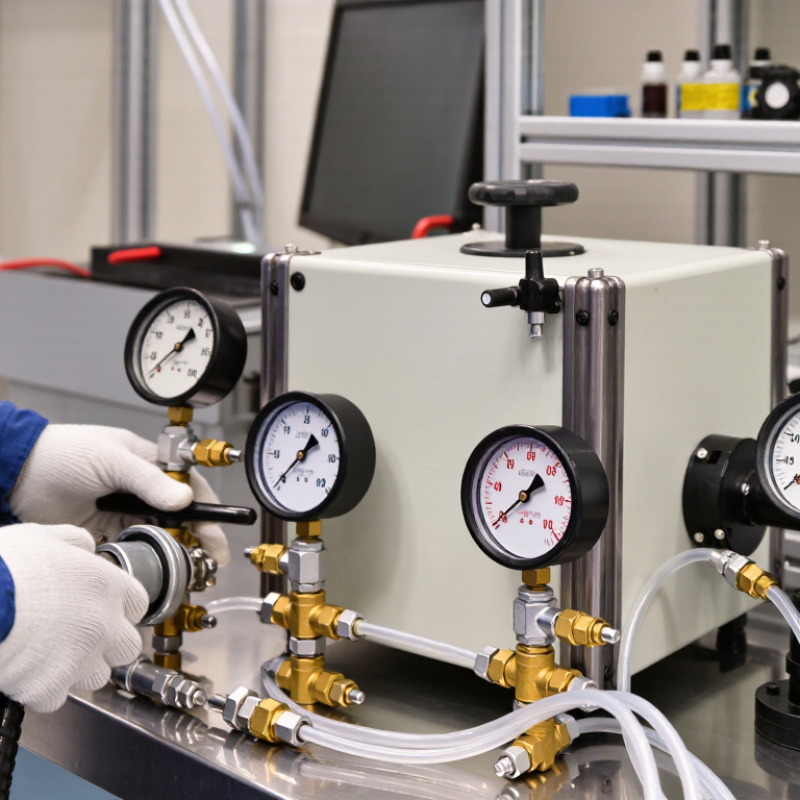
A hydraulic pressure comparator is a laboratory instrument for comparing an unknown pressure gauge with a trusted reference. It uses liquid pressure to create a controlled, nearly equal force on both instruments. A typical unit includes a hand pump, fine adjustment valve, reservoir, test ports, and a calibrated reference gauge.
During calibration, the operator fills the system with compatible hydraulic fluid and removes trapped air. The hand pump raises pressure gradually, while the fine adjustment mechanism stabilizes the reading. Both gauges should settle before measurements are recorded. Small leaks, temperature changes, or poor sealing can affect results. They matter more than many beginners expect.
In practical workshops, technicians use hydraulic comparators to check pressure gauges, transmitters, and test instruments. The reference gauge must have suitable accuracy and a current calibration certificate. Thread standards, pressure range, fluid compatibility, and port arrangement also require careful inspection. A higher maximum pressure does not always mean better performance. It may reduce sensitivity at lower points.
Reliable manufacturers should provide pressure stability data, operating instructions, material details, and traceable calibration support. However, printed specifications are not enough. I would inspect the adjustment response and repeatability under real working conditions. Some comparison units feel precise but respond slowly. That weakness can disturb testing schedules. Good practice includes regular cleaning, leak checks, and documented measurement records. Mistakes still happen, especially when air remains in the circuit.

A hydraulic pressure comparator generates and compares a known reference pressure with the pressure indicated by a device under test. The chart shows equivalent pressure values at common calibration points. The conversions are based on 1 bar = 100 kPa = 0.1 MPa = 14.5038 psi.
A hydraulic pressure comparator generates pressure in a sealed liquid circuit. A hand pump moves the fluid through connected lines. The test instrument and reference instrument share the same pressure.
Pascal’s law explains the process. Pressure applied to a confined liquid acts throughout the liquid. The operator raises pressure slowly, then closes the isolation valve. Both instruments should stabilize before readings are recorded. The BIPM SI Brochure, 9th edition, defines one pascal as one newton per square metre. Therefore, 1 MPa equals 1,000,000 Pa. Small details matter. Trapped air can compress and distort results.
During calibration, the operator compares readings at several pressure points. Increasing and decreasing pressure can reveal hysteresis. Temperature changes may also shift the reference reading. NIST Technical Note 1297 identifies repeatability, resolution, hysteresis, temperature, and reference uncertainty as important budget components. ISO/IEC 17025:2017 also requires laboratories to evaluate measurement uncertainty. A practical record should include fluid type, stabilization time, ambient temperature, and observed readings. In bench work, rushing this stage is a common weakness. The comparator may appear stable, yet the fluid still moves slightly. That deserves a second check. Reported accuracy is not always real uncertainty. Calibration quality depends on the method, the reference standard, and disciplined observation.
China manufactures several hydraulic pressure comparator types for laboratories, workshops, and field calibration. Hand-operated hydraulic comparators use a screw pump, reservoir, and test manifold. They suit pressures commonly found in hydraulic equipment, where technicians need stable pressure generation beside a machine. Compact models often include glycerin-compatible wetted parts and a dual-port connection for comparing a reference gauge with a test gauge.
Deadweight piston comparators provide stronger metrological control. They create pressure through calibrated masses and a piston-cylinder assembly. Chinese manufacturers also produce digital hydraulic calibrators with an integrated pump, pressure sensor, display, and data-recording function. These units are faster to use, but their accuracy depends on sensor drift, temperature control, and proper venting. A small air bubble can visibly disturb the reading. The boundary between a comparator and a complete calibrator is not always clear.
The broader pressure-sensor market illustrates rising demand for dependable measurement equipment. MarketsandMarkets estimated the global pressure-sensor market at about USD 14.1 billion in 2024, with projected growth to USD 18.6 billion by 2029. This figure does not measure hydraulic comparators directly, but it reflects expanding calibration needs. Buyers should check pressure range, generation stability, leak resistance, and traceability to national standards. ISO/IEC 17025-based calibration records add credibility, although documentation alone cannot correct poor installation or careless operation.
How to Evaluate China’s Hydraulic Pressure Comparator Manufacturers?
Evaluate technical evidence, not polished catalog language. Ask for calibration records, pressure-range data, stability results, and repeatability tests. ISO/IEC 17025:2017 emphasizes laboratory competence, impartiality, and consistent measurement processes. A serious manufacturer should explain its traceability chain clearly. The certificate should identify standards, uncertainty, environmental conditions, and calibration dates. Missing details matter.
Check performance across the working range. A comparator that performs well at full scale may drift at low pressure. Request test points near 20%, 50%, and 100% of capacity. NIST Technical Note 1297 states that significant uncertainty components must be evaluated and combined correctly. Compare uncertainty in practical units, not only percentages. Inspect the hand pump, valves, seals, and reference gauge connections. Small leaks become obvious during a thirty-minute hold test.
Production control needs physical proof. Review incoming-material checks, assembly records, software controls, and final inspection samples. ISO’s industry survey data shows ISO 9001 certification is widespread worldwide, but certification alone does not prove instrument accuracy. Ask for recent audit findings or corrective-action examples. This feels uncomfortable, yet it reveals maturity. Also evaluate response time, spare-seal availability, training, and technical English. A factory visit helps, although photographs can mislead. My imperfect rule is simple: trust repeatable records more than confident promises.
The best Chinese hydraulic pressure comparator manufacturer proves capability through measurable performance, not attractive brochures. According to the 2023 ISO Survey, more than one million ISO 9001 certificates existed worldwide. Certification helps, but it does not prove pressure-measurement competence. Buyers should request test records for stability, repeatability, leakage, and piston-cylinder performance.
A reliable manufacturer should provide traceable calibration certificates with pressure range, uncertainty, environmental conditions, and adjustment history. ISO/IEC 17025 principles matter here. The laboratory should identify uncertainty sources, control equipment, and protect calibration records. NIST Technical Note 1297 also emphasizes combining uncertainty components before reporting measurement results. This detail is easy to overlook. It should not be.
Practical experience reveals more than specifications. Check whether the comparator maintains pressure after fifteen or thirty minutes. Ask for data from low, middle, and high points. Examine the hand pump, valves, seals, and reading stability under repeated loading. Materials should suit the working medium, especially when oil, water, or aggressive fluids are involved. A manufacturer with documented factory testing, spare-part control, operator training, and responsive technical service is safer for long-term use. I would still question perfect-looking data. Real instruments show small deviations. Honest suppliers explain them, record them, and improve the design.
| Evaluation Dimension | Practical Benchmark for a High-Quality Manufacturer | Why It Matters | Evidence to Request |
|---|---|---|---|
| Pressure Range | A clearly specified working range, such as 0–60 MPa, 0–100 MPa, or another range matched to the application; the manufacturer should state whether the range is gauge, absolute, or differential pressure. | The comparator must safely cover the instruments under test without operating continuously at its maximum limit. | Technical datasheet, pressure-range diagram, working-medium specification, and rated-pressure information for every connection. |
| Generation and Fine Adjustment | A stable hydraulic pump combined with a fine-adjustment volume control or screw press that enables smooth pressure increase, decrease, and balancing. | Fine control reduces overshoot and makes it easier to obtain repeatable calibration points. | Pressure-stabilization procedure, adjustment resolution, leakage test results, and demonstration at low, mid, and high pressure points. |
| Accuracy and Measurement Uncertainty | Accuracy should be stated as a percentage of reading, percentage of full scale, or measurement uncertainty; the method and reference conditions must be clearly defined. | A numerical accuracy claim is meaningful only when its reference basis, temperature, pressure medium, and calibration method are known. | Calibration certificate, uncertainty budget, stated reference conditions, and traceability documentation. |
| Reference Instrument Compatibility | Support for the required reference gauge, digital pressure indicator, or pressure transducer, with suitable connection sizes and adapters. | The reference device determines the practical calibration capability of the complete system. | Connection drawings, thread standards, sealing details, adapter list, and reference-device installation instructions. |
| Stability and Leakage Control | Low pressure drift during a defined holding period, leak-tested hydraulic circuits, and durable seals compatible with the specified working fluid. | Pressure drift can create false readings and reduce repeatability during calibration. | Pressure-hold test records, leakage inspection procedure, seal material information, and recommended maintenance intervals. |
| Working Medium and Compatibility | Explicit identification of the approved medium, such as compatible hydraulic oil or distilled water, together with limitations for different instruments. | Incorrect fluid selection may damage seals, contaminate instruments, or create safety risks. | Fluid compatibility chart, safety data, cleaning procedure, and instructions for switching between fluids. |
| Materials and Construction | Pressure-bearing parts manufactured from suitable corrosion-resistant or high-strength materials, with a rigid base and protected adjustment mechanism. | Rigid construction improves alignment, operating safety, and long-term repeatability. | Material specifications, pressure-part drawings, surface-treatment details, and production quality records. |
| Safety Design | Clearly marked maximum allowable pressure, secure fittings, pressure-relief provisions where applicable, protective layout, and documented operating instructions. | Hydraulic energy can cause injury or equipment damage if connections or pressure limits are exceeded. | Risk assessment, safety instructions, pressure-test records, relief-device specifications, and operator training materials. |
| Calibration Traceability | Calibration results traceable to national or international measurement standards, preferably supported by an appropriately accredited laboratory. | Traceability allows calibration results to be recognized and compared across laboratories and locations. | Certificate sample, laboratory accreditation scope, reference-standard certificates, and calibration interval recommendation. |
| Manufacturing Quality System | Documented inspection and process controls covering incoming materials, machining, assembly, pressure testing, final inspection, and nonconforming products. | A controlled manufacturing process is more reliable than relying only on final visual inspection. | Quality-system certificate, inspection plan, factory acceptance checklist, and sample test records. |
| Customization Capability | Ability to configure pressure range, mounting layout, connection threads, working medium, reference instruments, adapters, and language-specific documentation. | Different industries and national standards often require different connections and test configurations. | Approved drawings, configuration checklist, engineering-change procedure, and pre-production sample approval process. |
| Documentation Quality | Complete manuals containing specifications, setup, venting, operation, calibration workflow, troubleshooting, maintenance, and spare-part information. | Clear documentation reduces setup errors and supports consistent work by different operators. | Manual sample, dimensional drawings, spare-parts list, inspection forms, and multilingual documentation capability. |
| After-Sales Support | Defined warranty terms, technical response process, replacement-seal availability, repair guidance, and support for recalibration or field troubleshooting. | Lifecycle support affects total ownership cost and minimizes downtime. | Warranty conditions, service-level commitments, spare-parts lead times, and escalation contacts. |
| Export and Compliance Readiness | Accurate product labeling, export packaging, commercial documentation, applicable conformity information, and packaging suitable for international transport. | Proper documentation and packaging reduce customs delays and transport-related damage. | Packing specification, product label sample, export documents, conformity declarations where applicable, and shipment inspection records. |
| Total Cost of Ownership | Evaluation based on purchase price, reference instrument, adapters, calibration, consumables, maintenance, training, shipping, and expected service life. | The lowest initial price does not necessarily provide the lowest operating cost or best measurement reliability. | Itemized quotation, recommended spare-parts list, calibration cost, maintenance schedule, and estimated annual operating cost. |
Selection should be based on verified technical documentation, pressure-test records, calibration traceability, application compatibility, and lifecycle support rather than price or marketing claims alone.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

