


Gr5 Titanium Tube is valued for its high strength-to-weight ratio, corrosion resistance, and performance in demanding environments. It commonly refers to Ti-6Al-4V, a titanium alloy used in aerospace, chemical processing, energy, and other engineered applications. Boeing’s 2024 Commercial Market Outlook projects demand for 43,975 new commercial airplanes between 2024 and 2043. That forecast signals continuing pressure on aerospace supply chains, though it does not measure titanium-tube demand directly.
For buyers, a manufacturer’s name is only a starting point. Material traceability, dimensional consistency, heat-treatment control, and documentation can matter as much as price. ASTM B861 covers seamless titanium and titanium-alloy pipe, while ASTM B862 addresses welded pipe; buyers should check the applicable specification and product form rather than assume every tube meets the same requirements. That distinction matters. A polished catalog cannot prove batch quality, and published capabilities may not reflect current production capacity.
This overview examines leading Gr5 Titanium Tube manufacturers worldwide through practical criteria: manufacturing scope, quality systems, export experience, and application fit. USGS mineral-commodity reporting offers useful context on titanium feedstocks, but it cannot rank finished-tube suppliers. A limitation worth keeping in view. Supplier data can change, and public claims are not always independently verified. Readers should confirm certifications, mill test reports, tolerances, and delivery terms directly before making a sourcing decision.
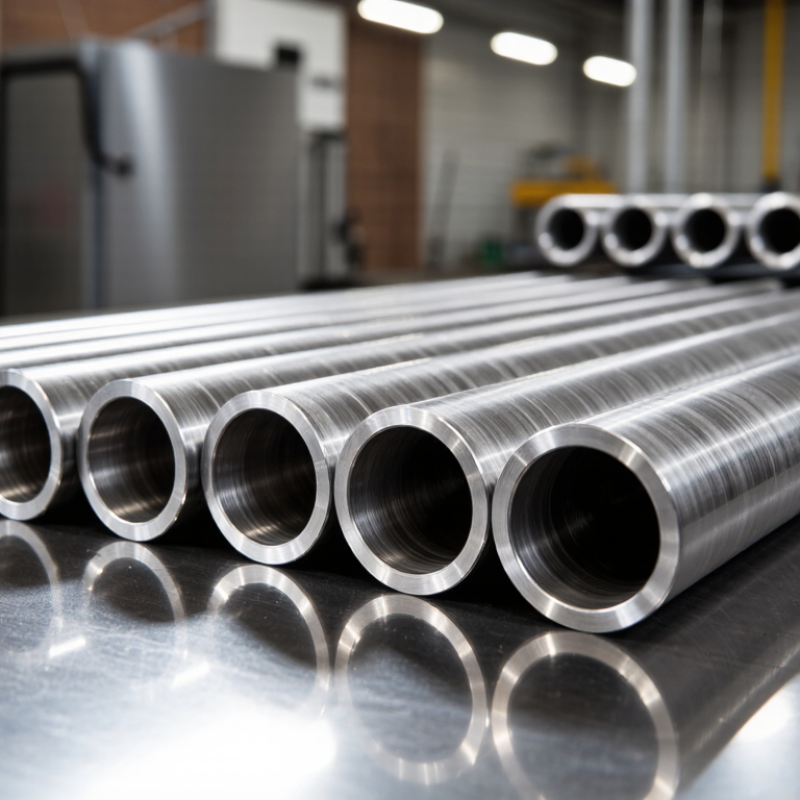
Grade 5 titanium tube is made from Ti-6Al-4V, an alloy containing titanium, aluminum, and vanadium. Typical specifications call for 5.5–6.75% aluminum and 3.5–4.5% vanadium, with titanium forming the balance. Exact limits depend on the applicable material standard. Small numbers matter. They affect how a tube is specified and verified.
Its density is approximately 4.43 g/cm³, giving it a low mass for its size compared with many steels. For design teams, this can help reduce component weight without making the tube feel flimsy in the hand. Grade 5 also offers a useful balance of strength and corrosion resistance. Yet density alone cannot predict performance; wall thickness, heat treatment, and service conditions matter too.
When evaluating tubing, check the certified chemistry, dimensions, and mechanical test results against the intended specification. A clean cut end and consistent wall thickness are useful visual checks, but they do not replace documentation. One detail is easy to overlook: processing history can influence properties, even when the alloy name is unchanged. A datasheet looks reassuring, though real service conditions may expose gaps in the design assumptions.

ASTM B338 covers seamless and welded titanium tubes for heat exchangers and condensers; ASME SB-338 carries the specification into the ASME Boiler and Pressure Vessel Code. For Grade 5, Ti-6Al-4V, buyers should confirm the required grade, tube dimensions, delivery condition, and applicable standard edition before ordering. Small details matter.
ASTM B338’s Grade 5 mechanical-property requirements commonly specify minimum tensile strength of 895 MPa, yield strength of 828 MPa, and elongation of 10%, subject to the applicable product dimensions and condition. The standard also addresses chemical analysis, tensile testing, and specified examinations, which can include hydrostatic or nondestructive electric testing. These figures are not a substitute for checking the governing edition and purchase order. A certificate should identify the heat, grade, test results, and inspection status.
For manufacturer comparisons, request traceable mill test reports and confirm that the tube marking matches the documents. Check weld-seam controls for welded tubing, plus dimensional records for outside diameter and wall thickness. A polished certificate can still leave gaps: verify whether required tests apply to each tube or a sampling lot. That question is easy to miss. cite: ASTM B338 and ASME BPVC Section II, Part B, SB-338.
| Evaluation Dimension | Relevant Fact or Requirement | What to Verify with a Manufacturer |
|---|---|---|
| Grade 5 material identity | Grade 5 titanium alloy is commonly identified as Ti-6Al-4V and UNS R56400. Its specified chemistry and properties should be confirmed against the applicable material specification and edition. | Check that the quotation, purchase order, tube marking, and material test report all identify the same grade and UNS number. |
| ASTM B338 scope | ASTM B338 covers seamless and welded titanium and titanium-alloy tubes intended for condensers and heat exchangers. The grade list and requirements depend on the edition in force. | Request confirmation that the exact grade, product form, dimensions, and intended application are covered by the specified B338 edition. Do not assume Grade 5 coverage without checking that edition. |
| ASME SB-338 | SB-338 is the ASME Boiler and Pressure Vessel Code material specification corresponding to ASTM B338. Code projects may require a particular edition and applicable code rules. | State the required ASME BPVC edition in the inquiry and verify that the supplier’s documentation supports the specified code and material designation. |
| Product form | B338 distinguishes between seamless and welded tube products; the permitted form and relevant requirements must match the order. | Specify seamless or welded construction and request traceable documentation identifying the supplied manufacturing route. |
| Dimensions and tolerances | Tube outside diameter, wall thickness, length, and applicable tolerances are order-critical and must be checked against the selected specification edition and purchase requirements. | Confirm the dimensional schedule, tolerance basis, straightness, end finish, and inspection method before production. |
| Chemistry and mechanical properties | Acceptance limits are grade- and edition-specific; values should be taken from the controlling specification rather than inferred from a generic Grade 5 data sheet. | Review test results against the exact ordered grade and specification. Confirm the required tests, sampling frequency, and acceptance criteria in writing. |
| Inspection and testing | Applicable examination and testing depend on the specification, product form, dimensions, and purchase order. Additional project testing may also be required. | Agree on required examinations, test methods, acceptance criteria, inspection stages, and any third-party witness or hold points before manufacture. |
| Documentation and traceability | For regulated or critical applications, material identification and traceability through production and testing are important purchasing controls. | Request a material test report linked to the delivered tubes, heat or lot identification, inspection records, and any required certificate of conformity. |
| Manufacturing capability | Capability varies by producer; available sizes, lengths, product forms, finishing operations, and inspection resources should not be presumed from a general catalogue. | Evaluate documented capacity for the requested Grade 5 specification, dimensions, quantity, delivery schedule, and quality requirements. |
| Application suitability | Grade 5 is an alpha-beta alloy used where its strength characteristics are relevant; suitability for a heat-exchanger or pressure-boundary service depends on design conditions and applicable code requirements. | Have the design authority confirm alloy, corrosion environment, temperature, joining method, and code acceptability before ordering. |
Purchasing note: Specify the governing ASTM or ASME edition, grade, product form, dimensions, testing, inspection, and documentation requirements on the purchase order. Confirm Grade 5 inclusion and applicability against the edition and project code requirements before placing an order.
For Grade 5 titanium tube, 895 MPa is a threshold, not a guarantee of identical performance in every finished part. ASTM B338/B338M specifies a minimum tensile strength of 895 MPa for Grade 5 tube, alongside minimum yield strength of 828 MPa and minimum elongation of 10%, subject to the applicable product requirements. ASTM E8/E8M provides the tensile-test method for metallic materials. The number matters. But it does not state a tube’s pressure capacity or fatigue life. Wall thickness, heat treatment, specimen direction, and sampling can all affect the result.
When comparing manufacturers worldwide, ask for heat- and lot-linked test certificates, not just a headline strength figure. Check that the reported test method, tube condition, dimensions, and chemistry match the purchase specification. A measured result comfortably above 895 MPa may offer useful margin, but it cannot replace design checks for temperature, cyclic loading, or joining. I would not treat the minimum as a shortcut. Even a polished certificate can leave questions about sampling and production consistency, so traceability and repeatable test records deserve close review.
Minimum tensile and yield strength benchmarks for Grade 5 (Ti-6Al-4V), shown in MPa.
These are commonly cited minimum values for annealed Grade 5 titanium. Requirements may vary by product form and governing specification; confirm the applicable tube standard.
Worldwide Grade 5 tube capability depends on more than installed capacity. Buyers should check whether a producer controls melting, billet preparation, tube forming, heat treatment, and final inspection. Grade 5 titanium, commonly Ti-6Al-4V, needs careful temperature control; small process changes can affect strength and dimensional consistency. Seamless and welded routes serve different applications, so compare the production method with the required wall thickness, diameter, and service conditions.
The USGS Mineral Commodity Summaries 2024 estimated global titanium sponge production at 330,000 metric tons in 2023, including 210,000 metric tons in China. Sponge is an upstream material, not finished tube, and these figures do not measure tube-making capacity. Still, they show why regional supply chains matter. When assessing manufacturers worldwide, ask for mill test certificates, heat-treatment records, non-destructive testing procedures, and evidence of lot traceability. Published capacity figures can be hard to compare; actual delivery consistency deserves equal attention.
Tips: Request sample inspection data and confirm tolerances before placing an order. Check how the supplier handles thin-wall tubing, where ovality or surface marks may be easier to miss. A production claim alone is not proof.
Top Gr5 Titanium Tube Manufacturers Worldwide
Comparing Grade 5 titanium tube suppliers takes more than checking price and availability. Start with the product specification and confirm which tests apply to the tube’s form, dimensions, and intended use. Review chemical composition, tensile results, dimensional checks, and any specified nondestructive testing. Ask for sample reports tied to the actual production lot, not just a generic example. Small details matter.
Traceability should connect each tube or bundle to its heat or lot number. Check that markings, packing lists, and material test reports agree. Then verify the report’s measured values against the purchase requirements. A mismatch may be a clerical error, but it still deserves clarification before acceptance. Supplier certifications also need context: confirm the issuing body, validity, and scope, and check whether the certified processes cover the work being purchased. A certificate alone does not prove that every tube meets your requirements.
Tips: Request a redacted report from a recent shipment and follow one tube’s identification through the records. Keep questions specific: Which test standard was used? Who performed the inspection? What happens if results fall outside limits? Some paperwork can look complete while leaving gaps, so allow time to review it carefully.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

