


Choosing among the top aluminum furnace manufacturers requires more than comparing price, capacity, or brand visibility. A furnace may look impressive in a brochure, yet perform poorly beside a busy casting line. Operators notice the difference through uneven melt temperatures, excessive dross, slow recovery, and unexpected maintenance stops.
George E. Totten, a respected authority in aluminum heat treatment, stated, “Process control is the foundation of consistent heat treatment.” This principle also matters when evaluating an aluminum furnace. Reliable manufacturers combine accurate temperature sensors, stable combustion or electric heating, strong insulation, and responsive control systems. They also design equipment around the customer’s alloy, batch size, production rhythm, and safety requirements.
The strongest suppliers usually offer melting, holding, heat-treatment, and atmosphere-control solutions. Some focus on high-volume foundries. Others serve smaller operations that need flexible chamber furnaces. The right choice depends on actual working conditions, not marketing language. Energy consumption matters, but it should be measured beside cycle time, metal loss, service access, and operating labor.
This guide examines leading aluminum furnace manufacturers through those practical factors. It considers technology, customization, efficiency, installation support, and long-term reliability. Company rankings are never completely objective. A manufacturer leading in aerospace heat treatment may not suit a die-casting workshop. That distinction is easy to miss.
Expect a useful comparison, but not a perfect verdict. Factory visits, reference checks, and performance data still matter. A polished sales presentation cannot replace molten-metal experience.
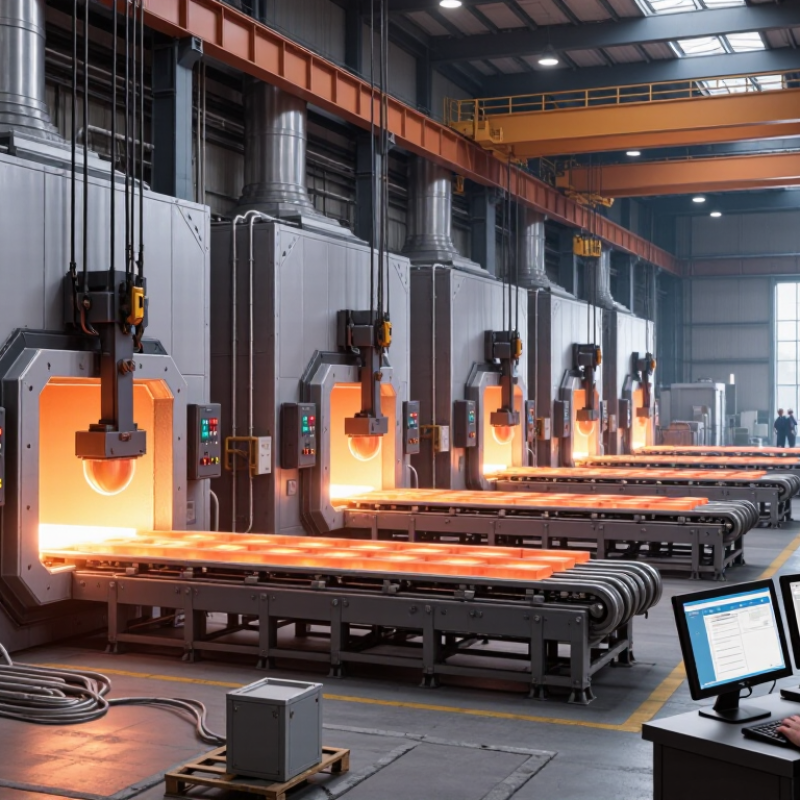
A leading aluminum furnace manufacturer is defined by more than production capacity or a polished catalog. Real expertise appears in the melt shop, where engineers study alloy recipes, charge size, temperature curves, and furnace loading. During commissioning, they should measure heat-up time, temperature uniformity, fuel use, and metal loss under actual operating conditions. Numbers matter. Calibrated thermocouples, infrared cameras, and recorded batch data can reveal uneven heating that operators may miss. These details show whether a design works beyond a controlled demonstration.
Reliability is equally practical. Look for traceable material certificates, documented refractory choices, safety interlocks, and service records from comparable installations. Strong manufacturers explain maintenance intervals and provide realistic performance ranges, rather than promising perfect efficiency. They also train operators to respond to burner faults, door damage, and unexpected temperature drift. That support reflects accountability. However, no furnace performs perfectly in every plant. Poor charge preparation, unstable power, or rushed maintenance can distort results. A credible supplier admits these limits and helps customers test improvements. Some specifications may still feel vague. Ask for acceptance criteria, test methods, warranty boundaries, and energy data measured with the same alloy and workload. Independent inspections can add confidence before payment and after installation. During a site visit, observe noise, fumes, access points, and how easily workers can inspect the lining.

Aluminum furnace manufacturers produce several designs for different melting, holding, and recycling requirements. The right choice depends on batch size, alloy control, fuel costs, and workplace conditions.
Crucible furnaces suit small foundries, laboratories, and short production runs.
Operators place aluminum inside a ceramic or metal crucible, then heat it externally. These furnaces are compact and relatively simple to maintain. They may struggle with high output.
Reverberatory furnaces handle larger batches by heating aluminum in a shallow hearth.
Gas burners or electric elements transfer heat through the furnace chamber. Their spacious design supports continuous casting and demanding production schedules. However, poor temperature control can increase oxidation and metal loss.
Induction furnaces use electromagnetic energy to heat the charge directly.
They offer fast melting and useful temperature control, although electrical demand can be significant.
Electric resistance furnaces provide steady, clean heating for melting or holding applications.
They are often selected where emissions and indoor heat require closer management.
Rotary furnaces can process certain contaminated scrap and recoverable aluminum materials.
Their rotating chamber improves contact between the charge and heat, but operating settings need careful adjustment.
Manufacturers also build holding furnaces, tower furnaces, and custom systems with automated charging or temperature monitoring.
A holding furnace keeps molten aluminum ready for casting without repeated melting cycles. In practical installations, insulation quality matters more than brochures suggest.
Operators should inspect temperature uniformity, refractory wear, energy consumption, and access for cleaning.
No design is perfect.
I would recheck the furnace choice after reviewing actual scrap quality, daily throughput, and maintenance records.
Top aluminum furnace manufacturers are separated less by advertising than by measurable process control. Leading suppliers combine gas-fired, electric, and regenerative heating options with accurate temperature sensing. Their systems often hold molten aluminum within a narrow operating range, reducing oxidation and inconsistent casting quality. In plant trials, engineers should inspect thermal uniformity at several points, not only the controller display. A furnace wall may read correctly while the metal bath remains colder. That detail matters.
Technology comparisons should include burner modulation, insulation design, exhaust recovery, and control software. Modern systems use oxygen monitoring, automatic fuel adjustment, and alarms for door leakage or abnormal pressure. Electric resistance units can offer precise temperature control, while fuel-fired designs may deliver stronger output for large melting volumes. Performance depends on the full installation. Poor charge placement, wet tools, or delayed skimming can erase the benefit of expensive automation. Manufacturers with experienced commissioning teams usually provide heat-up records, energy data, and operator training. These documents make claims easier to verify.
Reliability appears in maintenance access and component life, not just melting speed. Ask for cycle-time data under a stated aluminum load, ambient temperature, and holding temperature. Otherwise, comparisons become vague. Refractory quality, spare-part availability, and remote diagnostic support also affect production continuity. A compact furnace may save floor space but restrict cleaning access. Field experience shows efficient designs can perform poorly when operators cannot reach buildup around the hearth. The best evaluation includes a witnessed test, independent temperature checks, and a realistic energy calculation. Even then, results may vary between seasons and alloys.
| Comparison Dimension | Manufacturer Profile A | Manufacturer Profile B | Manufacturer Profile C | Manufacturer Profile D | Manufacturer Profile E | Manufacturer Profile F |
|---|---|---|---|---|---|---|
| Primary furnace technology | Gas-fired reverberatory | Regenerative gas-fired | Electric resistance | Medium-frequency induction | Rotary melting | Tower or shaft melting |
| Typical application | Foundries and casting lines | High-throughput primary or secondary melting | Clean melting and holding | Rapid alloy melting and precise temperature control | Contaminated scrap and dross-rich feedstock | Continuous high-volume melting |
| Typical capacity range | 0.5–20 t/h | 5–40 t/h | 0.1–10 t/h | 0.1–15 t/h | 1–15 t/h | 10–60 t/h |
| Normal operating temperature | 700–800°C | 700–800°C | 680–800°C | 680–800°C | 700–850°C | 700–800°C |
| Energy efficiency characteristics | Good; depends strongly on heat recovery | Very good due to regenerative combustion | High point-of-use efficiency; electricity source matters | High electrical-to-metal efficiency | Good with optimized burner and exhaust control | Very good for continuous production |
| Temperature uniformity | Good with circulation and zoning | Very good with multi-zone control | Excellent | Excellent within the melt zone | Good; dependent on charge distribution | Very good in continuous operation |
| Melting speed | High | Very high | Moderate | Very high | High | Very high |
| Automation and controls | PLC, SCADA, burner ratio control | PLC, SCADA, oxygen trim, heat recovery control | PLC, PID temperature control, data logging | Power control, PLC, recipe management | PLC, burner sequencing, charge monitoring | Advanced PLC, process monitoring, production tracking |
| Atmosphere and oxidation control | Good with tuned combustion and bath protection | Very good with oxygen monitoring | Excellent; no combustion products | Excellent; low bath disturbance | Moderate to good; design-specific | Very good with controlled charging |
| Emission-control options | Baghouse, afterburner, low-NOx burners | Low-NOx burners, baghouse, heat recovery | Low direct combustion emissions | Low direct combustion emissions; fume extraction | Afterburner, baghouse, enclosed charging | Low-NOx burners, baghouse, heat recovery |
| Best performance advantage | Flexible batch production | Low fuel consumption at large scale | Clean, precise, low-oxidation melting | Fast melting and excellent alloy control | Strong tolerance for difficult scrap | Continuous high-volume productivity |
| Main limitation | Higher oxidation risk than electric systems | Higher initial complexity and maintenance needs | Electricity demand and lower very-large-scale capacity | Higher electrical infrastructure requirements | Potentially higher dross and refractory wear | Less suitable for frequent batch-size changes |
| Recommended buyer priority | Flexibility and proven reliability | Fuel efficiency and throughput | Product quality and environmental performance | Speed, precision, and compact footprint | Scrap flexibility and recovery rate | Maximum continuous output |
Note: The profiles are anonymized. Capacity and temperature figures represent common commercial design ranges for aluminum melting and holding furnaces; actual performance depends on alloy, charge material, furnace size, operating practice, fuel or electricity price, refractory condition, and emissions requirements.
Aluminum furnace manufacturers serve a wide industrial chain, not one narrow market. Their equipment supports secondary aluminum recycling, die casting, extrusion, rolling, and foundry production. The International Aluminium Institute reports that recycled aluminum can require about 95% less energy than primary aluminum production. This makes melting furnaces essential for recovering scrap from vehicles, beverage cans, window frames, and machining operations.
Automotive plants often use gas-fired or electric melting furnaces for engine housings, wheels, and structural castings. Aerospace suppliers demand tighter temperature control for certified components. Extrusion companies use billet-heating and homogenizing furnaces before shaping profiles for buildings, rail systems, and solar frames. Packaging producers need continuous melting systems that maintain stable metal quality at high throughput. The U.S. Department of Energy identifies aluminum as an energy-intensive industrial material, so furnace efficiency directly affects operating costs and emissions.
Recycling plants usually prioritize fast melting, low metal loss, and adaptable charging systems. Foundries may value holding stability more than maximum output. That difference matters. A furnace designed for clean extrusion scrap may perform poorly with oily, mixed post-consumer material. According to the International Energy Agency, aluminum production represents roughly 4% of global electricity consumption, although estimates vary by system boundary. Manufacturers therefore increasingly combine waste-heat recovery, oxygen control, insulation upgrades, and digital temperature monitoring. These tools help, but they do not remove every problem. Operator skill, scrap preparation, and maintenance still decide whether the promised efficiency appears on the factory floor.
Buyers should evaluate aluminum furnace manufacturers through measured performance, not attractive brochures. The U.S. Department of Energy reports that process heating uses about 51% of energy in American manufacturing. Therefore, request energy consumption in kWh per tonne of aluminum, based on a defined charge mix and production rate. Ask for independent test records, not estimates. Melt-loss data matters too. A small oxidation increase can quietly reduce annual output.
Feedstock changes the decision. The International Aluminium Institute states that recycled aluminum requires about 5% of the energy used for primary aluminum production. A suitable furnace should handle the buyer’s actual scrap ratio, coatings, moisture controls, and alloy range. Ask how the supplier maintains temperature uniformity across the bath.
Check burner turndown, exhaust treatment, refractory life, and automatic shutoff functions. Safety documentation should be specific.
Service capability deserves equal attention. Request commissioning procedures, spare-parts availability, remote diagnostics, and response times in writing. Visit a comparable installation if possible. Examine maintenance records, not only production photographs. A furnace that reaches temperature quickly may still suffer from uneven heating or frequent refractory repairs. That detail is easy to miss.
Independent certification can support confidence, but it cannot replace a site acceptance test. Define fuel use, melt rate, temperature deviation, emissions limits, and uptime before signing. A perfect quotation is not proof. Buyers should also challenge their own assumptions, because one trial with clean ingot may hide poor performance with contaminated scrap. Reliable suppliers welcome measurable trials and clearly explain failures. That is a stronger signal than polished marketing.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

