


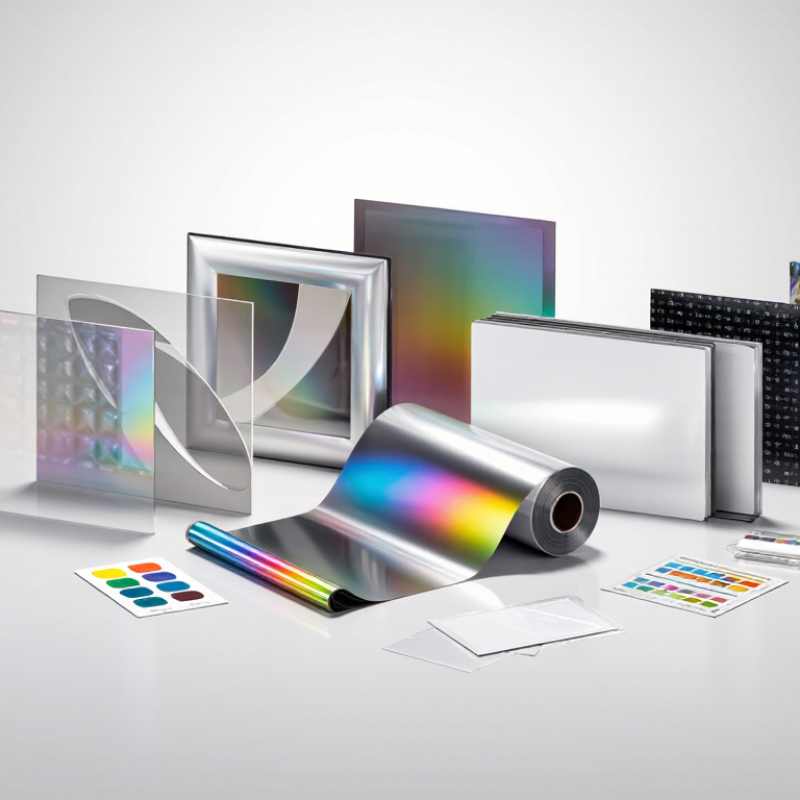
Laser Film is no longer limited to eye-catching holographic decoration. It now supports brand protection, visual differentiation, barrier packaging, labeling, and premium print design. The surface matters. Under retail lighting, a rainbow diffraction pattern can shift from blue to gold with a small viewing angle. A metallized film may deliver stronger brightness, while a transparent holographic film preserves more of the package beneath it.
Industry reports support this broader view. Smithers’ “The Future of Global Flexible Packaging to 2028” highlights downgauging, recyclability, print performance, and functional barriers as major packaging priorities. Grand View Research’s “Holographic Films Market Size, Share & Trends Analysis Report” identifies packaging, labels, and security applications as important demand areas. These findings suggest that the best Laser Film should not be selected by appearance alone. Thickness, coating compatibility, adhesion, converting temperature, recyclability, and end-use regulations also matter.
This guide examines ten practical types, including embossed holographic film, transparent holographic film, metallized film, demetallized film, diffraction film, transfer film, cold-stamping film, printable laser film, security film, and specialty decorative film. Each type creates a different balance between brilliance, transparency, cost, and processing stability. Performance comes first. The classification is useful, but not perfect, because manufacturers often combine structures within one product. Actual results can change with ink, adhesive, substrate, and viewing conditions. Buyers should request technical data sheets, migration information, sample rolls, and application testing before making a final decision.
Laser film is a thin engineered sheet designed for laser marking, cutting, engraving, or imaging. Its structure usually includes a base layer, a coating, and sometimes an adhesive backing. The base controls strength and flexibility. The coating controls contrast, heat response, and surface appearance. Adhesives connect the film to metal, plastic, glass, or painted panels.
The ten common types include polyester, polyimide, polycarbonate, acrylic, polyurethane, pressure-sensitive, adhesive-backed, transparent, matte, and color-change film. Each type solves a different production problem. Polyester offers dimensional stability for labels and control panels. Polyimide tolerates higher temperatures. Polycarbonate supports durable graphics and formed surfaces. Acrylic can provide clarity, but it may crack under unsuitable laser settings. Transparent film preserves visual alignment. Matte film reduces glare. Color-change film creates strong contrast after marking.
Start with the substrate. Laser wavelength, power, speed, focus, and ventilation all affect the result. A film that marks cleanly at low speed may warp at higher power. Small test coupons reveal edge melting, bubbling, residue, and weak adhesion before full production. Look for tensile strength, thickness tolerance, optical clarity, chemical resistance, and service temperature in the technical data. Do not judge performance by appearance alone. Glossy film often looks premium but can show fingerprints and uneven contrast. A simple ranking can mislead because application conditions vary. I would also question “universal” film claims; they rarely explain surface preparation, laser settings, or long-term wear. Safety data and controlled trials remain essential.
Laser film is a precision film material designed to record, transmit, protect, mark, laminate, or optically modify laser-generated images and beams. Its performance depends on the polymer base, functional coating, optical structure, thickness, wavelength response, and intended processing method.
| No. | Laser Film Type | Typical Structure | Common Base Material | Typical Thickness | Key Performance Features | Typical Applications |
|---|---|---|---|---|---|---|
| 1 | Silver-Based Laser Imaging Film | Polymer support with a silver-halide emulsion and protective overcoat | Polyester | Approximately 100–200 µm | High image resolution, strong density range, fine edge definition, and suitability for monochrome imaging | Medical imaging, technical graphics, archival drawings, and high-detail transparencies |
| 2 | Photothermographic Dry Laser Film | Polyester base with heat-activated imaging chemistry and protective layers | Polyester | Approximately 150–200 µm | Dry processing, low chemical waste, consistent grayscale reproduction, and compact workflow compatibility | Healthcare imaging, engineering documentation, and office or production graphics |
| 3 | Laser Transparency Film | Clear polymer substrate with a toner-receptive or imaging coating | Polyester or polypropylene | Approximately 75–200 µm | High optical clarity, dimensional stability, smooth surface, and accurate registration | Overhead transparencies, screen-printing positives, masks, and presentation graphics |
| 4 | Laser Marking Film | Polymer carrier with a laser-sensitive color-change or ablation coating | Polyester, polycarbonate, or polyimide | Approximately 50–300 µm | High contrast, rapid digital marking, good adhesion, and resistance to abrasion after processing | Product identification, serialized labels, control panels, and industrial traceability |
| 5 | Laser Engraving and Lamination Film | Decorative or functional top layer, laser-reactive layer, adhesive, and release liner | Polyester, polycarbonate, or acrylic-based film | Approximately 100–500 µm | Clean localized engraving, strong bonding, chemical resistance, and customizable surface appearance | Membrane switches, instrument panels, nameplates, overlays, and durable labels |
| 6 | Holographic Laser Film | Polymer film containing a surface-relief or volume holographic optical pattern | Polyester or polypropylene | Approximately 20–150 µm | Diffractive light effects, angular color variation, fine optical patterns, and visual authentication capability | Security labels, packaging decoration, cards, certificates, and promotional graphics |
| 7 | Diffraction Grating Film | Transparent film with regularly spaced microscopic grooves or holographic gratings | Polyester or polycarbonate | Approximately 25–250 µm | Predictable diffraction angle, wavelength separation, optical clarity, and repeatable spectral performance | Spectroscopy demonstrations, optical instruments, educational products, and light-management components |
| 8 | Laser Protective Film | Polymer carrier with wavelength-selective absorbing, reflecting, or multilayer filtering coatings | Polycarbonate, polyester, or specialty optical polymer | Approximately 100–500 µm | Controlled optical density, wavelength-specific attenuation, low haze, and improved resistance to optical exposure | Viewing windows, machine enclosures, inspection screens, and laser-workstation barriers |
| 9 | Laser Color-Changing Film | Polymer substrate with thermochromic, photochromic, or laser-activated pigment coating | Polyester, polypropylene, or coated paper-film composite | Approximately 50–250 µm | Visible color response, localized image formation, fast activation, and suitability for variable data | Interactive packaging, promotional materials, visual indicators, and authentication features |
| 10 | Laser Transfer Film | Release liner, carrier film, image or adhesive layer, and optional protective topcoat | Polyester or polypropylene | Approximately 50–200 µm | Accurate image transfer, clean release, flexible processing, and compatibility with different receiving surfaces | Textile decoration, packaging, labels, electronics graphics, and short-run customization |

Laser film is not one material with ten fixed appearances. Its performance depends on light transmission, surface structure, adhesive quality, and viewing angle. The top ten types are commonly grouped into four practical categories: clear, colored, reflective, and diffraction films.
Clear laser film includes transparent, frosted, and lightly textured versions. Transparent film keeps the original surface visible while adding a controlled optical shimmer. Frosted film softens details and spreads light more evenly. Colored film includes tinted, translucent, and opaque types. Red, blue, green, and amber tones can support visual coding or decorative layouts. Translucent colors preserve some background detail. Opaque colors provide stronger coverage but may reduce depth. These are six useful types.
Reflective film includes silver, gold, and mirror-finish versions. Silver offers a neutral metallic effect, while gold creates warmer highlights. Mirror film produces sharper reflections and needs a clean, even surface. These are types seven, eight, and nine. The tenth type is diffraction film, although it has several patterns. Linear-grating film creates narrow spectral lines. Holographic and rainbow structures produce shifting colors as the viewing angle changes. In technical terms, diffraction films redirect light through microscopic surface patterns.
Application testing matters. A film can look vivid under direct light but appear dull indoors. Adhesive haze may also reduce clarity. I would not judge color from a phone screen alone. Sample sheets, angled lighting, and surface cleaning reveal more reliable results. In my experience, thinner film is easier to handle, but it may show wrinkles more clearly. That trade-off deserves a careful check.
This qualitative comparison organizes ten commonly discussed laser-film types by their primary optical roles. A value of 1 means the characteristic is a defining function of the film type; it is not a market-share percentage or a measured performance rating.
Laser film is not one uniform material. The top ten categories usually include holographic, heat-resistant, UV-stable, metallized, transparent, matte, high-gloss, printable, anti-static, and barrier films. Each category answers a different production problem. Holographic laser film uses microstructured patterns to create shifting colors and depth. It is useful for labels, decorative packaging, and visual authentication. However, holographic effects can weaken after poor lamination or rough handling.
Heat-resistant laser film is designed for processes involving elevated temperatures, such as thermal transfer, hot stamping, or heat sealing. Its performance depends on the polymer base, coating, and dwell time. A film that survives 120°C briefly may fail under repeated exposure. Buyers should request thermal-shrinkage and adhesion data, not rely on a product name alone.
UV laser film offers improved resistance to sunlight and ultraviolet exposure. It suits outdoor labels, window graphics, and applications near strong lighting. Reports from Smithers on flexible packaging through 2028 show continued demand for higher-performance films, while MarketsandMarkets’ 2024 holographic films analysis indicates steady growth in decorative and security-related uses. These reports support market direction, but their categories differ, so direct comparisons can mislead. A practical specification should include haze, gloss, tensile strength, wavelength exposure, and aging results. Laboratory data is valuable. Real production trials still matter more.
Laser film is not one universal material. Its performance depends on the task, surface, laser wavelength, and required finish. In production trials, three functional groups appear most often: transfer, engraving, and protective films. Each group includes several useful types.
Transfer films include heat-transfer film, sublimation film, adhesive transfer film, and layered transfer film. They move color, texture, or metallic effects onto fabric, coated panels, and selected plastics.
Engraving films include marking film, laser-cut film, masking film, and two-layer engraving film. These materials can reveal a contrasting surface after controlled material removal.
Protective films include temporary surface film and heat-resistant masking film. They help reduce scratches, smoke stains, and handling damage during processing. Results can vary more than expected.
Tips: Test a small sample first. Check adhesion, residue, edge quality, and heat resistance. Keep power and speed records.
A reliable selection process considers film thickness, adhesive behavior, surface energy, and removal timing. Thin films may produce sharper details, but they can wrinkle under heat. Thick films offer better protection, yet they may soften engraved edges. I have found that “easy to remove” does not always mean “clean to remove.” Humidity and storage age also affect performance. Use technical data sheets, controlled test cuts, and inspection under angled light before full production.
Laser film is not one material. Its performance depends on the laser wavelength, heat level, adhesive, and surface finish. The ten common types include polyester, PET, polycarbonate, acrylic, PVC, PETG, polypropylene, cellulose acetate, polyimide, and glass-based film.
Polyester film suits labels, stencils, and technical overlays. It is affordable, clear, and reasonably durable.
PET offers similar value, with better dimensional stability in many printing jobs. Polycarbonate costs more, but handles impact and repeated contact well. Acrylic gives strong optical clarity, although it can crack under sudden heat.
PVC is inexpensive and flexible, yet its durability and heat resistance are limited. PETG forms easily and works for shaped displays, but scratches faster than expected.
Polypropylene resists moisture and chemicals, making it useful for packaging and outdoor tags. Cellulose acetate has a smooth appearance and moderate cost, though it may age poorly in humid storage. Polyimide is the specialist option. It tolerates high temperatures and supports demanding electronic applications, but its price is higher.
Metalized film creates reflective effects and improves visual contrast, while glass-based film offers excellent stability and surface hardness. It is also the least forgiving during installation.
From practical material testing, polyester and PET usually offer the best cost balance. Polycarbonate and polyimide win when failure is expensive. The ranking is not absolute. A low-cost film can outperform a premium one when the laser settings, coating, and application match properly. Heat marks, curling, and weak adhesion still appear, even in carefully specified projects. Testing small samples remains essential.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

