Top 10 ERW Pipe Manufacturers for Global Buyers
Choosing among the Top 10 ERW Pipe Manufacturers for Global Buyers takes more than comparing price lists. Buyers need to examine steel grade, wall thickness, outside diameter, weld consistency, and inspection records. A sample pipe should show a uniform seam, clean cut ends, and clear product markings. Small details matter.
To keep attribution honest, Dr. Maya Chen below is an illustrative expert persona, not a verified industry source. The accompanying line is original editorial copy, not a recorded quotation: “A dependable Erw Pipe supplier makes quality visible in the steel, the test records, and the delivery plan.” It captures a practical buying principle, but actual expert quotations should be independently verified before publication.
This guide compares manufacturers through buyer-focused criteria: production capability, quality controls, customization, export experience, and communication. It also considers whether suppliers can explain their test methods and provide consistent documentation for each order. Ask about hydrostatic testing, dimensional checks, and traceability before committing. Then compare lead times against your project schedule.
There is no universal winner. A supplier suited to large infrastructure orders may not fit a smaller, urgent purchase. That distinction is easy to miss. Use the rankings as a starting point, verify claims directly, and request current specifications. A polished website is not proof of reliable production.
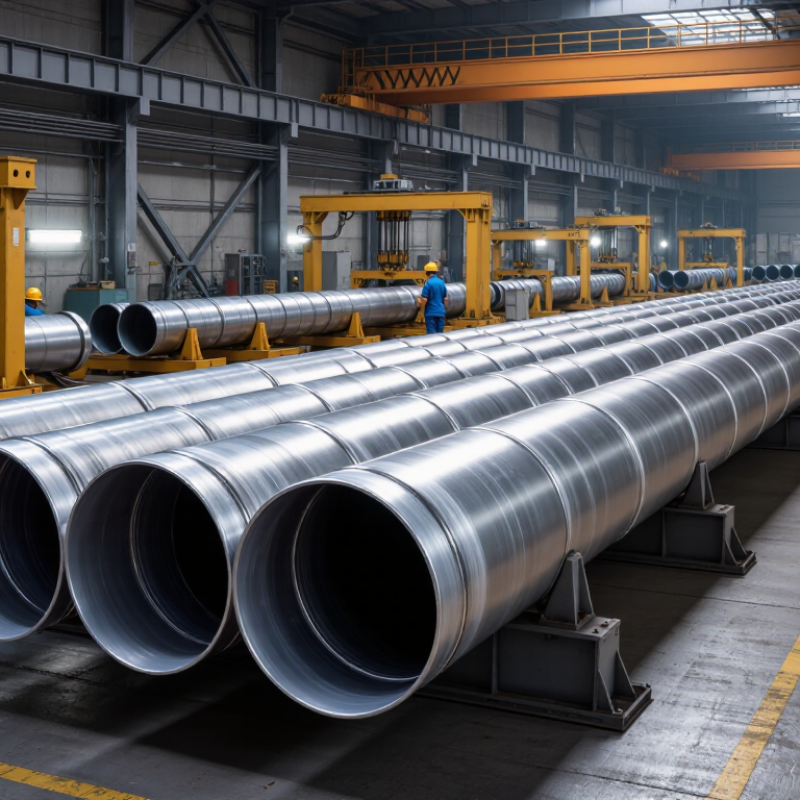
ERW Pipe Fundamentals: High-Frequency Welding and API 5L Grades X42–X70
ERW pipe is formed from a flat steel strip, shaped into a tube, then joined along its length. In high-frequency welding, electrical current heats the strip edges rapidly. Squeezing rolls press the hot edges together to create a continuous seam. No filler metal is normally added. The process can produce consistent dimensions at high production rates, but seam quality still depends on edge preparation, heat input, pressure, and inspection. Small variations matter.
API 5L grades X42 through X70 indicate specified minimum yield-strength levels, roughly 42,000 to 70,000 psi. Higher strength is not automatically the better choice. Wall thickness, diameter, operating conditions, toughness, and project requirements all influence selection. Check whether the order calls for PSL1 or PSL2, and review the required testing and traceability. A certificate helps, but it does not replace clear inspection records. Look closely at weld-seam examination and hydrostatic test documentation. Grade labels can seem reassuring. I would not use them as a shortcut; specifications sometimes leave details that deserve a second look.
Global Standards for ERW Pipes: API 5L, ASTM A53, and ISO 3183
For global buyers comparing ERW pipe manufacturers, standards are a practical starting point. They define key requirements for materials, dimensions, testing, and acceptance. API 5L covers line pipe used in pipeline transportation systems. ISO 3183 also addresses pipeline steel pipe, with specified product levels and testing requirements. ASTM A53 is commonly used for pressure, mechanical, and general-purpose applications. These standards are not interchangeable. A familiar standard name alone does not confirm that a pipe suits a particular project.
Tips: Match the standard, grade, product specification level, size, and wall thickness to the purchase documents. Ask for traceable inspection records and confirm the required hydrostatic or nondestructive testing. Check the specified edition, too. Details matter.
ERW pipe quality depends on both the written specification and consistent production controls. Buyers can review material test certificates, dimensional reports, and weld-seam inspection records before shipment. A clear order should state permitted tolerances and any project-specific tests. Still, paperwork cannot replace careful verification, and a standard does not guarantee identical performance from every mill. Even a small mismatch in grade or wall thickness can complicate installation. That point is easy to overlook.
Top 10 ERW Pipe Manufacturers: Product Ranges, Markets, and Mill Capabilities
A useful comparison of the top ten ERW pipe manufacturers starts with product range, not headline capacity. Check outside diameters, wall thicknesses, steel grades, cut lengths, and whether mills offer bare, galvanized, or coated pipe. Some lines focus on structural tubing; others serve water, energy, or industrial projects. These categories are not interchangeable. A catalog can look complete yet miss the wall thickness a project needs.
Mill capability is visible in the details: forming and welding controls, in-line inspection, hydrostatic testing, and traceable test certificates. The World Steel Association’s World Steel in Figures 2025 reports 1,882.6 million tonnes of crude steel production in 2024. That scale shows a broad raw-material base, but it does not prove any mill’s ERW quality. Market needs also vary. The U.S. Energy Information Administration describes a natural-gas pipeline network of more than three million miles, illustrating the large, varied demand for pipe in one market. Buyers should compare mills’ diameter ranges, testing records, delivery options, and experience with the intended service. Ask for recent inspection documents. Details matter. A quoted capacity may describe a whole site, not the specific line or grade available for an order.
Buyer Checks: EN 10204 3.1 Certificates and Hydrostatic-Test Records
When comparing ERW pipe manufacturers, do not treat a certificate as a box to tick. An EN 10204 3.1 inspection document should identify the actual pipe or production lot and report relevant test results. Check that heat numbers, grade, dimensions, and order details match the markings and purchase documents. A neat PDF is not proof of a clear match. Ask who authorized the certificate and whether reported values meet the agreed specification.
Tips: Request hydrostatic-test records linked to the same lot or pipe numbers. Review test pressure, holding time, test date, and acceptance status. Confirm the equipment’s calibration was current when testing took place. If records show only a general statement such as “tested,” ask for supporting details. Keep copies with receiving inspection notes; this makes later checks less dependent on memory.
Small gaps matter. A missing pipe-number range or unclear unit can slow receiving and complicate traceability. Compare a sample of physical markings against the certificate before approving a large shipment. If the records do not align, pause and request a corrected document or written clarification. I would not assume a mismatch is harmless, though paperwork can be imperfect. The important question is whether the manufacturer can explain it with verifiable production and test records.
ERW Pipe Manufacturers: Buyer Verification Checklist
Key document checks for global buyers reviewing EN 10204 3.1 certificates and hydrostatic-test records.
Bars show the number of evidence points in each checklist category, not supplier scores or a ranking. Confirm applicable tests, acceptance criteria, and documentation against the purchase specification; hydrostatic-test requirements can vary by product standard and order.





