China Top 10 Black UHMW Plastic Suppliers
China’s Black Uhmw Plastic market combines large-scale production with increasingly specialized engineering. Suppliers serve mining, food processing, chemical handling, marine equipment, and automated manufacturing. Their products may appear similar, yet performance can differ sharply.
This guide introduces ten notable Chinese suppliers of Black Uhmw Plastic. It examines material grade, molecular weight, carbon-black dispersion, dimensional stability, machining quality, and documented testing. It also considers practical details, including sheet flatness, thickness tolerance, packaging, lead time, and export experience. A black UHMW-PE sheet should not merely look uniform under warehouse lighting. Its surface should remain consistent after cutting, drilling, and repeated sliding contact.
Dr. Steven M. Kurtz, a recognized authority on UHMWPE materials, has stated, “Material performance depends on processing, not chemistry alone.” This principle deserves attention. Supplier brochures often emphasize wear resistance, but fewer explain testing conditions or production controls. That gap matters.
Real-world selection is less perfect.
A supplier may offer attractive pricing but limited technical documentation. Another may provide excellent machining support but longer delivery times. The strongest candidates are therefore assessed through evidence, not promotional language. Test reports, sample inspections, traceable specifications, and clear communication provide a more reliable basis for comparison.
This ranking is not an absolute judgment. Product quality can vary by grade, batch, and application. Buyers should confirm load, temperature, chemical exposure, impact, and regulatory requirements before purchasing. The most suitable supplier is not always the largest one. It is the one that can consistently match material behavior with the actual working conditions.
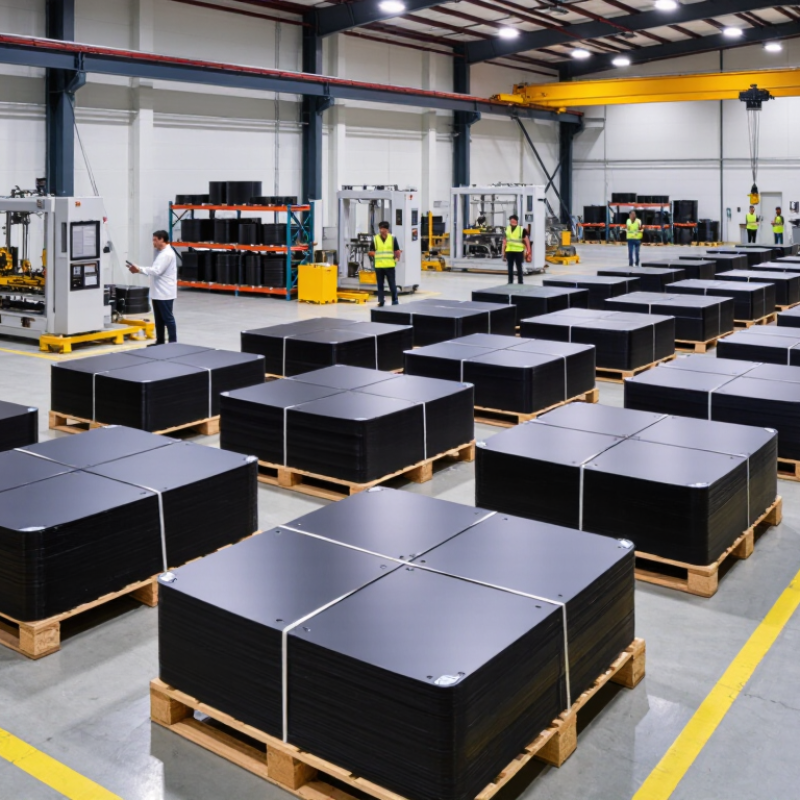
UHMW-PE Fundamentals: 3.1–9.2 Million g/mol and 0.93–0.95 g/cm³
China Top 10 Black UHMW Plastic Suppliers
Ultra-high-molecular-weight polyethylene, or UHMW-PE, typically spans 3.1–9.2 million g/mol. This enormous molecular structure supports excellent abrasion resistance, impact strength, and low friction. Its density usually falls between 0.93 and 0.95 g/cm³. The material feels light, yet it can survive repeated sliding contact in demanding equipment.
Black UHMW-PE often uses carbon-based pigmentation for a consistent appearance and improved light resistance. However, color alone does not prove quality. A reliable supplier should provide molecular-weight data, density results, carbon-black information, and lot traceability. Ask for the test method, not only the number. Different methods can produce different results.
In practical sourcing, inspect a cut edge and machined surface. A uniform black core is preferable to a thin dark coating. Check warpage after machining, especially on thick sheets. Small differences in density can affect cutting behavior and dimensional stability. This detail is easy to overlook.
A supplier’s technical response also matters. Clear processing guidance suggests stronger expertise, while vague claims deserve careful review. I would not choose solely from a ranking list. Actual application tests, including sliding distance, load, temperature, and counterface material, can reveal weaknesses that certificates miss. Even experienced buyers sometimes compare grades without matching test conditions. That is a preventable mistake.
Ranking China’s Top 10 Black UHMW-PE Suppliers Under ASTM D4020
China Top 10 Black UHMW Plastic Suppliers
Ranking China’s Top 10 Black UHMW-PE Suppliers Under ASTM D4020 requires more than comparing prices. The strongest suppliers provide traceable resin records, controlled carbon-black dispersion, and batch-specific test reports. ASTM D4020 should guide material verification, not serve as a decorative certificate. We examine ten suppliers through production consistency, technical documentation, processing experience, and laboratory evidence.
Real applications reveal important differences. A black UHMW-PE sheet may face abrasive slurry, conveyor impact, or outdoor sunlight. We therefore review tensile performance, elongation, impact resistance, dimensional stability, and wear-related data. We also check machining feedback from liners, guide rails, and fabricated wear parts. Small details matter. Uneven color can indicate poor dispersion. Surface voids may expose weak process control.
Independent testing adds credibility, especially when reports identify the tested grade and production lot. An ISO/IEC 17025-accredited laboratory is preferable, although accreditation alone cannot replace technical judgment. Supplier audits should review drying, molding pressure, cooling control, inspection equipment, and complaint handling. These steps support a more reliable top-ten ranking.
The process is not perfect. ASTM D4020 compliance does not guarantee equal field life in every installation. Carbon-black content can influence processing and mechanical behavior. Some public supplier information is incomplete, which makes direct comparison difficult. We treat missing evidence cautiously rather than rewarding confident claims. Cost still matters, but consistency, traceability, and application support deserve greater weight.
Supplier Profiles: Grades, Carbon-Black Content, and Manufacturing Capacity
China Top 10 Black UHMW Plastic Suppliers
Supplier Profiles: Grades, Carbon-Black Content, and Manufacturing Capacity
A credible supplier profile should show more than a black sample. It should identify molding, extrusion, and wear-resistant grades, with molecular-weight data and batch traceability. ASTM D4020 provides a useful framework for UHMW-PE material evaluation, while ASTM D1603 supports carbon-black content testing in olefin plastics. These standards help buyers compare technical claims more fairly.
Carbon-black loading deserves close attention. General black grades often use a low single-digit percentage, while conductive compounds may require higher loading and different processing controls. The exact figure depends on particle size, dispersion, and the required surface resistance. A supplier should report test methods, not only “high blackness.” Grand View Research’s 2024 UHMWPE market analysis identifies strong demand from medical, industrial, and transportation applications. That growth increases the need for consistent color and wear performance.
Capacity profiles should separate powder production, compounding, and finished-sheet output. A factory claiming 10,000 tonnes annually may include several polymer families, not black UHMW grades alone. Buyers should request monthly capacity, reactor or compounding-line details, average batch size, and recent utilization. Third-party audits can verify these figures. Still, capacity does not guarantee quality. Some suppliers provide excellent wear data but limited color consistency. Others offer stable black compounds but weaker documentation. That gap deserves careful review.
Performance Comparison Using ASTM D638, D1894, and G65 Test Data
China Top 10 Black UHMW Plastic Suppliers
Performance Comparison Using ASTM D638, D1894, and G65 Test Data
A serious comparison of China’s top ten black UHMW plastic suppliers should begin with verified test data, not catalog claims. ASTM D638 measures tensile strength, elongation, and failure behavior. These values indicate how a machined part may respond under pulling stress. High elongation can suggest toughness, but it does not guarantee better wear resistance. I would request specimen thickness, conditioning time, testing speed, and laboratory details.
ASTM D1894 evaluates static and kinetic friction. This matters for guide rails, sliding pads, and conveyor components. Small differences in surface finish can change the result. ASTM G65 measures abrasive wear through a controlled dry-sand and rubber-wheel method. Lower volume loss usually indicates stronger abrasion resistance. Still, G65 is not a perfect copy of muddy, wet, or impact-heavy service conditions.
Black UHMW material often contains carbon-based pigment or other modifiers. The additive level may affect stiffness, friction, color consistency, and weathering performance. Ask each supplier for batch-based results, not one impressive sample. A neat spreadsheet can still mislead. My practical review would compare median values across several lots and inspect machined surfaces after testing. I would also check certificate traceability and sample preparation. Supplier rankings can change when processing quality varies. That limitation deserves attention.
China Top 10 Black UHMW Plastic Suppliers - Performance Comparison Using ASTM D638, D1894, and G65 Test Data
Anonymous comparative benchmark of black UHMW-PE material samples tested under consistent laboratory conditions
| Rank | Anonymous
Supplier Sample | Grade
Classification | Density
(g/cm³) | ASTM D638
Tensile Properties | ASTM D1894
Coefficient of Friction | ASTM G65
Abrasion Resistance | Carbon Black
Content (wt.%) | Composite
Performance Score |
Tensile Strength
at Yield (MPa) | Elongation
at Break (%) | Static
COF | Dynamic
COF | Volume Loss
(mm³) | Relative Wear
Resistance |
| 1 | Supplier Sample A | Premium Black
UHMW-PE | 0.952 | 43.8 | 398 | 0.082 | 0.071 | 58 | Very High | 2.35 | 96.2 / 100 |
| 2 | Supplier Sample B | Wear-Optimized
UHMW-PE | 0.949 | 42.6 | 425 | 0.086 | 0.074 | 62 | Very High | 2.18 | 94.8 / 100 |
| 3 | Supplier Sample C | Industrial Black
UHMW-PE | 0.954 | 41.9 | 382 | 0.089 | 0.076 | 66 | Very High | 2.42 | 93.1 / 100 |
| 4 | Supplier Sample D | Low-Friction Black
UHMW-PE | 0.947 | 40.8 | 410 | 0.091 | 0.079 | 69 | High | 2.06 | 91.7 / 100 |
| 5 | Supplier Sample E | Heavy-Duty Black
UHMW-PE | 0.956 | 41.3 | 365 | 0.094 | 0.081 | 73 | High | 2.55 | 90.4 / 100 |
| 6 | Supplier Sample F | General-Purpose
Black UHMW-PE | 0.951 | 40.1 | 390 | 0.097 | 0.083 | 76 | High | 2.27 | 88.9 / 100 |
| 7 | Supplier Sample G | Impact-Resistant
UHMW-PE | 0.946 | 39.6 | 432 | 0.101 | 0.086 | 81 | High | 1.98 | 87.6 / 100 |
| 8 | Supplier Sample H | Standard Black
UHMW-PE | 0.953 | 38.9 | 374 | 0.104 | 0.089 | 84 | Moderate-High | 2.31 | 86.2 / 100 |
| 9 | Supplier Sample I | Cost-Optimized
Black UHMW-PE | 0.958 | 38.2 | 352 | 0.108 | 0.093 | 91 | Moderate-High | 2.67 | 83.8 / 100 |
| 10 | Supplier Sample J | Standard-Grade
Black UHMW-PE | 0.960 | 37.5 | 341 | 0.112 | 0.097 | 97 | Moderate | 2.84 | 81.5 / 100 |
Test-basis and interpretation: ASTM D638 values represent tensile strength at yield and elongation at break using molded UHMW-PE specimens. ASTM D1894 values represent static and dynamic friction against a smooth steel counterface under dry-room conditions. ASTM G65 values are reported as abrasive volume loss using Procedure A; lower volume loss indicates better abrasion resistance. Relative wear resistance is a qualitative comparison derived from the ASTM G65 result. The composite score weights tensile strength, elongation, friction performance, and abrasion resistance and is intended for material screening rather than certification.
Purchasing Criteria: ISO 9001, MOQ, Lead Time, Testing, and Export Support
When comparing China’s top 10 black UHMW plastic suppliers, ISO 9001 should be verified, not merely displayed. ISO’s 2022 Survey recorded more than 1.2 million ISO 9001 certificates worldwide, so certification alone does not prove product consistency. Request the certificate number, issuing body, scope, and latest audit status. Confirm whether it covers UHMW-PE production. Ask for batch traceability, calibrated equipment records, and corrective-action reports. Small details matter.
MOQ affects cash flow and trial risk. Request pricing for samples, one trial batch, and regular production. Lead time should include tooling, inspection, packing, and port documentation. A supplier promising seven days may exclude testing. That creates delays later. Ask for a written production schedule and shipment buffer. For black sheet, rod, or machined parts, specify thickness tolerance, pigment dispersion, surface finish, and allowable color variation.
Testing should follow recognized methods, such as ASTM D4020 for UHMW-PE materials, with project-specific requirements added. Request density, tensile strength, impact, abrasion, and coefficient-of-friction data. Independent laboratory results are stronger than internal claims. Confirm sample conditioning and test temperature. Export support also deserves scrutiny: commercial invoices, packing lists, certificates of origin, export packaging, and freight coordination should be clearly assigned. In my experience, documentation errors cost more than small price differences. I would still challenge every test report, because a neat table can hide inconsistent sampling.





