


Replacing a Fluoropolymer PPA Is More Than an Additive Change
As film manufacturers evaluate alternatives to fluoropolymer-based polymer processing aids, one question becomes increasingly important:
How can a PFAS-free PPA be compared with the existing fluoropolymer PPA under real production conditions?
The answer cannot be based only on additive dosage or the appearance of the first film produced after changeover.
A processing aid operates within a complete extrusion system. Resin type, film structure, other additives, screw and die design, output, melt temperature, and downstream converting requirements can all influence the result.
For this reason, replacing a fluoropolymer PPA with a PFAS-free alternative should be treated as a controlled production-line change.
The objective is to determine whether the candidate can establish a stable and repeatable production window while maintaining the required film quality.
That means looking beyond one parameter. Melt fracture, die build-up, pressure stability, film appearance, production losses, and downstream conversion should be considered together.
Start With a Stable Production Baseline
Before changing the PPA, the existing production condition should be clearly documented.
Without a reliable baseline, it is difficult to determine whether a later improvement or deterioration comes from the candidate PPA or from normal process variation.
The most relevant baseline information includes the resin formulation, film structure, current PPA and dosage, major additives, extrusion output, melt temperature, pressure condition, film quality and cleaning history.
| Area | Key Information |
| Formulation | Resin grades, blend ratio, existing PPA, dosage and major additives |
| Film | Structure, layer ratio, thickness and quality requirements |
| Process | Output, melt temperature, pressure, screw speed and cooling condition |
| Equipment | Extruder, die configuration and filtration condition |
| Production | Scrap, cleaning frequency, rejected rolls and downstream requirements |
The baseline should represent stable production rather than a single machine reading.
Process variation also matters. A similar average pressure, for example, does not necessarily mean the process is equally stable if pressure fluctuation increases significantly.
The goal is to establish a reference condition that can later be compared with the PFAS-free candidate.
One of the most common problems in replacement trials is evaluating the candidate too early.
Residual fluoropolymer PPA may remain in the feeding system, screw, screen pack, die channels or equipment dead zones after the formulation is changed.
As a result, the first film produced after changeover may not represent the independent performance of the PFAS-free PPA.
A useful trial therefore separates three stages:
Changeover — the previous formulation is being displaced.
Conditioning — the new PPA is moving through the extrusion system and establishing its processing response.
Stable production — the process has reached a sufficiently repeatable condition for comparison.
There is no universal conditioning time.
The required period can vary with equipment history, die geometry, previous PPA chemistry, resin system, dosage, output and processing temperature.
For this reason, conditioning should be measured on the actual production line rather than assumed from another machine or formulation.
The trial team should also define in advance when transition material will be discarded and when candidate data will begin to be treated as valid production data.
Compare PFAS-Free and Fluoropolymer PPA at Matched Output First
Once the process has stabilized, the first comparison should be made under operating conditions that are as similar as practical.
The purpose at this stage is not to maximize output.
It is to answer a more basic question:
Can the PFAS-free PPA maintain the current production requirement while preserving process stability and film quality?
Where possible, resin formulation, film structure, film thickness, output, screw speed, melt temperature, cooling and filtration condition should remain consistent.
If the PPA is changed at the same time that output and processing conditions are significantly adjusted, it becomes difficult to determine what caused the observed result.
Higher-output testing should therefore be conducted separately, after stable performance has first been demonstrated at the reference condition.
Dosage also needs to be compared carefully.
A statement such as “1% versus 1%” can be misleading if the products have different active contents, carriers or layer allocations.
For multilayer films in particular, it should be clear whether dosage refers to the total film formulation, one specific layer, the masterbatch addition rate or the actual active processing-aid concentration.
A valid comparison requires the dosage basis to be defined before conclusions are drawn.
Do Not Treat Melt Fracture, Die Build-Up and Pressure as the Same Result
A good PPA replacement trial should avoid reducing extrusion performance to one visible or numerical indicator.
Melt fracture may appear as sharkskin, repetitive roughness, surface distortion, uneven gloss or irregular lines.
Rather than recording only that melt fracture is “better” or “worse,” the comparison should consider defect severity, the output at which the defect appears and the time required for the surface to reach an acceptable condition.
Standardized photographs can help support visual comparison.
Any significant temperature adjustment should also be recorded because melt temperature itself can influence surface instability, degradation, cooling and downstream film behavior.
Die build-up should be evaluated separately.
A smoother film does not automatically mean that die deposits have been eliminated.
Useful observations include deposit growth, location, transfer to the film, cleaning interval, cleaning-related downtime and scrap.
Because die build-up may also be influenced by resin degradation, contamination, filtration and additive interactions, it should be observed over a meaningful production period rather than judged from one short run.
Melt pressure and motor load can provide useful information about processing behavior, but neither should be interpreted in isolation.
For example, a lower current reading does not automatically prove lower production energy.
Where energy efficiency is part of the trial objective, a more relevant metric is:
Specific energy consumption = energy used ÷ kilograms of acceptable film produced
The amount of acceptable film matters more than nominal output alone.
Film Quality Still Determines Whether the Replacement Works
A processing aid may improve extrusion behavior but still affect another part of the finished-film specification.
For packaging applications, relevant checks may include haze, gloss, coefficient of friction, blocking, sealing, printing adhesion, lamination and winding behavior.
Industrial or technical films may require additional mechanical or durability testing.
The exact test plan should therefore follow the end-use application rather than a fixed universal checklist.
This is especially important when the formulation already contains slip, antiblock, pigments, stabilizers or reclaim material.
The PPA does not operate independently from the rest of the additive package.
Downstream conversion should also remain part of the approval process.
A candidate that improves extrusion but causes unacceptable printing, lamination or sealing performance cannot be considered a successful replacement.
From Replacement Trial to Stable Production Window
A controlled trial should ultimately answer three questions.
First, can the PFAS-free PPA reproduce the required production condition at matched output?
Second, can that condition remain stable over a meaningful production period?
Third, can the process be optimized further without moving the finished film outside specification?
A practical evaluation can be summarized as follows:
| Stage | Main Objective |
| Baseline | Define the current stable production condition |
| Changeover & conditioning | Separate residual PPA effects from candidate performance |
| Matched-output comparison | Compare process stability and film quality |
| Long-run evaluation | Observe melt fracture, die behavior and production losses |
| Downstream validation | Confirm printing, lamination, sealing or other requirements |
| Output optimization | Increase output only after stable performance is established |
| Repeatability | Confirm the preferred condition before regular production approval |
If the PFAS-free PPA allows higher output, that additional capacity should only be considered meaningful when film quality remains acceptable.
The same principle applies to lower pressure, reduced torque or longer cleaning intervals.
Each improvement should be evaluated in the context of the complete production result.
A successful replacement is therefore not defined by the lowest pressure reading or the fastest disappearance of melt fracture.
It is defined by a stable, repeatable production window that meets the required film specification.
How SILIKE Supports PFAS-Free PPA Replacement Trials
SILIKE’s SILIMER PFAS-free PPA portfolio includes both silicone-based and silicone-free technologies, available in active-additive and masterbatch formats for film and other extrusion applications. Product selection is based on the resin system, film structure, extrusion process, existing PPA technology, additive package, processing conditions, and customer requirements.
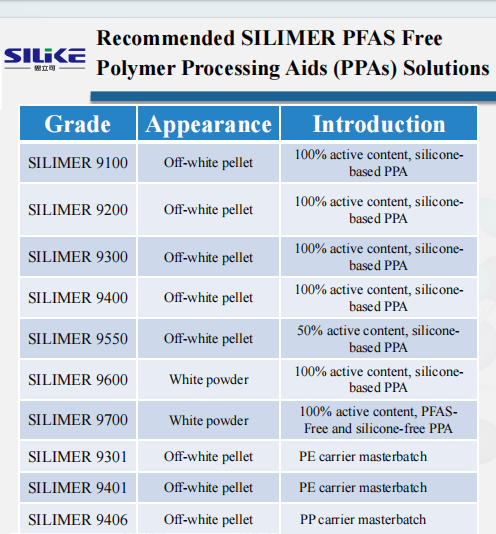
For a more relevant technical evaluation, customers can share key application information such as resin formulation, film structure, current PPA and dosage, extrusion output, processing temperature, and the main processing issue to be addressed.
Based on these conditions, the SILIKE technical team can recommend a suitable PFAS-free PPA candidate and help define a controlled production trial to determine the appropriate dosage, conditioning response, and stable operating window.
Planning to replace a fluoropolymer PPA in film extrusion?
Discuss your formulation and processing conditions with SILIKE.
Website: www.siliketech.com
Email: sale@levvymetal.com
Frequently Asked Questions
Not necessarily. Products may differ in active content, carrier resin, and recommended addition level. Dosage should be compared on a clearly defined basis and validated in the intended formulation.
There is no universal conditioning time. Equipment history, previous PPA, resin, dosage, output, and die design can all influence how quickly the process reaches a stable response.
The first comparison is more useful when conducted at a representative matched-output condition. Higher-output testing should follow after stable performance and acceptable film quality have been confirmed.
Conclusion
Replacing a fluoropolymer PPA with a PFAS-free alternative should be managed as a controlled extrusion trial rather than a simple additive substitution.
The evaluation should begin with a stable baseline, separate changeover and conditioning from steady production, and compare the candidate under matched operating conditions.
Melt fracture, die build-up, pressure behavior, film quality, and downstream conversion should then be assessed as separate but related parts of the production system.
The most useful outcome is not one isolated improvement.
It is a stable, repeatable production window that delivers acceptable film quality and supports regular production.


