What Is a Nozzle Cutting Machine and How Does It Work?
A Nozzle Cutting Machine is a specialized system designed to cut, shape, or finish nozzle components with controlled accuracy. These parts appear in welding torches, spray systems, burners, and industrial fluid equipment. Their openings may look simple, but small errors can affect flow, pressure, alignment, and service life.
Manufacturing-process expert Dr. John A. Schey emphasized the importance of controlled production: “Manufacturing quality begins with controlling the process, not correcting defects afterward.” This principle applies directly to nozzle cutting. The machine usually combines a cutting head, positioning system, workholding fixture, and computer-controlled settings. Depending on the material and design, it may use laser, plasma, waterjet, or precision mechanical cutting.
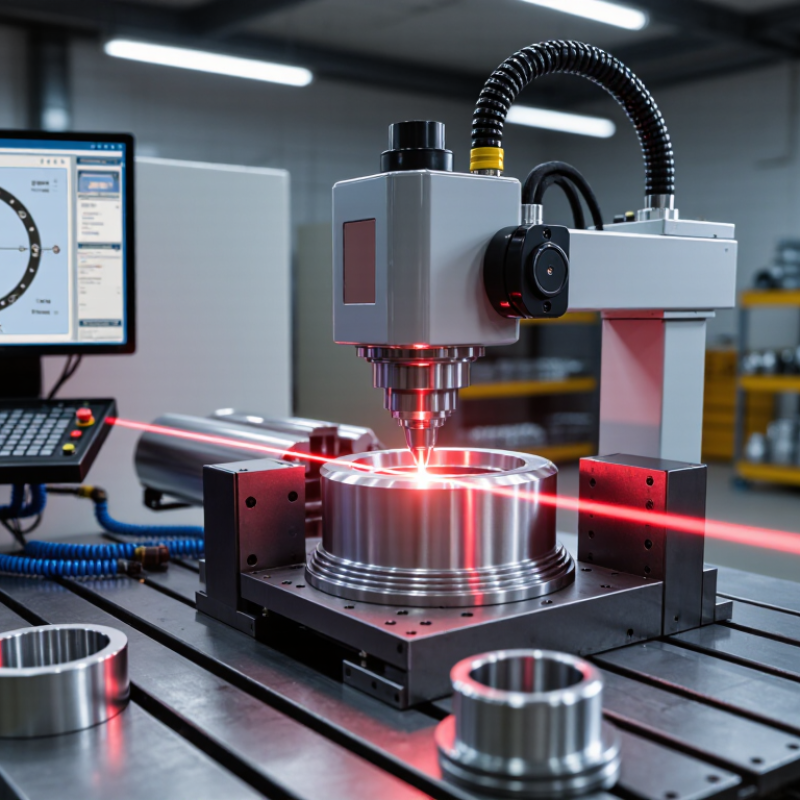
During operation, an operator loads the tube or nozzle blank, sets the cutting profile, and checks the material thickness. The machine then follows programmed paths around the component. A bright laser line may trace the edge, while sensors monitor position and cutting stability. Finished parts often receive deburring, dimensional inspection, and visual checks.
The process sounds straightforward.
It is not always perfect.
Heat distortion, tool wear, vibration, and incorrect settings can still produce rough edges or uneven openings. Experienced technicians understand this risk. They inspect the actual part, not only the digital file. This guide explains what a Nozzle Cutting Machine does, how its main systems work, and where practical judgment remains essential. Reliable results depend on suitable equipment, skilled setup, preventive maintenance, and honest quality control.
Definition and Purpose of a Nozzle Cutting Machine
A nozzle cutting machine is a CNC system designed to create accurate openings in pipes, tanks, and pressure-vessel plates. The term is not perfectly standardized across workshops. Some suppliers use it for plasma cutting, while others describe laser or oxy-fuel equipment. Its main purpose remains similar: forming a nozzle opening with the correct diameter, angle, and position.
The machine reads a CAD drawing or programmed cutting path. A rotating worktable may hold the pipe or vessel shell. The cutting head then follows the required contour, often producing a circular, oval, or angled opening. Sensors can help control height and alignment. This matters because poor positioning can affect later welding and inspection. The World Steel Association reported 1.892 billion tonnes of crude steel production in 2023. That scale shows why repeatable fabrication methods remain important across heavy industry. Yet automation does not remove judgment. Material distortion, rust, and imperfect drawings can still cause errors.
Tips: Confirm the plate thickness before selecting the cutting process. Check the nozzle angle with a calibrated gauge. Leave enough allowance for beveling and welding. Review the first cut manually. A perfect digital path can still produce a poor opening when the workpiece shifts. Record actual measurements, not only machine settings. This small habit improves traceability and reveals weak assumptions in the production plan.
Main Components and Their Functions
A nozzle cutting machine uses a focused cutting stream to separate metal or other suitable materials. The nozzle is the working end of the system. It directs compressed gas, plasma, water, or another cutting medium toward the workpiece. A narrow opening improves precision, but it can clog or wear during demanding jobs. Small changes matter.
The cutting head holds the nozzle and maintains the correct distance from the material. The gas supply regulates pressure and flow, while the power unit controls cutting energy. A motion system moves the head along programmed paths. Its rails, motors, and drive components affect edge quality. The controller converts drawing data into movement commands. Sensors may detect height, position, or abnormal conditions. The worktable supports the sheet and allows debris to leave the cutting area. In practical use, operators still need to inspect these parts. Automatic control is helpful, not magical.
Tips: Clean the nozzle before each shift. Check its opening for distortion, residue, or uneven wear. Confirm gas pressure with a calibrated gauge. Secure the workpiece firmly. Run a small test cut first. If the edge shows heavy dross, review speed, power, and nozzle distance. Do not change several settings at once. That makes troubleshooting confusing. Keep maintenance records, even when the machine seems stable. A missed inspection can become an expensive mistake.
How the Cutting Process Works Step by Step
What Is a Nozzle Cutting Machine and How Does It Work?
A nozzle cutting machine directs plasma, laser, or gas through a shaped nozzle. The nozzle focuses energy onto metal with controlled pressure. A 2024 Grand View Research report forecasts steady growth in the global cutting machine market through 2030. This reflects wider factory investment in automated, repeatable cutting.
How the Cutting Process Works Step by Step
The operator loads a CAD drawing and selects material thickness. The controller calculates the cutting path, speed, pierce point, and kerf compensation. The nozzle then moves above the sheet at a fixed height. Gas flows through the opening before the arc or beam starts. A brief piercing cycle creates the entry hole. The cutting head follows the programmed path, removing a narrow strip of metal. ISO 9013:2017 classifies thermal-cutting quality by features such as edge angle, roughness, and tolerance. Real production is less perfect. Warped sheets, dirty nozzles, and unstable gas pressure can distort edges. The machine may finish the program, yet the part still needs inspection.
Tips: Check nozzle wear before every shift. Measure the standoff distance carefully. Use a test cut on unfamiliar material. Compare the edge with ISO 9013 requirements, not appearance alone. A clean, bright edge can still hide excessive taper. Record speed, gas pressure, and defects for later adjustment.
Common Materials and Industrial Applications
A nozzle cutting machine uses a controlled stream to separate material along a programmed path. Depending on the process, the nozzle delivers laser energy, plasma, or high-pressure water with abrasive particles. A CNC system moves the cutting head, while gas pressure, focal distance, speed, and nozzle height affect the final edge. Small errors matter. A worn nozzle can create taper, dross, or uneven corners.
Material choice determines the best method. Mild steel remains a major target, supported by the World Steel Association’s report of about 1.89 billion tonnes of crude steel production in 2023. Stainless steel and aluminum are also common in fabrication, transport, and machinery. The U.S. Geological Survey reported global primary aluminum production near 70 million tonnes in 2023. Aluminum reflects heat, so laser settings require careful control. Waterjet cutting suits thick metal, glass, stone, ceramics, and layered composites. It produces little heat distortion, but abrasive disposal and operating cost need attention.
Industrial applications are broad. Automotive plants cut brackets and body components. Shipyards process thick plates. Aerospace suppliers use narrow kerfs for aluminum alloys and composite panels. Construction workshops cut beams, pipes, and façade parts. Job shops often choose waterjet cutting when heat could weaken a finished surface. The result is not always perfect. Operators still inspect kerf width, burrs, dimensional accuracy, and material deformation. Reports from the International Organization for Standardization also emphasize process control and measurement, not machine speed alone.
What Is a Nozzle Cutting Machine and How Does It Work?
Common materials used in nozzle-based cutting processes, shown by their approximate melting points.
A nozzle cutting machine directs a focused stream of energy or high-pressure fluid through a small nozzle to remove material. Plasma and laser systems cut by melting or vaporizing material, while abrasive waterjet systems cut through mechanical erosion and can process materials that are difficult to cut thermally.
These machines are commonly used in automotive fabrication, aerospace components, structural metalwork, shipbuilding, machinery manufacturing, architectural panels, and precision prototype production. The best cutting method depends on material type, thickness, required accuracy, heat sensitivity, and production volume.
Safety Measures and Maintenance Requirements
A nozzle cutting machine directs laser, plasma, gas, or abrasive flow through a small nozzle to cut metal and other materials. The nozzle controls the cutting path, pressure, heat, and material removal rate. Operators must understand the machine’s specific energy source before starting work. A damaged nozzle can produce uneven cuts, sparks, excess heat, or unexpected spray.
Safety deserves more attention than cutting speed. The U.S. Bureau of Labor Statistics reported 844 fatal workplace injuries involving contact with objects and equipment in 2023. This figure covers many industries, but it shows why guarding and operator training matter. Keep doors, shields, and interlocks functional. Wear eye and face protection rated for the process. Use suitable gloves, hearing protection, and flame-resistant clothing when required. Remove flammable materials from the cutting area. Never reach toward the nozzle during operation, even when the machine appears idle. Stored pressure and residual heat can remain dangerous.
Tips: Inspect the nozzle before every shift. Check alignment, cracks, clogging, and tip wear. Clean it with approved tools, not improvised metal objects. Follow the maintenance schedule recommended in the equipment manual and record each inspection. Replace filters, seals, and consumable parts before failure. In practice, checklists are sometimes rushed. That is a weakness worth correcting. A five-minute inspection may prevent poor cuts, downtime, or injury. The International Organization for Standardization’s ISO 12100 framework also supports risk assessment throughout machine design and use.