7 Machine Safety Guard Buying Tips for Global Buyers
Buying a Machine Safety Guard is not just a matter of choosing a strong panel. The right guard must suit the machine, the task, and the people working nearby. A design that looks secure in a catalogue may block an operator’s view or make routine cleaning awkward. Small details matter.
For global buyers, requirements and working conditions can differ between sites. Check the machine’s hazards, access points, operating speed, and maintenance routines before comparing suppliers. A packaging line may need clear panels for visibility, while a cutting machine may require more robust barriers. No single material or layout fits every application.
This guide presents seven practical buying tips, from assessing risk and selecting materials to checking access, installation, and supplier documentation. Ask how panels are joined, how doors are interlocked where needed, and whether replacement parts are readily available. Request drawings and confirm that the proposed guard works with the actual machine—not only a showroom model. It is easy to overlook maintenance access. That can become a daily frustration.
Safety expectations also vary by destination and industry. Verify applicable local requirements with qualified safety professionals, and document the reasoning behind your choice. A supplier’s assurance can be useful, but it should not replace a site-specific review. Some decisions remain imperfect: budgets, space, and visibility can pull in different directions. Careful questions help buyers spot those trade-offs before purchase.
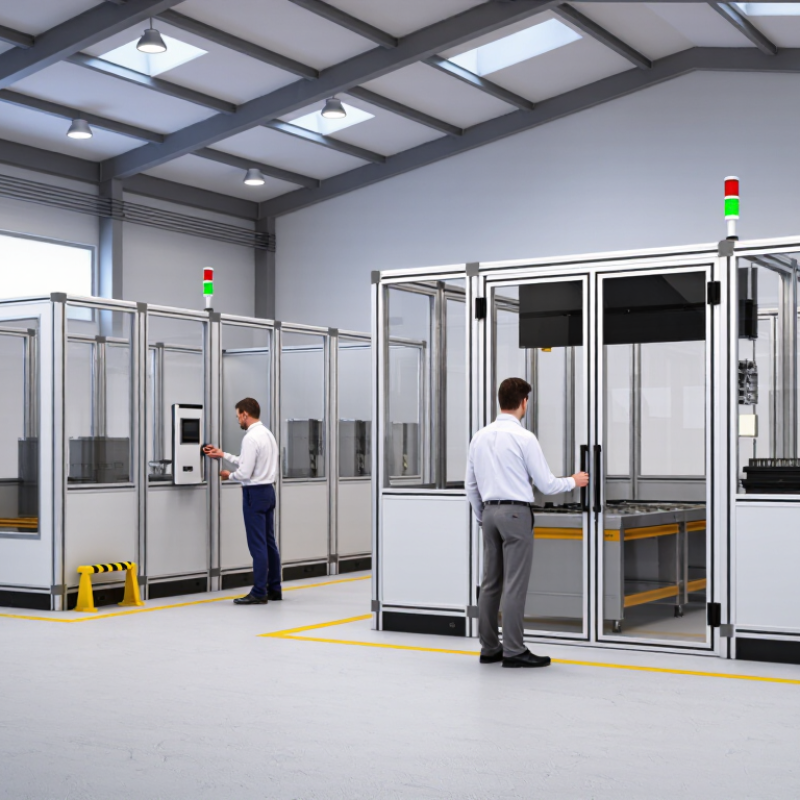
Assess Machine Hazards and Risk Reduction Under ISO 12100:2010
Assessing hazards under ISO 12100:2010 starts with the machine’s real tasks, not just its appearance. Observe setup, operation, cleaning, jam clearing, and maintenance. Map contact with moving parts, ejected material, sharp edges, and unexpected startup. A hand reaching past a feed opening may reveal more than a drawing. Estimate each risk by considering potential injury severity and the likelihood of exposure, then reduce it through inherently safer design, safeguarding, and clear information. Reassess after changes. Small gaps matter.
The ILO’s 2023 global estimates report 2.93 million work-related deaths and 395 million non-fatal work injuries each year. These figures cover many hazards, not machine guarding alone, but they underline why risk assessment must be practical and documented. Record who may be exposed, how often access occurs, and what could fail. A neat risk score can still miss a rushed adjustment or a guard removed for cleaning. That deserves a second look.
Tips: Check reach distances with the actual tool and workpiece. Verify guards stay secure during routine use, and confirm interlocks stop hazardous motion when opened. Ask operators and maintenance staff to test foreseeable tasks; their observations often expose awkward access points. Keep the assessment specific to each machine and review it after incidents, modifications, or new production demands.
Set Safe Reach Distances Using ISO 13857:2019 Tables
ISO 13857:2019 helps determine how far a hazard must sit from a guard to prevent reaching over, under, around, or through it. Use the table that matches the access route and guard opening. A hand reaching through a narrow slot is not the same case as an arm reaching over a panel. Check the opening’s shape and clear dimensions, then measure to the nearest hazardous point. Small details matter.
Do not choose a distance by eye. A mesh panel may look secure, yet its openings can allow access closer than expected. A tidy CAD model can also mislead if it omits a gap near the floor or a removable section. Recheck the finished guard, including hinges, seams, and nearby surfaces. Measure twice.
The tables provide design guidance, not a substitute for assessing the actual machine and how people may approach it. Consider the hazard’s location, likely reach direction, and whether another opening creates a shorter path. If the layout does not fit a table neatly, pause and get a competent safety review rather than forcing a convenient value. Small changes to panel height or opening size can affect the required distance, so record the chosen table and measurements for future checks.
Specify Interlocks and Required Performance Levels (PL a–e)
A guard interlock should match the risk, not simply the machine’s purchase price. ISO 13849-1:2023 defines five Performance Levels, from PL a to PL e, using probability of dangerous failure per hour (PFHd). Its bands range from 10⁻⁵–less than 10⁻⁴ for PL a to 10⁻⁸–less than 10⁻⁷ for PL e. These figures help compare safety functions; they do not determine the required level by themselves.
Set the required Performance Level (PLr) through a documented risk assessment. Consider access frequency, potential injury severity, and whether workers can avoid the hazard. A frequently opened door near a fast-moving cutter needs a different assessment from a rarely accessed enclosure. ISO 14119:2013 also addresses interlocking devices and measures to reduce defeat or bypass. Still, a sophisticated switch cannot compensate for an unsafe layout.
Specify the interlock type, guard-locking need, fault monitoring, reset location, and expected operating cycles. Check the full safety circuit, including wiring and control logic, against the selected PLr. For a locked guard, verify that release occurs only after hazardous motion has stopped. Small details matter. A release button placed inside the enclosure can create a serious blind spot. Ask suppliers for supporting calculations and validation records, then confirm that the proposed design fits the actual machine and maintenance routine. Even careful specifications can miss real-world workarounds. Revisit them with operators before ordering.
Verify Market Compliance: OSHA 1910.212 and EU 2023/1230
Machine guards should be checked against the requirements of the country where equipment will be installed and sold. Under OSHA 1910.212, employers must provide guarding for hazards such as points of operation, ingoing nip points, and rotating parts. Guards should prevent access to danger zones without creating new hazards or unnecessarily obstructing work. Small details matter. A narrow opening may still allow a hand to reach a moving blade.
For equipment placed on the EU market from 20 January 2027, Regulation (EU) 2023/1230 applies, replacing the Machinery Directive 2006/42/EC. Ask suppliers which conformity documents apply to the machine and its guards, and check that the documentation matches the delivered configuration. Review risk assessments, guard drawings, and instructions for use. A drawing should show openings, fixing points, and access for routine cleaning or maintenance. If a panel is removable, confirm how it is secured and whether hazardous movement is controlled when access is needed.
Do not rely on a certificate or checklist alone. Walk around the machine and compare the guard with real tasks, including loading, clearing jams, and cleaning. A guard that looks solid in a brochure can leave a reach path beside a conveyor. I have seen small gaps overlooked. Local workplace rules and product-market obligations can differ, so have a qualified safety professional review uncertain cases before purchase or installation.
Machine Safety Guard Buying Tips: Regulatory Milestones
Use these dates to plan compliance checks for equipment destined for the U.S. or EU market.
Buyer check: OSHA 29 CFR 1910.212 sets general machine-guarding requirements for U.S. workplaces. Regulation (EU) 2023/1230 entered into force on 19 July 2023 and generally applies from 20 January 2027. Confirm which rules apply to the machine, its intended use, and the destination market before purchase.
Sources: OSHA 29 CFR 1910.212 · Regulation (EU) 2023/1230





