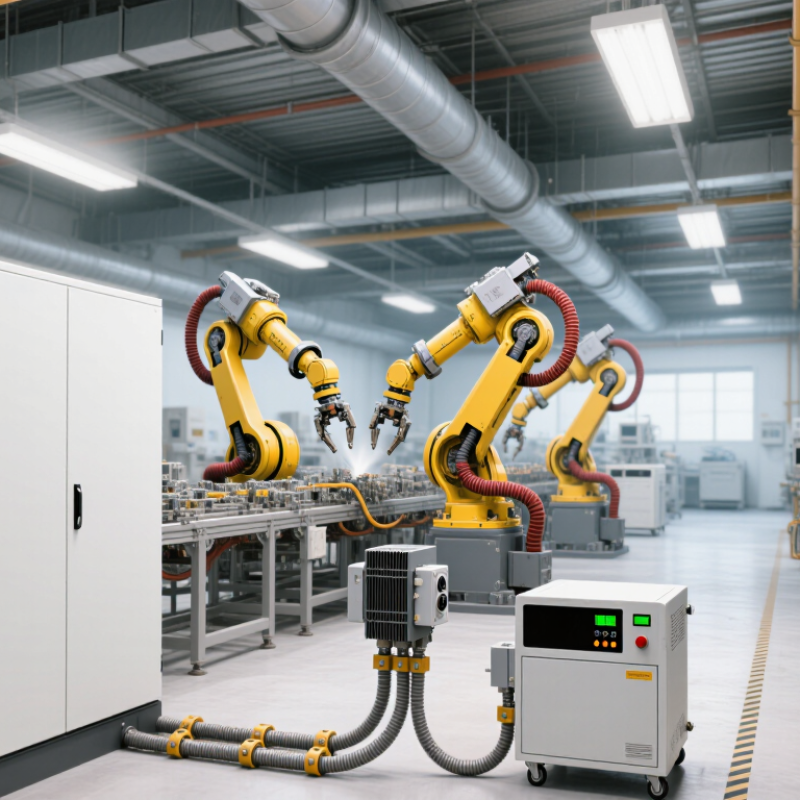
Industrial EMC Solution selection has become a practical engineering decision for global buyers. Factory robots, variable-speed drives, medical equipment, and control cabinets can all create or suffer from electromagnetic interference. A reliable solution must work beyond the laboratory. It should survive vibration, heat, dust, maintenance cycles, and changing production loads.
Henry W. Ott, a respected EMC engineer and author, stated, “EMC is not a black art; it is an engineering discipline.” His observation remains relevant. Effective control depends on measurable design choices, including grounding paths, cable routing, shielding continuity, filtering, and enclosure construction. A two-millimeter gap near a cabinet door can weaken an otherwise strong shield. A poorly terminated cable shield can also turn a careful design into an unpredictable antenna.
This guide examines leading Industrial EMC Solution options for international procurement teams. It considers filters, ferrites, shielded enclosures, grounding systems, surge protection, and pre-compliance testing. Supplier experience matters, but product data matters more. Buyers should review insertion-loss curves, operating temperature ranges, installation instructions, test conditions, and documented quality processes. Regional certification requirements also need careful verification before purchase.
No shortlist is perfect. Real installations often expose problems that simulations miss. A drive may pass testing at light load, then disturb nearby sensors during acceleration. That is why experienced engineers combine calculation, controlled testing, and field observation. The strongest solution is not always the most expensive one. It is the one that remains stable, serviceable, and technically defensible under actual operating conditions.
Top Industrial EMC Solutions for Global Buyers
Industrial EMC solutions control unwanted electromagnetic emissions and improve equipment immunity. They help machines operate reliably near motors, drives, welding systems, and wireless devices. A practical solution may include power-line filters, shielded enclosures, grounding plans, ferrite components, and carefully routed cables. Each part must match the equipment’s current, frequency, enclosure design, and operating environment.
Global buyers need these solutions because factories rarely share identical electrical conditions. A control cabinet tested in one country may face different voltage systems, grounding methods, cable lengths, or installation practices elsewhere. Regional compliance requirements also vary. Buyers should request clear test reports, technical drawings, material specifications, and installation instructions. Independent laboratory testing adds useful confidence, especially for export projects.
Small details often matter. A poorly bonded door can weaken shielding. A 30-meter motor cable can increase noise near sensor wiring. In one common failure pattern, a machine passes bench testing but resets after installation beside a variable-speed drive. Better site surveys can reveal that risk earlier. No solution is perfect. Filters may reduce noise but create heat, leakage current, or maintenance concerns. Engineers should review the complete system, not select parts from a catalogue alone. A dependable supplier explains limitations, verifies performance under realistic conditions, and supports troubleshooting when field results differ from laboratory results.
EMC standards strongly influence industrial product selection across international markets. A unit that passes one regional test may still fail another port or immunity requirement. IEC 61000-6-2 addresses industrial immunity, while IEC 61000-6-4 covers industrial emissions. These standards affect enclosure design, cable routing, grounding, and filter selection. FCC Part 15 and European harmonized requirements also shape market access decisions.
The IEC Annual Report 2023 lists more than 11,000 published international standards, showing how broad technical alignment has become. The European Commission’s 2023 Safety Gate report recorded 3,412 product alerts, reinforcing the cost of weak compliance planning.
Buyers should request complete test reports, not only certificates. They should inspect operating voltage, connector layouts, shield termination, and surge performance. A compact control cabinet can become noisy when a variable-speed drive shares an unfiltered cable path. Small details matter.
Tips: Build a market matrix before purchasing. Map each destination to its EMC limits, test method, and documentation needs. Ask suppliers for raw emissions plots and immunity test conditions. Leave design margin. Perfect global compatibility is rarely achieved on the first revision, and even experienced teams sometimes underestimate installation-specific noise.
Industrial EMC solutions work best when matched to equipment, not selected from a generic catalog. In factory commissioning, I start by identifying noise sources, cable routes, switching frequencies, and enclosure materials. A variable-frequency drive may need input and output line filters, shielded motor cables, and a carefully bonded cabinet. Sensitive measurement equipment often needs feedthrough filters, clean grounding, and physical separation from power circuits. Small details matter.
The environment changes the design. Dusty production floors call for sealed enclosures and connectors that preserve shielding after repeated maintenance. Outdoor cabinets face moisture, temperature swings, and long cable runs, so surge protection and corrosion-resistant bonding deserve attention. In medical, laboratory, or control areas, leakage current and signal integrity can restrict filter choices. For mobile equipment, vibration can loosen grounding points unless connections are mechanically secured. Testing should include normal loads, motor starts, switching events, and nearby radio transmitters.
I would not treat compliance testing as the only proof of performance. Pre-compliance scans, current probes, and near-field measurements can reveal problems before certification costs rise. Still, test results can mislead when equipment is evaluated under unusually tidy conditions. That is where engineering judgment matters. One overlooked cable opening may undo an expensive filter. Review the installation, document changes, and retest after maintenance. Perfect EMC control is rarely achieved on the first attempt. That is acceptable, if weak points are measured and corrected.
| Equipment or System | Typical EMC Disturbance | Recommended EMC Solution | Key Design Details | Suitable Environment | Common Reference Standards | Verification Methods |
|---|---|---|---|---|---|---|
| Variable-Frequency Drives and Motor Control Panels | High-frequency switching noise, conducted emissions on power cables, radiated emissions, and motor-cable common-mode currents. | Input EMC filter, DC-link or output reactor, common-mode choke, shielded motor cable, and 360-degree cable-shield termination. | Keep motor cables separated from signal wiring; bond the enclosure at high frequency; minimize cable loops; follow the drive manufacturer’s filter and cable-length limits. | Factories, process plants, machine rooms, and electrically noisy production lines. | IEC 61800-3; IEC 61000-6-2; IEC 61000-6-4. | Conducted-emission measurement, radiated-emission testing, EFT/burst, surge, ESD, and conducted-RF immunity tests. |
| Industrial PLC and Remote I/O Cabinets | Transient coupling from contactors and motors, ground-potential differences, cable-borne interference, and electrostatic discharge. | 24 V DC input filtering, surge protection, shielded I/O cables, isolated communication interfaces, and a controlled cabinet bonding system. | Separate power, analog, digital, and high-current wiring; use short bonding conductors; avoid relying on signal cable shields as protective-earth conductors. | General industrial automation, packaging lines, water treatment, and material handling systems. | IEC 61131-2; IEC 61000-6-2; IEC 61000-6-4. | I/O functional checks during EFT, surge, ESD, RF immunity, and power-frequency magnetic-field testing. |
| Industrial Power Supplies and DC Systems | Switching harmonics, differential-mode noise, common-mode leakage, input transients, and ripple coupled into control circuits. | Two-stage input filter, differential-mode inductor, common-mode choke, surge protective device, and low-noise DC output filtering. | Select components for the actual voltage, current, leakage-current, and short-circuit conditions; maintain creepage and clearance distances. | Control cabinets, telecom rooms, production equipment, and distributed automation systems. | IEC 61000-6-2; IEC 61000-6-4; IEC 61204-3; IEC 61000-3-2 where applicable. | Input-current harmonic testing, flicker assessment where applicable, conducted emissions, ripple measurement, and transient immunity testing. |
| Industrial Robots and Servo Systems | Fast PWM edges, encoder feedback errors, motor-cable radiation, regenerative braking transients, and interference between power and feedback circuits. | Shielded servo cables, ferrite or common-mode suppression, DC-bus filtering, isolated feedback interfaces, and low-impedance chassis bonding. | Route feedback cables away from motor and braking cables; use twisted pairs and proper termination; verify cable flex-life requirements for moving axes. | Automotive production, electronic assembly, machining, welding, and high-speed material handling. | IEC 61800-3; IEC 61000-6-2; IEC 61000-6-4; ISO 10218 for robot-system safety context. | Position-error monitoring during immunity tests, emission scans, encoder-integrity checks, and emergency-stop verification. |
| Industrial Ethernet and Fieldbus Equipment | Common-mode noise, ground loops, shield-current coupling, radiated RF exposure, and surge events on long outdoor or inter-building cables. | Galvanic isolation, shielded balanced cabling, appropriate surge protection, fiber-optic links for high-risk runs, and controlled grounding at cable entry points. | Use compatible cable categories and connector shielding; maintain separation from high-energy circuits; consider fiber where lightning or ground-potential differences are likely. | Large factories, substations, outdoor utilities, warehouses, and inter-building networks. | IEC 61000-6-2; IEC 61000-6-4; IEC 61158 where applicable; IEC 61000-4-5 for surge testing. | Packet-error monitoring, link-drop testing, shield-current checks, surge testing, EFT/burst, and radiated-RF immunity. |
| Measurement, Instrumentation, and Process-Control Devices | Low-level signal corruption, thermocouple or sensor drift, RF coupling, magnetic-field interference, and ground-loop errors. | Galvanic isolation, input low-pass filtering, twisted-pair shielded wiring, differential measurement, and carefully designed analog/digital ground separation. | Use shield termination appropriate to signal frequency and system grounding; prevent high-current returns from sharing sensitive measurement paths. | Process plants, laboratories, utilities, energy systems, and environmental monitoring installations. | IEC 61326-1; IEC 61000-6-2; IEC 61000-6-4; IEC 61000-4 series. | Accuracy and drift checks during ESD, RF, EFT, surge, conducted-disturbance, and magnetic-field immunity tests. |
| Welding, Induction, and High-Power Heating Equipment | High conducted and radiated emissions, rapid load changes, harmonic currents, flicker, and strong magnetic fields. | Input line reactor, harmonic mitigation, high-current EMC filtering, screened enclosures, short high-current paths, and dedicated bonding structures. | Design for thermal dissipation and fault current; coordinate filters with leakage-current limits and the facility’s power-distribution capacity. | Metal fabrication, foundries, heavy manufacturing, and high-power production areas. | CISPR 11; IEC 61000-3-2; IEC 61000-3-3 or relevant equipment-specific limits; IEC 61000-6-4 where applicable. | Harmonic and flicker measurements, conducted and radiated emissions, magnetic-field surveys, and coexistence checks with nearby control systems. |
| Outdoor Pumps, Compressors, and Utility Skids | Lightning-induced surges, long-cable coupling, motor-drive noise, moisture-related shielding degradation, and ground-potential differences. | Coordinated surge protection, weather-resistant screened enclosures, shielded power and signal cables, equipotential bonding, and fiber-optic communications where appropriate. | Coordinate protective devices by voltage and energy rating; provide short, direct earth connections and maintain enclosure ingress protection after installation. | Water and wastewater facilities, oil and gas support systems, agriculture, utilities, and remote outdoor sites. | IEC 61000-6-2; IEC 61000-6-4; IEC 61000-4-5; IEC 62305 for lightning-protection planning where applicable. | Surge testing, insulation and bonding checks, communication reliability tests, enclosure inspection, and operational testing under cable-transient conditions. |
| Medical and Laboratory Industrial Equipment | Sensitive measurement interference, leakage-current concerns, RF susceptibility, electrostatic discharge, and coupling from motors or pumps. | Low-noise power entry filter, isolated signal interfaces, shielded compartments, controlled protective bonding, and filtered ventilation openings. | EMC design must be coordinated with electrical safety, patient or operator protection, functional performance, and leakage-current requirements. | Laboratories, clean production areas, diagnostic facilities, and controlled technical rooms. | IEC 61326-1 for laboratory equipment; IEC 60601-1-2 for applicable medical electrical equipment; CISPR 11 where applicable. | Performance verification during ESD, RF immunity, EFT, surge, conducted RF, emissions, and power-frequency magnetic-field testing. |

Selection note: Final EMC requirements depend on the equipment category, installation environment, power system, cable configuration, operating modes, and applicable regional regulations. The standards listed above should be confirmed against the current edition and the product’s specific conformity route.
Global Industrial EMC Solutions: How to Evaluate Suppliers, Testing, Certifications, and Support
Choosing an EMC supplier requires more than comparing prices. Examine its testing experience across your product category and operating environment. Ask whether engineers can explain conducted emissions, radiated emissions, immunity, and grounding risks clearly. A reliable supplier should provide test plans, calibration records, and traceable measurement data. Request sample reports with confidential details removed. Vague answers often signal weak process control.
Certifications must match your target markets and product type. Check laboratory accreditation, applicable standards, certificate validity, and testing scope. Do not accept a certificate without reviewing its conditions. A product may pass one configuration but fail after a cable, enclosure, or firmware change. Supplier support also matters. During evaluation, ask about design reviews, pre-compliance testing, corrective actions, and response times. In real projects, delayed technical advice can cost more than the test itself. I have seen teams focus heavily on certificates and overlook practical installation guidance.
Tips: Visit the test facility when possible. Check chamber maintenance and equipment calibration dates. Request a clear quotation with retest fees included. Confirm who owns the test data. Ask for support in your working language and time zone. Keep one technical contact on both sides. Do not rely on marketing claims alone. A supplier may appear highly experienced, yet still lack knowledge of your application. Leave room for doubt, and verify important details in writing.
Top Industrial EMC Solutions for Global Buyers?
Installation should begin with the machine layout, not the filter catalogue. Separate noisy drives from sensitive control cables. Keep power and signal wiring crossing at right angles. Bond doors, panels, and cable trays with short, wide connections. IEC 61000-4-4 specifies industrial test levels of 2 kV on power ports and 1 kV on signal ports. These values are practical design targets, not decorative numbers. During commissioning, record cable routes, bonding points, filter locations, and grounding resistance. Photographs help maintenance teams find hidden changes later.
Maintenance must treat EMC as a living condition. Check shield terminations after vibration, repainting, and cabinet modifications. Inspect loose bonding straps and damaged cable glands during scheduled shutdowns. The 2024 Uptime Institute Global Data Center Survey reported that about 54% of respondents experienced an outage within three years. Industrial plants face different loads, but the lesson is similar: small power-quality weaknesses can become expensive interruptions. Thermal scans and portable power-quality measurements can reveal problems before alarms appear.
Long-term performance needs repeatable testing. Compare emissions and immunity results against the original commissioning record. Re-test after adding variable-speed drives, wireless equipment, or larger motors. IEC 61000-4-2 defines 8 kV contact and 15 kV air-discharge tests, showing how severe static events can be. A perfect installation is a useful myth. Field teams sometimes overlook a painted bonding surface or an improvised cable loop. Those mistakes deserve documentation, correction, and honest review.
A practical planning baseline for maintaining EMC performance in industrial installations. Shorter intervals are used for controls that can degrade quickly because of vibration, corrosion, contamination, or cable movement. Actual intervals should be adjusted according to the site risk assessment, operating environment, and applicable EMC standards.
The intervals shown are planning recommendations rather than mandatory certification requirements. Verify protective earth continuity, bonding, shield termination, enclosure integrity, filter condition, and noise levels after major equipment changes or abnormal events.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.