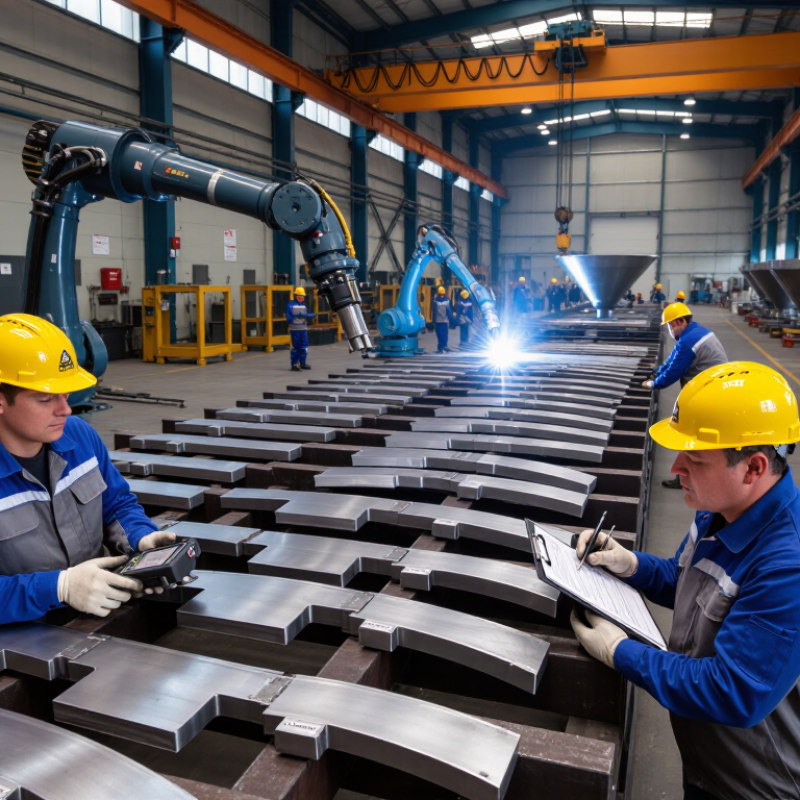
Choosing among the top chromium carbide wear plate manufacturers requires more than comparing prices or catalog photographs. These plates protect equipment exposed to severe abrasion, impact, heat, and sliding wear. Mining chutes, cement conveyors, steel hoppers, and dredging systems all create different service conditions. A reputable manufacturer should explain its alloy chemistry, overlay hardness, deposition method, plate thickness, and expected wear life. Clear technical documents matter.
Real-world experience also reveals details that brochures may omit. Ask how the chromium carbide wear plate is cut, formed, welded, and inspected after production. Check whether the supplier provides batch records, hardness results, dimensional tolerances, and traceable quality certificates. Factory capability should match the project scale. A small repair panel needs different support from a complete processing line.
Look closely.
Reliable manufacturers usually discuss failure risks rather than promise unlimited durability. They should recommend practical testing, including field measurements and operating-temperature reviews. Independent inspection can strengthen confidence when downtime costs are high. Customer references are useful, but they must reflect similar materials, impact levels, and maintenance practices. Otherwise, comparisons become misleading.
No ranking is perfect. Manufacturer performance can vary by region, application, and production batch. Some suppliers have impressive engineering teams but limited delivery capacity. Others offer attractive prices but weaker documentation. This guide compares technical expertise, manufacturing consistency, customization, service response, and verified application experience. The goal is not to name a universal winner. It is to help buyers ask sharper questions and select a wear solution that performs reliably in actual working conditions.
Global demand for chromium carbide wear plates follows industries that move abrasive materials every day. Mining chutes, crusher liners, conveyor transfer points, and bucket surfaces face constant impact and sliding wear. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023. This scale supports steady demand for longer-lasting maintenance materials.
Cement plants are another major user. The U.S. Geological Survey estimated global cement production at roughly 4.1 billion tonnes in 2023. Raw mills, clinker conveyors, and separator components often suffer from hard mineral abrasion. Chromium carbide overlay plates combine a tough steel backing with a carbide-rich surface, commonly reaching approximately 55–65 HRC. They can reduce replacement frequency, but performance depends on welding quality, plate thickness, and operating temperature.
Recycling, power generation, and bulk material handling also use these plates. Grand View Research identifies expanding industrial maintenance and material-handling activity as important drivers for wear-resistant steel demand. However, published market figures rarely isolate chromium carbide plates from other abrasion-resistant products. That limitation matters. A harder surface is not always better; severe impact can cause cracking or premature failure. Field inspection, abrasive testing, and accurate application data remain essential when comparing manufacturers and selecting a plate for global operating conditions.
Top Chromium Carbide Wear Plate Manufacturers?
Chromium carbide overlay plates typically reach 55–65 HRC through controlled welding and rapid solidification. Chromium and carbon form hard carbide particles inside a tougher iron-based matrix. The base steel supports impact, while the overlay resists abrasion from rock, coal, sand, and mineral fines. Hardness readings can vary across the surface. They should not be treated as absolute values.
Experienced manufacturers control dilution, welding speed, heat input, and overlay thickness. These details influence carbide distribution and cracking behavior. Small stress-relief cracks may appear in the deposit. They can be acceptable in abrasion service, but excessive cracking may indicate poor process control. Quality checks should include hardness mapping, thickness measurement, visual inspection, and, when needed, metallographic testing. A reliable supplier should explain test locations and methods clearly, not only publish a maximum hardness figure.
Tips: Ask for hardness ranges, not isolated results. Check whether readings cover the full plate. Confirm the base steel grade and overlay thickness. Match the plate to the wear pattern, because extreme hardness alone cannot solve impact damage. Compare real production samples when possible. My view is cautious: laboratory hardness may exceed field performance. Installation, support spacing, heat, and particle shape can change service life significantly.
Chromium carbide overlay deposits are commonly specified at approximately 55–65 HRC. This high hardness is produced by chromium-rich carbide phases dispersed in a tougher iron-based matrix. Actual results vary with alloy chemistry, deposition parameters, cooling conditions, plate thickness, and hardness-testing method.
Top chromium carbide wear plate manufacturers should be compared through chemistry, thickness control, and verified production capacity.
Global crude steel output reached about 1.892 billion tonnes in 2023, according to the World Steel Association. That scale supports strong demand from mining, cement, recycling, and bulk-material handling.
Overlay chemistry is the practical separator.
Industrial plates commonly contain about 20–35% chromium and 4–6% carbon. Their deposited layers often measure 58–65 HRC, although hardness alone can mislead. A capable producer should provide spectrometer results, dilution data, and weld-bead inspection records. ASTM G65 testing is useful for comparing abrasive wear resistance, but field conditions still change performance.
Thickness deserves equal attention.
Typical overlay thickness ranges from 3 to 20 millimeters, with base plates commonly measuring 6 to 30 millimeters. The best suppliers control cracking patterns, flatness, and heat distortion across large panels. Some buyers overlook this detail. They should not.
Production capacity must mean more than a large factory photograph.
Request documented monthly output, maximum plate width, furnace availability, and recent delivery records. Capacity claims are rarely comparable between manufacturers. A better assessment combines audited production data, batch traceability, and realistic lead times. Industry market reports can describe demand growth, yet they seldom verify individual plant capability. That gap requires careful questioning, and sometimes a second technical audit.
Choosing top chromium carbide wear plate manufacturers requires more than comparing hardness numbers. In field inspections, abrasion loss often reveals the real difference. A plate may show excellent laboratory results yet wear unevenly under wet ore, sharp rock, or repeated impact. Carbide volume, distribution, weld quality, and base-plate toughness all matter. Hardness alone is not enough.
Test the actual duty cycle.
Measure thickness at fixed points before installation. Repeat the readings after a defined tonnage or operating period. This produces a more useful abrasion rate than a supplier’s isolated test result. A well-made plate can retain a stable surface while its softer substrate supports impact. However, excessive carbide concentration may increase cracking risk during cutting or welding. That trade-off is easy to overlook. I have seen premature failures caused by poor fit-up, not weak metallurgy.
Service life should be compared with total cost, not purchase price. A thinner plate may cost less initially, but frequent shutdowns, lifting work, and replacement labor can quickly reverse the saving. Estimate cost per operating hour or cost per processed tonne. Include transport and installation time. Ask for traceable inspection records, dimensional tolerances, deposit chemistry, and recommended welding procedures. These details support reliable decisions. Still, no chart predicts every site. Material moisture, impact angle, temperature, and operator practice can alter results. Field feedback should challenge the original specification when performance falls short.
Selecting top chromium carbide wear plate manufacturers requires more than comparing hardness values. The USGS Mineral Commodity Summaries 2024 estimated global chromite mine production at about 41 million metric tons in 2023. This scale makes raw material traceability important. Buyers should request heat numbers, chemical analysis, and production records. Chromium content alone does not prove service life.
Testing must reflect the actual failure mode. ASTM G65 dry-sand rubber-wheel testing measures abrasive mass loss under controlled conditions. ASTM G99 pin-on-disk testing can compare sliding wear, but it may not represent impact loading. Hardness should be checked using ISO 6507 or an equivalent method. Ask for carbide volume fraction, matrix hardness, overlay thickness, dilution, and heat-affected-zone data. Small test coupons are useful. They are not the whole plate.
Field experience suggests that consistent welding quality often matters as much as nominal chemistry. Inspectors should examine cracks, porosity, flatness, and overlay uniformity across several locations. A certificate without raw test values deserves caution. I would also compare samples after cutting and bending, because plates can look excellent before fabrication. Higher hardness is not automatically better. Brittle overlays may fail under impact, and this is where some evaluations become too simplistic.
| Evaluation Dimension | What to Check | Relevant Standard or Reference | Typical Testing or Verification Method | Buyer Acceptance Guidance | Required Supplier Evidence |
|---|---|---|---|---|---|
| Overlay Chemistry | Chromium, carbon, manganese, silicon, and iron balance in the deposited hardfacing layer. | Product specification, welding procedure, and agreed chemical analysis limits. No single universal chemistry applies to every chromium carbide overlay plate. | Optical emission spectroscopy, X-ray fluorescence, or an equivalent laboratory method performed on representative overlay samples. | Confirm that the chemistry matches the agreed grade and intended wear mechanism, especially abrasive wear and elevated-temperature service. | Heat or batch chemical report, sampling plan, and traceability records. |
| Carbide Microstructure | Distribution, morphology, continuity, and orientation of chromium-rich carbides within the iron-based matrix. | Metallographic acceptance criteria defined in the purchase specification or approved reference sample. | Cross-section preparation followed by optical microscopy or scanning electron microscopy. Image analysis may be used for carbide spacing and area fraction. | Look for a reasonably uniform carbide network without excessive segregation, porosity, unmelted particles, or abnormal cracking. | Metallographic report with etched micrographs, sample location, magnification, and evaluation date. |
| Hardness | Surface hardness of the overlay and, where relevant, hardness through the overlay thickness and in the base plate. | ASTM E18 for Rockwell testing, ASTM E384 or ISO 6507 for microhardness, depending on the approved method and material thickness. | Multiple hardness readings taken from cleaned, representative locations; indents should avoid visible cracks and edges. | Use the contract range rather than a generic number. Chromium carbide overlays commonly have very high hardness, but hardness alone does not predict service life. | Hardness map, test load, scale, number of readings, calibration status, and sampling location. |
| Abrasive Wear Resistance | Resistance to sliding or three-body abrasion under controlled conditions. | ASTM G65 dry sand/rubber wheel abrasion is widely used for comparative evaluation of hardfacing materials. | Measure mass loss or volume loss after exposure to specified abrasive, load, wheel condition, speed, and test duration. | Compare only results generated using the same ASTM G65 procedure, test severity, and reporting units. Lower mass or volume loss indicates better laboratory abrasion resistance. | Complete test report, specimen orientation, test procedure, abrasive details, raw mass data, and calibration records. |
| Impact and Gouging Performance | Ability of the overlay and substrate system to withstand impact, deformation, and localized gouging. | No single wear test represents every field condition; an application-specific qualification test is normally required. | Instrumented impact testing, laboratory gouging tests, or controlled field trials using representative impact energy and material feed conditions. | Prioritize a balanced overlay/substrate design. Extremely hard deposits can be unsuitable where repeated impact or severe bending dominates. | Application test protocol, failure photographs, impact energy, operating conditions, and performance comparison against the approved reference. |
| Crack Pattern | Presence, spacing, width, depth, and orientation of stress-relief cracks in the overlay. | Acceptance limits must be stated in the purchase specification because stress-relief cracking can be normal in many hardfacing products. | Visual inspection, dye penetrant testing where appropriate, dimensional measurement, and cross-sectional examination for crack depth. | Do not reject all cracks automatically. Reject cracks that exceed agreed limits, reach the substrate, form interconnected defects, or create unacceptable structural risk. | Inspection standard, crack map, photographs, crack-size limits, and disposition procedure for nonconforming areas. |
| Bond Integrity | Fusion between the hardfacing layer and base plate, including lack of fusion, delamination, and inclusions. | Acceptance criteria should be agreed before production; the applicable welding or surfacing procedure should define essential variables. | Metallographic cross-sections, ultrasonic testing where suitable, dye penetrant testing for surface-connected defects, and visual inspection. | Require continuous metallurgical bonding in critical areas and clearly defined limits for discontinuities, edge defects, and repair zones. | Cross-sectional records, NDT reports, welding procedure qualification, and repair documentation. |
| Dimensional Accuracy | Overall length, width, thickness, overlay thickness, flatness, squareness, and hole or cutout locations. | Approved drawings, tolerances in the purchase order, and agreed measurement procedures. | Calibrated steel rule, caliper, micrometer, laser measurement, straightedge, or coordinate measurement equipment as appropriate. | Specify whether dimensions are measured before or after cutting, forming, machining, or stress-relief distortion. | Dimensional inspection report, equipment calibration certificates, and marked-up inspection drawing. |
| Flatness and Distortion | Plate bow, twist, edge lift, and distortion caused by thermal deposition. | Project drawing or purchase specification; a universal flatness tolerance is not applicable to every plate format. | Straightedge and feeler gauge, surface table, laser scan, or other documented method over the specified measurement length. | Set limits based on installation method and whether the plate will be rolled, formed, bolted, or welded after delivery. | Flatness map, measurement grid, correction records, and final inspection approval. |
| Base Plate Quality | Base metal grade, thickness, lamination condition, weldability, and mechanical properties. | Material standard stated in the purchase order, such as the applicable carbon steel or alloy steel specification. | Mill test certificate review, thickness measurement, visual inspection, ultrasonic examination for laminations where required, and mechanical testing when specified. | Ensure the substrate is suitable for the intended welding, forming, temperature, and structural requirements rather than evaluating the overlay alone. | Mill certificate, heat number, chemical composition, mechanical properties, and supplementary NDT results. |
| Welding and Surfacing Procedure | Process, consumable classification, preheat, interpass temperature, travel speed, deposition sequence, and cooling control. | EN 14700 may be used for hardfacing welding consumables; qualification requirements should be defined by the project specification and applicable welding code. | Procedure review, qualification coupon testing, welder or operator qualification where applicable, and production parameter monitoring. | Require controlled essential variables and documented repair procedures. Verify that production practice matches the qualified procedure. | Welding procedure specification, qualification record, consumable certificates, parameter logs, and operator qualifications. |
| Temperature Capability | Retention of wear performance, dimensional stability, and bond integrity at the actual operating temperature. | Application-specific qualification is necessary; room-temperature hardness or abrasion data cannot establish high-temperature performance by itself. | Elevated-temperature hardness, thermal cycling, oxidation evaluation, and wear testing at the specified service temperature. | Confirm maximum continuous and intermittent temperature, atmosphere, thermal cycling frequency, and cooling conditions. | Temperature-specific test report, service limitations, and recommended operating envelope. |
| Cutting and Fabrication Suitability | Recommended cutting process, heat-affected zone, edge cracking, drilling method, and minimum bend radius. | Manufacturer’s fabrication procedure and project-specific fabrication requirements. | Trial cutting, edge inspection, bend trial where required, and dimensional verification after fabrication. | Confirm that the plate can be cut and installed using the buyer’s available equipment without damaging the substrate or overlay. | Cutting guide, forming limits, drilling recommendations, repair instructions, and fabrication test results. |
| Traceability and Quality System | Ability to trace finished plates to raw materials, welding consumables, production parameters, inspections, and shipment records. | ISO 9001 certification can support process control, but certification does not replace product-specific inspection requirements. | Document review and audit of heat numbers, batch records, inspection reports, nonconformance reports, and corrective actions. | Require full traceability for critical applications and verify that certificates correspond to the delivered plate identification. | Quality manual, certificate of conformity, batch record, inspection and test plan, and nonconformance history. |
| Application Fit | Compatibility with the dominant wear mode: sliding abrasion, impact, gouging, erosion, corrosion-assisted wear, or high temperature. | Engineering selection based on actual operating conditions rather than a single hardness or chromium percentage. | Review of particle size and hardness, impact energy, material flow, temperature, corrosion environment, plate support, and expected service life. | Select the product using field conditions and total cost of ownership, including installation, downtime, repairs, and replacement frequency. | Application references without confidential brand claims, wear-life data, design calculations, and service recommendations. |
| Commercial Evaluation | Price per usable area, lead time, minimum order quantity, packaging, warranty, replacement policy, and technical support. | Contract terms, inspection and test plan, agreed Incoterms, delivery schedule, and warranty conditions. | Supplier quotation comparison, sample approval, reference checks, pre-shipment inspection, and review of historical delivery performance. | Compare total delivered cost and expected service life rather than purchase price alone. | Formal quotation, delivery commitment, warranty terms, packing specification, technical datasheet, and after-sales procedure. |

Note: Chromium carbide overlay plates are application-specific products. Test values, hardness ranges, crack-pattern limits, dimensions, and acceptance criteria should be agreed in the purchase specification before production. Laboratory wear results are comparative and should not be treated as a universal prediction of field service life.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.