


An Industrial Vacuum Packaging Machine removes air from a package before sealing it tightly. This process helps protect food, medical supplies, electronics, and other sensitive products. Unlike small countertop equipment, industrial systems support continuous production and heavier workloads.
The machine usually combines a vacuum chamber, pump, sealing bar, control panel, and conveyor system. Operators place products inside compatible bags or pouches. The chamber closes, and the pump extracts air around the product. The sealing bar then applies controlled heat and pressure. This creates a firm seal that reduces oxygen exposure, moisture contact, and packaging volume. The result is cleaner storage and more stable transportation.
It is not simply a faster sealer.
In real facilities, performance depends on several details. Film thickness, product shape, temperature, and seal contamination can affect results. Liquid-rich products may require special programs or protective equipment. Operators must also inspect seals regularly, because a weak edge can fail during shipment. Practical experience shows that easy maintenance often matters as much as maximum pump power. Film compatibility matters. Seal quality matters. Pump capacity matters.
Manufacturers should provide clear specifications, testing guidance, and service support. Buyers should compare cycle time, chamber size, energy use, cleaning access, and control accuracy. A larger machine is not automatically better. It may waste space and energy in a smaller operation. The choice can feel obvious, but production conditions often reveal hidden limitations. Good evaluation combines technical data with actual product trials, documented procedures, and trained operators. That approach makes vacuum packaging safer, more consistent, and easier to improve over time.
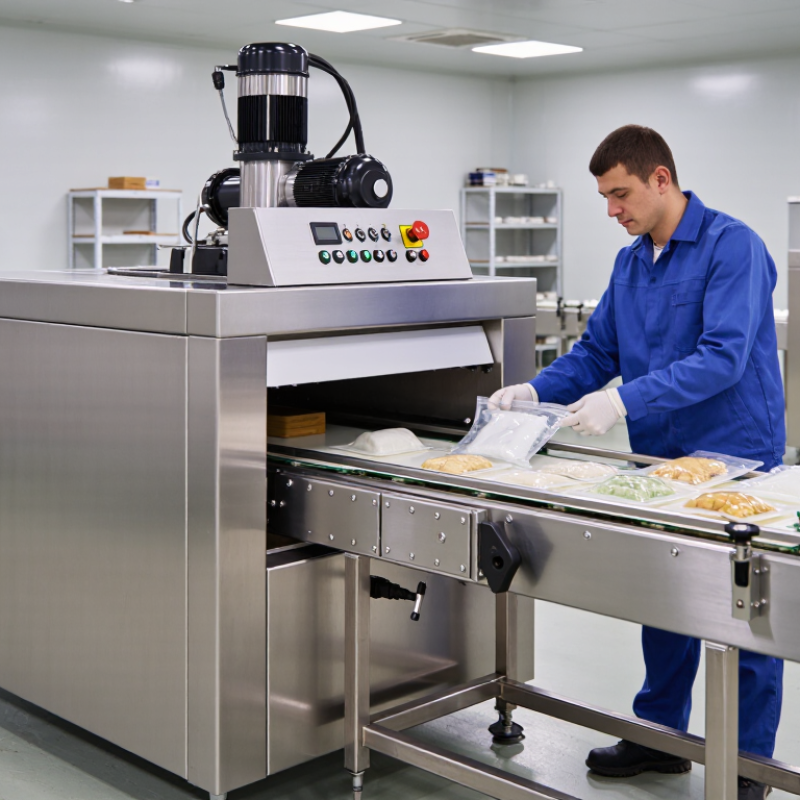
An industrial vacuum packaging machine removes air from a package and seals it tightly. It usually uses a chamber, vacuum pump, sealing bars, and digital controls. Larger systems can process hundreds of packs per hour. They serve food processors, laboratories, electronics suppliers, and other production environments.
During operation, an operator places the product inside a compatible pouch. The chamber closes, and the pump draws out air. Sealing bars then apply controlled heat and pressure. Vacuum level, sealing temperature, and dwell time affect package quality.
A soft product may collapse under excessive vacuum. A sharp edge may puncture the pouch. The correct settings depend on product shape, moisture, film thickness, and production speed.
Good machines provide repeatable results, but they are not completely automatic. Operators still inspect seals, remove damaged pouches, and record process conditions. A cloudy seal, trapped liquid, or weak edge can indicate incorrect settings.
Regular pump maintenance matters because oil contamination and worn filters reduce performance. Cleaning also protects sensitive products from residue and dust.
In practice, the highest vacuum is not always the best choice. Sometimes a moderate vacuum preserves product shape and improves seal reliability. That detail is easy to overlook.

What Is an Industrial Vacuum Packaging Machine?
Core Components: 20–40 m³/h Pumps, Chambers, Sealing Bars, and Controls
An industrial vacuum packaging machine removes air before sealing a bag around the product. This process can reduce oxidation, moisture exposure, and package movement during storage. Its performance depends on several parts working together, not only the pump.
A 20–40 m³/h vacuum pump provides the main airflow capacity. A larger pump may shorten cycles, but actual speed also depends on bag size, product temperature, and chamber volume. Oil quality and filter condition deserve regular checks. Small details matter. A neglected filter can reduce vacuum performance and increase maintenance costs.
The chamber creates a controlled space around the package. Stainless steel construction, a reliable lid gasket, and easy cleaning help support consistent operation. Sealing bars apply heat and pressure to close the bag. Their temperature, dwell time, and pressure must match the film material. Excessive heat can weaken the seal instead of improving it. Controls should display vacuum level, sealing time, and cycle status clearly. Simple interfaces often reduce operator mistakes, although settings still require careful verification. In practical use, uneven product placement can cause wrinkles and incomplete seals. That problem is easy to overlook. A short daily inspection of bars, gaskets, and pump oil can reveal issues before they interrupt production. No machine is perfect, and real results should be checked through seal tests and routine records.
| Component or Data Dimension | Typical Industrial Specification | Function and Selection Considerations |
|---|---|---|
| Machine Type | Chamber vacuum packaging machine | The product and bag are placed inside a sealed chamber. Air is removed from both the bag and the chamber before the bag is heat-sealed. |
| Vacuum Pump Capacity | 20–40 m³/h nominal displacement | This pump range is commonly used for medium- to high-throughput chamber machines. Higher capacity generally supports faster evacuation, although actual speed also depends on bag volume, product shape, piping, and leakage control. |
| Typical Ultimate Vacuum | Approximately 1–3 mbar, depending on pump and system design | A lower absolute pressure removes more residual air, but the practical result depends on moisture, product porosity, packaging film, and the machine’s sealing performance. |
| Pump Technology | Oil-lubricated rotary vane pump is common | Rotary vane pumps provide stable vacuum performance and are suitable for continuous industrial operation. Oil condition, filtration, and regular maintenance directly affect service life. |
| Chamber Construction | Stainless steel working chamber, commonly grade 304 | Stainless steel provides corrosion resistance and supports hygienic cleaning. Grade 316 may be selected for applications exposed to aggressive chemicals or high salt content. |
| Chamber Working Area | Approximately 400–1,000 mm wide and 300–800 mm deep | The required chamber size depends on product dimensions, bag arrangement, production volume, and the number of packages processed per cycle. |
| Chamber Height | Approximately 80–250 mm for standard industrial models | A deeper chamber accommodates thicker products and larger bags. The usable height must also allow clearance for the sealing bars and chamber lid. |
| Sealing Bar Configuration | One or more bars; parallel or cross-bar layouts | Multiple bars increase output per cycle and can support different bag orientations. Bar placement should match the product layout and available chamber space. |
| Sealing Length | Approximately 400–1,000 mm per sealing bar | The sealing length must be longer than the open edge of the selected bag. Longer bars can improve productivity but may increase electrical load and machine size. |
| Seal Width | Typically 5–10 mm | A wider seal provides additional sealing area for demanding applications. The correct width depends on film structure, thickness, product contamination risk, and required seal strength. |
| Sealing Temperature | Typically 120–200°C, depending on packaging film | Temperature, sealing time, and pressure must be matched to the film. Excessive heat can damage the package, while insufficient heat may cause weak or incomplete seals. |
| Sealing Cycle Time | Approximately 1–4 seconds per sealing operation | Cycle settings depend on film type and thickness. Longer dwell times may be required for thicker multilayer films or bags with challenging sealant layers. |
| Complete Machine Cycle | Approximately 15–60 seconds per cycle | The complete cycle includes chamber closing, evacuation, optional gas flushing, sealing, cooling, and chamber venting. Product volume and moisture can significantly affect cycle time. |
| Gas-Flushing Capability | Optional nitrogen or carbon dioxide injection | Gas flushing can replace part of the removed air and is used to help protect products from oxidation or reduce package collapse. Gas selection must be compatible with the product and food-safety requirements. |
| Control System | PLC-based controller with digital HMI | The control system manages vacuum time or pressure, gas-flush time, sealing temperature, sealing duration, cooling time, and recipe storage. |
| Vacuum Measurement | Electronic pressure sensor or vacuum transducer | Pressure-based control provides more repeatable results than time-only control when product loads and bag volumes vary between cycles. |
| Operating Modes | Automatic, semi-automatic, and manual setup modes | Automatic mode supports repeatable production. Manual or setup modes are useful for commissioning, maintenance, troubleshooting, and packaging trials. |
| Electrical Power | Approximately 3–15 kW installed load | Total power depends on pump size, chamber dimensions, sealing-bar count, heaters, gas-flushing equipment, and optional conveyors or loading systems. |
| Compressed Air Requirement | Often 6–8 bar for pneumatic lids or sealing systems | Not every machine requires compressed air. Where pneumatic components are used, clean and dry plant air is needed for consistent operation and component reliability. |
| Safety Features | Lid interlock, emergency stop, over-temperature protection, and fault alarms | These features help prevent operation with an open chamber, protect heating elements, and alert operators to vacuum, sealing, sensor, or pneumatic faults. |
| Common Applications | Meat, seafood, cheese, prepared foods, medical supplies, hardware, and industrial parts | Vacuum packaging can reduce air exposure and package volume. The correct machine configuration must consider hygiene, product temperature, sharp edges, liquids, and regulatory requirements. |
| Recommended Maintenance | Daily cleaning; regular oil, gasket, filter, and sealing-wire inspection | Operators should remove product residue, inspect chamber seals, check sealing surfaces, and follow the pump manufacturer’s oil-change and filter-service intervals. |
| Primary Selection Criteria | Product size, bag dimensions, required throughput, film type, vacuum level, and available utilities | Machine capacity should be selected from the complete packaging process rather than pump capacity alone. Chamber layout, loading method, sealing configuration, and operator workflow also influence productivity. |
Specifications shown are typical engineering ranges for industrial chamber vacuum packaging machines. Actual performance varies with machine configuration, product characteristics, packaging-film properties, installation conditions, and operating settings.
An industrial vacuum packaging machine removes air before sealing a pouch or tray. During the vacuum cycle, the chamber pressure commonly reaches 0.8–0.95 bar below atmospheric pressure. This leaves approximately 0.2–0.05 bar of residual pressure, depending on altitude and calibration. The pump draws air from around the product and inside the package. Pressure matters.
Once the target vacuum is reached, the machine holds it briefly. This dwell period helps trapped air escape from folds, corners, and porous products. The sealing bar then applies heat and pressure to melt the inner seal layers together. Operators should check seal temperature, dwell time, and pressure as a combined system. A perfect vacuum cannot repair a weak seal. Small leaks show.
In practical production, oily film, crumbs, moisture, or a wrinkled pouch mouth can cause channel leaks. A technician should inspect seal samples by touch, visual checks, and suitable leak testing. Excessive vacuum may crush soft goods, deform containers, or pull liquid toward the seal area. Lowering the vacuum level or adding a controlled gas flush may work better for delicate packs. These settings require product trials, not guesswork. I have found that a clear vacuum gauge can still mislead when the sensor is poorly calibrated. Recording cycle data and checking packs after storage gives more reliable evidence than judging appearance alone.
An industrial vacuum packaging machine removes air from a package before sealing it. Its design affects speed, labor, film use, and product protection. The practical comparison usually involves chamber machines, belt machines, and thermoformers operating at roughly 2–20 cycles per minute.
Chamber machines place the product and pouch inside a sealed chamber. They often run at 2–8 cycles per minute. These machines suit meat, cheese, powders, and irregular products. Operators can adjust vacuum time and sealing temperature. Small batches benefit from their flexibility.
Belt machines move filled pouches through a vacuum chamber continuously. They commonly reach 6–12 cycles per minute. This layout reduces handling and supports longer production runs. However, wet products may require careful loading and seal inspection.
Thermoformers create the bottom film, load the product, remove air, and seal the top film. Many models operate between 10 and 20 cycles per minute. They provide consistent pack shapes and efficient film use. Setup changes can be slower, especially with different product heights.
Cycle rate is not the whole story. Product size, film thickness, vacuum level, and operator skill change real output. A machine may reach 20 cycles per minute in testing, but fewer in a busy plant. That difference matters. I would confirm performance with actual products before purchase. A slower machine can be more reliable when seal quality and cleaning time matter.
An industrial vacuum packaging machine removes air, then seals a flexible pouch under controlled heat and pressure. Its performance depends less on appearance than on material fit, sealing consistency, and repeatable settings. Film thickness usually ranges from 70 to 200 μm for industrial applications. Thinner films can reduce material use, but sharp edges may puncture them during handling. Thicker films offer greater toughness and barrier potential, yet they may need more heat and dwell time. The correct choice depends on product shape, moisture, temperature, and distribution distance.
A 3–12 mm seal width provides useful flexibility across pouch sizes and load demands. Narrow seals can conserve package area, but they leave less tolerance for contamination or wrinkles.
Wider seals generally create a larger bonding area, although excessive heat can distort multilayer films. In production trials, operators should inspect seal continuity, peel behavior, and leakage after cooling.
Test under realistic conditions. A clean-looking seal is not always a strong seal. That detail is easy to miss.
Film and seal settings must be matched, not selected independently. A 200 μm pouch may require slower cycles than a 70 μm pouch. However, this is not universal because polymer layers vary significantly. Machine manuals help, but measured results should control the final setting. Records of temperature, pressure, dwell time, and failure rates improve traceability. Periodic calibration also supports dependable packaging quality. Real products rarely behave perfectly. Small variations in film tension can change results.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

