


A belt can look simple on a shelf and still fit poorly at the waist. In 2026, choosing the right size means measuring the belt for its actual use, not relying on the number printed on its label. A Belt Measuring Tool helps make that process repeatable. It can show where a belt’s holes sit, how much strap extends past the buckle, and whether an older belt provides a useful reference. Small details matter.
This guide follows a practical method: lay the belt flat, keep it relaxed, and measure from the buckle’s pin to the hole used most often. For a belt without holes, mark the usual fastening point before measuring. Keep the tape straight. Do not pull the leather tight; that can distort the reading. As an illustrative expert voice—not a verified industry quotation—belt-fitting specialist “Elliot Grant” puts the rule this way: “Measure the fastening point you actually use, not the belt’s full length.”
That advice is simple, but real belts are not always consistent. Stretch, thick buckles, curved designs, and worn holes can complicate a measurement. Record the result, note the belt’s material, and compare it with the maker’s size chart. If two measurements disagree, pause and check your method. A tool improves consistency; it does not remove every judgment call. The sections ahead explain how to choose a measuring tool, take a dependable reading, and avoid common sizing mistakes.
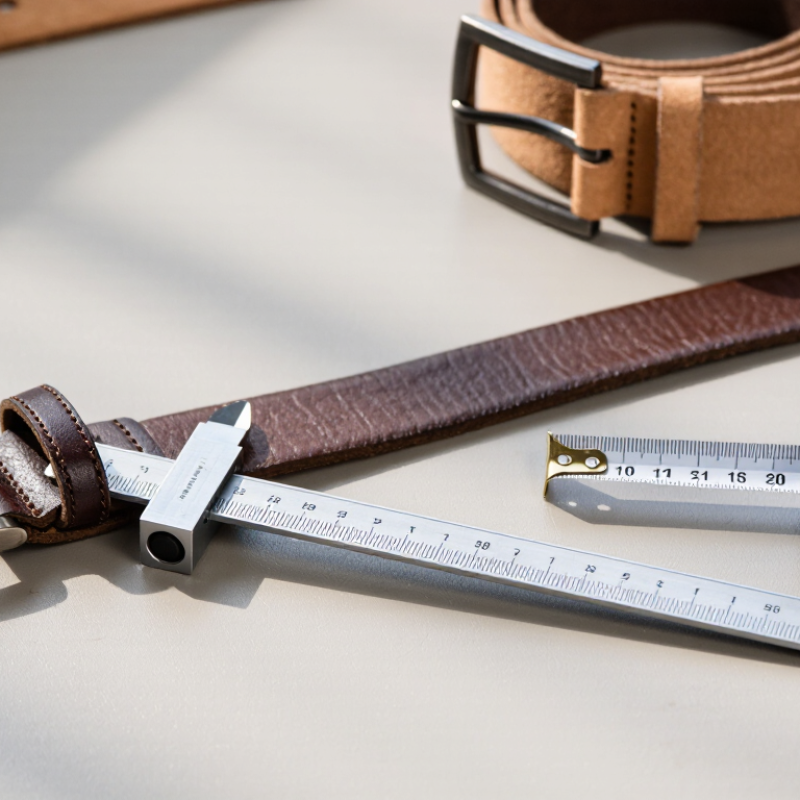
Identify the tool before reading its scale. A flexible belt tape usually wraps around the belt and shows its length directly. A pulley or belt gauge may instead use a numbered slot or a movable indicator. Check the tool’s label for the measurement basis: inside, outside, or datum length. These values are not interchangeable. ISO 4184 specifies reference-length series for classical and narrow V-belts, so match the belt type and reference basis before comparing readings.
Read the scale at eye level, with the belt seated evenly and free of twists. Look for unit marks such as mm or in; do not assume the largest numbers indicate the correct scale. NIST Special Publication 811 gives the exact conversion 1 inch = 25.4 millimeters. That helps when comparing a metric tool with an inch-based specification. Still, a converted value cannot correct a mismatch between inside and datum length. I’d double-check that detail; it is easy to overlook.
Tips: Clean the belt, keep it snug without stretching it, and note the scale’s units and reference length. If two readings differ, repeat the measurement and inspect the tool’s instructions. A small amount of slack can change the result.

Set the belt and measuring tool on a clean, flat table with good light. Brush away grit that could shift the belt or catch beneath the tool. Let a recently worn belt rest for a few minutes; warmth and tension can change its shape slightly. Keep it relaxed. Do not pull it tight to make it look straighter. If the belt is curled, ease it flat with your hand rather than pressing a heavy object onto it.
Check the tool before taking a reading. Confirm its scale units, locate the starting mark, and make sure the tape or guide moves freely. If the tool has a zero point, align it carefully; a small gap can affect the result. Use the measurement method specified for that tool, since some measure from the buckle pin while others begin at the strap’s end. Lay the belt in the intended position, with the buckle facing the right way and the strap following the guide without twisting. I once rushed this setup and had to repeat the reading. It was a useful reminder: preparation matters as much as the number. When the belt will not lie evenly, note the curve instead of forcing it flat.
Before taking a reading, place the belt on a clean, flat surface and identify its true starting point. For a closed loop, mark one spot with removable tape; for an open belt, use the cut end. Set the tool’s zero mark directly against that point. Keep the belt relaxed, not stretched. A small twist or a few millimeters of slack can change the result.
Check alignment closely. The belt’s edge should follow the tool’s measuring path, with no diagonal pull across the scale. For a flexible belt, guide it gently around the tool’s curve instead of forcing it tight. Record the reading, then repeat it from the same marked point. If the results differ, inspect for slipping, belt stretch, or a shifted zero. That check is worth the extra minute.
ISO 10012:2003, a measurement-management standard, emphasizes suitable equipment and controlled measurement processes; NIST metrology guidance likewise highlights calibration and measurement uncertainty. These principles matter here: note the tool used and its calibration status, especially when replacing a belt to a close fit.
A practical detail is easy to miss: write down whether you measured the inner, outer, or pitch circumference, since those values are not interchangeable.
Set the belt into the tool’s measuring channel, keeping it flat and untwisted. Apply steady, light tension; pulling hard can distort the reading. Follow the tool’s marked path, then read the scale where the belt’s end or indicator aligns. Record the unit, too. A reading of 42 inches is not the same as 42 centimeters. NIST Special Publication 811 gives the exact conversion: one inch equals 25.4 millimeters. Convert only after noting the original unit.
Check the belt for cracks, glazing, or stretched sections before measuring; damage can make a result misleading. Repeat the measurement after reseating the belt. Small differences matter. The U.S. Department of Energy’s Improving Motor and Drive System Performance sourcebook reports belt-drive efficiencies in the 90–98% range, depending on conditions. That range is a reminder that fit and setup matter, not a guarantee for every belt. If two readings disagree, inspect the tool’s zero point and your belt placement before choosing a replacement size. I have found this step easy to rush, especially with a dusty belt, and it is worth slowing down.
After using a belt measuring tool, treat its reading as a starting point, not a verdict. Decide where you want the belt to sit: at your natural waist, lower on your hips, or over thicker clothing. These choices can change the measurement. If you already own a belt that fits comfortably, measure from the buckle’s inner edge to the hole you use most. Keep the belt flat, without pulling it tight. Small errors add up.
Now compare the result with how you actually wear a belt. A snug fit may suit lightweight trousers, while extra room can help over a tucked shirt or heavier fabric. Check the tool’s units, then repeat the measurement once. If the readings differ, check that the belt or tape stayed straight. Don’t assume your trouser size matches your belt measurement; sizing methods vary. Leave enough adjustment for sitting and bending, not just standing in front of a mirror. I’ve found that fit can feel different after a full day, so a quick standing test may not tell the whole story. A little uncertainty is normal.
Example measurements in inches are illustrative, not universal size recommendations. Measure around your waist where the belt will sit, then measure a well-fitting belt from the buckle fold to the hole you use. Compare both readings and check the belt’s hole range; sizing and measurement methods can vary.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

