


Corrugated plastic cable ducts are widely used in residential, commercial, and industrial construction to protect electrical and communication cables while supporting efficient installation.
In some PE-based conduit systems, however, the inner layer may still exhibit higher friction than desired. This can become more noticeable during longer cable pulls, routes with multiple bends, or installations involving larger and heavier cables.
When customers report that the conduit inner surface is not sufficiently smooth or that cable-pulling resistance remains relatively high, the issue should not be treated only as an installation problem. The material formulation and surface characteristics of the conduit inner layer may also need to be evaluated.
One material-level approach is to incorporate a high-molecular-weight silicone masterbatch into the PE inner-layer formulation during extrusion.
For this type of application, SILIKE LYSI-404 Silicone Masterbatch can be considered for evaluation as a processing additive and surface modifier where manufacturers are targeting lower surface friction, improved inner-surface lubricity, and stable extrusion processing.
Actual performance should be confirmed under the intended resin system, conduit structure, additive dosage, extrusion conditions and cable-pulling test method.
Cable-pulling resistance is influenced by friction between the cable jacket and the conduit inner surface.
One practical formulation approach is to incorporate a high-molecular-weight silicone masterbatch into the PE inner layer during extrusion. Depending on the formulation and processing conditions, this type of additive may help modify surface lubricity, reduce the coefficient of friction, and support a smoother cable-contact surface.
For PE-based conduit inner layers, SILIKE LYSI-404 Silicone Masterbatch can be considered for evaluation as a silicone-based processing additive and surface modifier.
The optimum dosage should be established through COF measurements, extrusion trials, and representative cable-pulling tests.
The performance of a corrugated cable conduit is determined by more than flexibility, mechanical strength, and dimensional stability.
During cable installation, the conduit inner wall becomes the direct contact surface for the cable jacket. Friction at this interface contributes to the total force required to move the cable through the duct.
As installation length increases, the effect of friction can become more important. Multiple bends, higher cable fill ratios, heavier cables, and tighter routing may further increase pulling resistance.
For conduit manufacturers, this means that the inner layer should be viewed not only as a structural component, but also as a functional surface that influences installation performance.
Polyethylene is commonly selected for cable conduit systems because it offers a useful balance of toughness, flexibility, chemical resistance, and extrusion processability.
However, PE alone does not determine the final friction behavior of the conduit inner surface.
Different PE grades can exhibit different surface and rheological characteristics. Pigments, fillers, waxes, lubricants, processing aids, and other additives may further influence the finished surface.
Processing conditions also play a role. Melt homogeneity, die condition, extrusion temperature, cooling, and line speed can affect the final inner-wall quality.
The cable jacket introduces another variable. PVC, PE, LSZH, TPU, TPE, and other jacket materials may interact differently with the same conduit formulation.
For this reason, where cable-pulling resistance remains higher than desired, manufacturers may need to evaluate the inner-layer formulation itself, rather than relying only on conduit geometry or installation-stage lubricants.
A low-friction additive should not be selected only according to hand feel.
For industrial conduit applications, several technical parameters need to be considered together.
The first is surface lubricity. A more lubricious inner layer may support easier cable movement through the conduit.
The second is the coefficient of friction. Static and dynamic COF measurements provide a more objective basis for comparing formulations.
The third is surface stability over time. Where conventional low-molecular-weight slip systems are used, manufacturers may also want to evaluate whether surface behavior changes during storage or whether blooming becomes visible.
Processing compatibility is equally important. An additive intended to improve surface performance should not create unacceptable changes in torque, melt pressure, output, or surface quality.
High-molecular-weight silicone masterbatch offers a different formulation approach from conventional low-molecular-weight lubricants.
Some traditional slip systems rely more strongly on migration toward the polymer surface. Their final behavior can therefore be influenced by storage time, temperature, additive concentration and interactions with other formulation components.
A high-molecular-weight siloxane system can instead be incorporated directly into the polymer matrix as a processing additive and surface modifier.
Depending on the formulation, this type of technology may contribute to both processing lubrication and final surface-property modification.
For conduit manufacturers, the practical value lies in the possibility of engineering lower-friction behavior directly into the inner layer rather than relying only on lubricants applied during cable installation.
Silicone masterbatch technology has been used in cable ducts, optical fiber ducts, telecom ducts, and PE pipe inner layers where manufacturers seek to modify surface lubricity and reduce friction during cable or fiber installation.
In these applications, silicone masterbatch can be incorporated into the PE-based inner layer during extrusion as a processing additive and surface modifier.
Depending on the polymer formulation, conduit structure, and processing conditions, this approach can be evaluated to help reduce inner-surface COF, improve surface smoothness, and support more persistent surface-slip performance.
For similar applications, SILIKE Silicone Masterbatch, including LYSI-404, can be considered for evaluation in PE-based inner-layer formulations where lower surface friction and improved lubricity are targeted.
SILIKE Silicone Masterbatch ( Siloxane Masterbatch ) LYSI-404 is a pelletized formulation with 50% ultra-high-molecular-weight siloxane polymer dispersed in High-density polyethylene (HDPE ). It is widely used as an efficient additive in PE-compatible resin systems to improve the processing properties and modify surface quality. Because LYSI-404 uses an HDPE carrier, it is particularly relevant for evaluation in PE-based extrusion systems, including conduit, duct, and pipe inner-layer applications.
Compared to conventional lower molecular weight Silicone / Siloxane additives, like Silicone oil, silicone fluids, or other types of processing additives, SILIKE Silicone Masterbatch LYSI series are expected to give improved benefits, eg,. Less screw slippage, improved mold release, reduced die drool, a permanent low coefficient of friction (COF), fewer paint and printing problems, and a broader range of performance capabilities.
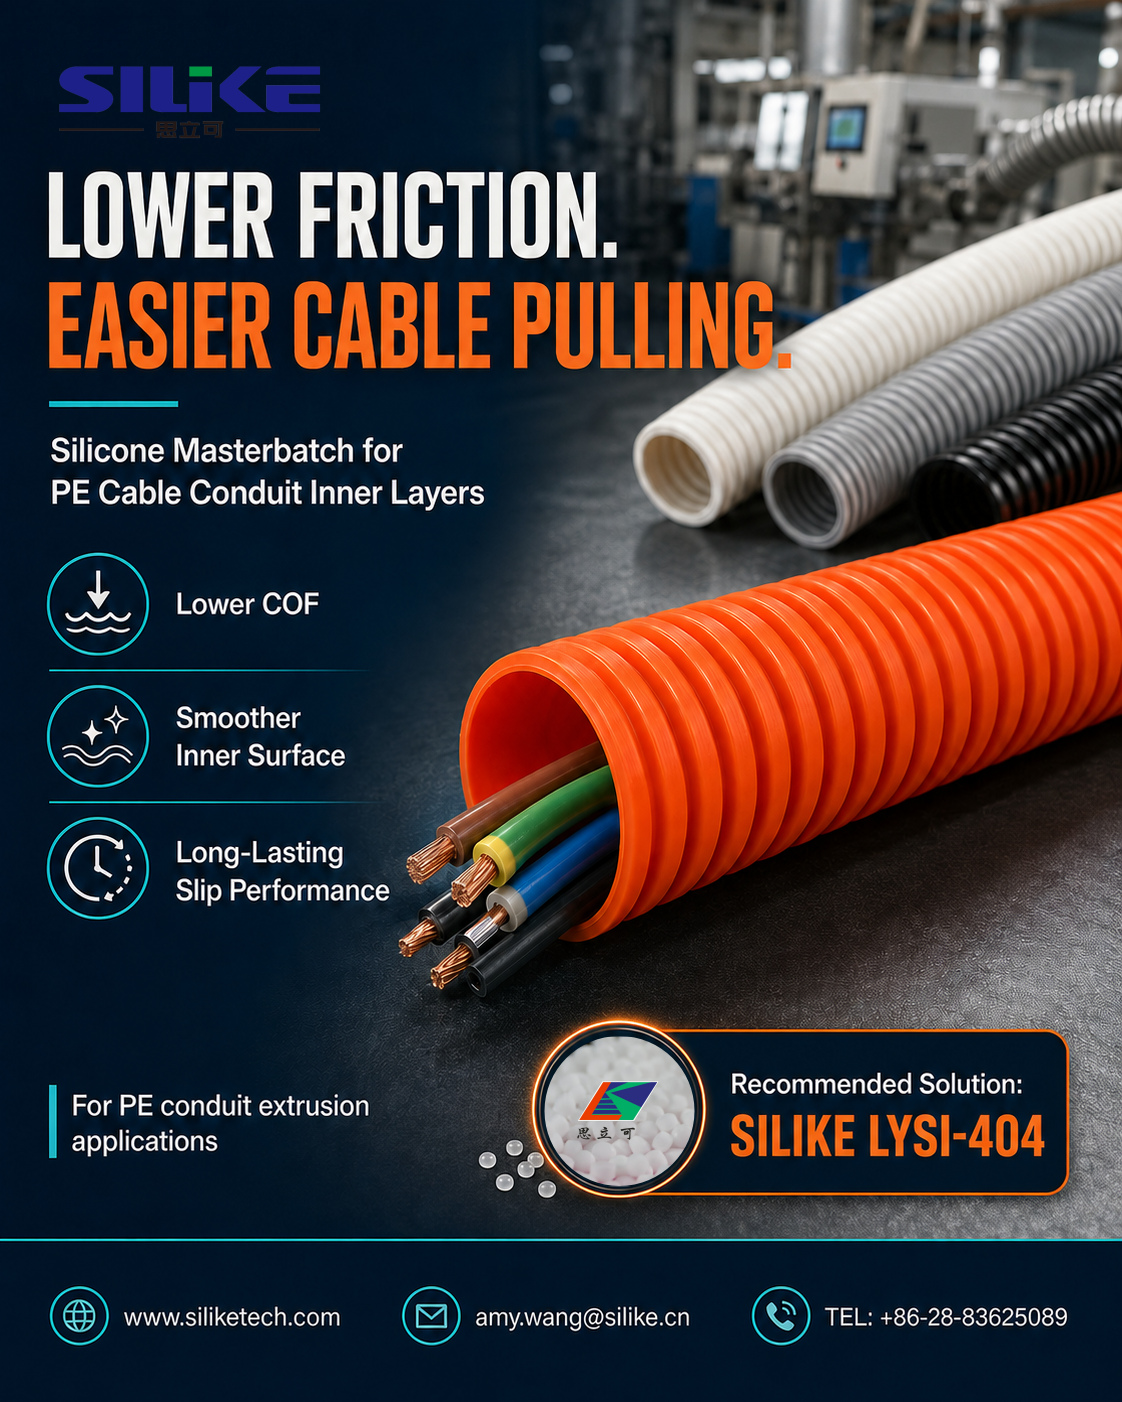
For corrugated PE cable ducts, Thermoplastic Additive LYSI-404 can be evaluated against several technical objectives.
The first is surface lubricity and smoothness. Depending on dosage, resin type, and processing conditions, the UHMW siloxane component may help support a smoother and more lubricious conduit inner surface.
The second is the coefficient of friction. Static and dynamic COF should be measured against the unmodified control formulation.
The third is extrusion processability. Silicone masterbatch LYSI-404 may also contribute to processing lubrication, so any changes in torque, melt pressure, die pressure, output, surface quality, and line stability should be recorded during trials.
Where long-term surface behavior is important, the modified conduit should also be re-evaluated after storage.
Reference HDPE inner-layer data can provide a useful technical benchmark for development.
In one reference evaluation, silicone masterbatch was incorporated into an HDPE-based inner layer and compared with an unmodified HDPE control.
Under the referenced formulation and test conditions, static COF changed from approximately 0.21–0.22 to 0.11–0.13, while dynamic COF changed from approximately 0.12–0.13 to 0.05–0.06 at an addition level of approximately 1–1.5%.
These results illustrate the potential of silicone-masterbatch modification as a low-friction inner-layer approach.
They should be treated as reference application data rather than universal performance specifications, because actual performance depends on resin grade, dosage, extrusion conditions, conduit structure, cable jacket material and test method.
For a more detailed discussion of HDPE inner-layer COF data and test considerations, see our technical article:
Silicone Masterbatch for Low-Friction HDPE Duct Inner Layers: Reference COF Data and Trial Considerations
The optimum dosage should be determined experimentally rather than assumed in advance.
For an existing PE inner-layer formulation, one possible initial screening sequence is:
Control → 0.5% → 1.0% → 1.5% → 2.0% LYSI-404
If the desired friction level is not achieved, higher concentrations can be evaluated within the recommended dosage range.
A dosage ladder helps identify the balance between surface performance, extrusion behavior, and formulation cost.
A conduit trial should combine surface, processing, and installation measurements.
For surface performance, static and dynamic COF are useful primary indicators. Inner-wall appearance and surface uniformity should also be inspected.
For installation relevance, representative cable-pulling force should be measured, where practical, using the same cable, conduit geometry, pull length, and pulling speed.
On the processing side, manufacturers should monitor torque, melt or die pressure, motor load, output, and line stability.
Where long-term slip performance is important, the same surface or COF measurements can be repeated after storage according to the manufacturer’s internal protocol.
A lower COF can be useful, but it does not fully predict field cable-pulling performance.
Actual pulling force can also be influenced by cable weight, stiffness, jacket chemistry, conduit diameter, route length, bends, cable fill ratio, installation temperature, and pulling speed.
For this reason, a stronger validation program combines:
COF measurement + extrusion evaluation + representative cable-pulling trials.
LYSI-404 silicone-based plastic additive may be relevant when the existing PE inner layer is not sufficiently smooth, when cable-pulling resistance remains higher than desired, or when the current formulation relies strongly on conventional slip or lubricant systems.
It may also be considered where manufacturers want to evaluate a material-level surface-modification approach while retaining the existing PE extrusion process.
The product should not be treated as a universal solution. Its suitability depends on the specific formulation, conduit design, processing conditions, and performance target.
Silicone masterbatch is an additive material approach that can be evaluated to modify conduit inner-surface lubricity and COF.
Actual cable-pulling performance depends on the polymer formulation, cable jacket, conduit geometry, and installation conditions.
LYSI-404 silicone masterbatch can be considered for evaluation in PE-based conduit inner layers where improved surface lubricity and lower friction are targeted.
Final suitability should be confirmed through application-specific testing.
Silicone masterbatch LYSI-404 has a recommended dosage range of approximately 0.5–5.0%.
addition level of 0.5- 2.0% can improve the product’s processing, fluidity, and mold release.
At a high level:1.0-5.0% can improve the surface properties(smoothness, scratch resistance, and abrasion resistance).
For initial screening, several dosage levels should be compared against the control formulation rather than relying on one fixed concentration.
Silicone masterbatch LYSI-404 should not be described as completely non-migrating.
Its high-molecular-weight siloxane technology is intended to provide a more persistent surface-modification mechanism and is less dependent on the rapid migration behavior associated with some low-molecular-weight slip additives.
This should not be assumed.
The need for installation lubricant depends on conduit length, number of bends, cable weight, cable jacket, and installation conditions.
The more appropriate objective is to reduce conduit-side friction and support improved cable installation performance.
For corrugated cable duct manufacturers, the inner PE layer is not only a structural component. It is also the direct interface between the conduit and the cable.
Where manufacturers are seeking lower friction, smoother inner surfaces, and more persistent slip behavior, high-molecular-weight silicone masterbatch provides one material route worth evaluating.
SILIKE LYSI-404 Silicone Masterbatch can be considered for PE-based cable duct inner layers where surface lubricity and processing modification are required.
Actual performance should be established through application-specific extrusion, COF, and cable-pulling tests before commercial adoption.
If you manufacture corrugated cable conduits, electrical ducts, telecom microducts, optical fiber ducts, or HDPE innerducts, SILIKE offers tailored solutions for your production needs. As a leading silicone masterbatch supplier for cable conduits and a low-friction additive supplier for PE pipes, we support full formulation optimization and trial evaluations for our SILIKE LYSI-404 low-friction additive.
For a more targeted evaluation, please share your PE grade, conduit structure (e.g., single or multi-layer), inner-layer thickness, conduit diameter, extrusion conditions, current lubricant system, cable jacket material, and target COF requirements.
Web: www.siliketech.com
Email: sale@levvymetal.com
TEL: +86-28-83625089


