


Choosing the right Safety Lockout devices is a practical step in controlling hazardous energy during equipment maintenance. A red padlock on a control switch may look simple, but the correct choice depends on the machine, energy source, and task. Electrical panels, valves, plugs, and moving parts each require compatible devices. A lock that does not fit securely can create confusion at the worksite.
Start by identifying every energy source connected to the equipment. Consider electricity, hydraulic pressure, compressed air, heat, and stored mechanical force. Then check whether each isolation point can accept a lockout device and remain clearly visible. For example, a valve cover should resist tampering without blocking nearby controls. A breaker lock should fit the specific breaker design, not merely look close enough. Small differences matter.
Good selection also depends on people. Devices should be durable, easy to recognize, and practical for workers wearing gloves. Labels need clear names and space for essential details. Where several workers share a task, group lockout equipment may help keep responsibility visible. Training and written procedures support the hardware; neither can replace the other. That part is sometimes underestimated.
There is no universal kit. Review the equipment, consult its manufacturer information, and involve qualified safety personnel before purchasing devices. Test fit when appropriate, and inspect devices for wear or damage. A checklist helps, but it can still miss an awkward valve or a hidden energy source. Pause and verify. The right Safety Lockout setup is the one that matches the actual equipment and supports a clear, consistent process.
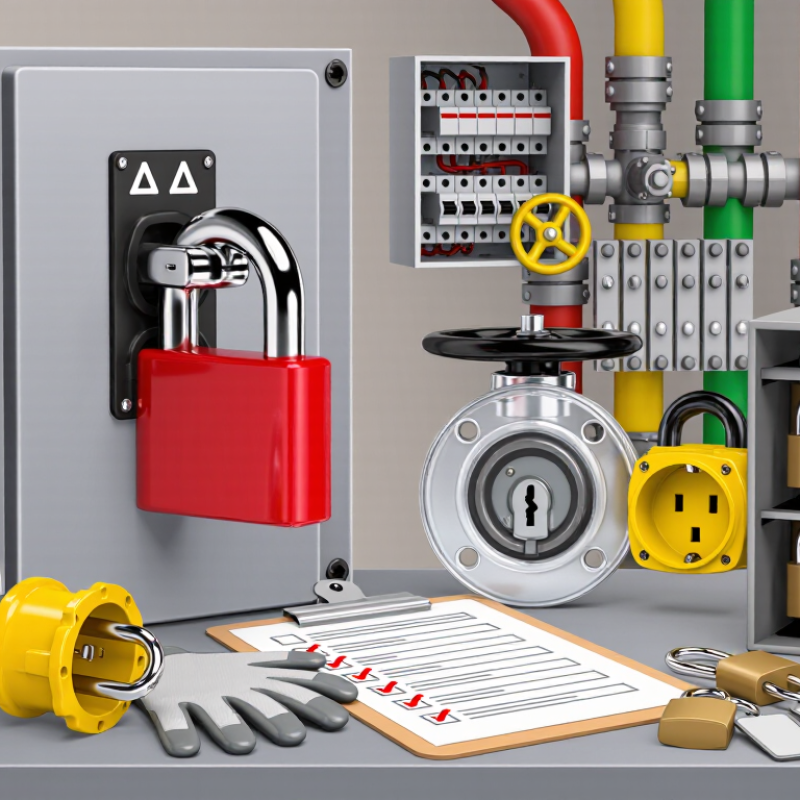
Safety lockout devices isolate hazardous energy before maintenance begins. They prevent a machine from starting unexpectedly or releasing stored electrical, mechanical, hydraulic, or pneumatic energy. A lock on a disconnect switch is only one part of the process. A complete setup may also need valve locks, hasps, tags, and devices for blocking gravity-driven parts. OSHA estimates that effective lockout/tagout practices protect nearly three million workers and prevent about 120 fatalities and 50,000 injuries each year. These figures, reported by the U.S. Occupational Safety and Health Administration, show why device selection must match the hazard—not just the machine’s appearance.
Define the scope by tracing every energy source to its point of isolation. Check equipment drawings, inspect the work area, and ask the people who service the machine where energy can remain trapped. A tag communicates danger, but it does not physically stop a switch from moving. A lock does. Verify isolation by testing controls and checking for residual pressure or motion before work starts. Small details matter. A valve handle may look secured while a second feed line remains open. I have seen planning focus on the obvious disconnect and overlook stored energy in a raised component; that is an easy assumption to make, and a useful one to challenge. U.S. OSHA’s Control of Hazardous Energy standard and guidance provide a reliable basis for defining these procedures.

Lockout/tagout follows a sequence: identify and isolate hazardous energy, apply suitable devices, control stored energy, then verify isolation before work begins.
Choose devices that physically secure the specific energy-isolating points on the equipment—for example, breaker lockouts for compatible circuit breakers and valve lockouts for compatible valves. Follow the equipment-specific procedure and applicable regulations.
Choosing a lockout device starts with a careful walk-through, not a catalog. Trace every energy source feeding the equipment: electrical circuits, hydraulic lines, compressed air, steam, gravity, and stored spring tension. A conveyor may be switched off but still hold a raised load or pressurized air. Check drawings against the machine itself; older equipment may not match its paperwork.
At each isolation point, confirm whether the device can physically secure the control in its safe position. A breaker may need a suitable breaker lockout; a valve may require a cover or cable device. Note secondary feeds, shared piping, and energy that can rebuild after shutdown. Verify isolation using the site’s established procedure, and have an authorized worker check the equipment before servicing. OSHA’s Control of Hazardous Energy guidance emphasizes controlling all hazardous energy, including stored energy. In practice, the overlooked source is often the one closest to the task.
A safety lockout device should fit both the equipment and the energy it controls. For an electrical disconnect, use a lockout that holds the switch in the off position and prevents access to its operating handle. Check the enclosure and handle dimensions before choosing a device; a close fit matters. Then apply a personal lock and verify that the equipment cannot start.
Different energy sources call for different controls. A ball valve may need a clamp that blocks the handle from turning, while a gate valve may need a cover sized to enclose its handwheel. For pneumatic or hydraulic lines, select a device suited to the coupling or isolation point, and relieve stored pressure according to the equipment procedure. Mechanical hazards can require blocking or restraint, not just a lock on a nearby power source.
Fit is only part of the decision. Consider heat, moisture, vibration, and whether workers can see the locked point during a handover. A device that works on a clean test bench may be awkward in a cramped plant room. That is worth rechecking. Match each device to the isolation point, label it clearly, and have trained workers test the isolation before maintenance begins.
Choosing a safety lockout device starts with the equipment it must secure. Check the energy-isolating point’s shape, size, and movement before selecting a device. A valve handle may need a different cover than a breaker toggle. Measure the opening and test the fit while the equipment is safely isolated. The device should prevent operation without blocking nearby controls or creating a snag hazard. A fit that looks close is not always a safe fit.
Durability matters in daily use. Inspect the body, hinge, and locking points for cracks, corrosion, or looseness. In a damp washdown area, materials must tolerate moisture and cleaning agents; outdoors, they may face sunlight and temperature changes. Try the device with the gloves workers actually wear. Small details count. I have seen a sturdy device become awkward when its label rubbed off or its hasp was difficult to reach. That is easy to overlook.
Check that the device supports your site’s lockout procedure and applicable safety requirements. Confirm how many personal locks it accepts, whether its labels remain readable, and whether workers can identify the isolation point clearly. Keep inspection records and replace damaged devices promptly. Requirements differ by equipment and location, so verify choices with a qualified safety professional. Compatibility is not a one-time guess; review it when equipment or work conditions change.
Establishing Procedures for Use, Inspection, and Storage
A suitable lockout device must fit the energy source and the equipment’s isolation point. A valve cover, breaker lock, and cable device serve different purposes. Match each device to the machinery, then document its application in a clear, equipment-specific procedure.
OSHA estimates that effective lockout/tagout practices prevent about 120 fatalities and 50,000 injuries each year. That estimate underscores why procedures need to work on the shop floor, not just on paper.
Keep instructions near the equipment. Include shutdown steps, energy-isolation points, stored-energy controls, and a method for verifying isolation. Short steps help. So do clear labels.
Train authorized workers to apply and remove devices, and make inspection part of routine use. Check for cracks, worn cables, illegible tags, or locks that no longer secure firmly.
OSHA’s Control of Hazardous Energy standard requires periodic inspections of energy-control procedures, at least annually. Record findings and correct problems promptly.
Storage matters, too. Keep devices clean, dry, and organized in a designated cabinet or board, with damaged items separated from ready-to-use equipment. A missing device can disrupt a job; a poorly stored one may be overlooked.
Procedures are never perfect. Ask workers where steps feel unclear, then revise them when equipment or tasks change.
Source: OSHA, Control of Hazardous Energy (Lockout/Tagout), 29 CFR 1910.147.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

