How to Choose the Best PET Bottle Baling Machine?
Choosing the right Pet Bottle Baling Machine can look simple on a product page. In practice, the decision affects labor, storage space, bale quality, and daily operating costs. A machine that appears powerful may still perform poorly with wet, mixed, or loosely prepared bottles. Buyers should examine the complete recycling process, not only motor power or advertised capacity.
This guide focuses on practical selection criteria used in real PET recycling environments. It considers feeding methods, pressing force, chamber size, bale density, automation, safety controls, maintenance access, and energy use. Operators should also inspect the tying system, because loose bales can collapse during transport. Small details matter. A reliable supplier should provide clear specifications, installation guidance, spare-parts support, and test results from comparable materials. Claims without measurable data deserve careful questioning.
There is no perfect machine for every facility. A compact vertical model may suit a small warehouse, while a horizontal automatic baler may fit a high-volume sorting line. The best choice depends on bottle volume, available floor space, workforce skills, and budget stability. Buyers sometimes focus too heavily on the lowest purchase price. That can be a costly mistake. However, the most expensive option is not automatically the strongest one. A balanced evaluation is better, although real conditions may challenge the original plan. This article outlines a practical method for comparing machines, checking supplier reliability, and selecting equipment that supports safer, cleaner, and more consistent PET bottle recycling.
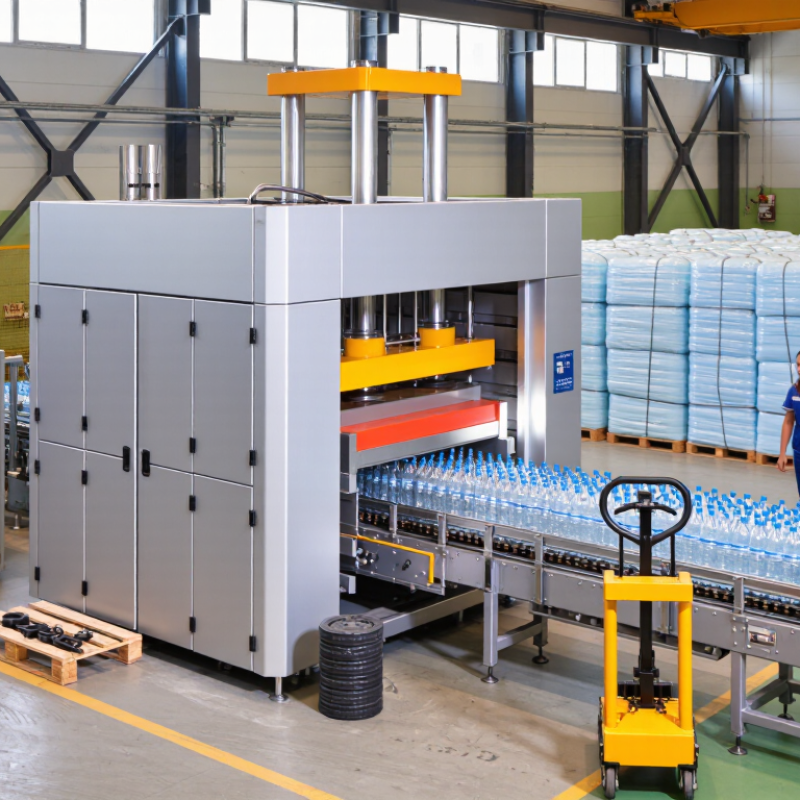
Define PET Feedstock Using Its 1.38 g/cm³ Resin Density (ISO 1183)
How to Choose the Best PET Bottle Baling Machine?
Define PET Feedstock Using Its 1.38 g/cm³ Resin Density (ISO 1183)
PET resin has a density of approximately 1.38 g/cm³ under ISO 1183 testing. This value identifies the polymer, not a loose bottle’s actual density. Empty bottles contain air, labels, caps, and moisture. Their bulk density can be far lower. That difference matters when selecting a PET bottle baling machine.
Measure your feedstock before comparing equipment. Collect a representative sample from several production hours. Remove obvious foreign materials, then record its weight and container volume. A simple bulk-density test can reveal whether your bottles arrive flattened, dusty, or loosely packed. Do not rely on resin density alone. It is a material reference, not a complete machine specification.
The machine should match your measured throughput, bottle shape, and desired bale weight. Check chamber dimensions, compression force, tying method, and feeding stability. A narrow chamber may create dense bales but slow uneven material flow. Excessive compression can also trap moisture and make handling difficult. Leave room for real operating variation.
Test the machine with actual PET bottles. Ask for bale-density results, cycle times, and energy data from comparable feedstock. Inspect bale edges after tying. Loose corners often indicate poor filling, not weak compression. I have seen calculations look perfect on paper, yet the line struggled with wet bottles and tangled labels. That is why measured site data should guide the final choice.
How to Choose the Best PET Bottle Baling Machine?
PET resin has a density of approximately 1.38 g/cm³, equivalent to 1,380 kg/m³, according to ISO 1183. The chart models the theoretical PET mass in one cubic metre of bale volume at different solid-material fractions. Higher-density bales generally require stronger compaction force, robust chamber construction, and reliable bale-wire or strapping systems.
Set Bale-Density Targets of 200–350 kg/m³ for Transport Efficiency (EN 643)
Choosing a PET bottle baling machine starts with a measurable density target. A practical range is 200–350 kg/m³ for transport efficiency. However, EN 643 mainly classifies recovered paper and board, not PET bottles. It should not be treated as a PET density standard. For PET, document bale composition, moisture, contamination, dimensions, and traceability separately.
A 1.2 × 1.0 × 0.8 metre bale has a volume of 0.96 m³. At 200 kg/m³, it weighs about 192 kilograms. At 350 kg/m³, the same bale reaches roughly 336 kilograms.
That difference affects truck loading, handling safety, and storage space. The OECD Global Plastics Outlook reports 353 million tonnes of plastic waste generated globally in 2019. Better compaction cannot solve recycling alone, but it can reduce unnecessary transport movements.
Set the machine near 250–300 kg/m³ initially. Then verify actual bales with a calibrated scale and measured dimensions. Do not rely only on hydraulic pressure readings. Bottle shape, label content, moisture, and feeding consistency can change density quickly. A bale may look firm while its core remains loose. That happens.
In daily operation, check three consecutive bales from each shift. Record weight, volume, wire integrity, and recovery quality. If bales exceed 350 kg/m³, sorting equipment may face feeding problems. If they remain below 200 kg/m³, transport costs can rise sharply. The target is useful, but not sacred. Local contracts and equipment limits may require adjustment.
Match Machine Throughput in kg/h to the Available PET Feed Rate
How to Choose the Best PET Bottle Baling Machine?
Match Machine Throughput in kg/h to the Available PET Feed Rate
The correct PET bottle baling machine should match your real feed rate, not a brochure’s maximum figure. Measure incoming bottles during normal shifts, including pauses, sorting delays, and material changes. If your line supplies 420 kg/h, a machine rated for 500–550 kg/h may provide useful operating space. A much larger unit could increase purchase costs without improving production.
Do not measure only one busy hour. Record feed rates across several days. Wet bottles, labels, caps, and loose containers can reduce practical throughput. A machine rated at 600 kg/h may process less when material is irregular or poorly distributed. Keep the feed steady. Large surges can overload the conveyor and create uneven bales. A buffer hopper may help, but it cannot repair an undersized feeding system.
Check the machine’s continuous working capacity, not only its peak capacity. Ask for test conditions, material density, moisture assumptions, and bale weight. For example, if your average supply is 300 kg/h but peaks at 430 kg/h, select equipment that handles the peak without running constantly at its limit. Leave some capacity for seasonal changes. Still, excessive margin is not always wise. I once trusted average figures too much; the quiet hours looked efficient, but peak loads exposed the mistake. Real measurements are less convenient, yet they produce a more reliable choice.
Compare Vertical and Horizontal Presses by Bale Size and Space Limits
How to Choose the Best PET Bottle Baling Machine?
PET volume is growing, but recovery remains uneven. The OECD reported that only 9% of global plastic waste was recycled in 2019. NAPCOR’s 2022 report recorded about 1.9 billion pounds of PET bottles collected in the United States. These figures make bale density and handling speed practical decisions, not small technical details.
A vertical press usually suits stores, warehouses, and small recycling stations with limited floor space. It often produces PET bales weighing roughly 40–150 kilograms, depending on material preparation and chamber size. The machine can fit against a wall, but operators must allow room for loading and bale removal. It is slower for continuous, high-volume streams. That matters more than many buyers expect.
A horizontal press needs a longer installation area, yet it can create denser bales of about 300–600 kilograms. Those larger units reduce handling frequency and may improve transport efficiency. The U.S. Energy Information Administration reports that transportation costs remain sensitive to load efficiency, although its data is not specific to PET bales. I would not treat these ranges as promises. Bottle shape, moisture, feeding consistency, and compression pressure change the result. Measure your narrowest aisle first. Then calculate weekly PET volume, available power, forklift access, and bale storage space before choosing vertical or horizontal equipment.
Verify Guarding and Interlocks Against Baling-Press Safety Rules (EN 415-8)
How to Choose the Best PET Bottle Baling Machine?
When choosing a PET bottle baling machine, inspect its guarding before comparing output rates. Guards should block access to the compression chamber, ram, and moving tie points. Fixed guards need secure fasteners and should not be removable by hand. Interlocked doors must stop hazardous motion when opened. They should also prevent automatic restarting after closure. That detail is easy to miss.
Ask the supplier for risk-assessment records, interlock specifications, and validation evidence related to EN 415-8. Check the machine against the current edition and applicable local requirements. EN 415-8 should guide the review, not replace a competent safety assessment. During a site inspection, test every access door under controlled conditions. Confirm that the ram stops, stored energy is controlled, and restarting requires a deliberate reset. An emergency stop is essential, but it cannot replace guarding. A practical inspection may reveal one rear panel treated as “maintenance only.” That assumption deserves questioning.
Tips: Use a written test sheet. Record each guard, switch, stopping response, and reset action. Check for damaged hinges, bypassed switches, or loose wiring. Test again after cleaning and maintenance. If a result feels unclear, pause the purchase and request independent verification. Safety shortcuts can become expensive habits.





