


Choosing an Embossed Aluminum Sheet supplier requires more than comparing prices on a spreadsheet. The supplier must understand alloy selection, temper, embossing depth, thickness tolerance, and the final application. A roofing panel, elevator interior, and industrial floor need different performance priorities.
Dr. J. Gilbert Kaufman, a respected aluminum metallurgy author, offers a useful warning: “A specification is only as reliable as the inspection behind it.” Buyers should request mill test certificates, production samples, surface inspection records, and clear explanations of testing methods. Check whether the supplier can maintain a consistent pattern across repeated batches. Tiny height differences can affect light reflection, bonding, and installation.
Look closely.
Ask about alloy grades, such as 1050, 3003, or 5052, and confirm the required temper. Verify sheet thickness at several points, not only at the edge. Review embossing depth, flatness, coating adhesion, and corrosion resistance. A reliable supplier should identify its rolling mill, explain traceability, and provide realistic production and shipping schedules.
Factory experience matters. A supplier may display attractive samples but struggle with a large order. Request references from similar projects. If possible, inspect packaging, labeling, and moisture protection before shipment. Poor wrapping can leave pressure marks or stains on the surface.
The cheapest quotation may hide inconsistent tolerances, delayed replacements, or weak documentation. Still, expensive does not always mean better. I have learned that a polished certificate cannot replace physical verification. Buyers should compare evidence, not promises, before choosing an Embossed Aluminum Sheet supplier.
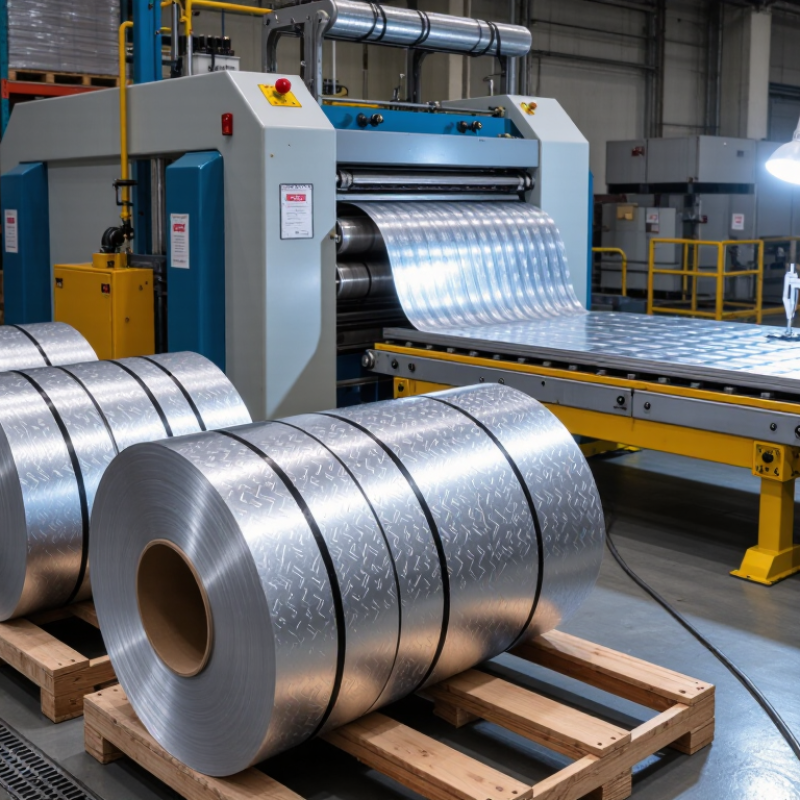
Define the alloy before comparing prices. 3003-H14 suits general forming, panels, and decorative applications. It offers useful corrosion resistance and moderate strength. 5052-H32 provides higher strength, especially for demanding enclosures and marine-related environments. Ask suppliers for mill test certificates, temper records, and traceable batch numbers.
Thickness usually ranges from 0.3 to 6 mm. Thin sheets need careful leveling and protective packaging. Thicker sheets require consistent rolling pressure and accurate flatness control. Request actual tolerance data, not only nominal dimensions. A 0.2 mm difference can affect bending results. Small errors matter.
Specify the pattern clearly including rib shape, pitch, depth, and direction. Pattern height can change the effective thickness and usable surface area. Confirm standard sizes, cut-to-length options, edge conditions, and squareness. Review a physical sample under angled light. Photos often hide uneven embossing.
I once treated pattern depth as a cosmetic detail; that was a costly assumption.
A sample can still mislead if it comes from another production batch. Require inspection records for both appearance and mechanical properties, then compare them with your drawings before placing a larger order.

Choosing an embossed aluminum sheet supplier requires more than comparing patterns or prices. Start by checking whether the alloy, temper, thickness, and sheet form match ASTM B209 requirements. ASTM B209 covers aluminum and aluminum-alloy sheet and plate, while EN 573-3 verifies chemical composition and material designation. Ask for a recent mill test certificate, not a generic brochure. It should show the alloy, temper, lot number, dimensions, and test results. Small details matter.
ISO 9001 certification indicates a controlled quality management system, but it does not automatically prove product compliance. Request the certificate scope, issuing body, validity date, and audit status. Compare these records with samples from the same production lot. Measure thickness at several points, inspect embossing depth, and check for cracks, dents, stains, or uneven edges. Paperwork can look complete while traceability remains weak. That deserves attention.
Tips: Ask how nonconforming sheets are isolated and documented. Confirm whether independent testing is available for disputed results. Keep approved samples and written tolerances before ordering. If a supplier avoids sharing batch records, pause the evaluation. A reliable supplier should explain limitations clearly, including properties not covered by a specific standard.
| Evaluation Dimension | Relevant Standard | What to Verify | Required Evidence | Practical Acceptance Check |
|---|---|---|---|---|
| Base alloy and product form | ASTM B209/B209M EN 573-3 | Confirm the alloy designation, sheet or plate classification, temper, and whether the embossed product is manufactured from compliant wrought aluminum sheet. | Material test certificate, purchase specification, alloy and temper statement. | The certificate and purchase order should show the same alloy, temper, product form, and applicable standard requirements. |
| Chemical composition | EN 573-3 ASTM B209/B209M | Check that the measured elemental composition falls within the limits for the specified wrought aluminum alloy. | Heat number, laboratory chemical analysis, and traceable material test certificate. | Compare reported values with the alloy limits in the applicable edition of EN 573-3 or the ordered ASTM alloy specification. |
| Mechanical properties | ASTM B209/B209M | Verify tensile strength, yield strength, and elongation for the selected alloy, temper, and thickness range. | Tensile-test results, test method, specimen direction, thickness range, and heat or lot identification. | Results should meet the minimum or specified ranges stated for the ordered alloy and temper; do not rely only on nominal alloy names. |
| Thickness and dimensional accuracy | ASTM B209/B209M Purchase specification | Define whether thickness means base-metal thickness, embossed overall thickness, or both. Also specify width, length, flatness, and squareness. | Dimensional inspection report, calibrated measuring-tool records, and approved drawing. | Measure the base thickness and overall embossed profile separately where required, using the agreed sampling plan and tolerances. |
| Embossed pattern and surface condition | ASTM B209/B209M Purchase specification | Specify pattern type, pitch, embossing height, rolling direction, surface finish, allowable dents, scratches, stains, and burrs. | Approved sample, technical drawing, surface-inspection criteria, and pre-shipment photographs. | Compare production pieces with the approved sample under consistent lighting; reject cracks, delamination, severe distortion, or unacceptable surface damage. |
| Traceability and batch control | ASTM B209/B209M ISO 9001:2015 | Confirm that coils, sheets, test certificates, inspections, and shipping documents can be linked through a heat, lot, or batch number. | Lot identification system, material certificates, inspection records, and packing-list references. | Select a random package and trace it back to the production lot, raw material certificate, inspection result, and dispatch record. |
| Quality management system | ISO 9001:2015 | Verify that the supplier operates a documented quality management system covering purchasing, production, inspection, nonconformity control, and corrective action. | Valid ISO 9001 certificate, certification scope, issuing certification body, and certificate validity status. | Check that the certificate scope covers the relevant manufacturing or supply activities and independently confirm its validity where possible. |
| Inspection and test equipment | ISO 9001:2015 ASTM B209/B209M | Assess whether gauges and test instruments are suitable, identified, calibrated, and protected from use when inaccurate. | Calibration certificates, equipment register, inspection procedures, and test-laboratory records. | Calibration dates should cover the production and inspection period; instruments should have clear identification and calibration status. |
| Nonconforming product control | ISO 9001:2015 | Determine how the supplier identifies, segregates, evaluates, and disposes of material that fails dimensional, chemical, mechanical, or visual requirements. | Nonconformity procedure, corrective-action records, concession process, and customer complaint records with sensitive information removed. | The supplier should demonstrate documented decisions, root-cause analysis, corrective actions, and verification of effectiveness. |
| Pre-shipment documentation | ASTM B209/B209M EN 573-3 ISO 9001:2015 | Confirm that the final document package matches the ordered specification and shipment identification. | Certificate of conformity, material test certificate, dimensional report, packing list, and inspection release. | Review documents before shipment and verify consistency of alloy, temper, dimensions, quantity, lot number, and inspection status. |
Note: ASTM B209/B209M addresses aluminum and aluminum-alloy sheet and plate requirements; EN 573-3 specifies the chemical composition of wrought aluminum alloys; ISO 9001:2015 specifies quality management system requirements. The applicable edition, alloy, temper, thickness range, and contractual tolerances should be confirmed before purchase.
Choosing embossed aluminum sheet suppliers requires more than checking surface patterns. Capacity decides whether quality survives repeat orders. Ask for MOQ by alloy, temper, thickness, width, and embossing design. A supplier offering 500 kilograms may not support stable monthly production. The International Aluminium Institute reported about 70 million tonnes of primary aluminum production in 2023. That scale shows availability, not supplier reliability. Review actual production records.
Request the last three months of output for comparable sheets. Compare it with your forecast and peak-season demand. A factory should explain machine loading, inspection points, and backup capacity. Lead time must include tooling, sampling, production, packing, and port dispatch. Short promises can hide unfinished steps. UNCTAD’s Review of Maritime Transport 2023 notes that over 80% of global merchandise trade by volume moves by sea. Export experience therefore matters. Check destination markets, packing photos, shipping documents, and on-time delivery data. One perfect shipment proves little.
Tips:
Ask for a capacity sheet. Verify MOQ in writing. Request monthly output evidence. Separate production days from shipping days. Use the World Bank’s 2023 Logistics Performance Index as a reference for timeliness, tracking, and logistics competence. A low MOQ may seem attractive, but it can reduce production efficiency. Reconsider that trade-off.
A reliable supplier should provide measured quality data, not only attractive sample photos. The Aluminum Association’s Aluminum Standards and Data explains that sheet tolerances vary by alloy, temper, width, and thickness. ASTM B209/B209M follows the same principle. Therefore, reject vague claims such as “standard tolerance.” Request the actual tolerance table for your selected grade and size. Measure thickness on the flat land, not only across the raised pattern. A difference of 0.05 mm can affect bending, weight, and assembly fit.
Embossment depth needs separate control. Ask for the nominal depth, minimum depth, maximum depth, and sampling method. A digital height gauge or optical profilometer can record the pattern across several locations. Ten-point sampling is more informative than one center reading. Supplier drawings should show peak shape, pitch, and allowable variation. One weakness in many inspections is measuring only one sheet. That can hide roll-to-roll variation. A supplier’s report should include batch numbers, instrument calibration, and test dates.
Tips: Ask for three production samples, not one showroom piece. Check gloss, scratches, stains, and uneven rolling under angled light. ISO 21920-2 identifies parameters such as Ra and Rz for surface-texture evaluation, but Ra alone may miss directional marks. Request both numerical readings and clear photographs. Also compare the certificate with your own inspection; paperwork can be correct while the delivered surface still feels wrong.
A low material price can hide expensive weaknesses. Compare the alloy, temper, embossing depth, tolerance, and actual usable weight. The U.S. Geological Survey reported about 70 million metric tons of primary aluminum production worldwide in 2023. This scale does not remove price risk. Energy, alumina, and regional premiums still influence quotations. Ask suppliers to show the pricing formula and validity period.
Packaging deserves a line-by-line review. Check sheet separators, moisture barriers, edge protection, pallet strength, and loading photos. Damaged corners can create more waste than a higher unit price. The International Aluminium Institute states that recycling aluminum can save up to 95% of the energy used for primary production. Therefore, request recycled-content evidence, but verify it through certificates and batch records. Claims without documents are weak.
Freight is not just ocean freight. Include inland trucking, port charges, insurance, customs handling, and possible storage. UNCTAD’s Review of Maritime Transport reports that shipping carries over 80% of world merchandise trade by volume. Small delays can therefore affect delivery budgets. Warranty terms should define dent limits, coating defects, replacement timing, and inspection procedures. Traceability should connect each bundle to heat numbers, production dates, test reports, and packing records. In supplier audits, the cheapest offer is often incomplete. I may still overlook hidden handling costs, so a landed-cost worksheet and a second quotation review are sensible safeguards.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

