How to Choose a Powder Pressing Machine?
Choosing a Powder Pressing Machine is a production decision, not a simple equipment purchase. The right model must match powder behavior, target density, part geometry, output volume, and quality controls. A small ceramic component may need careful die filling and low-speed compaction. A larger metal part may require much higher force and stronger tooling.
Industry data supports careful planning. The World Powder Metallurgy Report 2024, published by the European Powder Metallurgy Association, describes continuing demand for powder-based manufacturing in automotive, aerospace, medical, and industrial applications. Grand View Research also reports steady growth in the global powder metallurgy market, driven by material efficiency and near-net-shape production. These figures show opportunity, but they do not guarantee a suitable machine.
Look closer.
A reliable evaluation should examine pressing force, stroke length, feeding accuracy, cycle speed, die compatibility, and density consistency. It should also consider dust control, guarding, noise, maintenance access, and operator training. Powder characteristics can change during storage, so laboratory trials are valuable. A machine that performs well with one blend may struggle with another.
Powder metallurgy expert Randall M. German has stated, “The powder is the process.” That short warning deserves attention. Machine specifications alone cannot solve poor powder flow or uneven lubrication. Buyers should request test pressing, inspect sample parts, and review documented service support. No selection is perfect. Cost, flexibility, and productivity often compete. The best choice is the machine that delivers repeatable results under real factory conditions, not merely impressive figures on a brochure.
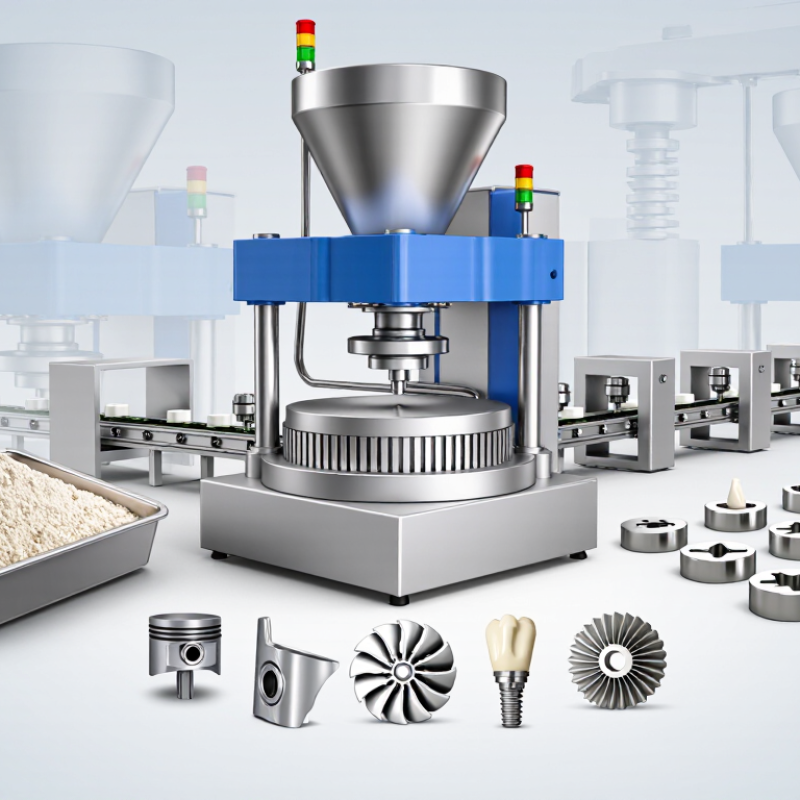
Understanding Powder Pressing Machine Types and Applications
How to Choose a Powder Pressing Machine? Understanding Powder Pressing Machine Types and Applications
Start with the powder. Its flowability, moisture, particle size, and compressibility determine the suitable machine. Single-action presses work well for simple parts with moderate thickness. Double-action presses improve density uniformity by applying force from both sides. Rotary presses suit high-volume tablet production, while hydraulic presses offer flexible pressure control for larger components. Hot isostatic pressing supports complex, high-performance parts, but it requires higher investment and thermal control.
Applications reveal practical differences. Ceramic components may need careful pressure distribution to prevent cracks. Metal powder parts often require controlled compaction, ejection, and later sintering. Pharmaceutical production demands repeatable filling, compression, cleaning, and validation. A 2024 Grand View Research report estimated the global powder metallurgy market at approximately USD 2.4 billion in 2023, with continued growth through 2030. This trend increases demand for reliable, automated compaction systems. The exact figure varies by research method.
Check more than maximum pressure. Review die dimensions, cycle speed, density variation, material loss, and maintenance access. For example, a small component with sharp edges may need precise filling rather than extreme force. A production trial should measure tablet weight, green density, ejection damage, and dimensional change. Small errors matter. ISO 13485 or pharmaceutical compliance may also influence machine design and documentation. In my experience, selecting only by tonnage often creates expensive tooling problems later. That choice is rarely neat. Powder behavior can change between batches, so test data should guide the final specification.
Assessing Material Properties and Production Requirements
How to Choose a Powder Pressing Machine?
Assessing Material Properties and Production Requirements
A suitable powder pressing machine begins with the material, not the advertised tonnage. Measure particle size, moisture, flowability, compressibility, and bulk density under controlled conditions. These properties affect die filling, pressure distribution, and finished-part strength. A powder that flows well in a small test may bridge inside a larger hopper. Real production can be less predictable.
Record the target dimensions, weight tolerance, hardness, cycle rate, and expected output. Fine powders may need controlled feeding and dust management. Granular materials may require different tooling and filling speeds. Check whether the machine provides adjustable pre-compression, main compression, dwell time, and ejection control. These settings help reduce cracks, lamination, and weight variation. However, more adjustment does not automatically mean better results.
Production requirements must include cleaning time, changeover frequency, operator access, and maintenance skill. Ask for test pressing with your actual powder, tooling, and planned speed. Inspect several hundred parts, not only the best samples. Measure density from the top, middle, and bottom of the batch. A calibrated force sensor and documented inspection method improve confidence. Still, laboratory results can mislead when humidity, temperature, or powder age changes. Leave room for process tuning. That part is often underestimated. A reliable selection balances material behavior, repeatability, practical throughput, and safe operation rather than maximum machine capacity.
How to Choose a Powder Pressing Machine?
Typical compaction pressure and target throughput vary with powder type. Use these representative engineering values as an initial guide, then confirm machine sizing through material trials.
Metal powders generally require the highest compaction pressure, while ceramics and graphite can support higher production rates at moderate pressure. Moisture-sensitive pharmaceutical powders require careful feeding, controlled humidity, and consistent fill depth in addition to suitable pressing force.
Comparing Press Capacity, Precision, and Operating Features
How to Choose a Powder Pressing Machine?
Choosing a powder pressing machine starts with the material, not the advertised maximum force. Press capacity should match the powder’s flow behavior, fill depth, and target density. A machine rated far above your needs may waste energy and reduce control. I recommend testing production samples under realistic conditions. Record the required force, cycle time, and rejection rate. Small differences become expensive at scale.
Precision deserves equal attention. Check fill-weight variation, pressure repeatability, and dimensional stability across several cycles. A useful trial should include startup, continuous running, and an intentional stop-and-restart. That reveals problems that a short demonstration can hide. Ask how often sensors require calibration, and request documented tolerance data. Numbers without test conditions are difficult to trust. Measure twice.
Operating features affect daily reliability. Adjustable filling, pressure, dwell time, and ejection speed help operators respond to changing powder conditions. A clear control panel reduces training errors. Tooling access should allow quick inspection without awkward reaching. Guarding, interlocks, dust management, and emergency stops also deserve practical checks. They are not decorative features. Maintenance records, spare-part availability, and service response should be reviewed before purchase. I once underestimated cleaning time; the machine performed well, but changeovers were slower than expected. That mistake changed how I evaluate total operating cost.
Evaluating Tooling, Automation, Safety, and Maintenance Needs
How to Choose a Powder Pressing Machine?
Tooling should match the powder, part geometry, and required tolerance. Ask how quickly dies can be changed. Examine punch alignment, die wear, and access around the pressing zone. A practical trial should include abrasive powder, repeated cycles, and realistic cleaning intervals. Shiny tooling can still hide poor ejection. Do not trust a brochure alone.
Automation must solve a measurable problem. Check feeding consistency, recipe control, sensor coverage, and recovery after a stoppage. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. That figure shows strong automation demand, but more automation also creates more failure points. A simple, well-documented system may outperform a complex one. I have seen impressive interfaces become difficult to repair.
Safety requires more than an emergency-stop button. Review guarding, interlocks, stored hydraulic energy, dust control, and safe die-change procedures. ISO 12100 supports risk assessment throughout machine design. The U.S. Department of Energy notes that compressed-air leaks can waste 20–30% of compressor output. Pneumatic losses therefore deserve measurement, not guesswork. Maintenance teams need access to filters, seals, lubrication points, and diagnostic data. Record cycle counts and inspect tooling before defects appear. Some schedules will be wrong. Revise them using wear patterns, downtime records, and operator feedback.
Selecting a Machine That Fits Your Budget and Production Goals
Choosing a powder pressing machine starts with the product, not the catalog price. Record powder flow, target weight, dimensions, allowable variation, and daily output. A benchtop unit may suit pilot batches. Continuous production demands stronger frames, guarded tooling, quick-change dies, and stable feed control. Build the budget around total ownership costs. Include tooling, dust extraction, compressed air, electricity, maintenance, validation, and operator training. The cheapest machine can become expensive after installation.
Use a simple capacity calculation: required output equals demand plus rejects and planned downtime. If the target is 12,000 pieces per shift, a 12,000-piece rating is too tight. Allow time for cleaning and changeovers. The U.S. Department of Energy’s compressed-air guide reports that leaks commonly waste 20–30% of compressor output. Check air consumption before approving the utility layout. A slower machine may cost less to operate and produce fewer defects. Measure that trade-off instead of guessing.
For growth plans, inspect data access, recipe control, alarm history, and integration options. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. This does not mean every press needs automation. It suggests that future handling and inspection deserve early consideration. Request sample runs using your actual powder. Measure weight variation, hardness, surface quality, noise, and cleaning time. I would not trust a perfect demonstration. Real powder varies, and operators make mistakes. Leave budget for those realities.





