Choosing a Linear Abrasion Tester begins with the surface, not the catalog. A coated panel, a plastic component, and a printed label may all need abrasion testing, but they do not necessarily need the same motion, load, or abrasive material. A machine that looks impressive on a specification sheet can still produce results that miss your real use conditions.
Start with the question your test must answer. Will the specimen face repeated rubbing, a defined stroke, or a particular contact pressure? Check the tester’s stroke length, speed range, load control, and fixture options. Look closely at how samples are secured. A small shift under the clamp can change the wear track and weaken comparisons between runs. Repeatability matters.
The instrument is only part of the method. Abrasive type, specimen preparation, conditioning, and inspection criteria also shape the result. Record them. Test representative materials, and compare the outcome with your intended application. Real surfaces can behave unpredictably. That deserves attention.
One practical principle for this guide is: “[Insert a verified industry expert’s name and exact quotation about repeatable abrasion testing].” No source article or verifiable expert quotation was provided, so this placeholder avoids inventing an expert or misattributing a statement. Replace it with a confirmed quotation before publication.
The sections ahead explain how to match tester features to materials, test goals, and lab routines. They also consider maintenance, operator usability, and documentation. A careful choice will not remove every uncertainty. It can make the results more consistent, interpretable, and useful.
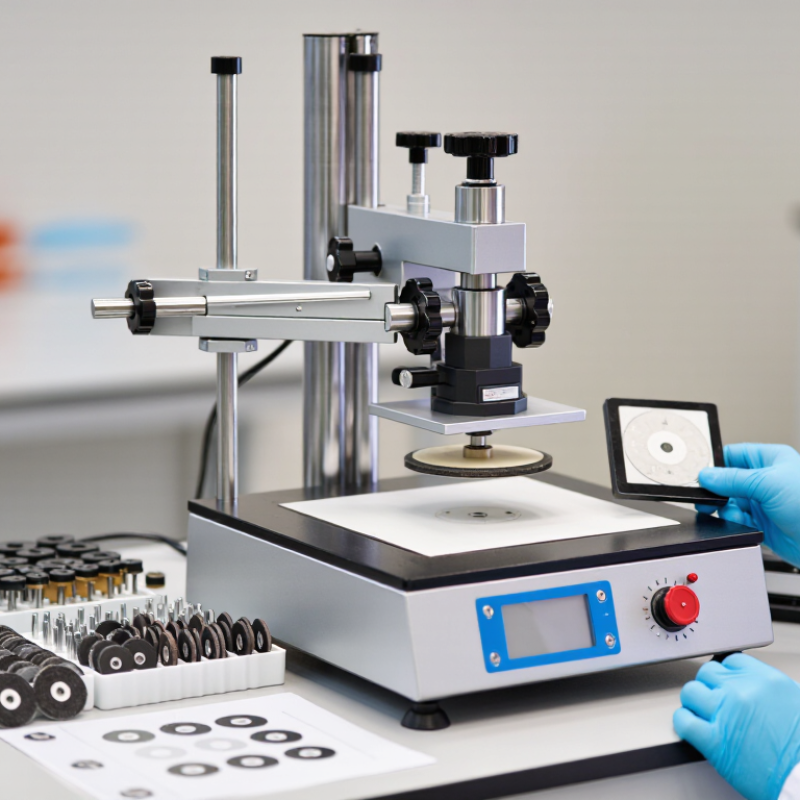
Before selecting a linear abrasion tester, define the exact material and surface under test. A woven fabric, printed film, soft coating, and molded plastic respond differently to the same rubbing action. Record thickness, finish, conditioning time, and specimen orientation. For textiles, ISO 12947-2 describes Martindale abrasion testing at pressures of 9 kPa or 12 kPa, depending on the test setup. These figures are useful context, not direct settings for a linear tester. The motion and contact geometry differ. Small details matter.
Next, specify the abrasive, applied force, stroke length, speed, cycle count, and endpoint. State whether failure means visible wear, color change, coating breakthrough, or a measured mass loss. A metal stylus can cut a soft polymer, while a fabric counterface may better represent repeated contact with clothing. Test the same surface condition customers will encounter, including any cleaning or aging step. Keep it realistic. ASTM D4060 offers a useful comparison for coatings because it controls abrasive wheels and test cycles, but it uses rotary motion. Do not treat its results as interchangeable with linear-abrasion data. Run replicates, photograph the wear track under consistent lighting, and report any specimen variation. It is tempting to choose a severe load for faster results. That may rank samples differently from ordinary use. Define the conditions before comparing materials.
Start by specifying the material, counterface, contact force, dry or wet condition, stroke length, and failure endpoint. The chart shows the rubbing-stroke tolerance specified for the crockmeter procedure in ISO 105-X12, a method for assessing textile colour fastness to rubbing—not a universal setting for every abrasion test.
Reference conditions: ISO 105-X12 specifies a 104 ± 3 mm rubbing stroke, a 16 ± 0.1 mm rubbing finger, and a 9 N force. Define whether testing is dry or wet, and use the method’s specified procedure and endpoint. For other materials or wear mechanisms, select conditions appropriate to the intended use and applicable test method.
How to Choose a Linear Abrasion Tester?
Understand How a Linear Abrasion Tester Works
A linear abrasion tester moves an abrasive head back and forth across a fixed specimen. A controlled load presses the head against the surface while the instrument records the stroke count. That repeated contact creates a narrow, measurable wear track. Simple in principle. Sensitive in practice.
The test result depends on more than cycle count. Abrasive grade, applied force, stroke length, speed, and specimen mounting can all change the wear pattern. ISO 12947-2, a textile abrasion test method, specifies test pressures of 9 kPa and 12 kPa for defined applications. These values offer useful context, but they are not automatic settings for every linear abrasion test. Match the method to the material and intended use.
When evaluating a tester, check whether its load is adjustable and its stroke remains consistent under repeated runs. Look for secure specimen clamps, replaceable abrasives, and clear cycle controls. Inspect the track, too: uneven wear may point to misalignment or inconsistent contact, not weak material alone. There is a practical limitation. A lab test cannot reproduce every scuff, dust particle, or pressure variation found in daily use. Record settings carefully, and compare samples only under the same conditions. A neat result can still mislead.
| Selection Dimension | What to Check | Why It Matters | Practical Selection Guidance |
|---|---|---|---|
| Operating principle | The instrument moves an abrasive tool back and forth along a straight path while applying a controlled load to the specimen. | Reciprocating contact can reproduce localized rubbing and wear more closely than broad, continuous rotary abrasion for some products. | Confirm that the stroke path, contact geometry, and motion match the type of wear the product is expected to experience. |
| Specimen type and size | Check specimen thickness, dimensions, flexibility, surface shape, and how it will be held in the fixture. | Secure, repeatable mounting helps keep the abrasive contact consistent throughout each test. | Choose a fixture that accommodates the actual sample without stretching, slipping, or obstructing the test area. |
| Abrasive tool | Review the available abrasive media, such as an abrasive tip, pad, cloth, or other specified contact material. | Abrasive type, condition, and contact area influence the wear pattern and can affect comparisons between tests. | Select media suitable for the material and test method. Define replacement or conditioning practices to support repeatability. |
| Applied load | Check the load range, available loading accessories, and how the force is applied to the contact point. | Load affects contact pressure and the severity of abrasion; inconsistent force can produce misleading comparisons. | Choose a tester that can apply the force required by the intended procedure and maintain it consistently during motion. |
| Stroke length and speed | Verify the available linear travel, reciprocation rate, and whether these settings are adjustable. | Travel distance and motion rate affect how often and how far the abrasive passes over the specimen. | Match the instrument’s operating range to the relevant test procedure or product-use simulation. Avoid assuming that a faster test is equivalent to a longer test. |
| Cycle or endpoint control | Look for a cycle counter, programmable stop, or a clear way to define and record the test endpoint. | Consistent cycle counts make it easier to compare samples tested under the same conditions. | Decide whether the test ends after a set number of cycles or when a defined change, such as visible damage, occurs. |
| Test environment | Determine whether temperature, humidity, wet contact, or other conditioning requirements apply to the material or procedure. | Material response and friction can vary with environmental conditions and specimen preparation. | Use appropriate conditioning and document environmental conditions when they are part of the test method or comparison plan. |
| Evaluation method | Identify how wear will be assessed: visual inspection, mass change, surface change, color change, or another defined measurement. | The tester creates the abrasion action, but the evaluation method determines how the resulting damage is reported. | Choose the assessment method before testing and use consistent lighting, measurement tools, and acceptance criteria where applicable. |
| Repeatability and documentation | Check adjustment procedures, maintenance needs, operating instructions, and the ability to record key test settings. | Controlled settings and documented procedures help different operators repeat and compare tests. | Record the abrasive media, load, stroke length, speed, cycle count, specimen preparation, and evaluation method for each test series. |
| Best-fit decision | Compare the tester’s motion, fixtures, load range, controls, and evaluation workflow with the intended material and test objective. | A suitable instrument is one that can reproduce the required contact conditions and support a consistent measurement—not simply one with the most settings. | Prioritize compatibility with the applicable test procedure or defined wear simulation, then confirm that the instrument can accommodate the samples and reporting needs. |
Compare Motion, Load, and Stroke-Setting Options
Start with the wear pattern your product experiences. A reciprocating motion suits repeated back-and-forth contact, such as fabric sliding against a surface. If your test method calls for another motion, confirm the instrument can reproduce it consistently. The right movement matters more than a long feature list. Small differences can change the wear track.
Next, match the applied load to the real contact condition and the test method. Too much force may damage a coating unrealistically; too little may hide meaningful wear. Check how the load is applied and whether it can be adjusted in suitable increments. Then review stroke settings. A longer stroke covers more surface, while a shorter one concentrates rubbing in a smaller area. Make sure the chosen range fits your sample size and test procedure. I’ve found that setup details are easy to overlook. They still affect the result.
Tips: Test a representative sample before settling on settings. Record motion, load, stroke length, cycle count, and conditioning details. Keep the specimen positioned the same way between runs. A neat result is not automatically a reliable one, so repeat the test and inspect whether the wear pattern is consistent.
Choose the test method before comparing linear abrasion testers. For textiles, check whether ASTM D4157’s oscillatory-cylinder procedure matches your specimen and intended claim. ISO 12947 uses a Martindale motion, so its results are not directly interchangeable with linear-stroke results. Small details matter. Confirm stroke length, speed, applied load, abrasive type, and the standard’s failure endpoint. A fixture should hold the sample flat without stretching it; uneven clamping can produce misleading wear tracks. For coated panels or soft materials, check whether the holder prevents slipping and keeps the contact area consistent.
Data recording matters just as much as the mechanism. Look for cycle counts, load, speed, stroke settings, test duration, and clear sample identification in every record. Exportable logs and time-stamped photographs make it easier to compare results across operators.
The U.S. EPA’s 2020 Advancing Sustainable Materials Management: 2018 Fact Sheet estimated that 17.0 million tons of textiles entered the U.S. municipal waste stream, with 11.3 million tons landfilled. That figure does not prove abrasion testing prevents waste, but it underlines why durability claims deserve careful evidence.
One detail is easy to miss: a tidy spreadsheet cannot correct a poorly aligned fixture. Record the setup, too. It feels repetitive, but that is often the useful part.
How to Choose a Linear Abrasion Tester?
Match Tester Specifications to Your Laboratory Requirements
Choosing a linear abrasion tester starts with the materials and tests your laboratory actually handles. List the sample types, dimensions, and surface finishes you expect to assess. A coated panel, a small plastic part, and a flexible textile may need different fixtures. Check that the tester’s stroke length, load range, and motion settings suit those samples. More adjustment is not automatically better.
Look closely at how load is applied and verified. A nominal setting is useful only when the applied force remains consistent during testing. Ask how the instrument is calibrated and how often calibration should be checked. Consider speed control, cycle counting, and whether the test area can hold your specimens securely. Small slips matter. A sample that shifts under the rubbing head can produce misleading wear patterns.
Your lab’s workflow matters, too. Confirm that operators can set up tests consistently, clean the contact surfaces, and record the settings used. If you follow a test method, compare its requirements with the tester’s available motion, load, and accessories before purchasing. Also check bench space, power needs, maintenance access, and data-export options. It is easy to focus on specifications and overlook daily handling. One practical trial with representative samples can reveal awkward fixtures or inconvenient setup steps. No single configuration fits every lab, and a detail you dismiss today may become a routine frustration.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.