How to Choose a Ceramic Insulated Band Heater in 2026?

Choosing a Ceramic Insulated Band Heater in 2026 requires more than comparing wattage and price. The right unit must fit the barrel diameter, operating temperature, control system, and production rhythm. A heater that looks powerful on paper may create cold bands, uneven melting, or unnecessary energy loss.

Materials engineer Dr. Robert W. Messler Jr. offers a useful principle for thermal design: “Performance depends on the system, not one component.” That idea matters here. A Ceramic Insulated Band Heater works with the machine surface, thermocouple placement, insulation, clamping pressure, and controller. Ignore one detail, and the heater may underperform. Small gaps can become large temperature problems.

This guide examines the practical choices behind modern band-heater selection. It considers ceramic-fiber insulation, maximum temperature, watt density, heater width, flexibility, and service life. It also explains how to read technical specifications without trusting every impressive number. Some assumptions deserve a second look. Higher wattage is not always better. Higher temperature ratings do not guarantee longer life. Even a reputable supplier can provide the wrong design when operating data is incomplete.

Expect a grounded comparison, not a glossy buying shortcut. Measure the barrel first. Check the control method. Think about heat loss around the machine. A few minutes with a caliper and infrared camera may reveal more than a sales brochure. The best Ceramic Insulated Band Heater is the one that delivers stable, efficient heat where the process actually needs it.
How to Choose a Ceramic Insulated Band Heater in 2026?

What Is a Ceramic Insulated Band Heater?

How to Choose a Ceramic Insulated Band Heater in 2026?

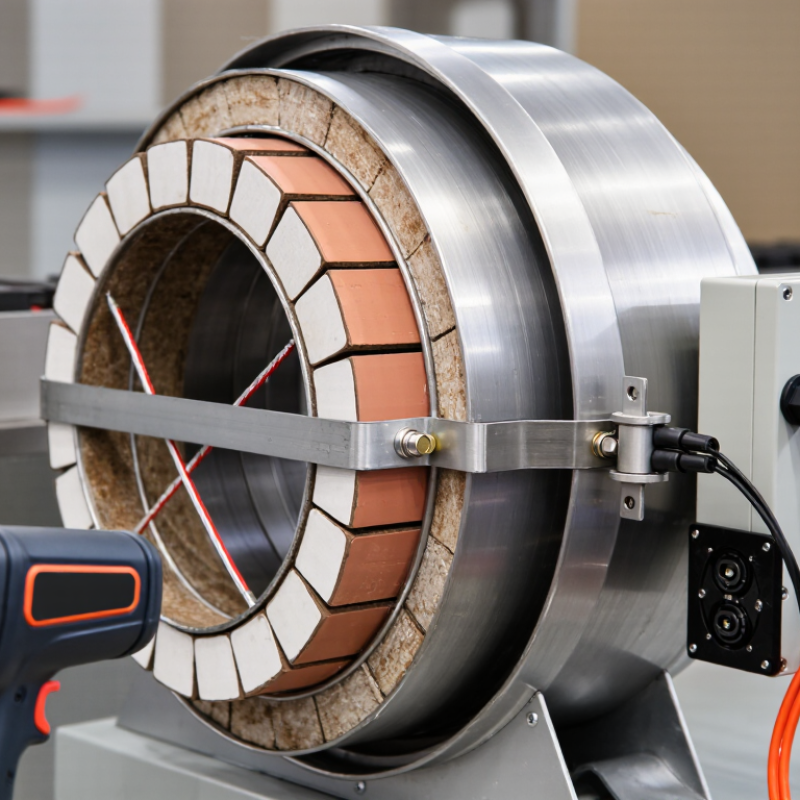
A ceramic insulated band heater is an electric heating jacket wrapped around a cylindrical surface. Its resistance coils sit inside ceramic modules, which retain heat and reduce direct contact with the metal shell. The heater transfers controlled heat to barrels, pipes, nozzles, and other round components.

Ceramic insulation matters. It improves heat retention and supports higher operating temperatures than many basic metal band designs. The U.S. Department of Energy reports that process heating consumes about 51% of manufacturing energy in the United States. Better heat control can therefore influence operating costs, material quality, and emissions. Small details count.

In practice, select the heater by diameter, width, voltage, watt density, and target temperature. A poorly fitted band can leave cold zones near the edges. Excessive watt density may scorch polymers or shorten heater life. Ceramic models usually suit injection molding, extrusion, and high-temperature processing, but they need firm mechanical contact. Loose mounting creates air gaps and uneven heating.

The IEC 60519 series stresses protection against thermal hazards in industrial electroheating systems. Temperature sensors, grounding, insulation clearance, and independent over-temperature protection deserve careful review. Ceramic elements can survive demanding cycles, yet they are not unbreakable. Rough installation may crack the insulation. Measure the barrel accurately, check the controller’s sensing position, and allow for thermal expansion. One overlooked gap can waste energy.
How to Identify Your Equipment’s Heating Requirements

How to Choose a Ceramic Insulated Band Heater in 2026?

How to Identify Your Equipment’s Heating Requirements

Start with the equipment, not the heater catalogue. Measure the barrel diameter, heated length, wall material, and available installation space. Record the target temperature, warm-up time, operating hours, and production cycle. Measure twice. A ceramic insulated band heater must fit tightly, but it should not crush fragile surfaces or obstruct sensors.

The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies process heating as roughly 51% of manufacturing energy use. This makes accurate heat planning commercially important, not merely technical. Calculate heat loss from the equipment surface, nearby airflow, material feed, and open ends. Then check voltage, phase, total wattage, and acceptable watt density. High watt density may heat quickly, but it can damage coatings or create uneven temperature zones.

Temperature control also deserves careful attention. Specify the sensor location, control tolerance, maximum surface temperature, and alarm response. Ceramic insulation helps reduce heat loss, yet it cannot correct poor contact or weak control logic. I have seen estimates fail because the material entering the barrel was much colder than expected. Keep it realistic. Allow a modest design margin, but avoid excessive power. The IEA’s Energy Efficiency 2023 report states that industry consumed about 37% of global final energy in 2022. That figure reinforces the value of measuring actual heat demand before selecting equipment. A perfect calculation is rare; documented assumptions make later adjustments safer.

How to Choose a Ceramic Insulated Band Heater in 2026?

How to Identify Your Equipment’s Heating Requirements

The chart shows typical reference ranges for common band-heater applications. Compare the required operating temperature with surface watt density when selecting a ceramic insulated band heater. Actual sizing should also account for equipment diameter, heater width, insulation, material heat capacity, heat loss, warm-up time, and temperature-control requirements.

How to Compare Heater Materials, Sizes, and Power Ratings

How to Choose a Ceramic Insulated Band Heater in 2026?

Material selection should match temperature, atmosphere, and maintenance exposure. Stainless steel offers practical corrosion resistance for many plastics processes. Nickel-based alloys suit higher temperatures and harsher environments, but they cost more. Ceramic insulation reduces heat loss and supports faster heating. The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies process heating as approximately half of manufacturing energy use. Small efficiency gains matter.

Size and power ratings need equal attention. Measure the barrel diameter, heater width, clearance, and clamping method before ordering. A loose band creates air gaps, uneven heating, and early failure.

Calculate watt density by dividing total watts by the heated surface area. For example, 1,000 watts across 0.1 square metre equals 10 kW/m². Compare that figure with the material supplier’s recommended range.

The IEA’s Energy Technology Perspectives 2024 reports that industry uses about 37% of global final energy, so oversizing is not harmless. It increases cycling and electrical demand.

I sometimes see wattage selected from old drawings. That is risky. Confirm voltage, controller limits, operating temperature, and sensor position on the actual machine. Use IEC 60519 guidance and qualified electrical inspection practices for safer installation.

How to Select the Right Temperature Control and Installation Features

Choosing a ceramic insulated band heater in 2026 requires more than matching diameter and wattage. Temperature control and installation details often determine real performance.

Start by defining the material, operating temperature, heating speed, and acceptable temperature variation. Measure the barrel surface, not only the machine’s display. A thermocouple should sit close to the heating zone and remain firmly attached. Too much distance creates delayed readings and unstable control. I have seen heaters cycle repeatedly because the sensor was placed against an insulated cover. It looked correct. It was not.

Choose a controller with proportional control, suitable sensor input, and clear alarm settings. Independent over-temperature protection adds a valuable safety layer. Confirm the heater’s voltage and power before installation. Incorrect electrical ratings can cause poor heating or premature failure. Keep terminals away from resin, oil, and moving components. Tighten connections evenly, but do not crush the ceramic insulation. Small gaps can create hot spots. That mistake is easy to miss.

Installation fit matters as much as controller selection. Clean the metal surface, remove burrs, and ensure the band sits flat around the cylinder. Use the specified clamping method, then recheck tightness after the first heating cycle. Ceramic components can shift slightly during expansion. Allow ventilation around wiring and inspect cables for heat damage. My own preference is to record surface temperature at several points during commissioning, although this step is sometimes skipped when production pressure rises. That shortcut deserves reconsideration.

How to Choose a Ceramic Insulated Band Heater in 2026? - How to Select the Right Temperature Control and Installation Features

Selection Dimension Typical Requirement Recommended Heater or Feature Why It Matters Key Selection Check
Operating Temperature Up to approximately 300 °C Standard ceramic insulated band heater with suitable electrical insulation Provides efficient barrel heating for many low-to-medium temperature processes. Confirm the heater's maximum sheath, insulation, and terminal temperature ratings.
High-Temperature Operation Approximately 300–600 °C, depending on the process High-temperature ceramic band heater with heat-resistant leads and terminals Ceramic insulation can support higher operating temperatures than many conventional insulated designs. Check the manufacturer's declared continuous operating temperature; do not use the short-term limit as a continuous rating.
Heated Cylinder Diameter Small, medium, or large cylindrical barrel Custom-diameter heater or segmented heater design Correct diameter improves contact, reduces air gaps, and helps maintain uniform heat transfer. Measure the actual barrel circumference or outside diameter after allowing for surface condition and tolerances.
Heater Width Narrow heating zone or extended axial coverage Single-width band for localized heating; multiple bands for long barrels Separate zones allow better temperature distribution and easier maintenance. Match each heater width to the required heating zone and avoid overlapping unless specifically permitted.
Voltage and Power Available supply voltage and required heat-up rate Heater selected by voltage, wattage, watt density, and circuit capacity Incorrect electrical sizing can cause slow heating, excessive surface temperature, or circuit overload. Use the relationship Current (A) = Power (W) ÷ Voltage (V) and verify the circuit, wiring, and switching capacity.
Watt Density Heat-sensitive material or standard metal processing Lower watt density for sensitive materials; higher watt density only when process conditions allow Watt density affects surface temperature, heat-up speed, and the risk of material degradation. Calculate watts per heated surface area and compare it with the process material's allowable temperature.
Temperature Sensor Closed-loop temperature regulation Thermocouple or RTD installed close to the actual control point Sensor location has a direct effect on measurement accuracy and process stability. Match the sensor type to the controller input and protect it from direct heater radiation where necessary.
Temperature Controller Stable process temperature with limited overshoot PID controller with adjustable proportional, integral, and derivative parameters PID control can improve stability compared with simple on/off control, especially during changing loads. Select a controller with the correct sensor input, output type, alarm functions, and supply voltage.
Control Output Frequent switching and accurate power modulation Solid-state relay or power controller, correctly rated for the heater load Electronic switching reduces mechanical contact wear during frequent temperature corrections. Provide a properly rated heat sink, overcurrent protection, and adequate cabinet ventilation.
Installation Fit Fast replacement or limited-access installation Hinged, split, or clamp-style band with accessible terminals A service-friendly design can reduce downtime during installation and replacement. Confirm hinge position, clamp direction, terminal clearance, and the available installation space.
Clamping and Contact Efficient heat transfer to a clean cylindrical surface Adjustable clamping hardware with close-fitting band geometry Poor contact or loose bands create hot spots, slow heat transfer, and premature heater failure. Clean the barrel, remove burrs, tighten evenly, and follow the specified installation clearance.
Thermal Insulation Reduced heat loss and lower external surface temperature External thermal insulation rated for the operating temperature Insulation can improve energy efficiency and protect nearby components and operators. Ensure insulation does not cover terminals, restrict ventilation, or exceed its own temperature rating.
Electrical Protection Industrial equipment with continuous operation Grounding, overcurrent protection, correctly rated leads, and suitable terminal covers Protection reduces the risk of electric shock, short circuits, and equipment damage. Follow applicable electrical codes and verify protective-earth continuity before energizing.
Maintenance Access Frequent inspection or high-utilization production Replaceable leads, accessible fasteners, and clearly labeled heating zones Accessible components simplify testing, troubleshooting, and planned replacement. Allow sufficient clearance for tightening, electrical testing, and safe heater removal.
Final Verification Before commissioning the heating system Documented inspection and controlled heat-up test A pre-start check helps identify wiring, fit, sensor, and temperature-control problems early. Verify resistance, insulation condition, grounding, sensor response, clamp tightness, and controller operation.

Note: Temperature ranges and heater configurations are typical engineering selection guidelines. Always confirm the final electrical, mechanical, thermal, and safety ratings against the heater and control-system documentation.

How to Check Safety, Efficiency, Durability, and Supplier Quality

How to Choose a Ceramic Insulated Band Heater in 2026?

Safety starts with the heater’s fit, not its catalogue wattage. Measure the barrel diameter, clamping gap, and heated length carefully. A loose band creates hot spots and wastes power. Check the insulation resistance with a calibrated megohmmeter before installation and after thermal cycling. The U.S. Department of Energy’s Industrial Decarbonization Roadmap reports that process heating represents about 51% of manufacturing energy use. Efficient heat transfer therefore matters. Select a heater with stable ceramic insulation, accurate thermocouple placement, and controllable watt density. Do not assume higher wattage means faster production.

Watch the first heating cycle.

Durability depends on expansion control and clean assembly. Ceramic elements can crack when clamps are overtightened or moisture is trapped inside. Ask for operating-temperature limits, insulation test records, and resistance readings from each production lot. The IEA’s Energy Efficiency 2023 report recorded a 2.2% improvement in global energy intensity during 2022, showing why small efficiency losses deserve attention. Still, laboratory figures may not match a dusty factory floor. I have seen heaters fail early because the sensor was mounted several centimetres away from the real hot zone.

Supplier quality needs evidence, not confident language. Request material certificates, batch traceability, dimensional inspection reports, and a clear warranty process. Verify the supplier’s quality certification and its actual manufacturing scope. Ask how rejected units are isolated. A polished certificate proves little if test data cannot be linked to your order. Compare sample heaters under the same voltage, temperature, and cycling conditions. The cheapest quotation may become the most expensive maintenance decision.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.