How to Choose the Right Blind Flanges?
Choosing the right Blind Flanges is not a simple matter of matching pipe diameter. A flange may fit the bolt circle and still fail the application. Pressure class, material compatibility, temperature, corrosion exposure, and sealing method all influence the decision. In practical procurement work, small errors often appear later as leaks, difficult maintenance, or delayed commissioning. The flange looks simple. The service conditions are not.
This guide approaches selection from an engineering and site perspective. It explains how to read flange dimensions, compare pressure ratings, verify facing types, and confirm material certificates. It also considers carbon steel, stainless steel, alloy options, gasket selection, bolting, and surface protection. Reliable choices depend on drawings, equipment data, applicable standards, and supplier quality records. Never rely on a product photograph alone. It hides too much.
A sound review should ask uncomfortable questions. Is the Blind Flanges product rated for the actual design pressure and temperature? Will the gasket remain stable after repeated opening? Does the supplier provide traceability and inspection documentation? These checks support safer, more predictable systems. They also prevent a common mistake: treating the lowest purchase price as the lowest total cost. Even experienced teams can overlook a detail. This article highlights those details, while acknowledging that site conditions and project specifications may change the final answer. Use the guidance with qualified engineers and verified standards.
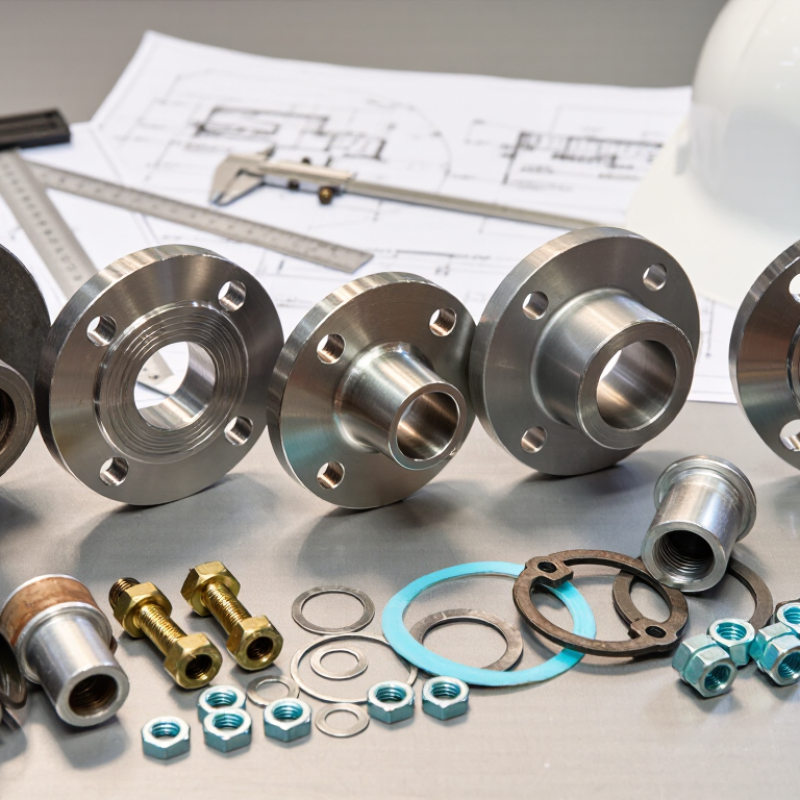
What Blind Flanges Are and How They Work
How to Choose the Right Blind Flanges?
A blind flange is a solid, disk-shaped component without a center opening. It closes the end of a pipe, valve, or pressure vessel. Unlike a standard flange, it blocks the entire flow path. Bolts clamp it against a mating flange, while a gasket creates the pressure seal.
During maintenance, this arrangement helps isolate equipment safely. It also supports pressure testing when installed according to an approved procedure. In field inspections, correct alignment and clean sealing faces often matter as much as flange size.
Choosing one requires more than matching the pipe diameter. Check the nominal size, pressure class, temperature range, material, and flange facing. Stainless steel may suit corrosive service, while carbon steel can fit many general applications. Confirm the gasket type and bolt dimensions together.
Standards such as ASME B16.5 or ASME B16.47 can guide dimensional selection, but the system engineer should verify the final choice. A flange that looks oversized may still have the wrong pressure rating. That mistake is easy to overlook.
Tips:
Inspect the sealing face for scratches, rust, and distortion. Confirm the gasket is centered before tightening. Use a calibrated torque method and follow the required bolt sequence. Do not reuse damaged bolts or compressed gaskets. Record the flange rating and material for future maintenance. Small details matter. Reduced-temperature service, vibration, or frequent removal may require a more careful review. I may sound cautious, but blind flanges sit directly against stored pressure.
How to Determine Pressure, Temperature, and Material Requirements
How to Choose the Right Blind Flanges?
Pressure and temperature should be assessed together, not separately. ASME B16.5 pressure-temperature tables show that a carbon-steel Class 150 flange may be rated at 285 psi at 100°F. A Class 300 flange reaches about 740 psi under the same conditions. These values are reference points, not automatic design approvals. Higher temperatures reduce allowable pressure. Confirm the rating at the actual operating and design temperatures.
Temperature also affects gasket performance, bolt stress, and flange leakage. Record normal operation, startup, shutdown, and upset conditions. A line carrying steam at 400°F needs different verification than a water line at 100°F. ASME BPVC Section II provides material strength data for design calculations. Still, field conditions can be less predictable. Thermal cycling is often underestimated.
Material selection should match the fluid and environment. Carbon steel is common for dry, non-corrosive service. Stainless steel may better resist moisture, chlorides, or aggressive chemicals. Low-temperature service requires impact-toughness verification, especially near freezing conditions. For hydrogen sulfide exposure, NACE MR0175/ISO 15156 provides material guidance. Check the flange, bolts, gasket, and pipe as one system. Mixing grades can create galvanic or sealing problems. A blind flange is not simply a thick steel plate. Verify dimensions, facing, bore compatibility, corrosion allowance, and test requirements before ordering. The uncomfortable question is simple: are the design conditions complete?
How to Select the Correct Size, Rating, and Facing Type
How to Choose the Right Blind Flanges?
Selecting a blind flange starts with the correct nominal pipe size, not the outside diameter alone. Match the flange’s bolt circle, bolt-hole count, and raised-face diameter with the mating flange. ASME B16.5 dimensional tables cover NPS 1/2 through NPS 24, while ASME B16.47 addresses larger sizes from NPS 26 through NPS 60. A blind flange has no bore, but its thickness still affects pressure resistance and deflection.
Pressure rating needs careful judgment. Class 150, 300, 600, and higher ratings are not simple pressure multiples. ASME B16.5 pressure-temperature tables show that allowable pressure changes with material and operating temperature. A flange rated for Class 300 at ambient conditions may require a lower limit in hot service. Check the design temperature, fluid, gasket, bolts, and corrosion allowance together. Do not select by pipe size alone.
Facing type must match the gasket and mating flange. Raised face is common for many process connections. Flat face can suit specific low-pressure or fragile-flange arrangements. Ring-type joint facing supports demanding high-pressure service, but the groove and metal ring must match exactly. Field inspections often expose a basic mistake: the flange size is correct, but the facing is wrong. I would also recheck the standard edition, because small dimensional differences can stop assembly. The latest ASME tables deserve a final review before ordering.
How to Check Standards, Compatibility, and Installation Conditions
Choosing the right blind flange begins with standards, not appearance. Confirm the piping code, nominal size, pressure class, facing, and material grade. ASME B16.5 covers many flanges up to NPS 24, while ASME B16.47 addresses larger sizes. EN 1092-1 may apply to European systems. Never mix drilling patterns casually. A small mismatch can prevent full gasket compression.
Compatibility also depends on temperature, fluid chemistry, and corrosion allowance. The NACE IMPACT study estimated global corrosion costs at US$2.5 trillion annually, equal to about 3.4% of global GDP. That figure makes material selection more than a paperwork exercise. Check whether stainless steel, carbon steel, or an alloy suits the service. Review gasket type, bolt material, and pressure-temperature ratings together. The flange may be rated correctly, yet the gasket may not be.
Tips: Measure the existing flange, bolt-hole diameter, and center-to-center spacing before ordering. Inspect the sealing face for scratches, rust, or weld spatter. During installation, clean threads and tighten bolts in a cross pattern with calibrated equipment. Record torque values and test conditions. Avoid relying only on visual alignment. Even experienced teams miss this. No checklist is perfect; site temperature, damaged threads, or uneven piping loads can change the result. Have a qualified engineer verify unusual services, high temperatures, and temporary isolation arrangements.
How to Compare Quality, Safety, and Long-Term Maintenance Needs
Choosing a blind flange requires more than checking diameter and pressure class. Quality begins with traceable material certificates, correct grade, controlled heat treatment, and a clean raised face. ASME B16.5 defines dimensions and pressure-temperature ratings, while ASME PCC-1 provides guidance for bolted joint assembly. These standards reduce guesswork, but they do not replace inspection.
Safety depends heavily on installation details. Verify gasket compatibility with the fluid, temperature, and pressure. Check bolt condition, thread engagement, and flange alignment before tightening. A calibrated torque tool helps, although torque alone cannot guarantee preload. Uneven tightening may leave a small leak path around the gasket. It can look acceptable during a quick visual check.
Long-term maintenance deserves equal attention. The NACE International IMPACT study estimated global corrosion costs at approximately US$2.5 trillion annually, equal to about 3.4% of global GDP. Blind flanges should therefore be inspected for corrosion under insulation, pitting, coating damage, and distorted sealing faces. Record material heat numbers, gasket type, bolt replacement, and inspection dates. This creates a useful maintenance history.
Field conditions are rarely perfect. A flange selected correctly on paper may still fail after vibration, thermal cycling, or poor access. That is the uncomfortable part. Periodic inspection intervals should reflect service severity, not habit. Sometimes replacing inexpensive bolts early is wiser than stretching their service life. Reliability is built through disciplined records, competent assembly, and honest review of previous failures.





