


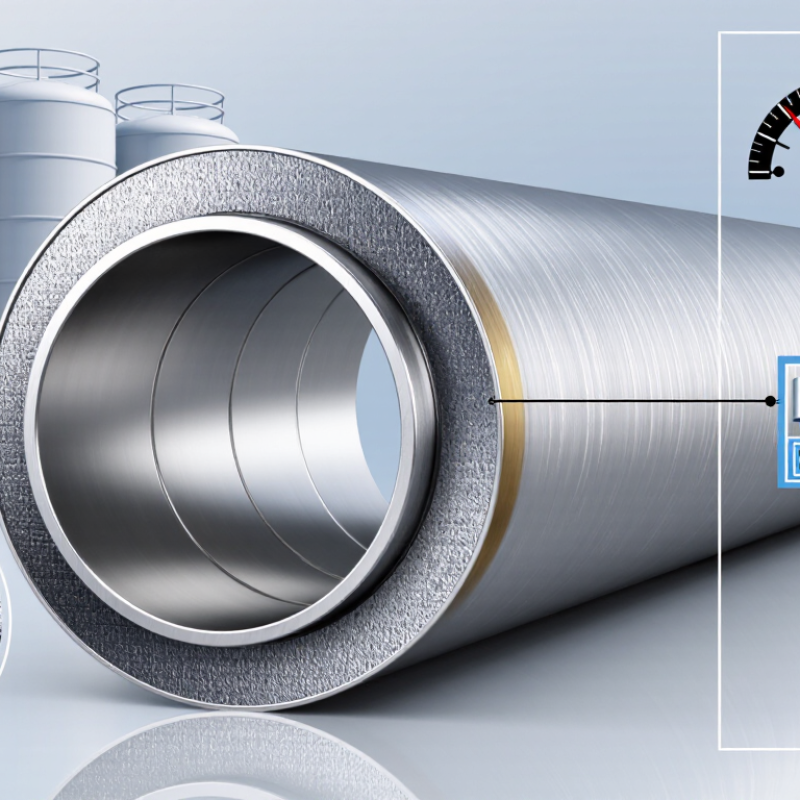
Buying an Overlay Welded Pipe is not simply a matter of comparing prices, diameters, or alloy names. The right choice must match the service environment, base pipe, weld overlay, and expected wear mechanism. A pipe carrying abrasive slurry may need different protection from one exposed to sour gas, chlorides, high temperature, or repeated pressure cycling. Small details matter. A rough bore can increase turbulence. Poor fusion can create hidden failure points. An unsuitable overlay may crack during fabrication or operation.
Dr. John C. Lippold, a respected welding metallurgy specialist, captures the central concern in this practical principle: “A sound weld begins with control of heat, materials, and procedure.” Buyers should treat that principle as a checkpoint, not decoration. Ask for the overlay alloy, welding process, thickness tolerance, dilution control, hardness data, and inspection records. Confirm whether testing covers ultrasonic examination, visual inspection, dimensional checks, and sample metallography. Also examine the supplier’s experience with similar pipe sizes and operating conditions. Experience helps, but it does not replace evidence.
The ten tips in this guide focus on decisions that are easy to overlook. They cover specification review, corrosion and abrasion assessment, weld quality, documentation, delivery risks, and lifecycle value. A cheaper Overlay Welded Pipe may appear attractive beside a higher-priced option. That comparison can be misleading. Maintenance access, downtime, replacement frequency, and field repair difficulty may change the real cost. No checklist is perfect. Even experienced buyers can miss an interaction between alloy chemistry and service conditions. Careful questions reduce that risk.
Overlay welded pipe combines a structural pipe with a metallurgically bonded alloy layer. The cladding protects the surface from abrasion, corrosion, or both. Its typical cladding thickness ranges from 3 to 6 mm. That range is practical, but it is not automatically suitable for every service condition.
Ask how the layer was deposited, such as by strip or wire welding. The method affects dilution, hardness, and surface uniformity. Request the base-metal grade, cladding chemistry, hardness results, and thickness tolerance. Check whether the measured thickness is nominal or minimum.
A 3 mm layer may be inadequate under severe impact, while 6 mm can increase weight and fabrication difficulty. Measure samples at several points, not only at the pipe end.
Look for records of ultrasonic testing, visual inspection, and weld-repair procedures. The cladding should show sound fusion without visible cracks, trapped slag, or excessive overlap.
Confirm the pipe’s inner diameter, straightness, and end preparation before installation. I have seen attractive surfaces hide uneven thickness, so appearance alone is weak evidence.
Ask for test samples from the actual production batch. Small details matter. Also question the supplier about bending, cutting, and field welding limits. Specifications sometimes leave these points unclear, and that gap can become an expensive problem later.
10 Tips for Buying Overlay Welded Pipe
Match the base metal to the process fluid, pressure, and fabrication method. Tip 1: Confirm whether carbon steel, stainless steel, or a nickel alloy supports the pipe’s structural role. Tip 2: Select the overlay alloy for corrosion, erosion, or high-temperature oxidation. Tip 3: Compare thermal expansion rates before approval. At 600°C, mismatched metals can create stress, distortion, or hidden cracking. A datasheet alone is not enough.
Tip 4: Ask for the qualified welding procedure and dilution control records. Excessive base-metal mixing may reduce alloy performance. Tip 5: Check overlay thickness after machining, not only before it. Tip 6: Review hardness, chemistry, bond quality, and non-destructive test results. Tip 7: Consider thermal cycling, because repeated heating and cooling can be harsher than steady operation. In field reviews, this detail is often missed. I have seen apparently strong pipes fail near poorly designed transitions.
Tip 8: Verify creep strength and oxidation resistance at the actual service temperature. Tip 9: Confirm dimensional tolerances, roundness, and end preparation for installation. Tip 10: Request traceable material certificates and test records. Include weld maps and inspection acceptance criteria. Do not assume “600°C rated” means suitable for every fluid or pressure. Service data can be incomplete, and that uncertainty deserves a written engineering review before purchase.
When buying overlay welded pipe, verify chemistry before reviewing surface appearance. ASTM A265 covers nickel and nickel-base alloy clad steel plate, not every pipe construction. Confirm that the purchase specification applies to your pipe design. The latest applicable ASTM edition should identify alloy grade, base metal, and required chemical limits.
Request the mill test certificate for each heat number. Compare carbon, chromium, nickel, molybdenum, iron, and trace elements against the specified ASTM grade. Portable X-ray fluorescence testing can screen chromium and nickel, but it cannot reliably measure carbon. Use optical emission spectroscopy or laboratory combustion analysis when carbon affects corrosion or weldability. Record the test location, method, calibration status, and laboratory uncertainty. Small details matter.
ASME BPVC Section IX, 2023 edition, addresses welding procedure and performance qualification, not product chemistry limits. Review the qualified welding procedure specification beside the certificate. Check filler-metal classification, preheat, interpass temperature, heat input, and post-weld treatment. These controls influence dilution between the overlay and substrate. A compliant chemistry report cannot rescue a poorly qualified weld. I have seen paperwork look complete while heat numbers were missing from cut sections. That is a serious weakness. ASTM A265-2023 also requires careful attention to clad material requirements, so buyers should document where the standard applies and where it does not.
The chart compares the standard atomic weights of elements commonly reported when verifying nickel-alloy overlay chemistry, including nickel, chromium, molybdenum, iron, and carbon. These values are reference data, not acceptance limits. ASTM A265 addresses nickel and nickel-base alloy clad plate, while the applicable material specification should define the chemical limits for the purchased pipe. ASME Section IX is used to qualify welding procedures and personnel, so the purchase review should also confirm that the qualified welding documentation covers the specified overlay material and essential variables.
When buying overlay welded pipe, do not judge quality from photographs alone. Ask how bond integrity was verified across the full weld area. Ultrasonic testing can reveal lack of fusion, while macro sections may confirm the interface more directly. Request test locations, acceptance criteria, and complete inspection records. A polished certificate is not enough.
Hardness deserves equal attention. Excessive hardness can increase cracking risk, while low hardness may reduce wear resistance. Ask for a hardness map covering the overlay, bond zone, and base pipe. The testing method, load, spacing, and calibration status should be recorded. Compare results with the project specification, not only with a supplier’s typical values. Small variations may matter.
A 100% visual inspection should cover the entire accessible surface, not a convenient sample. Inspectors should check for cracks, pores, undercut, overlap, uneven bead shape, and exposed base metal. Bright lighting and a clean surface make small defects easier to see. Require dated inspection images and traceable pipe identification. Still, visual inspection cannot prove internal fusion. That limitation is easy to overlook. I would also confirm who performed the inspection and whether an independent review was used. In practice, the strongest purchase decision combines documented bond testing, controlled hardness measurements, and honest visual reporting.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.


