


How to Choose a Pneumatic Bending Machine?

Choosing the right Pneumatic Bending Machine requires more than comparing prices and advertised pressure ratings. The correct model should match your materials, production volume, bend angles, and available workshop space. A machine handling thin aluminum may struggle with stainless steel. Check the maximum sheet thickness, working width, bending radius, and air consumption before making a decision. Small details matter.

Experienced operators usually begin with the workpiece, not the machine brand. Measure a typical sheet, inspect its surface finish, and identify the tightest required bend. Then compare the machine’s force, die design, stroke length, and control method. A stable frame reduces vibration, while clear adjustment markings help operators repeat accurate bends. Ask suppliers for test results, maintenance guidance, and realistic cycle-time data. Do not rely only on polished demonstrations.

Safety deserves equal attention. Look for guarded moving parts, emergency controls, dependable foot pedals, and accessible maintenance points. Confirm that your compressor can provide clean, steady air at the required pressure. Otherwise, performance may fluctuate during long production runs. A perfect choice rarely exists. Your first estimate may also be wrong. Recheck actual workloads, future material changes, and operator skill levels before ordering. Reliable suppliers should explain limitations, not hide them. With practical measurements, documented specifications, and feedback from trained users, you can select a Pneumatic Bending Machine that delivers consistent results without creating avoidable operating costs.
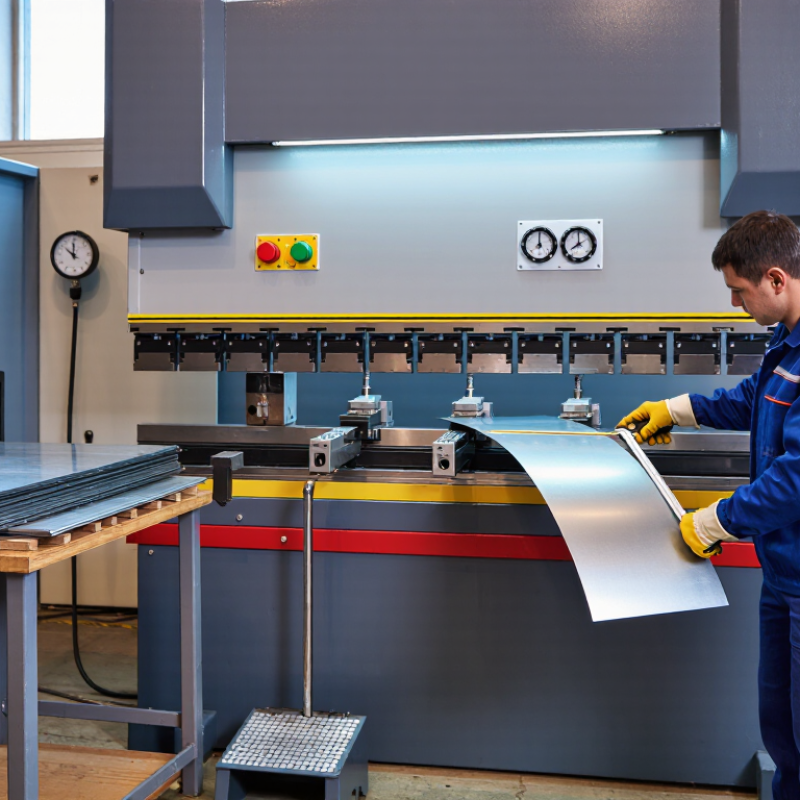
How to Choose a Pneumatic Bending Machine?

Understand How Pneumatic Bending Machines Work

How to Choose a Pneumatic Bending Machine?

A pneumatic bending machine converts compressed air into controlled mechanical movement. Air enters a cylinder through a directional valve. The piston then pushes a linkage, punch, or bending die. When the valve reverses, the piston returns. The basic force estimate is simple: cylinder force equals pressure multiplied by piston area. Real results are less tidy. Friction, pressure loss, tooling geometry, and material springback all reduce effective force.

The U.S. Department of Energy’s Compressed Air Systems Sourcebook reports that leaks can waste 20–30% of compressor output. That figure matters when comparing machines. A small cylinder may appear economical, yet it can cycle slowly under unstable pressure. Check the required bending force, stroke length, throat depth, cycle rate, and air consumption. Also inspect the regulator, filter, hoses, and exhaust mufflers. A pressure gauge should remain visible near the actuator.

ISO 4414 emphasizes safe pneumatic-system design, including controlled exhaust and protection against unexpected movement. During selection, match the machine to the material thickness and daily workload, not only its maximum rating. Leave practical capacity for variation. In workshop testing, a 90-degree bend may open slightly after release. That result can change with grain direction and tooling wear. A calculation helps, but one sample bend often reveals more than a perfect spreadsheet.


Identify the Materials, Shapes, and Bending Requirements

How to Choose a Pneumatic Bending Machine?

Identify the material before comparing machine specifications. Mild steel, stainless steel, and aluminum require different force, tooling, and springback allowances. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023, showing the material’s enormous industrial range. Aluminum behaves differently. The International Aluminium Institute recorded about 70.6 million tonnes of primary aluminum production in 2023. Its lower density does not mean every sheet bends easily. Alloy, temper, thickness, and grain direction still matter. Measure twice.

Shape selection is equally important. A shallow V bend needs less stroke than a deep U channel. Narrow flanges may require compact tooling, while large panels need sufficient throat depth and table support. Check the minimum inside radius, maximum sheet thickness, bend length, and required angle repeatability. For visible parts, even small springback can create costly rework. A practical trial with the actual material is more reliable than a catalog chart. Material batches vary, and that is easy to underestimate.

Review the air system, not only the bending force. The U.S. Department of Energy reports that compressed-air leaks can waste 20–30% of compressor output. Confirm working pressure, flow capacity, cylinder response, and recovery time during repeated cycles. A machine may bend one sample correctly, then slow noticeably in production. Record the target angle, cycle time, tooling change frequency, and acceptable tolerance. Do not guess. If the job involves thick steel, complex profiles, or tight tolerances, pneumatic capacity may be insufficient and deserves careful reassessment.

Evaluate Machine Capacity, Accuracy, and Operating Speed

How to Choose a Pneumatic Bending Machine?

Evaluate the machine’s capacity against your actual materials, not your best-case plans. Check maximum bending length, material thickness, and allowable pressure. A machine rated for 2,000 millimeters may struggle with thick steel across the full width. Ask for test bending with your own sheet samples. Watch for frame movement, uneven folds, and pressure loss. These details reveal more than a catalog specification.

Tips: Record the bend angle at several points. Measure after releasing the sheet. Small angle differences can affect assembly quality. Choose a machine with adjustable pressure and a clear back gauge. A simple control panel also reduces training errors. Do not ignore noise, leaks, or slow cylinder movement. They often indicate future maintenance work.

Accuracy depends on tooling condition, machine rigidity, and operator setup. Inspect the upper and lower tools for wear before comparing results. Operating speed matters, but faster is not always better. A rushed return stroke can damage edges or create inconsistent positioning. In practical evaluations, I prefer stable cycles over impressive empty-running speed. Still, my first assessment can be wrong when material batches vary. Repeat the test with different thicknesses and operators. Confirm repeatability after several cycles, not just one successful bend. Look for accessible service points, reliable gauges, and documented safety procedures. These features support consistent production and safer daily operation.

Compare Control Systems, Safety Features, and Maintenance Needs

When choosing a pneumatic bending machine, examine the control system before comparing speed. Basic relay controls may suit repetitive work, but PLC or CNC controls provide better angle consistency and fault diagnosis. Ask for cycle records, not only brochure figures. A useful controller should display pressure loss, sensor errors, and emergency-stop status clearly. Short menus help operators wearing gloves. They matter.

Safety deserves a practical test. The U.S. Bureau of Labor Statistics reported about 2.6 million nonfatal workplace injuries and illnesses in private industry during 2023. That figure supports careful guarding, not merely faster production. Check for two-hand controls, light curtains, interlocked guards, emergency stops, and automatic pneumatic pressure release. ISO 13849-1:2023 provides a recognized framework for evaluating safety-related control systems. However, compliance claims need verification through risk assessment and machine-specific testing. I would not trust a certificate alone.

Maintenance needs can decide the real operating cost. Inspect the air filter, regulator, lubricator, hoses, cylinders, and seals during routine service. Clean, dry compressed air reduces valve sticking and cylinder wear. The compressed-air network should also be checked for leaks with an ultrasonic detector or pressure-decay test. Keep a log of pressure, cycle count, repairs, and calibration results. Some machines appear simple, yet neglected moisture can create expensive downtime. A detailed maintenance schedule is useful, but operators may still miss early vibration or uneven bending. Training must address that gap.

How to Choose a Pneumatic Bending Machine? - Compare Control Systems, Safety Features, and Maintenance Needs

Comparison Dimension Basic Pneumatic Control PLC-Based Control CNC Electro-Pneumatic Control Selection Guidance
Typical application Simple, low-volume bending and forming tasks Regular production with repeatable part programs High-mix production requiring multiple programmed axes Match the control level to production volume, part variety, and tolerance requirements.
Operator interface Push buttons, foot pedal, pressure regulator, and manual valves Touchscreen or keypad with stored recipes and parameter access Graphical program editor with axis positioning and sequence control Choose an interface that operators can use without bypassing safety procedures.
Programming capability Usually no part-program storage; settings are adjusted manually Stores commonly used bending sequences and machine settings Stores multi-step programs, tool data, bend sequences, and axis positions Program storage reduces setup errors when the same parts are produced repeatedly.
Positioning and repeatability Dependent on operator technique and mechanical stops Improved consistency through sensors, timers, and programmed stops Highest consistency when the machine is correctly calibrated and tooling is stable Ask for a documented repeatability specification under defined material and load conditions.
Setup time Short for simple jobs, but manual adjustment increases with part complexity Moderate; stored settings can shorten repeat jobs Low for repeat work after programming, but initial programming takes longer Consider total setup time, including tooling, test bends, and first-piece inspection.
Pressure and force adjustment Manual regulator and valve adjustment Controlled through programmed pressure, timing, or stroke parameters Coordinated pressure, stroke, speed, and axis settings where supported Confirm that the control system can handle the material thickness and required forming force.
Essential safety features Emergency stop, guarded pinch points, foot-pedal protection, and pressure relief All basic features plus monitored guards, safety relays, and controlled restart All PLC features plus safety-rated axis monitoring and programmable safe limits Verify compliance with applicable local machinery-safety requirements before purchase.
Emergency-stop behavior Stops the control signal and exhausts or isolates pneumatic energy as designed Stops the cycle and prevents automatic restart after reset Stops motion through safety circuits and requires a deliberate reset sequence Check the actual stopping method, reset logic, and residual stored energy.
Air-quality requirements Requires clean, dry, regulated compressed air; filtration is essential Requires stable air pressure plus protection for valves and sensors Requires stable air quality and pressure to maintain programmed performance Confirm operating pressure, air consumption, filtration grade, and compressor capacity.
Daily maintenance Drain filters, inspect hoses and fittings, check leaks, and clean tooling Perform basic checks plus inspect sensors, cables, and control-panel alarms Perform basic checks plus review diagnostic messages and axis feedback Use a written checklist and record leaks, abnormal noise, and safety faults.
Periodic maintenance Inspect seals, valves, regulators, cylinders, fasteners, and mechanical stops Perform basic service plus verify I/O, sensor alignment, and program backups Perform basic service plus calibration, backup management, and safety-function testing Follow the machine manual; intervals depend on duty cycle, environment, and air quality.
Troubleshooting difficulty Generally low; common faults are air leaks, pressure loss, or worn seals Moderate; requires pneumatic and electrical diagnostic skills Higher; may require controls, sensor, motion, and calibration expertise Evaluate in-house skills and the availability of technical support and spare parts.
Energy efficiency considerations Air consumption can rise if the machine cycles frequently or has leaks Better cycle management can reduce unnecessary air use Optimized sequences may reduce idle time, but controls and sensors add complexity Compare air consumption per cycle, standby demand, and compressor operating cost.
Best fit by production scale Occasional or low-volume production Small-to-medium batch production Frequent production with complex, repeatable bend sequences Select the simplest system that meets required accuracy, productivity, and safety levels.
Note: The comparisons describe typical configurations. Actual performance, air consumption, safety functions, maintenance intervals, and repeatability depend on machine design, tooling, material, operating conditions, and the manufacturer’s specifications.

Select the Best Machine for Your Budget and Production Goals

Choosing a pneumatic bending machine starts with your production goals, not the lowest price. Estimate your daily bending volume, material thickness, bend length, and required accuracy. A small workshop may need a compact machine with moderate pressure and simple tooling. A busy fabrication line needs stronger construction, faster cycling, and a duty rating suited to continuous work. Check whether your existing air compressor can maintain stable pressure. Weak air supply can reduce bending consistency.

Tips: Compare the complete cost, not only the purchase price. Include tooling, compressor upgrades, installation, maintenance, energy use, and operator training. Ask for test bends using your actual material. Measure the angle, surface marks, repeatability, and cycle time. A useful test reveals more than a sales sheet.

I once underestimated tooling costs on a budget machine. The initial saving disappeared after several urgent replacements. That experience changed my selection process. I now give priority to accessible service parts, clear technical documents, and adjustable pressure controls. For occasional work, a basic model may provide better value than an oversized system. For production work, downtime matters more than a slightly lower invoice. Leave some capacity for future orders, but avoid paying for features your operators will never use. Reliability is measurable through inspection records, warranty conditions, and practical feedback from experienced users. Check those details carefully.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
