How to Choose a Motorcycle Assembly Line?

Choosing a Motorcycle Assembly Line is a production decision, not merely an equipment purchase. The right system must match product design, output targets, workforce skills, and available floor space. A line that looks efficient in a showroom may create delays beside your actual warehouse. That detail matters. This guide explains how to compare line layouts, station balance, tooling, testing, maintenance, and supplier support. It also considers worker safety, quality control, energy use, and applicable manufacturing standards.

Experienced production teams begin with demand forecasts and takt time, then verify every assumption. They measure frame movement, fastening points, inspection steps, and material travel before approving equipment. A practical assessment should include sample builds, operator trials, noise checks, and emergency-stop verification. Ask suppliers for documented accuracy, service response times, spare-parts plans, and installation references. Reliable vendors explain limitations clearly. Be cautious with impressive speed figures. They may exclude changeovers, inspections, training, or minor stoppages.

The best choice often balances automation with human judgment. Full automation can improve consistency, yet it may increase cost and maintenance complexity. Manual stations can offer flexibility, but they demand disciplined training and inspection. Your decision should reflect current production and realistic growth, not optimistic projections. I have seen evaluations weaken when teams ignore lighting, ergonomics, or rework space. Those omissions become expensive later. Use measurable criteria and invite engineering, quality, maintenance, and operators into the review. A thoughtful selection process reduces operational surprises and supports dependable motorcycle production.
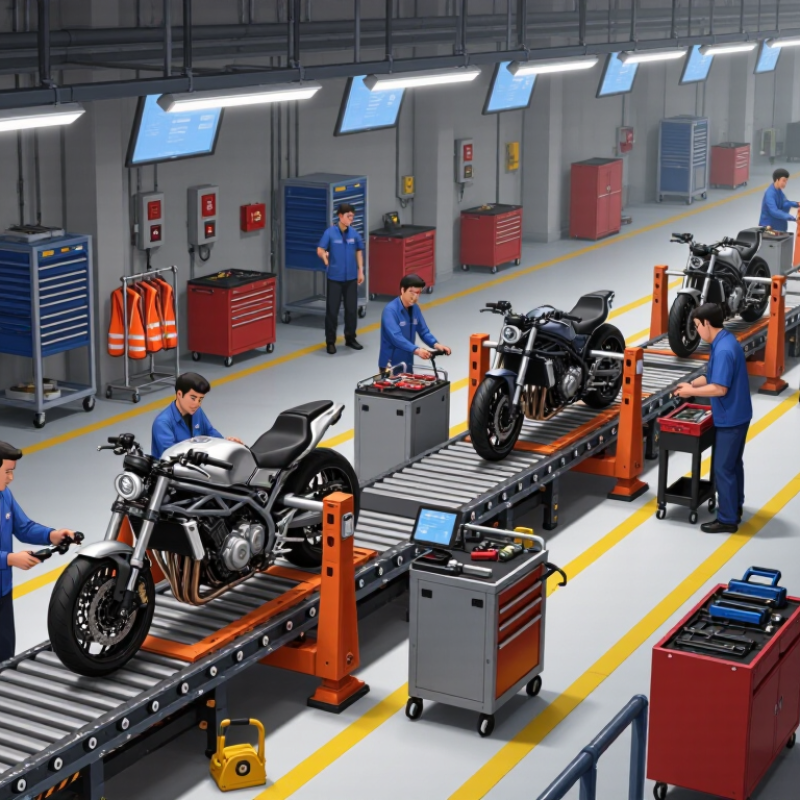
How to Choose a Motorcycle Assembly Line?

Define Production Requirements and Motorcycle Assembly Goals

How to Choose a Motorcycle Assembly Line: Define Production Requirements and Motorcycle Assembly Goals

A suitable assembly line begins with measurable production requirements. Define annual volume, shift patterns, motorcycle variants, quality targets, and available floor space.

For example, 480 motorcycles per eight-hour shift require a 60-second takt time before losses. At 90% line availability, the practical target falls near 54 seconds. That number affects conveyor speed, workstation balance, staffing, and buffer size. It also exposes weak assumptions early.

Market direction matters. The International Energy Agency reported that global electric two- and three-wheeler sales exceeded 10 million units in 2023, with most sales in China. Grand View Research estimated the global motorcycle market at USD 106.8 billion in 2022. These figures suggest growing variety, not simply higher volume. A line designed for one engine layout may struggle with battery packs, wiring checks, or different frame dimensions.

Set assembly goals beyond output. Specify first-pass yield, torque traceability, rework limits, changeover time, and operator safety. A practical target might include 98% first-pass yield and digital records for every critical fastener.

Yet perfect plans rarely survive the factory floor. I have seen efficient lines lose time because parts arrived in mixed bins. Leave room for model changes, training, and unexpected stoppages. A smaller, flexible line may outperform a faster line that cannot adapt.
Assess Assembly Line Types and Configuration Options

Choosing a motorcycle assembly line starts with product variety, not equipment catalogs. In practical planning, compare frame sizes, engine options, and expected daily volume. A manual line suits frequent model changes and lower output. It also depends heavily on operator skill. A semi-automatic line adds controlled fastening, lifting, and inspection steps. It can improve consistency without removing useful human judgment. Fully automatic systems support stable, high-volume production, but they need strong maintenance skills and careful process validation. More automation is not always better.

Configuration should follow the work content at each station. Map the takt time, then balance tasks across stations. Keep wheel fitting, brake adjustment, wiring, and fluid checks within safe reach. A straight conveyor simplifies planning, while a U-shaped layout can reduce walking and support smaller teams. Modular fixtures help when models share a frame but use different components. Adjustable torque tools, error-proofing sensors, and barcode records strengthen traceability. However, sensors can create false alarms when calibration or lighting is ignored. That detail is easy to underestimate.

Review the line with production, quality, maintenance, and operators before purchase. Their feedback exposes awkward lifting points and inspection steps that drawings miss. Check conveyor access, spare capacity, emergency stops, and cleaning areas. Leave room for future stations. Not too much. An efficient line should meet output targets while protecting people and preserving inspection discipline. Test one representative model before expanding the configuration. Early assumptions often fail during the first busy shift. That failure is useful when the team records it and adjusts the design.

How to Choose a Motorcycle Assembly Line? - Assess Assembly Line Types and Configuration Options

Assembly Line Type Typical Use Best Production Volume Flexibility Automation Level Main Advantages Key Limitations
Fixed-Position Assembly The motorcycle remains in one location while workers, tools, and parts move around it. Low volume, prototypes, special models, and highly customized motorcycles. Very high Low to moderate Simple layout, low initial investment, and easy product changes. Longer assembly time and more material movement between operations.
Straight Conveyor Line Motorcycles move sequentially through dedicated workstations on a linear conveyor. Medium to high volume with relatively stable product specifications. Moderate Moderate to high Clear process flow, predictable takt time, and efficient labor utilization. A station delay can affect downstream operations; expansion may require more floor space.
U-Shaped Assembly Line Workstations are arranged in a U shape to bring the beginning and end of the process closer together. Medium volume and mixed-model production. High Moderate to high Shorter walking distances, improved operator communication, and efficient space usage. Requires careful balancing and may be unsuitable for very large products or heavy handling.
Overhead Conveyor Line Frames or partially assembled motorcycles are suspended and transported above the floor. Medium to high volume where floor space and material flow are important. Moderate Moderate to high Keeps aisles clear, supports continuous flow, and reduces some manual transport activities. Higher structural requirements, more complex maintenance, and limited flexibility for unusual loads.
Pallet-Based Conveyor Line A motorcycle or frame is secured on a reusable pallet that travels through controlled stations. Medium to high volume with multiple models or variants. High Moderate to high Supports model identification, workstation routing, traceability, and controlled positioning. Pallet cost, return logistics, and fixture changes must be managed carefully.
Flexible Assembly Cell A compact group of stations performs several operations with manual or semi-automated handling. Low to medium volume and frequent product changes. Very high Low to moderate Fast changeovers, modular expansion, and good suitability for mixed-model production. Lower maximum throughput and greater dependence on operator skills.
AGV-Based Assembly System Automated guided vehicles transport pallets between assembly, inspection, and material-handling areas. Medium to high volume with changing routes or multiple production zones. Very high High Scalable routing, digital tracking, and reduced fixed-conveyor dependency. Higher software and safety requirements; performance depends on traffic management and battery planning.
Demand and Takt Time
Calculate required output from available production time and customer demand. A practical line should include allowance for breaks, minor stoppages, and planned maintenance.
Product Variety
Mixed-model production usually benefits from adjustable fixtures, barcode or RFID identification, recipe-controlled tools, and flexible material presentation.
Ergonomics and Safety
Consider lift assists, adjustable work heights, torque reaction control, guarded moving parts, emergency stops, and safe access for maintenance.
Quality and Traceability
Select in-process inspection, torque-angle monitoring, leak testing, electrical testing, end-of-line functional checks, and digital production records where required.

Compare Key Equipment, Automation, and Flexibility Features

How to Choose a Motorcycle Assembly Line?

Compare Key Equipment, Automation, and Flexibility Features

A capable motorcycle assembly line starts with suitable equipment, not maximum automation. Review frame fixtures, torque tools, wheel stations, inspection gauges, and conveyor systems together. Each station should support stable positioning and repeatable work. Adjustable fixtures matter when frame sizes or models change. Poor fixture access can create delays and operator fatigue.

Automation should match production volume and process risk. Automatic torque control improves consistency and records tightening results. Vision inspection can identify missing fasteners, incorrect parts, or uneven labels. However, sensors need clean lenses, clear lighting, and regular calibration. Otherwise, advanced equipment may produce confusing alarms. That is an expensive weakness.

Flexibility deserves equal attention. Choose modular stations, movable tool balancers, and software with simple recipe changes. A mixed-model line can reduce changeover time when demand shifts. Ask how quickly one operator can adjust a station safely. Check spare-part availability, maintenance access, and training requirements before approval. A compact line may appear efficient, but limited access can slow repairs. This detail is easy to underestimate. Pilot testing with real components often reveals awkward reaching, cable interference, or unreliable scanning. Leave room for improvement; the first layout is rarely perfect.

Evaluate Suppliers, Installation Support, and Safety Standards

How to Choose a Motorcycle Assembly Line?

A reliable supplier should understand your motorcycle models, production volume, and floor layout. Ask for documented cycle times, maintenance records, and references from comparable factories. A polished factory tour can still hide weak after-sales support. Request a live demonstration using similar frames, engines, and torque requirements. Check whether the supplier can adjust fixtures when your design changes. Small details matter, such as tool balancing, barcode tracking, and accessible service panels.

Installation support should include layout planning, operator training, commissioning, and clear troubleshooting documents. Confirm who supervises installation and how quickly technicians respond remotely or onsite. Safety evidence is equally important. Review risk assessments, emergency-stop locations, guarding, electrical protection, and safe access around conveyors. Ask whether the system follows recognized standards, such as ISO 12100 and ISO 13849, while checking local legal requirements. Do not accept certificates without verifying their scope. A mistake here can become expensive.

Tips: Ask for a complete acceptance checklist. Test the line under normal and worst-case conditions. Observe noise, heat, cable routing, and operator movement. Train maintenance staff before handover. Leave time for corrections; real commissioning rarely goes perfectly. One overlooked sensor or awkward tool position may slow every station. Suppliers should explain failures honestly, not hide them behind polished presentations.

Calculate Total Costs, Capacity, and Long-Term Return on Investment

How to Choose a Motorcycle Assembly Line?

A motorcycle assembly line should be evaluated through total cost, usable capacity, and long-term return on investment. Capacity is not speed. Calculate it from cycle time, shifts, working days, uptime, and first-pass yield. For example, an eight-minute cycle, two eight-hour shifts, 250 working days, and 85% OEE produce about 25,500 units annually. OEE means overall equipment effectiveness. The 85% assumption is demanding, so validate it with existing factory records. A slower line with stable quality may outperform a faster line with frequent stoppages.

Total cost includes equipment, tooling, installation, software, operator training, energy, maintenance, spare parts, floor changes, and production downtime. Add inspection systems and safety upgrades. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023, showing continued automation growth. However, automation does not automatically create profit. Deloitte’s 2023 Smart Manufacturing and Operations Survey found that 86% of manufacturers view smart manufacturing as important for competitiveness, but implementation still requires disciplined financial control.

Estimate return using incremental contribution margin, not sales revenue. Subtract labor, maintenance, energy, scrap, financing, and expected downtime from annual gains. Then divide the result by the complete installed investment. Include a sensitivity test for 70%, 80%, and 90% utilization. Real factories rarely match spreadsheets. Demand may weaken. Training may take longer. Rework may surprise you. Recheck every assumption with supplier guarantees, factory trials, and maintenance data. That evidence matters.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.