


How to Choose the Right Drywall Screw for Global Projects

Choosing the right Drywall Screw is a small specification decision with consequences across an entire project. Screw length, thread pattern, head design, and coating must suit the board, framing, installation method, and exposure conditions. A screw that works well in timber may perform poorly in light-gauge steel. The wrong length can also leave the board loose or damage its face. Small details matter.

Global projects add another layer. Materials, climate, available fasteners, and project specifications differ by region. The UNEP and GlobalABC Global Status Report for Buildings and Construction 2024/25 reports that buildings and construction accounted for 32% of global energy use and 34% of global carbon dioxide emissions in 2023. Those figures do not measure screw performance, but they underline why durable assemblies and avoidable rework deserve attention. Replacing a failed fastener can mean more than opening a tool case; it may require repairs, labor, and replacement board.

Reliable selection starts with the actual assembly, not a generic product label. ASTM C1002 covers specified steel screws for attaching gypsum board to wood or light-gauge steel framing; ASTM C954 addresses drill screws for gypsum board on steel framing. Project teams should confirm the current standard, local requirements, and manufacturer guidance before specifying. Corrosion exposure matters, too. A coating suitable for a dry interior may not suit a humid site. There is no universal shortcut. Even a tidy rule of thumb can miss an unusual substrate or installation condition. That is worth checking.
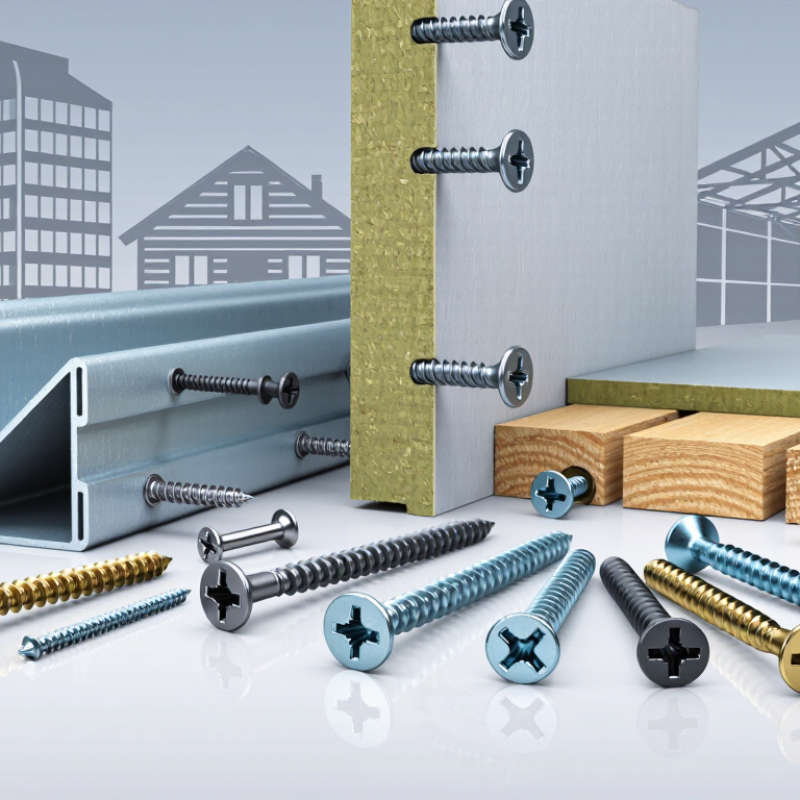
How to Choose the Right Drywall Screw for Global Projects

Understanding Drywall Screw Types and Their Core Functions

Drywall screws look similar, but their functions differ sharply. Coarse-thread screws grip wood studs with fewer turns. Fine-thread screws suit light-gauge steel framing and reduce thread deformation. Self-drilling points create their own openings in thicker steel sections. Cement-board screws use harder cores and corrosion-resistant finishes.

Head design also matters. A bugle head sits nearly flush without tearing the paper face. The correct length should penetrate the framing securely, but not extend dangerously behind it. ASTM C1002 covers screw requirements for gypsum board applications, while EN 14566 addresses mechanical fasteners in gypsum plasterboard systems. These standards support comparison, not automatic approval for every country.

Project scale makes consistency essential. The U.S. Census Bureau reported about 1.45 million privately owned housing completions in 2023. Small fastening errors can multiply across thousands of rooms. UNEP’s 2023 Global Status Report stated that buildings represented 37% of global energy and process-related emissions in 2022. A stable drywall assembly supports long service life and fewer repairs. Still, coating selection deserves more attention in humid or coastal locations. I would not trust a catalog alone. Check substrate thickness, exposure, torque, and pull-out performance on site. A trial panel can reveal problems early. That step is often skipped.


Matching Screw Length, Thread, and Point to Wallboard Materials

Choosing drywall screws starts with the wallboard and framing, not a universal length chart. The Gypsum Association’s GA-216 installation standard calls for at least 5/8 inch of screw penetration into wood framing and 3/8 inch into steel framing. Add panel thickness to that requirement, then check the screw manufacturer’s specifications. A 5/8-inch panel over wood needs more length than a 1/2-inch panel. Too-short screws can loosen; overly long ones may strike services behind the wall. That gap matters.

Match the thread to the frame. Coarse threads generally grip wood well, while fine threads suit steel studs. For thicker steel, check the framing gauge and select a compatible drill-point screw; a sharp point may not pass through reliably. ASTM C1002 and C954 distinguish screw applications for gypsum panels and metal framing, so verify the applicable specification rather than relying on appearance. On mixed-material projects, test a sample assembly and inspect the screw head: it should sit just below the paper surface without tearing it. I still treat published guidance as a starting point, not a substitute for checking the actual board, frame, and installation conditions.

How to Choose the Right Drywall Screw for Global Projects - Matching Screw Length, Thread, and Point to Wallboard Materials

Wallboard Material and Application Typical Board Thickness Recommended Screw Length Thread Selection Point Type Key Selection Notes
Standard gypsum board on wood studs 12.5 mm (1/2 in) 32 mm (1-1/4 in) Coarse thread Sharp point Coarse threads provide strong purchase in timber. The screw should penetrate the wood framing sufficiently without protruding excessively.
Standard gypsum board on wood studs 15.9 mm (5/8 in) 41 mm (1-5/8 in) Coarse thread Sharp point A longer screw maintains adequate embedment after passing through the thicker board.
Standard gypsum board on light-gauge steel studs 12.5 mm (1/2 in) 25–32 mm (1–1-1/4 in) Fine thread Sharp point for thin steel; drilling point for thicker steel Fine threads are designed to engage metal framing. Confirm the stud thickness and the screw manufacturer’s capacity before selecting the point style.
Standard gypsum board on light-gauge steel studs 15.9 mm (5/8 in) 41 mm (1-5/8 in) Fine thread Sharp or drilling point, according to steel gauge Use a screw long enough to pass through the board while maintaining reliable engagement in the metal stud without excessive penetration behind the framing.
Two layers of gypsum board on wood framing 25 mm (1 in) total 54–64 mm (2-1/8–2-1/2 in) Coarse thread Sharp point Select the length according to the total board thickness and the required wood embedment. Follow the tested assembly specification where fire or acoustic performance is required.
Moisture-resistant gypsum board in interior wet areas 12.5–15.9 mm (1/2–5/8 in) 32–41 mm (1-1/4–1-5/8 in) Coarse thread for wood; fine thread for steel Sharp or drilling point, according to framing Use corrosion-resistant fasteners suitable for the exposure. Moisture-resistant gypsum board is not automatically suitable for continuously wet or exterior conditions.
Type X gypsum board for fire-rated assemblies 15.9 mm (5/8 in) 41 mm (1-5/8 in) Coarse thread for wood; fine thread for steel Sharp or drilling point, according to framing Fastener type, spacing, penetration, and board layers must match the tested fire-resistance design. Do not substitute based on thickness alone.
Glass-mat or fiber-reinforced gypsum sheathing 12.5–15.9 mm (1/2–5/8 in) 32–41 mm (1-1/4–1-5/8 in) Framing-dependent; corrosion-resistant finish often required Self-drilling point for steel or sharp point for wood Use fasteners specifically approved for the board system and exposure. Exterior sheathing applications may require enhanced corrosion protection.
Fiber-cement board or cement backer board 6–13 mm (1/4–1/2 in) 32–41 mm (1-1/4–1-5/8 in) Board-specific thread, commonly high-low or coarse thread Self-drilling or notched cutting point Do not use ordinary gypsum drywall screws. Select corrosion-resistant cement-board screws with a compatible head and cutting point.
Acoustic or high-density gypsum board 12.5–15.9 mm (1/2–5/8 in) 32–41 mm (1-1/4–1-5/8 in) Coarse thread for wood; fine thread for steel Sharp or drilling point, according to framing Use the fastener and spacing specified by the board system to avoid reducing acoustic performance or damaging the dense core.
Global selection rules: Use coarse-thread screws for wood framing and fine-thread screws for steel framing. Choose screw length based on the total board thickness plus the required framing engagement. Use sharp points for wood and thin metal, and self-drilling points when the steel thickness exceeds the piercing capability of a sharp point. For fire-rated, exterior, corrosive, or wet-area applications, follow the applicable local building code and the tested board-system specification.

Evaluating Substrate, Load Requirements, and Installation Conditions

Choosing a drywall screw for global projects starts with identifying the substrate, not the screw box. Gypsum board fixed to timber needs coarse threads that bite deeply. Steel framing usually requires fine threads and a sharper point. For cement-based surfaces, use a tested anchor system instead of forcing a standard drywall screw. I once selected a screw by length alone. That assumption was wrong.

Load requirements also change the specification. A ceiling panel, partition, or service-access cover may face different pull-out and shear forces. Check board thickness, framing gauge, and expected fixture weight before choosing screw diameter and length. The screw should penetrate the framing securely without damaging hidden services. For heavier fixtures, add blocking or use a rated fastening method. Small tests help. A trial panel can reveal spinning, cracking, or poor thread engagement before installation spreads across a site.

Installation conditions deserve equal attention. Humid rooms, coastal air, and temperature changes can accelerate corrosion, so select a suitable protective finish and verify its environmental rating. Clean, dry surfaces improve seating and reduce slipping. Set the driver clutch carefully; excessive torque can tear the paper face and weaken the joint. On large projects, I record screw type, spacing, tool settings, and site conditions for quality checks. Local construction requirements still need review. Field experience is useful, but it is not a substitute for project-specific testing. I still question fast choices made under schedule pressure.

How to Choose the Right Drywall Screw for Global Projects - Evaluating Substrate, Load Requirements, and Installation Conditions

The chart shows typical screw-length ranges used for common drywall applications. Coarse-thread screws are generally selected for wood framing, while fine-thread screws are commonly used with light-gauge steel framing. Heavier boards, multiple layers, and higher loads require longer screws and verification of the required embedment, corrosion resistance, and local building-code requirements.

Planning reference: screw lengths are typical nominal values in millimetres, not project-specific structural design values. Confirm substrate thickness, minimum embedment, pull-out requirements, corrosion exposure, and installation torque before procurement.

Checking Regional Standards, Coatings, and Environmental Resistance

Choosing a drywall screw for an international project starts with the destination’s standard, not the supplier’s catalogue. Check whether the specification follows ASTM C1002, EN 14566, or another local system. These standards may differ in thread geometry, mechanical performance, dimensions, and testing methods. Do not assume approval in one market guarantees acceptance elsewhere. Ask for current test reports, declarations, and traceable batch information. That paperwork matters on remote projects. It also exposes missing data early.

Coating selection should match the actual exposure. For dry interior rooms, a suitable phosphate or zinc finish may provide adequate protection. Bathrooms, kitchens, coastal buildings, and unheated storage areas need closer review. Persistent humidity can attack exposed edges after installation. In corrosive environments, specify a tested corrosion-resistant coating and confirm compatibility with framing and joint compounds. A bright surface is not proof of durability. Check salt-spray results carefully; laboratory hours do not directly predict service life.

On site, inspect the screw head, recess, and threads before large-scale installation. Poor engagement causes cam-out, damaged boards, and uneven finishing. For a warehouse near the coast, I would request sample panels and humidity or salt-exposure testing. Small trials reveal problems that datasheets miss. Still, this process is not perfect. Local workmanship, storage conditions, and cut edges can change performance. Record the selected standard, coating, lot number, and installation tool settings. That record supports quality checks when conditions change.

Planning Sourcing, Quality Control, and Compatibility for Global Projects

How to Choose the Right Drywall Screw for Global Projects

Planning starts before the purchase order. Different regions may use gypsum boards, metal studs, or timber framing with varied thicknesses. I have seen projects delayed because a screw fitted the board but failed in the framing. Confirm thread design, screw length, head shape, point type, and corrosion protection with local installation teams.

A reliable sourcing plan uses approved samples from more than one qualified supplier. Ask for material declarations, coating details, dimensional reports, and batch traceability. Independent testing should check pull-out strength, torsional resistance, hardness, and corrosion performance. Quality control must continue after approval. Inspect random cartons, verify counts, and record lot numbers before shipment. Small packaging errors can create large site problems.

Tips: Match the screw to the substrate, not only the board. Test samples under real site conditions, including humidity and temperature changes. Keep a written acceptance standard for every destination. Check compatibility with automatic screwdrivers and local tools. Do not assume one specification fits every market. I once underestimated regional installer preferences; the product passed laboratory checks but slowed installation. That mistake deserved more attention. Keep spare samples for future comparisons. Also, review transport packaging, because damaged coating can reduce performance before installation.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
