


Choosing a Copper Stamping Machine is not simply a matter of selecting the largest press. It requires evidence, process experience, and careful cost judgment. Grand View Research valued the global metal stamping market at approximately USD 283 billion in 2023. Its forecast also indicates steady growth through 2030. Meanwhile, the U.S. Geological Survey continues to identify copper as a critical material for electrical equipment, construction, and transportation. These trends increase pressure for accurate, repeatable copper forming.
Richard Crowson, author of Handbook of Metal Stamping, offers a useful principle: “The best press is the one that produces the required part consistently, not merely the one with the highest tonnage.” This advice matters when comparing mechanical, servo, and hydraulic systems. A practical evaluation should examine material thickness, copper alloy, strip width, required stroke rate, die size, feeder accuracy, and allowable burr height. Ask for documented tests using your actual copper grade.
Look closely at the details. Does the machine control springback? Can it maintain alignment after hours of production? Is spare-part support available locally? These questions often matter more than brochure speed. A 160-ton press may outperform a 250-ton model when its servo feed reduces scrap and protects delicate contacts.
No single machine wins every job. That is the difficult part. Energy reports, supplier claims, and factory trials can disagree. Buyers should therefore request sample parts, maintenance records, noise data, and total operating costs. A modest machine with disciplined setup may deliver better results than an impressive machine chosen too quickly.
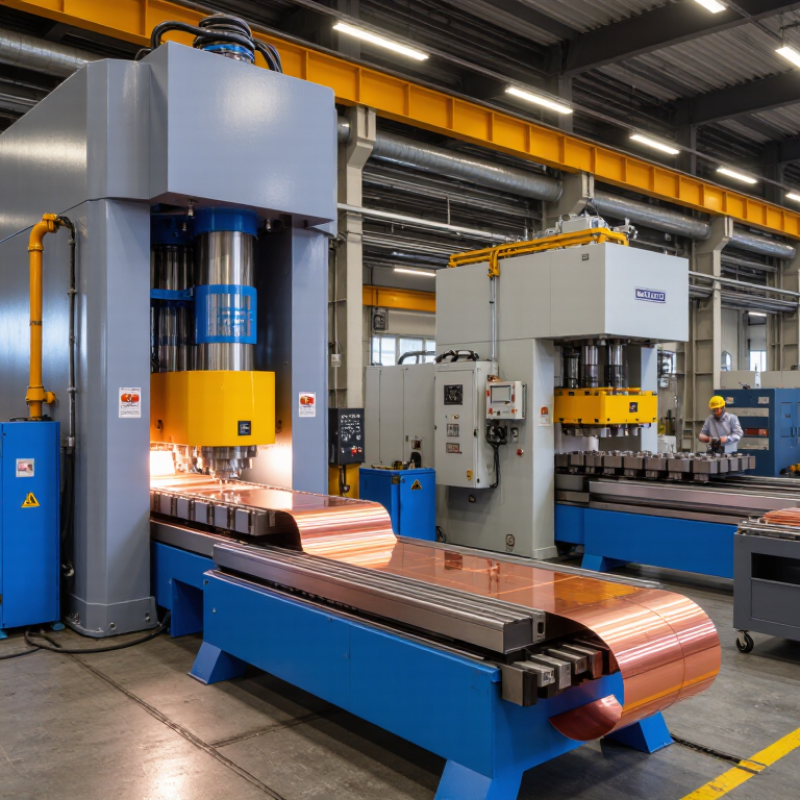
A copper stamping machine converts flat copper strip into precise parts through controlled pressure. Its main functions include feeding, positioning, punching, bending, and forming. A press applies force through a die, while sensors monitor strip movement and tool position. Copper conducts heat and electricity well, but it can scratch, buckle, or work-harden during production. A practical trial should inspect sample parts under magnification. Tiny burrs often reveal problems before production numbers do.
Choosing capacity requires more than reading the rated tonnage. Match the machine to copper thickness, part geometry, stroke length, and required output. A servo or mechanical press may suit different production rhythms. The feeder must hold the strip firmly without marking its surface. Ask for data on repeatability, die compatibility, guarding, noise, and maintenance access. Operators should reach adjustment points safely, with clear controls and documented procedures. Small details matter.
In my experience, the best assessment uses actual copper material, not a generic steel sample. Run several cycles, then measure hole diameter, bend angle, flatness, and burr height. Check the scrap rate after the machine warms up. That is where surprises appear. I would question optimistic speed claims because they may exclude setup time and tool changes. No machine is perfect. A careful buyer leaves room for calibration, training, and process corrections.

Choosing a copper stamping machine starts with the part, not the machine catalog. Start with the part. Record copper grade, thickness, strip width, blank size, and tolerance. Then estimate hourly output, shift patterns, and expected tool life. These figures reveal the real production load. A prototype may need 20 strokes per minute, while high-volume production may require several hundred. Do not trust nominal tonnage alone. Calculate forming force, stripping force, and a safety margin with a qualified tool engineer. Copper conducts heat well, but thin strip can buckle during feeding. That detail is easy to miss.
For flat terminals, washers, and simple brackets, a mechanical press with a compound die may provide accurate, economical cycles. Progressive dies suit long runs with several operations, including piercing, bending, and cut-off. Deep or irregular shapes may require a servo press or hydraulic press. Consider speed, force control, and draw depth. Servo control can reduce material stress, but it may increase programming work and cost. Hydraulic systems offer flexible force profiles, although cycle speed can be lower. Match the machine to the die, feeder, and inspection method as one system.
Before purchasing, run representative copper strip through a production-style die. Test it under load. Check burr height, edge cracks, flatness, feed accuracy, noise, and temperature after a full shift. Ask whether the frame maintains alignment under repeated loads. I have seen machines pass a short trial and struggle after hours of cycling. That experience changed how I judge capacity. A perfect specification sheet is not enough. Confirm spare parts, operator training, lubrication access, and measurement records. If demand is uncertain, leave room for a second feeder or future tooling. Do not guess.
| Production Requirement | Typical Copper Part or Operation | Suitable Machine Type | Typical Capacity Range | Recommended Operating Characteristics | Key Selection Considerations |
|---|---|---|---|---|---|
| Low-volume / prototype | Simple brackets, washers, terminals, experimental parts, and short production runs | Mechanical gap-frame press | Approximately 10–80 metric tons | Moderate stroke rate; manual, hand-fed, or simple batch operation | Choose adjustable stroke and shut height, accessible tooling space, and suitable guarding. A smaller press reduces initial investment and is easier to set up for frequent die changes. |
| High-volume blanking | Flat discs, plates, electrical contacts, and repetitive outline shapes from copper strip or sheet | High-speed mechanical press | Approximately 30–160 metric tons | Typically 200–1,000 strokes per minute, depending on part size, material thickness, and die design | Prioritize rigid construction, low vibration, accurate ram guidance, reliable lubrication, and a compatible automatic strip feeder. |
| Progressive stamping | Small terminals, connectors, clips, lead frames, and multi-step electrical components | Straight-side mechanical press with progressive-die feeding | Approximately 40–250 metric tons | High repeatability, stable feed pitch, and continuous coil processing | Verify die width, feed-line height, slide length, shut height, press speed, and the required number of die stations. Adequate tonnage must be available at the actual forming position, not only at the bottom of the stroke. |
| Precision forming | Deep-drawn cups, formed covers, embossed parts, and components requiring controlled material flow | Servo mechanical press | Approximately 50–300 metric tons | Programmable slide motion, controlled dwell, and adjustable speed through the forming zone | Servo motion can improve forming control and reduce sliding damage, but the die, lubrication, blank-holder system, and copper temper must also be matched to the operation. |
| Heavy forming | Thicker copper busbars, large connectors, substantial bends, and low-to-medium production volumes | Hydraulic press | Approximately 100–1,000+ metric tons | Slower cycle rate with adjustable force, pressure, and dwell time | Hydraulic presses are suitable when force must be maintained over part of the stroke or when complex forming requires controlled motion. Consider energy use, cycle time, oil temperature control, and maintenance requirements. |
| Thin strip stamping | Thin copper contacts, springs, shielding pieces, and miniature electronic components | High-speed precision press | Approximately 10–80 metric tons | High speed with precise feed control; commonly used with narrow coil stock | Focus on press stability, die clearance, feed accuracy, strip straightening, and scrap removal. Excessive speed or incorrect clearance can increase burrs and material distortion. |
| Thick sheet / busbar | Electrical busbars, grounding components, switchgear parts, and large conductive plates | Straight-side mechanical or hydraulic press | Approximately 160–800 metric tons | Lower speed, high frame rigidity, and sufficient daylight for the tooling | Calculate cutting and forming loads separately. Confirm bed dimensions, point-of-load capacity, die support, maximum material thickness, and safe handling of large blanks. |
| Variable product mix | Different copper alloys, thicknesses, part sizes, and frequent tooling changes | Servo press or programmable hydraulic press | Selected according to the highest required forming load | Adjustable speed, stroke profile, and programmable production settings | Useful when one machine must handle several products. Confirm that the control system can store recipes and that the available die space supports all planned tools. |
| Automated production cell | Continuous coil-to-part production with in-die sensing, inspection, and automatic collection | Automated mechanical or servo press line | Approximately 50–400 metric tons for many precision strip applications | Coil feeder, straightener, sensors, die protection, scrap handling, and part collection integrated with the press | Evaluate the complete line rather than the press alone. Synchronization, sensor response, emergency stopping, access protection, and changeover time directly affect overall equipment effectiveness. |
Note: Capacity and speed ranges are typical engineering guidelines, not universal limits. Final selection should be based on copper alloy, temper, thickness, blank size, die design, required production rate, calculated forming load, and applicable safety standards.
Capacity should match the copper strip, part geometry, and die load. Oversizing wastes energy and floor space. Undersizing causes deflection, burrs, and unstable dimensions. Calculate tonnage from material thickness, perimeter, shear strength, and a safety margin. Also check bed size, shut height, stroke length, and allowable die weight. These details matter more than a large headline capacity.
Accuracy Accuracy is not only a machine specification. Frame rigidity, slide guidance, lubrication, and feeder repeatability affect every terminal or connector. For tight copper parts, inspect dimensional drift during a long production run, not only during setup. ISO 230 measurement principles can support repeatable machine testing, although they do not replace practical die trials. A 0.01-millimeter claim may sound impressive. It still needs verification under real load.
Speed should be judged against quality and uptime. A faster stroke rate is useless if copper strips buckle or tools require frequent adjustment. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023, showing how quickly automation is expanding. Consider servo feeders, automatic coil loading, vision inspection, die protection, and production data collection. Automation reduces handling errors, but it can also create expensive mistakes when sensors are poorly configured. Run sample coils, measure scrap, and compare actual cycle stability. My experience suggests that a slightly slower machine often performs better when setup changes are frequent.
Choosing a copper stamping machine starts with the tooling, not the advertised tonnage. Copper is soft, conductive, and prone to galling when clearances or lubrication are poorly controlled. Tool steel selection, die alignment, and punch-to-die clearance should match the copper grade and sheet thickness. The International Copper Study Group reported global refined copper usage above 26 million tonnes in 2024, showing the scale of demand for consistent forming quality. Yet production volume alone should not decide the machine.
Material compatibility needs practical testing. Check feed accuracy, coil tension, surface protection, and heat buildup during continuous runs. Copper’s high conductivity can expose weaknesses in sensors, electrical connections, and control cabinets. ISO 12100 recommends documented risk assessment, while OSHA 1910.212 emphasizes guarding at points of operation. Maintenance should include daily die inspection, weekly lubrication checks, and scheduled verification of force, alignment, and emergency stops. I have seen clean-looking tooling produce burrs after only a few hours. That detail is easy to miss.
Tips: Request trial stamping with your actual copper grade. Measure burr height, springback, dimensional drift, and die temperature. Keep a maintenance log with photos. Replace damaged guards immediately. Do not trust a perfect first sample; copper behavior can change with batch, temper, and tooling wear. A spreadsheet cannot predict every coil variation. Reconsider the setup when scrap rises, even if the machine still runs. Reports from the U.S. Bureau of Labor Statistics continue to identify manufacturing as a high-risk environment, so safe access and isolation procedures deserve equal weight with output.
How to Choose a Copper Stamping Machine? Electrical conductivity is a useful material-compatibility indicator when selecting tooling clearance, forming force, cooling, and inspection requirements. These typical room-temperature values are expressed as a percentage of the International Annealed Copper Standard (% IACS); actual performance varies with temper, thickness, and supplier specifications.
Copper demand is becoming less forgiving. The International Energy Agency’s Global Critical Minerals Outlook 2024 projects copper demand rising from about 26 million tonnes in 2023 to 31 million tonnes by 2035. That growth supports added capacity, but it does not justify buying the largest press.
Compare the full cost: machine price, tooling, feeder installation, electricity, maintenance, scrap, and downtime. Request a written quote. Measure twice. Buy once.
Efficiency must be measured with your actual copper strip, thickness, and part geometry. The U.S. Department of Energy reports that motor-driven systems consume more than half of industrial electricity.
Ask for energy data at your required stroke rate, not only an impressive maximum speed. Check parts per minute, changeover time, misfeeds, and usable production hours.
A practical trial using real material is more reliable than a brochure.
Small losses accumulate quickly.
Long-term value depends on serviceability. Examine frame stiffness, guides, crankshaft access, control-system support, and spare-part lead times. A lower-priced machine may become expensive after repeated stoppages.
However, a premium specification can also remain underused. That is an easy mistake to make.
Use a five-year cost model, including expected scrap and maintenance. The IEA forecast is useful context, not a production schedule.
Sometimes, the cheaper press wins.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

