


Choosing a Cnc Centre Lathe is a practical decision, not merely a comparison of prices and specifications. The right machine should match your materials, component sizes, tolerance requirements, production volume, and operator experience. A lathe cutting stainless steel behaves differently from one producing small aluminium parts. Heat, vibration, chip control, and tool access quickly expose weak choices.
Teruyuki Yamazaki, founder of Yamazaki Mazak, described machine tools as “the mother machines of industry.” This idea remains relevant. A CNC Centre Lathe influences every stage of production, from drawing interpretation to final inspection. Buyers should examine spindle power, maximum turning diameter, bed length, chuck capacity, turret design, control system, and service support. These details matter on the shop floor. A powerful spindle is useful, but only when its speed range suits the intended work. A long bed may appear attractive, yet unused capacity increases cost and floor-space pressure.
This guide explores how to choose a CNC Centre Lathe with evidence-based thinking. It considers real machining conditions, including interrupted cuts, long shafts, difficult alloys, and repeated batch production. It also examines accuracy, maintainability, training needs, energy use, and future expansion. Some decisions remain imperfect. Brochure figures do not always predict daily performance. A machine may look excellent on paper but disappoint without reliable tooling, coolant control, or technical support. Careful trials, reference checks, and sample-part testing often reveal more than a sales presentation.
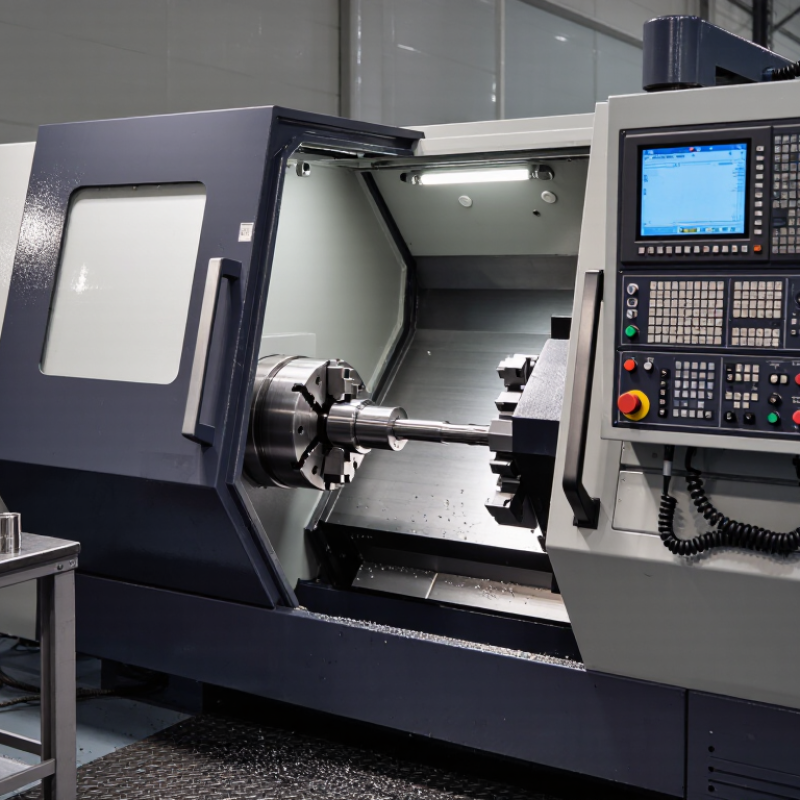
Define the machining requirements before comparing machine specifications. List the materials, maximum diameter, part length, thread types, tolerances, surface finish, and expected batch size. A steel shaft may need greater spindle torque than an aluminium component. Record the heaviest chuck load and the longest unsupported workpiece. These details prevent an attractive but unsuitable purchase.
Production goals should include cycle time, annual volume, changeover frequency, and operator skill. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. This indicates growing pressure for repeatable, connected production. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturers expect smart manufacturing to drive competitiveness within three years. Therefore, check automation interfaces, tool capacity, probing options, and data access. Still, automation is not always the best answer. A small workshop may lose money if setup time exceeds the labour saved.
Tips: Measure real parts, not ideal drawings. Ask for a test cut using your material and tooling. Compare complete cycle time, including loading and inspection. Check spindle power at your working speed, not only its peak rating. Leave capacity for future work, but avoid paying for unused travel. A lower-cost lathe can seem sensible until poor chip control, vibration, or repeated rework consumes the margin. My own assessment would remain provisional without production samples, because catalogue accuracy rarely reveals every shop-floor limitation.

How to Choose a CNC Centre Lathe?
CNC centre lathes vary by structure, axis layout, and production purpose. A standard two-axis model suits turning, facing, threading, and boring. It is often practical for shafts, bushes, and repair work. A slant-bed configuration improves chip flow and usually supports faster automated production. Flat-bed designs can offer wider working space for large or irregular parts.
Turning centres may include live tooling, a Y-axis, or a second spindle. Live tooling allows drilling and milling without moving the workpiece. This can reduce setup errors and handling time. A twin-spindle machine can complete both ends of a component. However, it may require more advanced programming and careful synchronization. Do not select these features only because they appear impressive. Match them to actual drawings, batch sizes, and operator skills.
Tips: Check the maximum turning diameter, swing over the bed, spindle bore, and bar capacity. Measure your longest part with the chuck and tailstock installed. Confirm the control system supports your preferred programming workflow. Ask for a test cut using similar material, tooling, and tolerances. Watch chip evacuation during the trial. It can reveal problems that specifications hide. I would also leave capacity for future work, but not too much. An oversized machine can consume floor space, energy, and training time unnecessarily.
Choosing a CNC centre lathe starts with capacity, not advertised spindle speed. The 2024 Gardner World Machine Tool Survey valued global consumption at about US$81.9 billion, showing intense demand for productive equipment. Yet production value does not guarantee suitability. Measure your largest workpiece, including chuck clearance, tool access, and tailstock reach. Select swing over bed, maximum turning diameter, and distance between centres with practical margin. A long shaft may fit the catalogue but still vibrate during cutting.
Spindle specifications deserve careful comparison. Check spindle bore, bar capacity, chuck size, speed range, and torque at low rpm. High speed helps aluminium and finishing, while stable torque supports steel roughing. A large motor is not automatically better. Power must match tooling, material, and duty cycle. The International Organization for Standardization’s ISO 230-2 positioning tests distinguish accuracy from repeatability. Request test results, thermal compensation details, and backlash measurements under controlled conditions. Small errors become visible on bearing seats.
Performance should be judged with your own material and tools. Ask for a cutting demonstration using a similar diameter, insert, and coolant method. Record cycle time, surface finish, dimensional drift, and chip control. A 0.01 mm repeatability claim may change after several hours of heat buildup. I have seen impressive trial cuts fail during continuous production. That uncomfortable gap matters. Review service records, test methods, and operator feedback before accepting laboratory figures.
| Evaluation Category | Key Specification | Practical Selection Range | What to Check Before Purchase |
|---|---|---|---|
| Workpiece Capacity | Maximum swing over bed | 450–800 mm for general production work | Choose a machine with at least 20–30% more swing than the largest planned workpiece to allow for fixtures, tool clearance, and safe chip evacuation. |
| Workpiece Capacity | Maximum turning diameter over cross slide | 250–500 mm for medium-duty applications | This value is often more useful than swing over the bed because it reflects the diameter available during actual tool movement. |
| Workpiece Capacity | Distance between centres | 500–1,500 mm | Select a centre distance longer than the maximum part length, including chucking allowance and support from a tailstock or steady rest. |
| Spindle System | Spindle bore | 52–105 mm for common bar and shaft work | The bore should accommodate the largest bar stock or workholding draw tube required by the production range. A larger bore can improve flexibility but may increase spindle mass and cost. |
| Spindle System | Spindle speed range | 30–4,000 rpm for general-purpose turning | Low-speed torque is important for large diameters and heavy cuts, while higher speed supports small-diameter parts and finishing operations. |
| Spindle System | Spindle motor power | 7.5–22 kW for medium-duty production | Compare continuous and short-time power ratings, not only the peak value. Confirm that available torque matches the materials, cutting depths, and insert grades used in production. |
| Axis Performance | X-axis travel | 180–350 mm | Verify that the travel covers the required turning diameter while leaving sufficient clearance for the turret, toolholders, chuck, and part geometry. |
| Axis Performance | Z-axis travel | 400–1,200 mm | Allow extra travel for facing, grooving, threading run-outs, workholding, and future part-size changes. |
| Axis Performance | Rapid traverse rate | 15–30 m/min | Higher rapid speed can reduce non-cutting time, but evaluate acceleration, positioning stability, and actual cycle-time data rather than speed alone. |
| Accuracy | Positioning accuracy | Approximately ±0.005 to ±0.010 mm per axis | Request a documented measurement method and test length. Accuracy should be evaluated together with thermal stability, calibration practices, and machine foundation quality. |
| Accuracy | Positioning repeatability | Approximately ±0.002 to ±0.005 mm per axis | Repeatability is critical for consistent batch production. Ask for test results under operating conditions and check performance after warm-up. |
| Machine Structure | Bed construction and guideways | Rigid slant bed with hardened linear or box guideways | A rigid bed helps control vibration and taper during heavy cuts. Inspect guideway protection, lubrication access, and resistance to chips and coolant. |
| Workholding | Chuck size and type | 200–315 mm hydraulic three-jaw chuck for general work | Confirm chuck bore, gripping range, clamping force, jaw change time, and compatibility with the spindle nose and planned part shapes. |
| Tooling | Turret capacity | 8–12 stations for standard turning; 12–16 for complex work | Consider the number of operations, duplicate tools for unattended production, driven-tool requirements, indexing time, and toolholder availability. |
| Tooling | Live tooling capability | Optional for turning-only work; recommended for drilling, milling, and off-centre features | Check live-tool power, maximum speed, C-axis resolution, coolant delivery, and whether the machine can complete secondary operations without an additional setup. |
| Control and Programming | CNC control functions | Conversational programming, standard G-code, tool compensation, and rigid tapping | Confirm memory capacity, USB or network transfer, simulation, tool-life management, probing support, alarm diagnostics, and compatibility with existing programs. |
| Production Efficiency | Chip and coolant management | Enclosed work area with chip conveyor and filtered coolant system | Evaluate conveyor type, chip handling for long-string materials, coolant tank capacity, filtration, washdown coverage, and access for cleaning and maintenance. |
| Safety and Compliance | Guarding and interlocks | Fully enclosed guarding with monitored door interlocks | Check emergency stops, interlock performance, chuck clamping confirmation, spindle-speed monitoring, visibility, lighting, and compliance with applicable local regulations. |
| Installation | Footprint and power requirement | Typically 2.5–5.5 m machine length; three-phase industrial power | Confirm floor loading, foundation requirements, electrical capacity, compressed air, coolant ventilation, access routes, and space for loading and maintenance. |
| Lifecycle Value | Serviceability and operating cost | Accessible lubrication, standard consumables, and documented preventive maintenance | Assess spare-parts availability, technical support response, warranty terms, energy consumption, training, maintenance intervals, and the total cost over the expected service life. |
Specification ranges are general purchasing guidelines for medium-duty CNC centre lathes. Final selection should be based on actual part drawings, material, batch size, tooling strategy, tolerance requirements, and a verified machine acceptance test.
A CNC centre lathe should be judged beyond spindle speed and cutting capacity. The control system affects setup time, alarm recovery, and daily confidence. On the shop floor, I look for clear menus, readable tool offsets, and simple program verification. A powerful control is not always an easy control. Operators should simulate toolpaths, edit offsets safely, and retrieve proven programs without searching through confusing screens.
Automation deserves equal attention. Consider bar feeding, tool monitoring, chip removal, probing, and workpiece handling. These features reduce interruptions, but only when they match your production pattern. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. That figure signals growing automation, but it does not prove every lathe needs a robot. For short batches, quick-change workholding may create more value than a complex cell. I have seen sophisticated systems lose time because operators avoided them.
Tips: Ask operators to complete a sample setup before purchasing. Measure clicks, walking distance, alarm recovery, and training time. Check whether the interface supports multiple skill levels. Request a realistic demonstration using your material, tooling, and part geometry. Independent validation matters. The 2024 Deloitte Smart Manufacturing survey found that manufacturers continue prioritizing digital operations, yet workforce capability remains a major implementation challenge. A useful control should teach through clarity, not punish through cryptic alarms. Leave room for doubt. A specification sheet cannot reveal every awkward moment at 6 a.m.
How to Choose a CNC Centre Lathe?
Choosing a CNC centre lathe is not merely a matter of comparing spindle speed and swing. Supplier support often determines whether production stays stable after installation. Ask how quickly technicians respond to alarms, software issues, and alignment concerns. A dependable supplier should provide operator training, setup guidance, and clear maintenance schedules. Request references from workshops with similar materials and production volumes. In my evaluations, a supplier’s response time revealed more than polished sales presentations. That detail matters.
Calculate the total cost before approving the purchase. Include tooling, installation, transport, training, electricity, coolant, lubrication, and planned downtime. Ask about spare-part availability and delivery times. A low initial quote can become expensive after repeated delays. Check warranty limits carefully. Some essential components may receive short coverage. I have seen buyers overlook this point. Their budgets changed quickly.
Safety needs practical inspection, not only paperwork. Check guarding, door interlocks, emergency stops, chip control, and visibility around the cutting area. Confirm that controls are understandable for every shift operator. Ask the supplier to explain risk controls during a live demonstration. Long-term value also depends on serviceable design, software updates, and future automation options. Review maintenance records from comparable machines. One uncomfortable question helps: can the supplier support this lathe five years from now? The answer may be less certain than expected.
This planning model assigns 100 points across the main purchase criteria. Total cost receives the highest weighting because purchase price, installation, tooling, maintenance, energy, downtime, and operator training all affect the real cost of ownership. Supplier support and safety are weighted heavily because preventive maintenance, spare-parts availability, guarding, emergency stops, and documented risk controls directly influence uptime and workplace risk.
The percentages are a transparent evaluation framework rather than market-share data. Adjust the weighting to match your production volume, regulatory requirements, workforce skills, and service conditions.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

