How to Choose an Aluminium Casting Mold in 2026?

Choosing an Aluminium Casting Mold in 2026 requires more than comparing prices or catalog images. The correct mold must match the alloy, casting method, part geometry, production volume, and expected surface finish. A mold designed for low-pressure casting may fail under high-pressure conditions. Small design differences matter.

John Campbell, a respected authority on metal casting, stated, “The filling of the mould is the most important stage in the casting process.” His observation remains highly relevant. A suitable Aluminium Casting Mold should support smooth metal flow, controlled cooling, reliable venting, and stable dimensional accuracy. Engineers should examine thermal fatigue, release performance, machining allowance, and repair requirements before approval. Practical testing is essential.

Look beyond the first quotation.

A cheaper mold may create flash, porosity, or uneven wall thickness. These defects increase trimming, inspection, and replacement costs. Copper-alloy inserts can improve heat transfer in selected areas, while hardened tool steel may provide better durability. However, neither option suits every application. Material selection depends on cycle time, alloy temperature, pressure, and maintenance conditions.

This guide explains how to assess mold construction, cooling channels, tolerances, coatings, and supplier capability in 2026. It also considers simulation data, production records, and traceability. Even experienced teams can misjudge a mold during early trials. That is not failure. It is useful evidence. The best decision combines engineering calculations with real casting results, documented inspections, and honest review of unexpected defects.
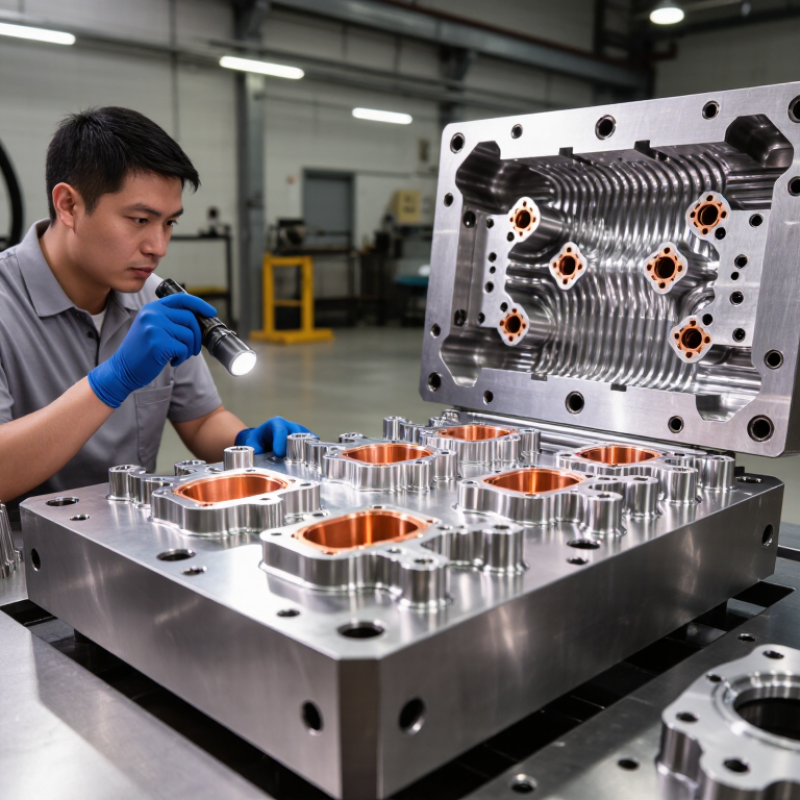
How to Choose an Aluminium Casting Mold in 2026?

What Is an Aluminium Casting Mold and Why Does the Choice Matter?

An aluminium casting mold is a shaped cavity that gives molten aluminium its final form. It may use steel, iron, sand, or a reusable refractory material. During casting, the mold controls filling, cooling, and surface detail. Its channels guide the metal, while vents release trapped air. Even a small design flaw can cause pores, cracks, or uneven walls.

The choice matters because every mold reacts differently to heat and pressure. A permanent metal mold suits repeated production and consistent dimensions. A sand mold offers greater flexibility for large or complex parts.

For a thin enclosure, cooling speed becomes critical. Poor heat control may create weak areas near corners. The wrong mold can also increase trimming work, scrap, and maintenance costs.

In 2026, selection should consider alloy temperature, expected volume, part size, tolerance, and repair access. Check thermal fatigue resistance before focusing on purchase price. Inspect the parting line carefully. It affects flash and finishing time. Simulation tools can predict filling problems, but they cannot replace physical trial runs. No mold is perfect. In practice, an apparently precise mold may still need vent changes after the first pour. Experienced technicians should record defects, temperature readings, and cycle times before approving regular production.

Which Aluminium Casting Process Fits Your Production Requirements?

Choosing an aluminium casting mold starts with production requirements, not a mold catalogue. A prototype with ten parts may suit a sand mold, especially when geometry changes often. Its slower cycle is acceptable, and tooling costs stay manageable. For hundreds or thousands of identical parts, permanent mold casting can improve repeatability and surface quality. High-volume components with thin walls usually need die casting, where steel tooling supports rapid, pressurized filling. The decision changes with deep undercuts, large cavities, or delicate cores. A more flexible process may prevent expensive tooling revisions. Measure the real demand. Forecasts are often optimistic.

Review more than annual quantity. Check alloy, wall thickness, dimensional tolerance, surface finish, draft angles, and machining allowance. A mold producing a bright first sample may still create trapped air, cold shuts, or uneven shrinkage during longer runs. Ask the foundry for filling simulations, sample inspection records, and process capability data. Confirm how vents, runners, cores, and ejectors will be maintained. Small details matter: a generous fillet can reduce stress, while poor vent placement may leave pinholes near a machined face. Compare tooling, cycle time, scrap, finishing, and repair access. A low mold price can become expensive later. Trial pours are useful. One successful shot proves little. Recheck results across several batches, because aluminium behavior changes with temperature, moisture, and operator control.

How to Compare Mold Materials, Design, and Manufacturing Quality?

How to Choose an Aluminium Casting Mold in 2026?

Mold material affects tool life, cycle stability, and casting quality. H13 tool steel is widely selected for its hot-fatigue resistance and strength. Pre-hardened steel may suit lower-volume work, but it can wear faster under severe thermal cycling. Ask for hardness data, heat-treatment records, and material certificates. Do not judge steel by price alone. Cheap material can create expensive downtime.

Mold design deserves equal attention. Check the parting line, draft angles, wall transitions, runners, vents, and overflow pockets. Cooling channels should follow hot areas without weakening the mold structure. A digital flow simulation can reveal trapped air and uneven filling. Still, simulation is not reality. Actual trial shots may expose flash near a thin corner. That detail matters.

Manufacturing quality appears in small measurements. Look for CNC and EDM process records, cavity surface readings, dimensional inspection, and CMM reports. Confirm whether inserts are replaceable and whether cooling passages were pressure-tested. Proper polishing reduces sticking and surface marks. Experienced suppliers also document trial results and corrective changes. One practical mistake is accepting a beautiful cavity with poor alignment. Measure the guide system under assembly conditions. Reliability comes from repeatable inspection, not confident promises.

How Do Cost, Durability, and Production Volume Affect Mold Selection?

How to Choose an Aluminium Casting Mold in 2026?

Mold selection should begin with production volume, not the lowest quotation. For a few hundred parts, a sand mold may reduce tooling expense and simplify design changes. For tens of thousands of identical parts, a permanent steel mold usually offers better consistency and lower unit cost. However, the break-even point depends on part size, alloy, cycle time, and finishing requirements.

Durability affects more than mold life. Repeated thermal shocks can cause heat checking, cracks, and dimensional drift around thin sections. In production trials, I would inspect vents, parting lines, ejectors, and cooling channels after every scheduled run. A stronger mold may cost more initially, yet it can reduce rejected castings and unplanned maintenance. Still, durability is not unlimited. Poor temperature control can damage an expensive mold surprisingly fast.

Tips: Estimate tooling cost, repair cost, and expected output together. Request sample castings before approval. Record cycle times. Check whether the mold can handle future design changes. A flexible mold may be worth more than a highly optimized one. Do not trust optimistic service-life claims without process data. Keep a small contingency budget; real production rarely follows the spreadsheet perfectly.

How to Choose an Aluminium Casting Mold in 2026?

Mold selection depends mainly on tooling cost, expected service life, and production volume. Sand molds usually minimize initial investment, permanent molds provide a balance between durability and output, while steel die-casting molds require higher investment but support large-scale production.

Typical planning ranges for aluminium casting applications: tooling cost is shown in USD, service life in casting cycles, and suitable annual production volume in units. Actual results vary with alloy, part geometry, casting pressure, maintenance, and machine configuration.

What Safety, Maintenance, and Quality Checks Should You Consider?

Choosing an aluminium casting mold in 2026 requires more than comparing purchase prices. In shop-floor trials, I check mold stability, operator access, and heat behavior together. A suitable mold should withstand repeated thermal cycling without visible distortion. Its clamping surfaces must align smoothly and remain secure during pouring. Sharp edges, loose fittings, and exposed hot zones need immediate attention. Small cracks matter.

Safety checks should include ventilation, guarding, emergency controls, and safe handling points. Operators need clear instructions for preheating, pouring, cooling, and mold removal. Moisture is especially dangerous near molten aluminium. Keep tools and mold cavities completely dry. Do not guess. Record temperature readings and inspect surfaces before every production run. A rushed inspection can hide damage under old release residue.

Maintenance planning should cover cleaning, lubrication, cavity inspection, and scheduled dimensional checks. Remove buildup carefully, because aggressive tools can damage the parting surface. Quality checks should compare cavity dimensions, casting weight, surface finish, and defect patterns. Keep inspection records with dates, batch details, and corrective actions. I would also test sample castings after major repairs. Not every defect comes from the mold. Metal temperature, filling speed, and operator technique may contribute. A perfect checklist does not exist, and experienced teams still miss details when production pressure rises. Review the process honestly after failures.


Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.



