How to Choose an Air Actuator Valve?
Choosing the right Air Actuator Valve is not a simple catalog exercise. It affects flow control, equipment protection, maintenance time, and plant safety. A valve that looks suitable on paper may respond slowly in real service. It may also fail under heat, moisture, dust, or frequent cycling.
Greg McMillan, a recognized process-control specialist, has said, “The control valve is the final control element in a control loop.” His observation remains practical when selecting an Air Actuator Valve. The actuator must deliver enough torque or thrust for the valve body, pressure, and operating temperature. The control signal must also match the site system, whether it uses pneumatic, electric, or digital control equipment.
Small details matter. Consider a valve installed near a vibrating pump. Check air quality, supply pressure, response speed, fail position, and available space. A quarter-turn valve may need a compact rotary actuator, while a larger linear valve may require stronger mechanical support. Stainless steel can resist corrosion, but it is not automatically the best choice.
The cheapest option can look convincing. It may still be wrong. Experienced engineers compare real operating conditions with manufacturer data, not only nominal size. They also review leakage limits, cycle frequency, seal materials, and service history. This guide examines those decisions clearly. It also recognizes an uncomfortable truth: even careful selection can miss changing process conditions. That is why commissioning checks, documented assumptions, and periodic inspection remain essential.
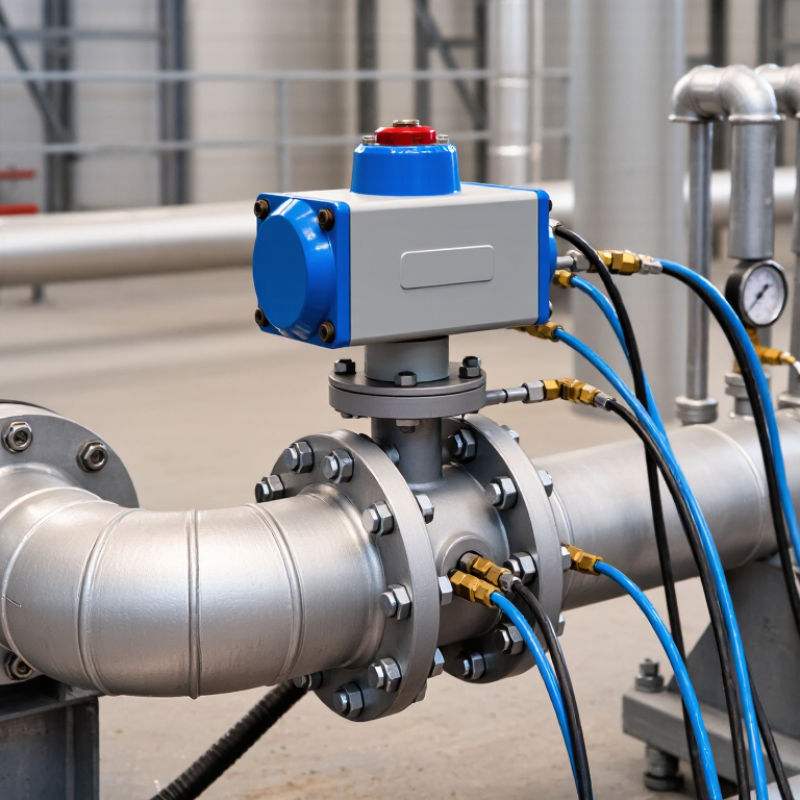
Define the Operating Requirements for the Air Actuator Valve
Choosing an air actuator valve begins with clearly defining its operating requirements. Identify the fluid, flow rate, pressure, and temperature range. Note whether the medium contains moisture, particles, or corrosive chemicals. These details directly affect valve materials and actuator protection.
Define how the valve will operate in practice. Is it opening occasionally, cycling hundreds of times daily, or regulating flow continuously? Specify the required opening time and control accuracy. Decide what should happen if air pressure fails. The valve may need to close, open, or remain in its last position. Do not assume the safest position is obvious. Process conditions and emergency procedures must guide that decision.
Actuator sizing requires more than matching the pipe diameter. Measure the valve’s operating torque, then allow for friction, pressure changes, and starting resistance. A small safety margin is useful, but excessive oversizing can reduce control quality. Check the available air pressure and confirm that the compressor can support peak demand. Air quality matters too. Water or oil contamination can shorten service life. Environmental conditions also deserve attention, including outdoor exposure, vibration, dust, and temperature changes.
In commissioning work, overlooked air pressure is a common problem. A valve may perform well during testing, then respond slowly during simultaneous operation. Specify the control signal, connection type, maintenance access, and expected service life. Requirements often change after installation. Leave room to question the original assumptions.
Match Materials, Pressure Ratings, and Air Conditions
How to Choose an Air Actuator Valve?
When choosing an air actuator valve, start with the air supply, not the catalog photograph. Confirm operating pressure, peak pressure, and cycle frequency at the valve location. A workshop may claim 6 bar, while a long, narrow tube delivers less during fast movement. Measure it. Material choice follows air quality. Dry, filtered air suits many aluminum and stainless-steel bodies, but moisture, oil, and cleaning chemicals can change the decision.
Check the pressure rating under real temperature conditions. Heat can reduce seal performance and lower the safe working range. Leave a practical margin above normal pressure, but do not oversize the valve without reason. Excessive capacity may increase cost and slow response. Match the actuator torque or thrust with the process load, including friction, startup resistance, and occasional pressure spikes. Static calculations often miss these details.
Seal material also matters. Nitrile may suit general service, while EPDM handles some water-based conditions better. Fluorocarbon compounds can tolerate higher temperatures, but compatibility must be verified. Review condensate, ambient temperature, dust, and cleaning fluids together. I have seen valves selected correctly on paper but fail after humid air entered an unprotected line. That mistake is avoidable, though not always obvious. Keep the air filter accessible, inspect drains regularly, and record pressure readings during actual operation. Small field checks reveal more than assumptions.
Evaluate Control, Safety, and Installation Requirements
How to Choose an Air Actuator Valve?
Choosing an air actuator valve depends on control, safety, and installation requirements. Start with the process conditions, not valve size alone. Define the medium, pressure, temperature, flow direction, and switching frequency. Then match actuator torque with the valve’s breakaway and running torque. Add a practical safety margin. Excessive torque, however, can increase cost and reduce response speed. For modulating service, confirm positioning accuracy, air consumption, and signal compatibility. A clear feedback device can help operators detect incomplete movement before it affects production.
Safety deserves careful attention. Specify whether the valve must fail open, fail closed, or hold position during air loss. Consider pressure relief, emergency isolation, and access for maintenance. In field inspections, poor tubing support often causes vibration and slow actuation. Use clean, dry instrument air and protect connections from moisture. Check the actuator’s temperature range, enclosure rating, and manual override design. Do not assume the factory setting fits every system. Site conditions can expose gaps in an otherwise sound selection.
Tips: Confirm available air pressure at the actuator, not only at the compressor. Measure the real installation space before ordering. Leave room for tool access and future servicing. Label air lines clearly. Test the full fail-safe sequence during commissioning. I would also document one unresolved issue: whether the chosen safety position truly protects downstream equipment. Recheck it with the process engineer.
Verify Performance, Maintenance Needs, and Supplier Support
Choosing an air actuator valve requires more than matching pipe size and pressure ratings. In field commissioning, I check response time, leakage, cycling stability, and fail position under actual load. A valve that performs well on a clean test bench may hesitate when moisture, oil, or pressure fluctuation appears.
Maintenance evidence matters. The U.S. Department of Energy’s Improving Compressed Air System Performance report states that leaks can waste 20–30% of a compressed-air system’s capacity. That loss may begin at fittings, tubing, or worn actuator seals. Ask for leakage-test procedures, seal materials, lubrication requirements, and expected service intervals. ISO 8573-1 air-quality classes can also help define filtration needs before installation. Do not accept “maintenance-free” without written conditions.
Supplier support is equally practical. Request traceable test certificates, spare-part availability, installation drawings, and response targets for technical questions. The supplier should explain how the valve behaves during low pressure, emergency shutdown, and repeated cycling. A useful acceptance test records opening time, closing time, supply pressure, and cycle count. Keep the records.
One detail is easy to miss: published cycle life may use ideal air and laboratory temperatures. Real plants are less forgiving. I would therefore test a sample in representative conditions before approving a large order. The U.S. DOE report also emphasizes measurement and leak detection, yet many selection processes still rely on assumptions. That is a weakness worth correcting.





