


How to Choose the Best RO Water Machine Plant?

Choosing the best RO Water Machine Plant requires more than comparing prices or stainless-steel appearance. The right system must match water quality, production demand, operating conditions, and local service capabilities. A plant designed for bottled water may not suit a factory, hotel, clinic, or commercial kitchen. That difference matters.

Begin with the source-water report. Test hardness, total dissolved solids, iron, silica, microbial indicators, and seasonal changes. These details determine the pretreatment design. Sand filters, carbon filters, softeners, and cartridge filters protect the reverse osmosis membranes from fouling. Poor pretreatment creates expensive problems.

Capacity must be measured realistically. A supplier may advertise a daily output under ideal laboratory conditions. Actual production can fall when water temperature drops or membranes become dirty. Ask for permeate flow, recovery rate, feed pressure, power use, and expected membrane life. Request verifiable test records.

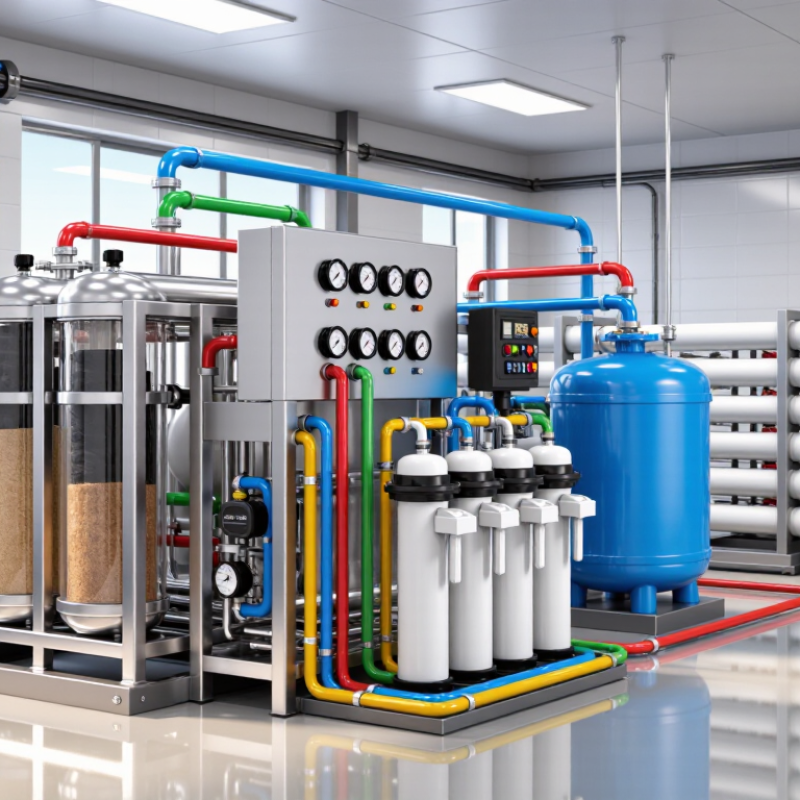
Look closely at the equipment layout. Clear pipe labels, pressure gauges, automatic controls, and accessible filter housings make daily operation safer. A reliable supplier should provide installation guidance, operator training, spare parts, and maintenance schedules. Certification and documented quality controls also deserve careful review.

A low purchase price can look attractive. It may hide weak pumps or limited support. I have seen buyers focus on output while overlooking wastewater discharge and replacement costs. That mistake is understandable, but avoidable. No checklist is perfect. Still, comparing lifecycle cost, water quality results, warranty terms, and service response can lead to a more dependable decision. The best plant is not always the largest. It is the one that consistently delivers safe, suitable water with manageable operating demands.
How to Choose the Best RO Water Machine Plant?

Understanding RO Water Machine Plant Types and Purification Principles

How to Choose the Best RO Water Machine Plant?

An RO water machine plant uses pressure to push water through a semi-permeable membrane. Dissolved salts, metals, and many microorganisms remain on the reject side. The purified stream passes through. However, membrane performance depends heavily on feed-water quality and operating pressure.

Common plant types include compact skid-mounted units, containerized systems, commercial plants, and industrial installations. Skid-mounted units suit restaurants, offices, and small factories with limited space. Containerized plants are practical for remote sites or temporary production.

Industrial systems handle higher flow rates, but they require stronger pretreatment and more careful monitoring. Seawater RO needs much higher pressure than brackish-water RO.

Pretreatment usually removes sand, rust, and suspended particles through multimedia or cartridge filters. Activated carbon can reduce chlorine, which may damage certain membranes. Water softening or scale control helps protect the membrane surface. After RO, ultraviolet treatment, mineral adjustment, or a storage tank may be added, depending on the application.

Measure TDS, pressure, flow, recovery rate, and conductivity regularly. A clear sample should not be mistaken for safe water. Laboratory testing remains important.

I have seen systems selected by capacity alone, then weakened by poor pretreatment. Bigger is not always better. A slightly lower recovery rate may reduce scaling and maintenance. That trade-off deserves honest review.


Assessing Water Quality, Production Capacity, and Treatment Requirements

How to Choose the Best RO Water Machine Plant?

Choosing the best RO water machine plant starts with the water entering it, not the equipment catalog. Test source water during different seasons. A clear sample can still contain dissolved salts, iron, hardness, silica, microbes, or pesticide residues. Use an accredited laboratory when possible. Record conductivity, pH, turbidity, hardness, temperature, and microbiological results. Do not guess. One test is rarely enough. Well water may change after heavy rain, while municipal water may carry disinfectant residuals.

Production capacity must match actual demand, not an optimistic sales forecast. Calculate daily use, peak-hour demand, operating hours, and planned expansion. A plant rated at 10,000 liters per day may produce less when feed temperature drops or membranes foul. Leave practical reserve capacity. Also check recovery rate and reject-water volume. This detail is often ignored. Storage tanks, pumps, pretreatment, and filling schedules should support the same flow. Otherwise, the RO unit becomes a bottleneck.

Treatment requirements depend on contaminants and final water use. Sediment filtration can protect membranes from visible particles, while carbon treatment may reduce chlorine and organic compounds. Softening or antiscalant dosing can control hardness, but neither solves every scaling problem. UV or other disinfection steps may be needed after purification. Confirm materials, monitoring points, cleaning procedures, and maintenance access before purchase. I have seen technically strong systems underperform because operators lacked training. That weakness deserves honest attention. A site trial may reveal problems that a specification sheet misses.

Comparing Key Equipment, Membrane Systems, and Automation Features

Choosing the best RO water machine plant starts with the feed water, not the equipment list. Test hardness, iron, silica, turbidity, microbial risk, and seasonal changes before sizing anything. A practical layout may include a raw-water tank, multimedia filter, activated carbon filter, cartridge filter, high-pressure pump, membrane housing, and product-water tank. Each component protects the next one. A five-micron cartridge cannot repair poor pretreatment. It only exposes the weakness.

Membrane selection depends on dissolved solids, recovery targets, temperature, and required flow. Check permeate quality, operating pressure, salt rejection, and cleaning access. For example, a plant producing 10 cubic meters per hour may need several membrane elements, rather than one oversized vessel. Calculate recovery carefully. Higher recovery saves water, but it can increase scaling risk. Use conductivity meters before and after the membrane. Keep records across shifts. Data reveals drift earlier than taste or appearance.

Automation should make decisions visible, not hide them. Useful controls include pressure transmitters, flow meters, conductivity alarms, tank-level sensors, and automatic shutdowns. A control panel can flag low feed pressure or rising differential pressure before damage occurs. Remote access is convenient, but local manual controls still matter during network failure. I have seen operators trust a clean screen too quickly. Sensors also need calibration. No design is perfect. Leave space for maintenance, chemical cleaning, and future capacity. The cheapest quotation often omits these working details.

How to Choose the Best RO Water Machine Plant?

Comparing typical membrane recovery and operating-pressure ranges by feedwater type

Brackish-water RO systems generally provide higher recovery at lower pressure, while seawater RO requires higher pressure and typically delivers lower recovery. Industrial wastewater systems can achieve broad performance ranges, but they depend heavily on pretreatment quality, fouling control, membrane configuration, and automation for stable operation. Actual values should be confirmed through feedwater analysis and pilot testing.

Checking Energy Use, Maintenance Needs, Safety, and Certification

How to Choose the Best RO Water Machine Plant?

Energy use deserves more than a brochure estimate. Ask for measured electricity consumption in kWh per cubic meter, not only motor power. A plant with high recovery may save water but require stronger pressure and more energy. Check the reject-water ratio during a real production test. Your source-water temperature, salinity, and daily demand will change the result. Small details matter.

Maintenance should be practical for your team. Inspect how quickly operators can replace prefilters, clean membranes, and record pressure readings. Look for accessible gauges, clear pipe labels, and spare parts with defined service intervals. A digital control panel is useful, but it cannot replace trained inspection. I have seen systems with advanced screens and neglected filters. That mistake reduced membrane life and increased operating costs.

Safety checks should cover electrical grounding, pressure relief, leak protection, and secure chemical storage. Ask whether the frame, tanks, and valves suit the local operating conditions. Certification needs careful verification. Request current certificates, laboratory reports, and the exact models covered by each document. Standards such as NSF/ANSI 58 may address RO performance, while electrical or structural requirements can differ by country. Check the issuing body independently. Certification is not a guarantee of good installation. Have a qualified technician review commissioning records, water tests, and sanitation procedures before regular operation.

Evaluating Suppliers, Installation Services, Costs, and Long-Term Value

Choosing the best RO water machine plant requires more than comparing equipment prices. Supplier evaluation should begin with proven operating experience, water analysis, and transparent performance data. Ask for reference installations with similar feedwater, capacity, and seasonal conditions. The 2023 WHO/UNICEF Joint Monitoring Programme reported that 2.2 billion people lacked safely managed drinking water in 2022. That pressure makes reliability important, not optional. A supplier should provide membrane specifications, pretreatment requirements, recovery rates, electrical loads, and verified test results. Vague promises are expensive later.

Installation quality directly affects long-term value. Check whether technicians can complete commissioning, operator training, pipe flushing, and onsite water testing. The International Desalination Association reports that modern seawater RO systems may use about 2.5–4.0 kWh per cubic metre, excluding intake and distribution. Small design choices matter. A poorly sized pump can quietly increase monthly energy bills. Maintenance access also matters; a crowded skid may save floor space but waste labor every week. I have seen projects focus on purchase cost and underestimate chemical storage, replacement membranes, and reject-water handling. That mistake deserves honest review.

Compare total cost over five to ten years, including electricity, consumables, labor, downtime, and disposal. Request a lifecycle-cost model with assumptions you can challenge. The World Bank’s water-sector guidance supports lifecycle costing because the lowest initial bid may not deliver the lowest total cost. Warranty terms should define response times and performance limits. Independent inspection is worth the fee. No system is maintenance-free.

How to Choose the Best RO Water Machine Plant? - Evaluating Suppliers, Installation Services, Costs, and Long-Term Value
Supplier Profile Typical Project Capacity Indicative Equipment Cost1 Typical Installed Cost1 Installation and Commissioning Typical Lead Time Warranty and Service Profile Typical Recovery Target2 RO Energy Use3 Estimated Annual Operating Cost4 Long-Term Value Assessment
Local Water-Treatment Integrator 5–100 m³/day US$8,000–60,000 US$15,000–110,000 Usually includes site survey, piping tie-in, electrical connection, start-up, and operator training. 3–8 weeks after approved design Commonly 12–24 months; local technicians may provide faster on-site response. 60–75% for brackish-water systems Approximately 0.5–1.2 kWh/m³ for brackish water Approximately 8–18% of installed cost per year, excluding major civil works Strong value for small and medium plants when local service quality is verified; compare the supplier’s spare-parts availability and reference installations.
Specialized RO System Manufacturer 20–1,000 m³/day US$25,000–650,000 US$50,000–1,100,000 May include factory testing, remote support, supervised installation, commissioning, and process optimization. 8–20 weeks after engineering approval Commonly 12–24 months; long-term value depends on membrane, pump, instrument, and control-system support. 65–80% for properly pretreated brackish water Approximately 0.45–1.0 kWh/m³ for brackish water Approximately 6–14% of installed cost per year, depending on labor, chemicals, and membrane replacement Often the best balance of engineering quality, efficiency, and price for repeatable commercial or industrial applications.
Industrial EPC Contractor 100–5,000+ m³/day US$150,000–3,000,000 US$300,000–5,000,000+ Typically covers civil works, buildings, tanks, electrical systems, automation, process integration, testing, and operator training. 6–12 months, depending on permitting and construction Often 24–36 months with formal performance guarantees and planned maintenance options. 70–85% for engineered brackish-water systems; seawater designs are usually lower. Approximately 0.4–0.9 kWh/m³ for optimized brackish-water systems Approximately 5–12% of installed cost per year at larger scale Best suited to large, complex, or regulated projects where single-point responsibility and performance guarantees justify the higher initial cost.
Low-Cost Export Supplier 5–500 m³/day US$5,000–250,000 US$15,000–450,000, excluding some site work and import charges May be limited to documentation and remote guidance; local contractors may need to complete installation and commissioning. 10–24 weeks, including production and shipping Commonly 6–12 months; verify exclusions, response times, replacement-part sources, and technical documentation. 55–70% unless the pretreatment system is carefully engineered Approximately 0.6–1.4 kWh/m³ for brackish water Approximately 10–25% of installed cost per year when local labor, shipping, and unplanned repairs are included Can provide a low purchase price, but the lowest bid may have a higher ten-year cost if commissioning, controls, documentation, and spare parts are weak.
Recommended evaluation rule: Compare suppliers using the same feed-water analysis, permeate-quality target, daily production requirement, recovery target, included scope, warranty terms, spare-parts list, operator-training plan, and ten-year total cost of ownership. Brackish-water benchmarks above do not apply directly to seawater systems, which generally require higher-pressure equipment, energy recovery, and approximately 3–6 kWh/m³ of RO energy.
1 Costs are indicative 2025–2026 US-dollar ranges for packaged or engineered systems and vary with capacity, feed-water quality, automation, civil works, freight, taxes, and local labor. 2 Recovery is the percentage of feed water converted into permeate; higher recovery requires suitable pretreatment and careful scaling control. 3 Energy figures represent the RO process and exclude some site loads, such as raw-water pumping, post-treatment, lighting, and buildings. 4 Operating costs include typical energy, chemicals, routine labor, filters, and periodic membrane replacement; they exclude financing, depreciation, and major civil repairs.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
