10 Tips to Choose the Best Carbon Steel Plates Supplier
Choosing the right Carbon Steel Plates Supplier can protect your project from costly delays, weak documentation, and inconsistent plate quality. A reliable supplier should offer more than competitive pricing. They should demonstrate traceable mill certificates, accurate dimensions, suitable grades, and dependable delivery records.
Quality expert W. Edwards Deming stated, “Quality comes not from inspection, but from the improvement of the production process.” This principle applies directly to steel purchasing. A supplier should control production, testing, packing, and shipment before the plates reach your facility. Ask for heat numbers, chemical composition, tensile results, impact data, and inspection procedures. Check whether the supplier understands ASTM, EN, or other required specifications. Do not accept vague assurances.
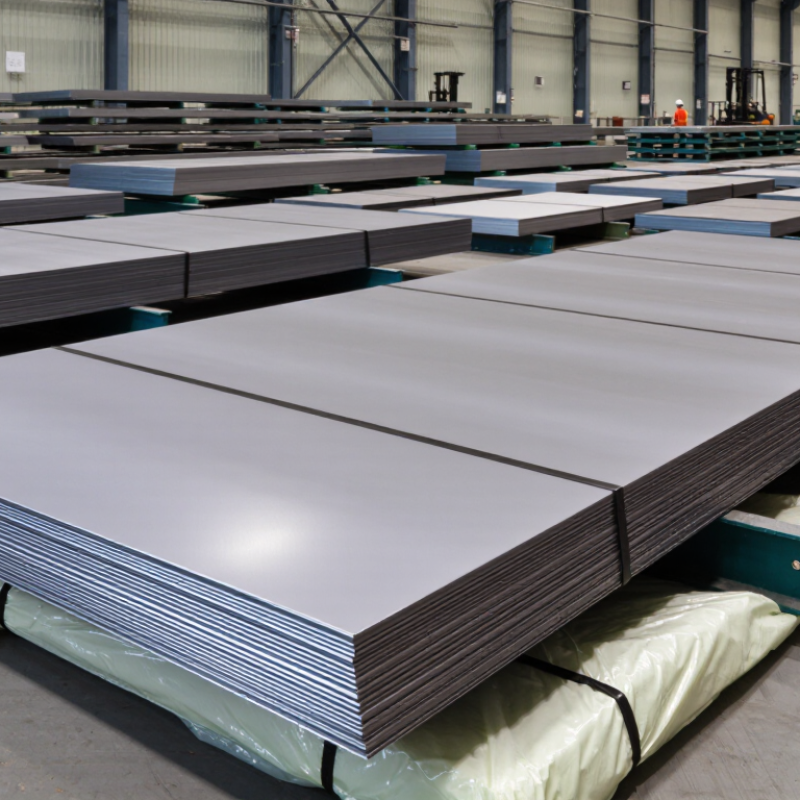
Look closely at practical details. Are plate edges clean? Are surfaces free from deep rust, laminations, and visible cracks? Does the supplier protect plates with proper separators and moisture-resistant wrapping? Small signs often reveal larger habits.
Price still matters. It should not lead the decision. A low quotation can hide poor traceability, delayed shipping, or expensive rework. Experience teaches this lesson repeatedly. Yet, supplier evaluation is never perfect. Even a respected company can struggle during sudden demand, transport disruption, or raw-material changes. That risk deserves honest discussion.
The following ten tips provide a practical framework for comparing suppliers. They focus on certification, production capability, technical support, communication, lead time, packaging, payment clarity, and after-sales responsibility. Choose evidence over promises. Verify before committing.
Define Carbon Steel Plate Grades: ASTM A36, A572, and A516 Standards
Choosing a Carbon Steel Plate Supplier starts with understanding the grade, not the sales brochure. ASTM A36 is a common structural grade for frames, brackets, base plates, and general fabrication. It offers a minimum yield strength of 36 ksi in standard plate thickness ranges. It is practical, but not automatically suitable for pressure service or severe loading.
ASTM A572 covers higher-strength low-alloy structural plates, including Grades 42, 50, 60, and 65. Grade 50 is widely selected when engineers need more strength without simply increasing plate thickness. ASTM A516 serves pressure-vessel applications, with Grades 55, 60, 65, and 70. Its suitability depends on thickness, temperature, welding procedure, and required impact performance. Grade numbers alone are not enough.
Ask the supplier for a material test certificate, heat number, chemical analysis, tensile results, and dimensional records. Check the standard edition and supplementary requirements. For A516, confirm whether the plate was normalized and whether impact testing was completed at the specified temperature. Traceability matters. A missing heat number can create serious questions during inspection. I have seen orders delayed because the certificate matched the grade but not the actual plate thickness. That mistake is avoidable. Request sample documents before placing a large order. Measure the edges, surface, and thickness when the shipment arrives. Paperwork helps, but physical verification still matters.
Compare Plate Thickness Tolerances Under ASTM A6 and EN 10029
Choosing a carbon steel plate supplier requires more than comparing price. Thickness tolerance can affect welding gaps, bending allowances, and final weight. ASTM A6 and EN 10029 are not interchangeable references.
ASTM A6 assigns thickness tolerances through tables linked to nominal thickness and plate dimensions. EN 10029 uses defined tolerance classes, commonly identified as A, B, C, or D. The permitted deviation may change with thickness range and selected class.
Check the purchase order carefully. “To standard” is too vague.
During receiving inspections, measure several points across the plate, not only the center. A micrometer near the edge may show a different result from one near the middle. Record the nominal size, actual readings, measurement location, and instrument calibration status. Ask the supplier for the applicable edition and tolerance class. Certificates help, but they do not replace inspection.
A practical detail matters.
Do not compare a negative tolerance under ASTM A6 with an EN 10029 class without checking the tables. One may control minimum thickness, while another defines a broader permitted range. Plate width, length, flatness, and waviness also require separate review. I have seen purchasing teams choose the cheapest compliant quotation, then discover machining loss was higher than expected. The decision looked efficient, but the specification was incomplete. A stronger supplier will explain these differences clearly and provide traceable inspection records.
Assess Production Capacity, Lead Times, and Minimum Order Quantities
Tip 1: Verify production capacity before discussing price. Ask how many tons the supplier produces monthly, not just its maximum claim. Request details about rolling lines, furnace schedules, thickness ranges, and available shifts. A facility may advertise impressive capacity but struggle with a sudden 300-ton order. Ask for recent production records or inspection evidence. Small details matter.
Tip 2: Examine lead times in practical terms. Confirm the time required for raw material preparation, rolling, heat treatment, testing, and packaging. Ask whether weekends, maintenance shutdowns, or port congestion affect delivery. Reliable suppliers provide a written schedule with realistic milestones. In my experience, vague promises create expensive planning problems. Fast is not always dependable.
Tip 3: Clarify minimum order quantities and production flexibility. A low MOQ can help smaller buyers, but it may increase unit costs or reduce customization options. Ask whether several plate sizes can share one production run. Confirm extra charges for unusual thicknesses, cutting, surface treatment, or small batches. Also check how rejected plates are replaced. I once overlooked this point, and the correction took longer than expected. Get every quantity, tolerance, and delivery condition in writing.
Evaluate Pricing, Traceability, Certifications, and After-Sales Support
When comparing carbon steel plate suppliers, treat the initial quotation as a working document, not a final promise. Ask whether it includes cutting, testing, packaging, freight, and realistic delivery dates. Request a written price breakdown, plus the formula for future adjustments. Cheap is not clarity. An unusually low figure deserves questions, not immediate approval.
Reliable traceability connects each plate to a heat number, test certificate, production date, and shipment record. Ask how these records are preserved and matched during loading. Photographs of markings can help, but they should support documents rather than replace them. During a warehouse visit, compare plate markings with the mill certificate and packing list. Small mismatches matter. An experienced supplier should explain them without defensiveness.
Check certificates against your required grade, thickness tolerance, testing method, and destination regulations. Do not accept impressive logos without verifiable certificate numbers or issuing-body details. After-sales support becomes visible when plates arrive late, damaged, or outside tolerance. Ask who handles claims, how quickly replies arrive, and which evidence is required. Put response times in the contract. A common procurement mistake is focusing so heavily on price that technical communication gets ignored. The decision may look efficient at first, but slow replies can create costly production delays. Your own checklist may be incomplete, especially when specifications are vague.





