


How to Choose Stainless Steel Mesh Sheet in 2026?

Choosing the right Stainless Steel Mesh Sheet in 2026 requires more than comparing price, opening size, and surface appearance. The global stainless steel industry remains substantial. World Stainless reported approximately 62 million metric tons of crude stainless steel production in 2024, showing the material’s continuing industrial importance. Demand is also supported by filtration, food processing, chemical equipment, construction, and energy applications.

J. R. Davis, editor of ASM’s Specialty Handbook: Stainless Steels, states, “Stainless steels are iron-base alloys containing a minimum of about 11% chromium.” That chromium content supports passive-film formation, but it does not make every mesh suitable for every environment. A 304 mesh may perform well around food-processing equipment, while 316 mesh offers stronger resistance in chloride-rich conditions. Wire diameter, weave type, aperture tolerance, tensile strength, and edge stability also affect real performance. Small details matter.

Reports from Grand View Research and MarketsandMarkets indicate continued growth in industrial filtration and metal-mesh applications, although forecasts differ by methodology. That difference deserves attention. Market reports are useful, not perfect. No selection guide can predict every site.

A practical evaluation should match the mesh to temperature, chemicals, pressure, cleaning methods, and required service life. For example, a 100-micron opening may improve particle capture, but it can also increase pressure loss and clogging risk. Buyers should request mill certificates, alloy verification, dimensional inspection records, and sample testing before approval. The cheapest sheet may become expensive after premature replacement. Sometimes, the “best” specification is still wrong.
How to Choose Stainless Steel Mesh Sheet in 2026?

Define Mesh Type, Aperture, and Terminology Under ISO 9044 and ASTM E2016

How to Choose Stainless Steel Mesh Sheet in 2026?

Choosing stainless steel mesh sheet starts with clear terminology. Under ISO 9044, woven wire cloth is described through mesh count, wire diameter, and aperture. ASTM E2016 also defines key terms for industrial woven wire cloth. These references reduce confusion between nominal mesh and actual opening size. Mesh type matters too. Plain weave suits general screening and filtration. Twilled weave supports heavier wires and smaller openings. Dutch weave offers strong filtration, but its structure needs closer inspection.

Aperture is the clear space between adjacent wires. Measure it carefully, not by appearance alone. A 1 mm aperture may behave differently with thicker wires and a lower open area. Check the wire diameter, mesh count, open area, material grade, and sheet tolerance. In real purchasing work, drawings often show mesh count but omit aperture. That omission can cause avoidable fitting problems. I still recheck supplier data against the applicable standard. Small errors become visible after cutting.

Tips: Ask for a test report and a dimensional inspection record. Confirm whether the sheet is plain, twilled, or Dutch woven. Compare measured aperture with the specified value. Do not rely on mesh count alone. Check edge condition, flatness, and cutting direction. If the specification looks incomplete, pause before ordering. A practical sample test may reveal clogging, weak edges, or unexpected flexibility. Sadly, even careful specifications can leave one detail unclear.


Select 304 or 316 Stainless Steel Using Corrosion Data and 2–3% Molybdenum

Choosing stainless steel mesh sheet in 2026 should begin with the environment, not the lowest quotation. 304 stainless steel suits many indoor, dry, and mildly humid applications. It contains little molybdenum. Chloride exposure changes the decision. Salt spray, coastal air, cleaning chemicals, and trapped moisture can trigger pitting. The holes do not prevent corrosion. They can create deposits around wires and intersections.

316 stainless steel normally contains about 2–3% molybdenum. This addition improves resistance to localized pitting and crevice corrosion, especially when chlorides are present. It does not make the mesh corrosion-proof. Concentration, temperature, oxygen levels, surface finish, and contact with other metals still matter. For a coastal filter or washdown screen, compare corrosion data at the actual service temperature. A generic “marine grade” claim is weak evidence. Request the material certificate, chemistry range, wire diameter, and test method.

Inspect the mesh after installation. Look at cut edges, welds, folded corners, and areas where water dries slowly. These locations often fail before open surfaces. I would choose 304 for controlled interiors after checking the cleaning process. I would consider 316 when salt or chlorides are continuous. Yet over-specifying 316 can waste money without improving service life. That is an uncomfortable point. Material selection needs records, not instinct. Recheck the choice if the chemical recipe, temperature, or maintenance schedule changes.

How to Choose Stainless Steel Mesh Sheet in 2026?

Select 304 or 316 stainless steel by comparing molybdenum content and the approximate Pitting Resistance Equivalent Number (PREN). PREN is estimated as: Cr + 3.3Mo + 16N.

Representative chemistry values are based on commonly specified compositions for 304 and 316 stainless steels. Type 304 contains virtually no molybdenum and is generally suitable for normal atmospheric and indoor environments. Type 316 typically contains about 2–3% molybdenum, providing a higher PREN and improved resistance to chloride-related pitting in coastal, marine, and chemical-processing environments. Actual performance also depends on temperature, chloride concentration, surface condition, welding, and exposure time.

Calculate Open Area from Mesh Count and Wire Diameter

How to Choose Stainless Steel Mesh Sheet in 2026?

Calculate Open Area from Mesh Count and Wire Diameter

Open area determines how much air, liquid, or light can pass through stainless steel mesh. Mesh count means the number of openings across one inch. Wire diameter changes the available space between wires. Use consistent units before calculating.

For inch-based specifications, the formula is: Open area (%) = 1 − (mesh count × wire diameter)2 × 100.

For example, 100 mesh with a 0.0045-inch wire gives a pitch of 0.010 inches. The clear opening is 0.0055 inches, and the calculated open area is about 30.25%.

Small changes matter.

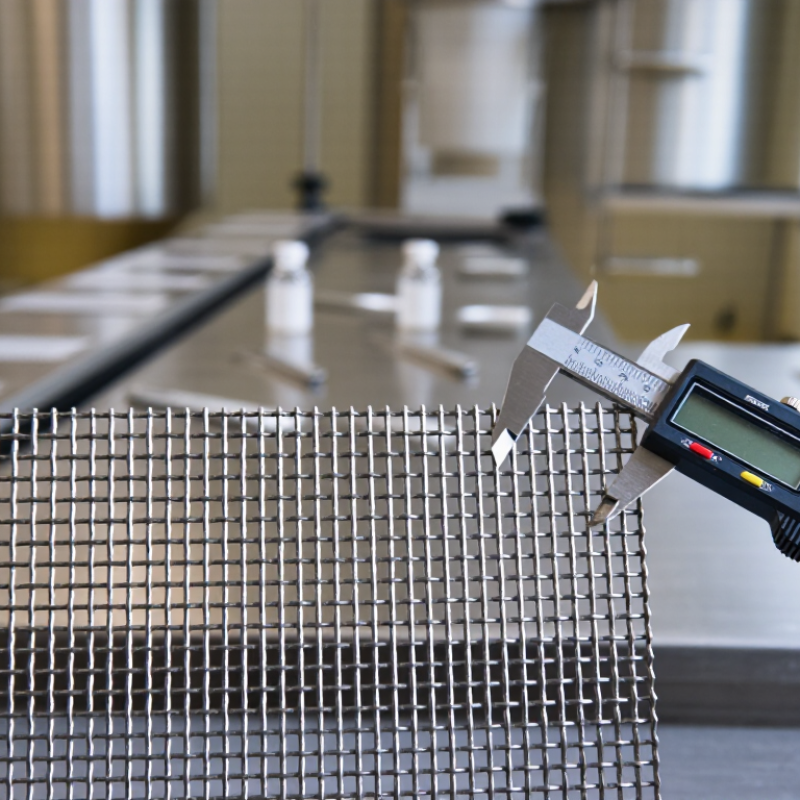
In practical purchasing, do not trust mesh count alone. Two sheets with the same mesh count may have different open areas because their wire diameters differ. Ask for the nominal aperture, wire tolerance, weave type, and inspection method. A caliper can check wire diameter, but measuring tiny openings requires care. Optical measurement is often more reliable. I have found that catalog values can look precise while actual sheets vary slightly after weaving, cutting, or tensioning.

Tips: Write mesh count and wire diameter in the same unit. Check whether the supplier counts openings or wires. Compare calculated open area with the test report. Leave allowance for manufacturing tolerance. A perfect calculation still needs physical verification.

Verify Wire Diameter and Aperture Tolerances Under ASTM A580

How to Choose Stainless Steel Mesh Sheet in 2026?

Verify Wire Diameter and Aperture Tolerances Under ASTM A580

A stainless steel mesh sheet can look precise while failing a simple measurement. ASTM A580/A580M helps verify stainless steel wire requirements, including specified wire diameter tolerances. It should not be treated as the only authority for mesh opening dimensions. Confirm the applicable mesh standard and purchase specification before approval.

Request the material certificate and record the alloy, wire diameter, lot number, and inspection date. Use a calibrated micrometer for wire measurements. Check wires at several locations, not only near the sheet edge. Measure both warp and weft wires. Small differences can change flow rate, filtration performance, and sheet weight.

Measure aperture size with an optical comparator or calibrated microscope. Inspect the center, corners, and cut edges separately. A sample may pass in the center but fail near a distorted edge. I have seen this happen after careless handling. One reading is not enough. Record the average, minimum, and maximum openings against the agreed tolerance.

Ask the supplier to identify the exact ASTM A580 edition used. Standards change, and an old certificate may not match current requirements. Also confirm whether aperture tolerances come from a separate mesh specification. This detail is easy to miss. It should not be. For critical applications, retain photographs, instrument calibration records, and measured samples with the order documents. That evidence supports a more reliable decision in 2026.

Specify 2026 Testing, Surface Finish, and Material Traceability Requirements

When choosing stainless steel mesh sheet in 2026, define testing requirements before comparing prices. Confirm mesh opening, wire diameter, sheet thickness, flatness, and allowable tolerances. Ask for inspection records, not verbal assurances. Small errors can affect filtration, airflow, and assembly fit.

Specify the material grade and required test evidence. A certified mill test report should show chemical composition, mechanical properties, heat number, and manufacturing route. Positive material identification can verify chromium and nickel content when the application is critical. Request tensile testing, dimensional checks, and corrosion-resistance testing based on the service environment. The exact standard matters. Requirements for food equipment may differ from industrial screening.

Surface finish deserves equal attention. State whether the sheet needs a bright, matte, brushed, or electropolished surface. Define roughness limits where cleaning or particle retention matters. Inspect welds, cut edges, scratches, discoloration, and embedded iron under suitable lighting. Packaging should prevent moisture marks and contact contamination during transport.

Traceability should continue from the raw coil to the finished panel. Each bundle should carry a heat number, batch reference, size, grade, and inspection status. Digital records are useful, but printed identification still helps on busy production floors. One practical weakness is assuming every certificate is complete. It may not be. Review sampling frequency, laboratory accreditation, and calibration dates before approval. Keep a retained sample when failure would be costly.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
