


Choosing Elevated Flooring in 2026 requires more than comparing panel prices. Buildings now carry heavier equipment, denser cabling, and stricter environmental expectations. A raised floor must support people, servers, air distribution, and future changes without creating unnecessary waste.
“Design for the next tenant, not only the current installation,” says Martin H. Clark, an independent raised-access-flooring consultant with more than two decades of commercial project experience. His point is practical. A floor that allows clean cable access can reduce disruption when layouts change. However, flexibility should not become an excuse for over-specification.
The right decision begins with the building’s real conditions. Measure the required floor height, concentrated loads, rolling loads, and access frequency. Check how panels behave beneath server racks, heavy storage, or mobile equipment. Consider air leakage, acoustic performance, fire classification, moisture resistance, and surface durability. A sealed edge may matter more than a fashionable finish.
Materials deserve equal attention. Steel, calcium sulphate, aluminium, and recycled-content systems offer different balances of strength, weight, cost, and embodied carbon. Product certificates should be verified, not simply accepted from a sales brochure. Installation quality matters too. Uneven pedestals, loose stringers, and poorly cut panels can undermine an excellent specification.
There is no universal answer. Sometimes a simpler system performs better. That can be overlooked. In 2026, the strongest choice will connect present performance with future adaptability. This guide examines the details, trade-offs, and quiet mistakes that influence a dependable Elevated Flooring investment.
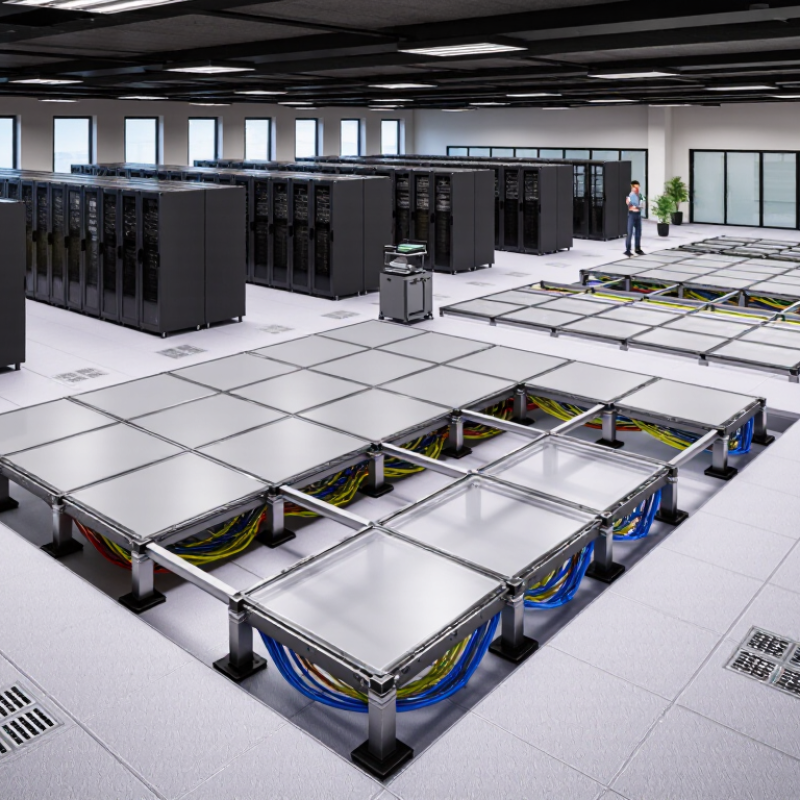
Elevated flooring, also called raised access flooring, uses removable panels supported by adjustable pedestals. This structure creates an open space beneath the walking surface. Cables, power lines, data connections, and air ducts can pass through this plenum. Maintenance becomes easier because technicians can lift selected panels instead of breaking concrete or removing finished flooring.
It is widely used in data centers, offices, control rooms, laboratories, and telecommunications spaces. It also suits renovated buildings where new services must pass through existing floors. In a data center, the underfloor space may help distribute cooling air. Airflow matters. However, not every system supports underfloor air delivery. The design must match the room’s cooling strategy.
Selection should begin with load requirements, floor height, panel material, and expected maintenance frequency. Heavy cabinets need stronger panels and carefully spaced supports. Areas with moisture may require sealed edges or corrosion-resistant components. Fire performance, electrical grounding, slip resistance, and accessibility should follow applicable local regulations. A common mistake is choosing height based only on today’s cables. Future upgrades often need more room. The answer is not always the tallest system. Greater height can affect ramps, doors, stairs, and structural limits. I would also inspect sample panels before purchase, because small flexing or poor edge alignment becomes noticeable under office chairs. Some decisions remain uncertain until the building survey is complete.

Elevated flooring now supports power, cooling, and safer maintenance. Its choice depends on the room, not fashion. A data center may need steel panels with bolted stringers. Offices often use lighter, stringerless panels. Calcium sulfate panels offer strong fire performance and sound control. Steel encapsulated panels resist moisture and rolling loads. Aluminum works well where corrosion resistance and lower weight matter. Woodcore panels cost less, but moisture can damage their edges.
Uptime Institute’s 2024 Global Data Center Survey reported an average PUE of 1.56. That figure keeps airflow management important. Perforated panels can supply cooling air beneath racks. However, too many openings may weaken pressure control.
I have seen layouts fail because airflow was estimated from drawings alone. Measure actual leakage, cabinet density, and future equipment loads.
The 2024 Global Status Report for Buildings and Construction highlights the sector’s continuing energy burden. Material selection should therefore include embodied carbon, recycled content, and service life. Calcium sulfate may suit permanent interiors. Reusable steel panels may suit frequently changing technical spaces.
Check concentrated-load ratings, rolling-load ratings, surface resistance, and fire classifications. Ask for tested data, not sales estimates. No system is perfect. A cheaper panel can become expensive after repeated replacements. Conversely, an oversized system may waste budget and embodied materials. Forecast ten-year loads before selecting panel thickness, pedestal height, and access strategy.
How to Choose Elevated Flooring in 2026?
Choosing elevated flooring starts with the load, not the finish. Calculate permanent loads from panels, pedestals, cables, equipment, and partitions. Then add people, carts, storage, and maintenance activity. Point loads matter more than average loads in many rooms. A narrow equipment foot can stress one panel severely. Check rolling loads near doors and service routes. Ask a qualified structural professional to verify the design against current local requirements. Do not rely only on a supplier’s maximum rating. Test reports may reflect ideal laboratory conditions.
Height creates practical consequences. Measure the available floor-to-ceiling space before selecting the system. A taller cavity may improve services access, but it can reduce headroom. It may also affect stairs, ramps, doors, sprinklers, and ventilation. Allow space for panel removal and safe maintenance. Tight clearances look efficient on drawings. They can become frustrating onsite. A small mistake here can force expensive changes later.
Accessibility must be reviewed from the user’s perspective. Keep walking surfaces stable, level, and free from unexpected movement. Control thresholds where the elevated floor meets existing areas. Confirm ramp gradients, landing sizes, handrails, and clear routes under applicable local standards. Consider wheelchairs, walking frames, delivery carts, and people with limited vision. Use contrasting edges where a level change remains necessary. A common site lesson is uncomfortable: technical compliance does not always feel accessible. Walk the route with different users before installation, and revise details that seem acceptable only on paper.
This chart shows the minimum ramp run required for common elevated-floor heights when applying a 1:12 maximum slope. The calculation is simple: ramp run = vertical rise × 12. For example, a 300 mm floor height requires at least 3.6 m of ramp length. Actual projects must also verify landings, handrails, edge protection, turning space, and local accessibility regulations.
Load capacity must be checked separately from height. As a screening reference, a typical office live-load requirement is approximately 2.4 kPa, equivalent to 50 psf under commonly used building-code tables. The selected raised-floor system must also be verified for concentrated loads, rolling loads, equipment loads, and the supporting structural slab.
Reference basis: a 1:12 maximum ramp slope is commonly used for accessible routes under ADA guidance; 2.4 kPa is a rounded conversion of 50 psf for office areas. Confirm all requirements with the applicable local code and structural engineer.
Choosing elevated flooring in 2026 starts with the room’s operating pattern, not the catalog. Record equipment loads, trolley routes, finished-floor height, and future cable changes. A 600 mm panel may simplify access, while smaller panels can reduce handling risks in tight rooms. Ask installers for a sequencing plan, including subfloor preparation, pedestal bonding, and tolerance checks. Measure twice. Installation labor often exceeds material assumptions, especially in occupied spaces requiring night work.
Compare installed cost, then model ten-year lifecycle cost under ISO 15686-5 principles. Include panels, pedestals, ramps, bonding, cleaning, spare stock, and planned relocations. Maintenance should be tested physically. Lift one panel, inspect edge protection, and check whether technicians can work without damaging nearby finishes. Specify static and rolling-load ratings separately; static capacity alone can mislead. Access matters. The U.S. EPA estimates 600 million tons of construction and demolition debris were generated in 2018, so damaged panels should not automatically become waste (EPA, 2020). A reuse plan needs compatible dimensions and documented condition.
Sustainability comparisons need evidence, not green wording. Request an EPD, recycled-content disclosure, repair instructions, and an end-of-life pathway. UNEP’s 2024 Global Status Report states that buildings and construction consume 32% of global energy and produce 34% of energy- and process-related CO2 emissions. Flooring is only one component, but repeated replacement still matters. I would question any low-carbon claim without declared scope and independent verification. Cost models also need carbon, downtime, and disposal sensitivity. No estimate is perfect. A transparent spreadsheet is better than a polished promise.
Selecting the best elevated flooring system starts with the room’s real demands. Measure equipment weight, service access, moisture exposure, and finished floor height. A server room needs stable panels and reliable airflow control. A laboratory may require chemical resistance and easy cleaning. An office renovation may value quick installation and quiet movement.
On one recent fit-out, our first panel choice was too heavy for the existing structure. We changed the layout after checking the structural drawings. That mistake cost time, but it prevented a larger safety problem. Ask an engineer to verify point loads, rolling loads, seismic needs, and deflection limits. The support structure should sit evenly on a prepared, level surface. Small height errors become obvious near doorways.
Check the system’s fire performance, slip resistance, acoustic behavior, and environmental documentation. Confirm that panels can be lifted without damaging nearby furniture or cables. Removable sections should allow technicians to reach power, data, and ventilation services quickly. In 2026, sensor-ready designs can help monitor temperature, humidity, and underfloor air quality. Still, connected features are not automatically useful. They need clear maintenance plans and secure data handling. Request test reports, installation guidance, replacement availability, and a realistic lifecycle estimate. Local building requirements may differ, so independent professional review remains important. Some systems look efficient on paper. They may disappoint on site.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

